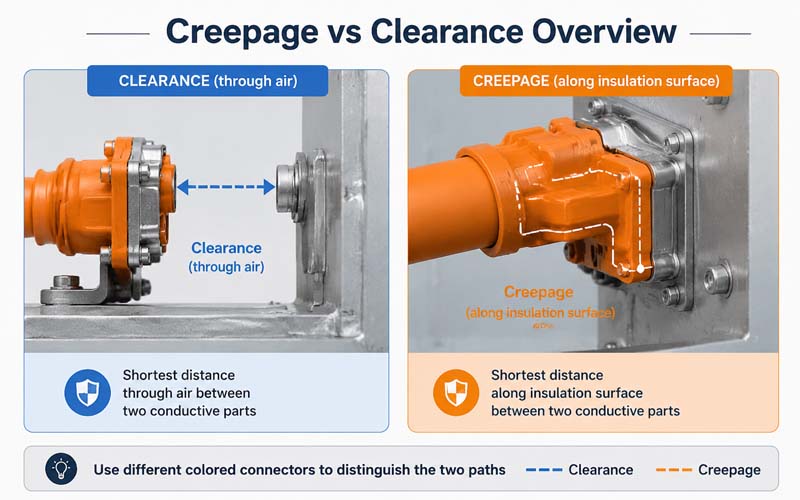
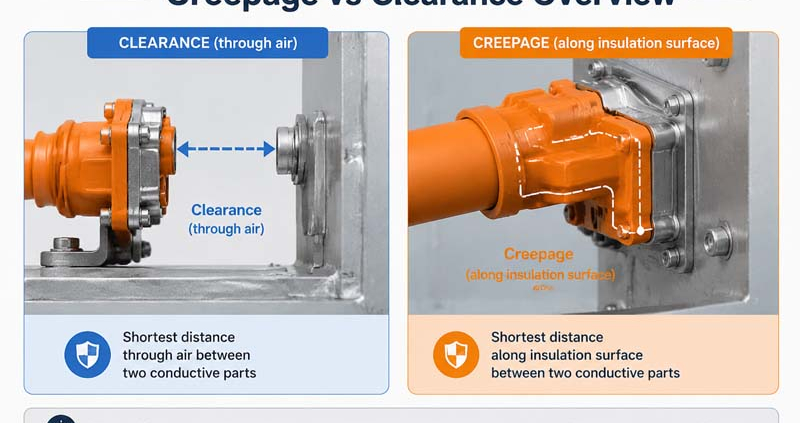
Creepage vs Clearance Overview

In high-voltage connectors design, electrical safety depends on much more than conductor size and insulation thickness.

Two of the most fundamental design parameters are creepage distance and clearance distance.

These dimensions determine how effectively a connector can withstand operating voltage, transients, humidity, contamination, and aging without flashover or tracking.

Whether you are designing connectors for electric vehicles (EVs), battery energy storage systems (ESS), charging equipment, or industrial power electronics, understanding creepage and clearance is essential.

This article explains the basic concepts, design rules, and validation considerations engineers should know.


What Is Clearance?

Clearance is the shortest distance through air between two conductive parts at different electrical potentials.

Examples include:

  • adjacent terminals
  • terminal to shield
  • terminal to connector shell
  • live parts to chassis ground

If clearance is insufficient, arcing may occur during voltage transients or at high altitude.


What Is Creepage?

Creepage is the shortest path along the surface of an insulating material between two conductive parts.

This path follows the connector housing rather than passing directly through air.

Insufficient creepage can lead to:

  • surface tracking
  • carbonization
  • insulation degradation
  • eventual electrical failure
  • Creepage vs Clearance Overview

Why Both Distances Matter

Clearance addresses air breakdown risk.

Creepage addresses surface leakage and contamination risk.

Both must meet applicable standards and application-specific requirements.


Factors Affecting Required Distances

Required creepage and clearance depend on several variables.

Operating Voltage

Higher voltage requires larger separation distances.

Transient Overvoltage

Switching events and fault conditions may create voltages significantly above nominal levels.

Pollution Degree

Defines the expected environmental contamination level.

Typical classifications:

  • Pollution Degree 1: controlled indoor environment
  • Pollution Degree 2: light non-conductive contamination
  • Pollution Degree 3: conductive contamination or condensation

Material Group (CTI)

Comparative Tracking Index (CTI) measures resistance to surface tracking.

Higher CTI materials can permit shorter creepage distances.

Altitude

Air insulation strength decreases as altitude increases, often requiring increased clearance.

Safety Standard Requirements

Applicable standards may define minimum distances and correction factors.


How Connector Designers Increase Creepage Distance

Design techniques include:

  • insulating ribs
  • barriers
  • recessed terminals
  • tortuous surface paths
  • optimized terminal orientation

These features increase surface distance without significantly enlarging connector size.


Clearance Optimization Techniques

Methods to improve clearance include:

  • wider terminal spacing
  • insulation walls
  • shield isolation
  • careful tolerance control

3D CAD analysis is often used to verify minimum distances.


Common Design Mistakes

Using Nominal Dimensions Only

Manufacturing tolerances may reduce actual distances.

Ignoring Contamination

Real-world environments can be more severe than expected.

Overlooking Altitude

Reduced air density lowers dielectric strength.

Neglecting Aging

Materials may degrade over time.

Assuming Creepage and Clearance Are Interchangeable

They address different failure mechanisms.


Example Applications

Typical high-voltage connector applications include:

  • EV battery pack connectors
  • inverter interfaces
  • onboard chargers
  • DC fast charging connectors
  • ESS battery interconnects

Each application may have unique safety requirements.


Validation Methods

Design assumptions should be verified by:

  • dielectric withstand (HiPot) testing
  • insulation resistance measurement
  • humidity conditioning
  • contamination testing
  • thermal cycling
  • altitude testing where applicable

Validation confirms that theoretical spacing performs under real conditions.


Relevant Standards

Common standards include:

  • IEC 60664-1
  • IEC 62109
  • IEC 61800
  • UL 840
  • ISO 6469
  • OEM high-voltage specifications

The applicable standard depends on the end product and market.


Practical Design Trade-Offs

Increasing creepage and clearance generally improves safety, but may also:

  • enlarge connector size
  • increase material cost
  • affect mating force
  • complicate packaging

The goal is to meet requirements efficiently while preserving manufacturability.


How FPIC Supports High-Voltage Connector Development

FPIC designs and manufactures high-voltage connectors and cable assemblies for EV, ESS, and industrial systems.

Our engineering support includes:

  • creepage and clearance review
  • material selection guidance
  • HVIL integration
  • sealing and shielding design
  • HiPot and insulation testing

We help customers balance electrical safety, packaging, and cost.


Final Thoughts

Creepage and clearance are foundational elements of high-voltage connector design.

A robust design must consider:

  • voltage level
  • environmental conditions
  • insulation material properties
  • tolerances
  • applicable standards

Understanding these principles early helps prevent costly redesigns and improves product safety.


FAQ

What is the difference between creepage and clearance?

Clearance is distance through air; creepage is distance along an insulating surface.

Why is CTI important?

Higher CTI materials resist tracking better and may allow shorter creepage distances.

Does altitude affect connector design?

Yes. Higher altitude reduces dielectric strength of air, increasing required clearance.

Can barriers increase creepage distance?

Yes. Ribs and barriers create longer surface paths.

How are these distances verified?

Through CAD analysis and electrical validation testing such as HiPot.


Designing a High-Voltage Connector?

FPIC provides engineering support and manufacturing for custom high-voltage connectors and cable assemblies with optimized insulation design and validated performance.

Contact us to discuss your application requirements.


Resources

  1. IEC 60664-1 – Insulation Coordination for Low-Voltage Systems
    Core standard for creepage and clearance requirements.
  2. UL 840 – Insulation Coordination Including Clearances and Creepage Distances
    North American guidance for electrical spacing.
  3. ISO 6469 – EV Safety Requirements
    Safety specifications for electrically propelled vehicles.
  4. TE Connectivity – High Voltage Connector Design Guide
    Practical connector design considerations.
  5. Molex – High-Voltage Connectivity Solutions
    Application guidance for EV and energy systems.
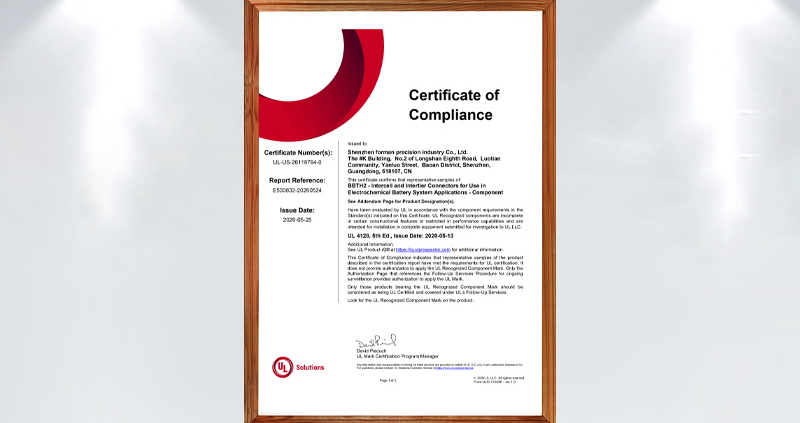
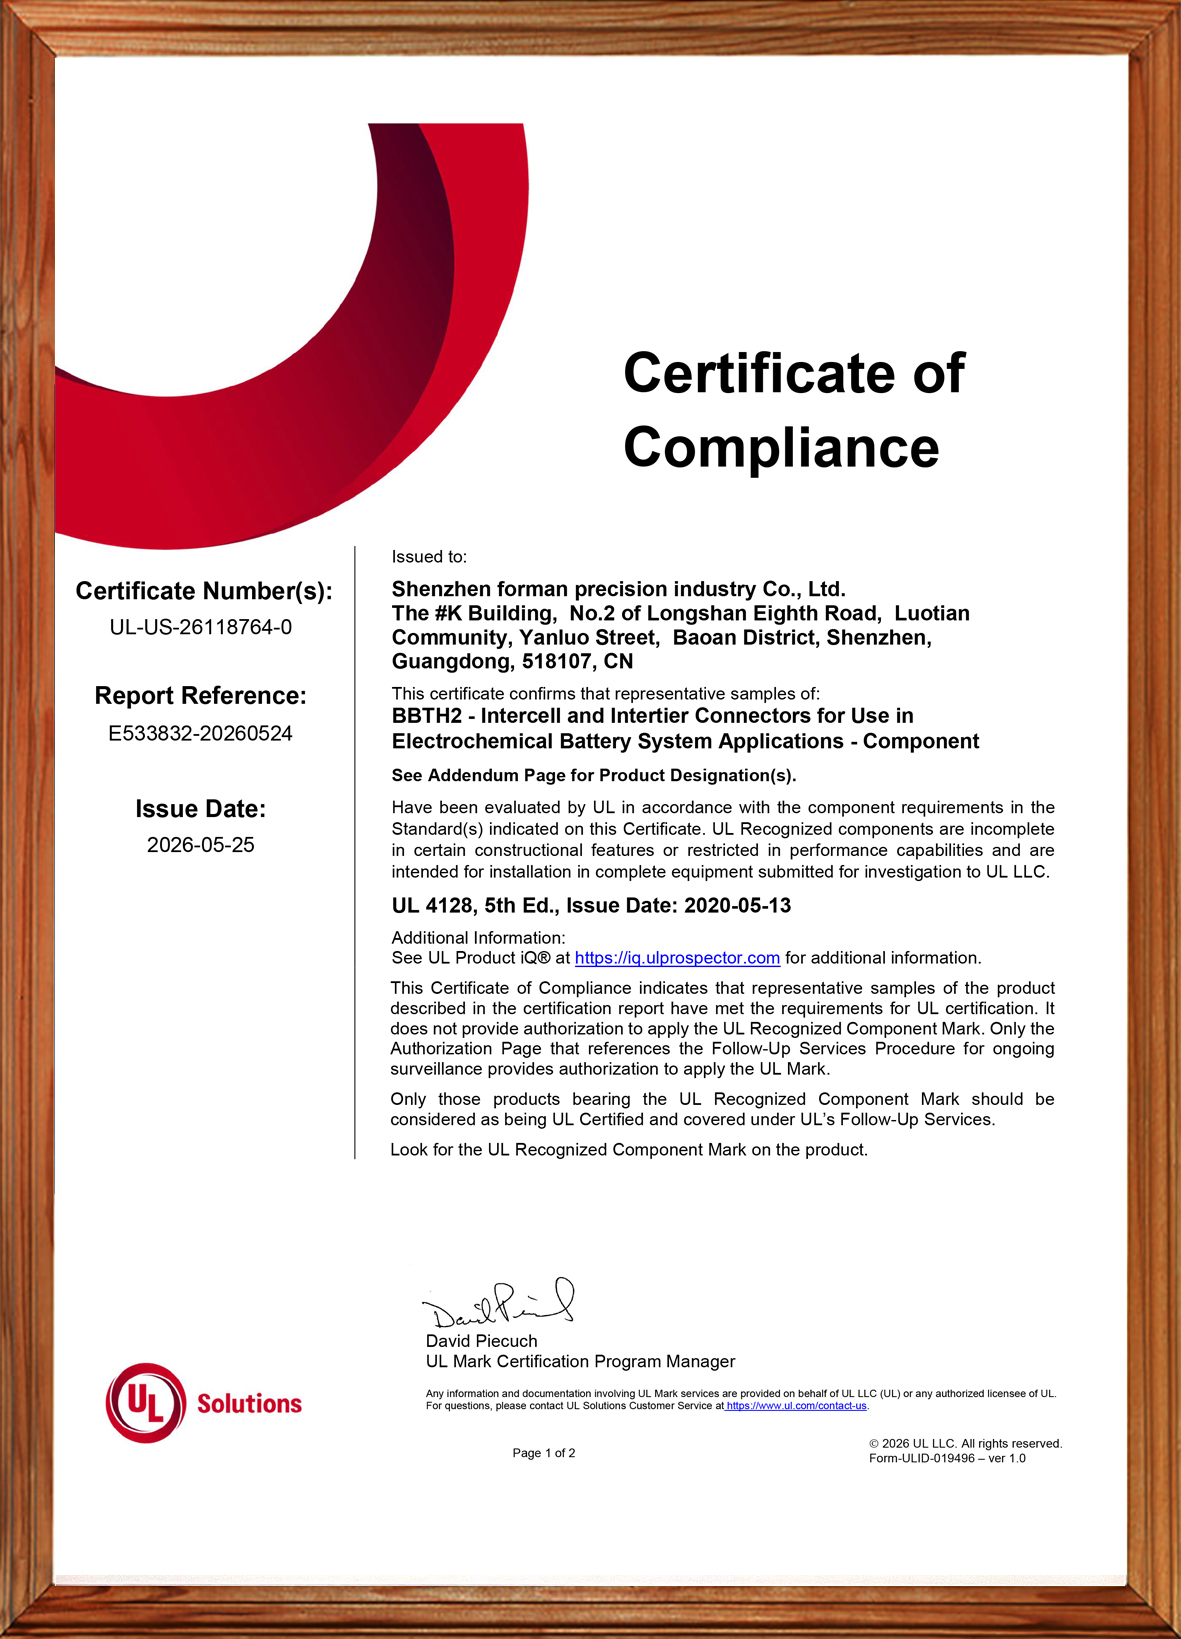
450A energy storage connector UL certificate

FPIC is pleased to announce that representative samples of our 2000V 450A energy storage connector series have been evaluated by UL for use in electrochemical battery system applications. The certification documents identify the product under UL 4128, 5th Edition, covering intercell and intertier connectors for battery system use.

This milestone strengthens FPIC’s capability in high-current battery interconnection solutions and provides additional confidence for customers developing energy storage equipment, battery packs, and related power distribution systems.
What This Certification Covers

According to the UL Certificate of Compliance, the evaluated product category is BBTH2 – Intercell and Intertier Connectors for Use in Electrochemical Battery System Applications – Component, with certificate number UL-US-26118764-0 and report reference E533832-20260524. The issue date is 2026-05-25.

The corresponding UL report describes the product as:

  • Cable Connectors
    Cat. Nos. A083-1F14-C150N-6A-##, A083-1F14-C150N-5A-##, A083-1F14-C150N-0A-##
  • Panel Mounted Inlets
    Cat. Nos. A083-2M14-E014F-6A-##, A083-2M14-E014F-5A-##, A083-2M14-E014F-0A-##

The report also states the key ratings of this series as 2000V DC and 450A. For the cable connector version, the evaluated conductor size is 300 kcmil.

FPIC 450A Energy Connector Meets UL 4128

Why This Matters for Energy Storage Applications

High-current battery connection points in energy storage systems demand more than basic electrical performance. They also require controlled insulation design, reliable mating, proper polarity identification, and suitability for integration into complete battery equipment.

The UL report identifies these products as intercell/intertier connectors intended for use in electrochemical battery equipment, including cable connector and panel mounted inlet configurations. The panel mounted inlet versions are intended for factory assembly onto copper conductors rated 90°C or higher and/or copper or copper alloy busbars in battery equipment.

For ESS manufacturers, battery pack integrators, and related equipment developers, this provides an important compliance reference point when evaluating connector solutions for high-voltage, high-current battery system designs.

Key Product Characteristics

Based on the UL report, FPIC’s 450A connector series includes the following core characteristics:

1. High Voltage and High Current Capability

The evaluated series is rated at 2000V DC and 450A, supporting demanding battery interconnection applications.

2. Cable and Panel-Mounted Configurations

The series includes both cable connector and panel mounted inlet versions, helping customers build matching connection interfaces for different battery system architectures.

3. Single-Pole Intercell / Intertier Connector Design

The report describes the cable connector products as insulated, single-pole mating intercell/intertier connectors, suitable for battery system connection needs.

4. Support for Battery Equipment Integration

The panel mounted inlet versions are intended for assembly to busbars or conductors in electrochemical battery equipment, which is especially relevant for energy storage cabinets, battery packs, and related systems.

Important Compliance Note

The UL certificate clearly states that these are UL Recognized components, not complete end-use equipment. It also states that the certificate itself does not provide authorization to apply the UL Recognized Component Mark; only products bearing the appropriate UL Recognized Component Mark and covered under UL follow-up services should be considered UL Certified within that program context.

In addition, the UL report notes that these devices are:

  • not suitable for disconnecting under load
  • not intended for use outside an equipment enclosure
  • not investigated for an environment rating
  • intended for use only in complete equipment where acceptability is determined in the end-use application

This is important for customers who are designing certified end products and need to evaluate the connector as part of the complete system.

What This Means for FPIC Customers

This UL milestone demonstrates FPIC’s continued progress in energy storage connector development and supports our ability to serve customers with more robust interconnection solutions for battery system applications.

For customers working on:

  • energy storage systems
  • electrochemical battery equipment
  • battery pack integration
  • power distribution interfaces
  • high-current cabinet connections

this development provides stronger confidence in FPIC’s capability to support demanding connector projects with both product development and manufacturing execution.

FPIC Energy Storage Connector Capability

FPIC has been continuously developing energy storage connector solutions for high-current and high-voltage applications. Our energy storage product direction includes connector and cable solutions designed for battery modules, battery packs, and related ESS equipment. FPIC’s internal product materials also describe energy storage connectors with features such as touch-proof design, multiple connection methods, and compliance direction aligned with UL 4128.

This new 450A certification-related progress further strengthens FPIC’s position in the energy storage connector segment.

Contact FPIC for Energy Storage Connector Projects

If you are developing battery packs, ESS cabinets, or related electrochemical battery equipment and need a reliable high-current connector solution, FPIC can support your project with product information, engineering communication, and manufacturing support.

Contact us to discuss your application requirements.

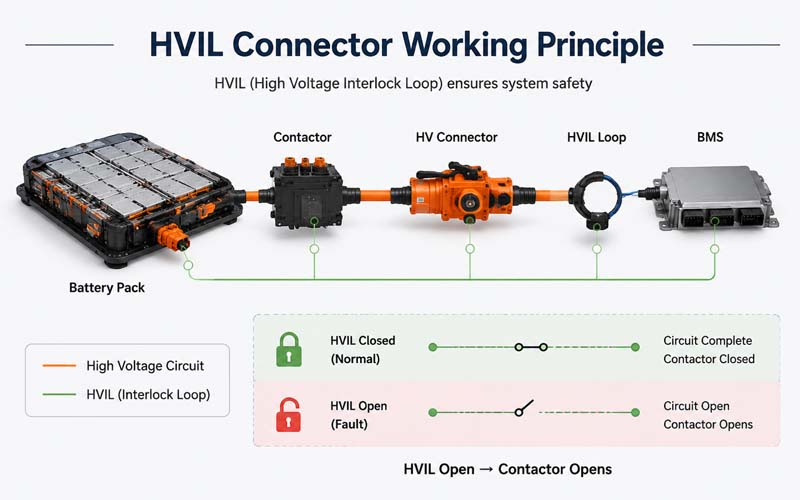
HVIL Connector Working Principle

In electric vehicles (EVs), battery energy storage systems (ESS), and other high-voltage applications, electrical safety extends far beyond insulation and creepage distance.

One of the most important safety mechanisms is the High Voltage Interlock Loop (HVIL).

HVIL circuits continuously monitor whether high-voltage connectors, service disconnects, and enclosures are properly engaged. If the loop is interrupted, the control system immediately disables the high-voltage contactors.

Although the HVIL circuit carries only a low-voltage signal, its reliability is essential to the safe operation of the entire system.

This article explains how HVIL connectors work, common failure modes, and the validation tests used to ensure robust performance.

HVIL Connector Working Principle


What Is HVIL?

HVIL stands for High Voltage Interlock Loop.

It is a low-current monitoring circuit that passes through:

  • battery pack connectors
  • inverter connectors
  • onboard chargers
  • DC fast charging interfaces
  • service disconnects
  • high-voltage enclosures

When all connectors are fully mated and covers are closed, the loop remains intact.

If any component is opened or partially disconnected, the loop opens and the system shuts down high voltage.


Why HVIL Is Important

HVIL helps protect:

  • service technicians
  • assembly operators
  • end users
  • vehicle electronics

Typical safety functions include:

  • disabling contactors before connector separation
  • detecting incomplete mating
  • monitoring service access covers
  • preventing energized exposure

In most EV architectures, HVIL is part of the functional safety strategy.


Basic HVIL Operating Principle

The battery management system (BMS) or vehicle control unit injects a low-voltage signal through the interlock loop.

The controller monitors:

  • loop continuity
  • resistance value
  • voltage level

If the signal falls outside expected limits, a fault is triggered.

Some systems use simple open/closed detection, while others use resistor coding to identify specific components.


HVIL Connector Design Features

A dedicated HVIL connector typically includes:

  • two low-voltage interlock contacts
  • staggered contact lengths
  • early-break / late-make sequencing
  • CPA locking features
  • sealed housing
  • mechanical polarization

The HVIL contacts are usually designed to disconnect before the high-voltage power contacts separate.


Early-Break / Late-Make Concept

HVIL contacts are intentionally longer or shorter than power contacts.

During Unmating

The HVIL circuit opens first, allowing contactors to open before high-voltage contacts separate.

During Mating

Power contacts are fully engaged before the HVIL loop closes.

This sequencing is critical to system safety.


Common HVIL Failure Modes

1.Contact Fretting

Micro-motion can increase resistance and cause intermittent loop faults.

2.Incomplete Mating

If the connector is not fully seated, HVIL continuity may be unstable.

3.Terminal Back-Out

Improper terminal retention can interrupt the circuit.

4.Corrosion or Water Ingress

Moisture may increase resistance or cause open circuits.

5.Broken HVIL Wires

Small-gauge wires are vulnerable to fatigue and handling damage.

6.Contaminated Contacts

Debris or oxidation can degrade signal integrity.


Design Considerations for Reliable HVIL Performance

Key design priorities include:

  • stable low-current contact resistance
  • robust terminal retention
  • vibration-resistant locking
  • environmental sealing
  • clear mating confirmation
  • protected wire routing

Because HVIL circuits carry very low current, they are especially sensitive to contamination and fretting.


Validation Test Points

Typical validation activities include:

  • contact resistance measurement
  • mating and unmating force
  • terminal retention force
  • vibration testing
  • thermal cycling
  • humidity exposure
  • salt spray
  • sealing tests
  • mechanical shock

Functional monitoring should verify that the HVIL circuit opens and closes in the correct sequence.


Critical Functional Checks

During validation, engineers should confirm:

  • HVIL opens before power contacts disengage
  • HVIL closes only after full mating
  • resistance remains within specification
  • no intermittent opens occur during vibration
  • CPA and locking systems function correctly

Standards and Specifications

Relevant standards may include:

  • LV214
  • USCAR-2
  • OEM high-voltage connector specifications
  • ISO 6469
  • ISO 26262

Requirements vary by customer and application.


Typical Applications

HVIL connectors are widely used in:

  • EV battery packs
  • inverters
  • PDU (Power Distribution Units)
  • onboard chargers
  • DC fast charge systems
  • ESS battery cabinets

How FPIC Supports HVIL Connector Projects

FPIC provides custom high-voltage connector and cable assembly solutions with:

  • integrated HVIL circuits
  • sealed connector designs
  • CPA and TPA features
  • continuity, IR, and HiPot testing
  • application engineering support

We help customers develop reliable high-voltage interconnect systems for EV and energy applications.


Final Thoughts

HVIL connectors carry only a low-voltage signal, but they play a critical role in high-voltage safety.

  • A robust design requires:
  • correct contact sequencing
  • stable low-current performance
  • secure mechanical locking
  • environmental protection
  • thorough validation

In EV systems, the reliability of the HVIL circuit is essential to protecting both people and equipment.


FAQ

What does HVIL stand for?

High Voltage Interlock Loop.

What happens when the HVIL circuit opens?

The system commands the high-voltage contactors to open and disables high voltage.

Why are HVIL contacts sequenced differently from power contacts?

To ensure the safety circuit opens before high-voltage contacts separate.

Can corrosion cause HVIL faults?

Yes. Low-current circuits are highly sensitive to contamination and corrosion.

Is HVIL required in EV systems?

It is widely used as a core safety mechanism in high-voltage architectures.


Developing High-Voltage Connectors with HVIL?

FPIC provides custom high-voltage connectors and cable assemblies with integrated HVIL solutions for EV, ESS, and industrial applications.

Contact us to discuss your design and validation requirements.


Resources

  1. ISO 6469 – Electrically Propelled Road Vehicles Safety Specifications
    Safety requirements for EV high-voltage systems.
  2. LV214 – Environmental and Electrical Requirements for Automotive Connectors
    Automotive connector validation standard widely used by OEMs.
  3. USCAR-2 – Performance Specification for Automotive Connectors
    Defines connector reliability and environmental tests.
  4. ISO 26262 – Functional Safety for Road Vehicles
    Functional safety framework for automotive systems.
  5. TE Connectivity – HVIL Design Concepts
    Technical guidance on high-voltage interlock connector design.
Plastic Mold Design Standardization Guide

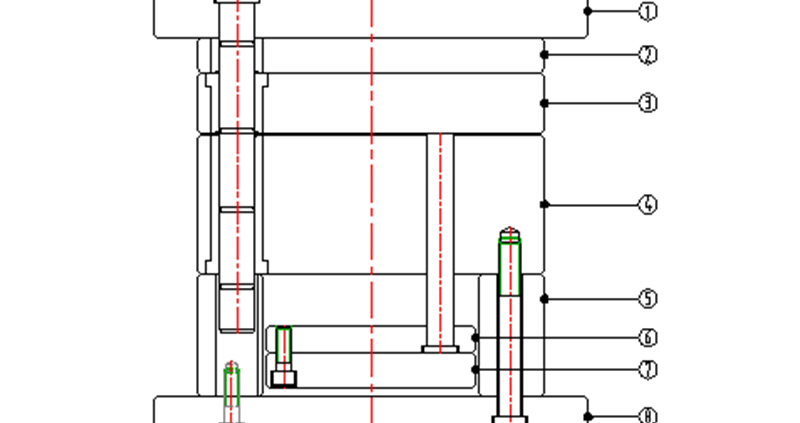
Plastic mold design standardization reduces rework, shortens lead time, improves interchangeability, and makes mass production more stable. For engineering teams, it is not just a documentation exercise. It is a practical system for mold bases, side actions, runners, gates, locating features, and ejection structures.

If you want faster mold development and more predictable molding results, standardize five things first: the mold base platform, movement structures, runner and gate logic, locating features, and ejection design. That approach helps engineering teams reduce variation, simplify purchasing, improve maintenance, and make quality more repeatable from prototype to mass production.

Below is a practical guide built from FPIC’s internal engineering standard and aligned with widely accepted industry thinking. It is written for buyers, product engineers, and mold teams who want better control over cost, quality, and launch timing.

What Plastic Mold Design Standardization Really Means

Plastic mold design standardization means using defined rules for mold platforms, standard components, structural calculations, gating logic, locating methods, and ejection choices instead of redesigning every detail from scratch. In practice, this shortens design cycles, improves repeatability, and makes molds easier to build, inspect, repair, and scale across product families.

That industry logic is consistent with FPIC’s internal engineering presentation, which starts standardization with mold-base selection, preferred materials, ordering rules, datum logic, and standard machining expectations before moving into side actions, runners, locating, and ejection.

Why Standardization Pays Off

Standardization is valuable because mold performance depends on many linked decisions. A well-defined mold base platform makes procurement and machining more predictable. Standard side-action rules reduce assembly risk. Balanced runner logic helps filling consistency. Repeatable ejection rules reduce part damage and maintenance time.

For companies serving automotive, medical, industrial, and connector programs, this matters even more. Product families often share similar geometries, tolerance expectations, and validation paths. A standardized mold design approach makes design reviews faster and engineering decisions easier to reuse.

Faster Engineering Decisions

When design rules are already clear, engineers spend less time debating routine choices and more time solving real product-specific challenges.

Better Manufacturing Consistency

Standard platforms and structures reduce dimensional variation, simplify machining, and improve assembly accuracy.

Easier Mold Maintenance

A mold built on standard logic is easier to inspect, repair, and modify during long production runs.

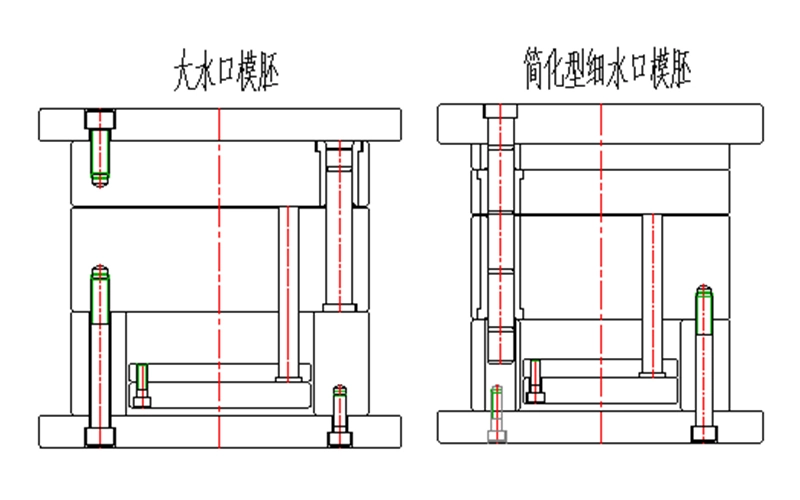
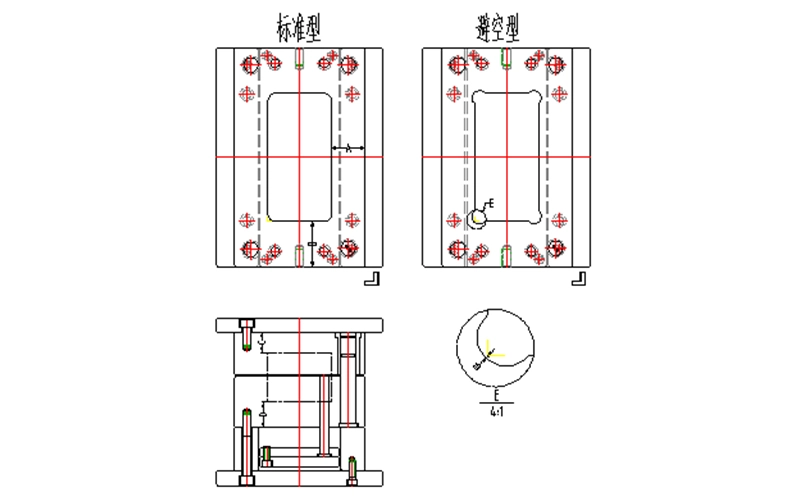
Start with a Standard Mold Base Strategy

FPIC’s engineering standard identifies two common mold-base types: a large sprue mold base and a simplified pin-point gate mold base. It also specifies common reference suppliers, mold-base material in the S50C–S55C range, and common core materials such as S136, SKD61, DC53, and VIKING. The same internal standard also requires chamfering of machined edges, default dimensioning from the datum corner unless otherwise stated, and standardized ordering logic for mold-base sizes and plate thicknesses.

Why the Mold Base Matters

The mold base is the structural foundation of the tool. A standardized base improves rigidity, purchasing efficiency, and machining predictability.

Why the Mold Base Matters

Material Selection Should Not Be Arbitrary

Mold-base and core material choices directly affect wear resistance, heat treatment stability, polishing behavior, and maintenance cycles.

Standard Ordering Reduces Errors

Using a consistent ordering format for mold-base size, plate thickness, and supplier requirements reduces communication mistakes and speeds up purchasing.

Standard Ordering Reduces Errors


Standardize Movement Structures Before They Become Problems

Slides, hydraulic side actions, first-return mechanisms, and lifters are common failure points when teams rush concept work. FPIC’s engineering standard gives clear rules here: slide geometry follows defined angular relationships, hydraulic cylinders must not be used to seal off plastic directly, first-return mechanisms are required when ejectors sit under moving members, and lifter angles are generally kept in the 3°–10° range while ensuring no interference with surrounding parts or the molded product.

Slide Design Should Follow Fixed Geometry Rules

Slide systems work best when angular relationships, guide structures, and clearance rules are standardized early.

Hydraulic Structures Need Safety Logic

Hydraulic cylinders can add flexibility, but they also introduce sealing and timing risks if used incorrectly.

Lifter Design Must Balance Motion and Part Safety

Lifters must avoid interference with both the product and neighboring components, while also preventing scraping or plastic damage during ejection.


Treat Runner and Gate Design as a System

FPIC’s internal standard treats the gating system as a structured decision set. It defines nozzle-to-sprue relationships, locating-ring use, runner cross-section choices, runner layout logic, and gate selection guidance. It specifically notes that round and trapezoidal runners are both common, that multi-cavity runner layouts should prioritize balanced filling, that H-shaped distribution generally gives better balance than T-shaped layouts, and that different gate types serve different production goals.

Runner Geometry Affects More Than Flow

Runner shape and size influence pressure drop, thermal loss, filling balance, and cycle stability.

Gate Selection Should Match the Product Goal

Submarine gates support automation. Large sprues are simple but often manual. Pin gates improve automatic separation but raise mold complexity.

Balanced Layouts Improve Multi-Cavity Stability

A balanced runner system helps ensure that all cavities fill more consistently, reducing quality variation between parts.


Make Locating Features Do More Than Just Align Parts

A good mold does not rely on memory. It relies on features that prevent mistakes. FPIC’s internal standard makes this clear by treating locating structures as a core method to prevent assembly errors and preserve mold precision. It also recommends insert-level locating to prevent rotation or incorrect assembly, and it uses anti-error design when a part is not center-symmetric or when left/right variants exist.

Mold Accuracy Starts with Repeatable Positioning

Stable locating improves assembly precision and reduces accumulated tolerance errors inside the tool.

Anti-Mistake Design Saves Real Cost

Simple anti-error structures can prevent reversed assembly, insert rotation, and rework during tool build or maintenance.


Ejection Rules Should Protect Parts and Tool Life

Ejection design is another area where standardization saves money quickly. FPIC’s internal standard prioritizes ejector placement near ribs or high-release-force areas, requires enough distance between water channels and ejector pins, encourages fewer ejector-pin size variations in a single tool, and defines when to switch from pins to sleeve ejection, push blocks, or stripper plates. It also calls for vent grooves in sleeve ejectors to reduce thermal friction and wear.

Ejector Pins Are Not Always the Best Answer

Pins are efficient, but deep bosses, thin walls, and cosmetic surfaces may require sleeves, push blocks, or stripper plates.

Standard Pin Layout Rules Improve Stability

Uniform pin placement and limited pin-size variation simplify machining, assembly, and future maintenance.

Venting and Clearance Protect the Tool

Vent grooves and proper spacing reduce friction, sticking, and heat-related wear during long production runs.


A Practical 5-Step Standardization Framework

If you want to build or upgrade your own plastic mold design standardization system, use this sequence:

Step 1 – Lock the Platform

Define preferred mold-base families, suppliers, base materials, and standard machining scope.

Step 2 – Lock the Motion Rules

Standardize slide, cylinder, first-return, and lifter geometry before detailed 3D work starts.

Step 3 – Lock the Flow Logic

Create a gating decision table by resin, part size, cosmetic requirement, and automation goal.

Step 4 – Lock Locating and Mistake-Proofing

Use consistent locating features for mold bases, inserts, and asymmetrical parts.

Step 5 – Lock the Ejection Decision Tree

Define when to use pins, sleeves, blocks, and stripper plates, plus spacing and venting rules.

This is the point where standardization stops being a document and starts becoming a productivity tool.


What Buyers and Product Engineers Should Ask Mold Suppliers

If you are outsourcing tooling, ask these five questions before approving design freeze:

  1. Do you use a standard mold-base system?
  2. How do you standardize slides, lifters, and hydraulic side actions?
  3. How do you choose runner layout and gate type for this resin and part geometry?
  4. What locating features prevent assembly mistakes and insert rotation?
  5. What is your standard ejection strategy for ribs, deep bosses, and cosmetic surfaces?

A supplier that answers clearly is more likely to control risk later.


Where FPIC Adds Value

At FPIC, we view mold design standardization as part of product quality, not just tooling efficiency. That matters for connector programs, precision plastic parts, and complex assemblies where dimensional consistency, cosmetic control, and repeatable mass production all matter. Our internal engineering standard covers mold-base selection, side-action logic, runner and gate decisions, locating, and ejection in a structured way, and it is supported by our broader manufacturing focus on automation, process discipline, and scalable production.

We do not recommend over-standardizing blindly. Some parts need exceptions. But a good standard should make exceptions visible and intentional. That is usually the difference between a mold that merely works and a mold that works predictably over time.

If you are developing precision plastic parts, connector components, or custom tooling programs, FPIC can support manufacturability review, tooling optimization, and scalable production planning.


Conclusion

Plastic mold design standardization is one of the fastest ways to improve tooling quality without adding unnecessary complexity. Done well, it reduces variation, accelerates design reviews, improves maintainability, and supports more stable mass production.

If you are evaluating a new tooling partner or trying to improve internal mold performance, start with the five areas above. If you need support on precision plastic parts, connector tooling, or manufacturability review, FPIC’s engineering and manufacturing teams can help you move from concept to stable production with fewer surprises.


References / Notes

  1. FPIC internal engineering presentation: R&D Dept., compiled by Zhu Xiaolong, 2026.04.14. This article incorporates FPIC’s internal design rules for mold bases, side actions, runners, locating, and ejection.
  2. HASCO, Specifications for Injection Moulds 2.0 and HASCO standard mold-unit information.
  3. DME, official mold-base, mold-component, CAD, and technical-guide resources.
  4. Protolabs Network (formerly Hubs), Injection Molding Design Guide.
  5. Ma et al., research on standard component libraries for plastic injection mold design.
  6. Mold-Masters, discussion of runner balance and shear effects.
Square Pin Terminals vs. Automotive Rounded Pin Terminals

A square pin terminal works well in standard PCB headers and low-vibration electronics. An automotive rounded pin terminal is built for stronger guidance, better vibration resistance, improved self-cleaning contact, and higher long-term reliability. If the application is automotive or high-reliability industrial equipment, the rounded automotive design is usually the better choice.

The main difference is not just the shape. Standard square pin terminals prioritize easy insertion and low cost for general electronics, while automotive rounded pin terminals are designed for vibration resistance, guided mating, stable contact, and long service life in harsher environments. Their structure, stamping process, plating method, and performance targets are all different.

If you only look at the pin tip, the difference may seem small. In real applications, though, terminal geometry affects contact stability, corrosion resistance, plating consistency, insertion feel, and even failure risk over time. This article breaks down the differences step by step so engineers, sourcing teams, and product managers can make better design decisions.

Start With the Right Terminology

Before comparing the products, it is important to use the right language.

In this article:

  • Standard square pin terminal means the square or flat-edged metal pin commonly used in PCB pin headers.
  • Automotive rounded pin terminal means the rounded or bullet-shaped male terminal used in automotive low-voltage connector systems.

This distinction matters because industry-leading suppliers do not treat pin headers and terminals as the same category. Aptiv’s public connection systems catalog lists Connectors, Terminals, Seals, and Pin Headers as separate product groups, which confirms that “pin header” and “automotive terminal” should not be used interchangeably.

Why This Comparison Matters

Automotive connectors work in a very different environment from ordinary board-level connectors.

According to VDA, electrical and electronic components in vehicles must continuously adapt to stricter requirements around safety, reliability, environmental exposure, vibration, temperature, and chemical resistance. VDA also highlights that wiring systems and connector components are part of that evolving standardization work.

That is why a terminal for a vehicle cannot be chosen the same way as a terminal for a simple PCB header. Even if both parts are conductive metal pins, the design priorities are different:

  1. Consumer electronics focus more on cost, compactness, and ease of assembly
  2. Automotive systems focus more on durability, vibration stability, and long-term consistency
  3. Harsh environments require stronger protection against debris, contact instability, plating wear, and corrosion

FPIC’s internal technical comparison document makes the same point very clearly: a standard square pin terminal is meant for lower-stress electronic connections, while the automotive rounded pin terminal is designed for high-vibration, high-reliability service conditions.

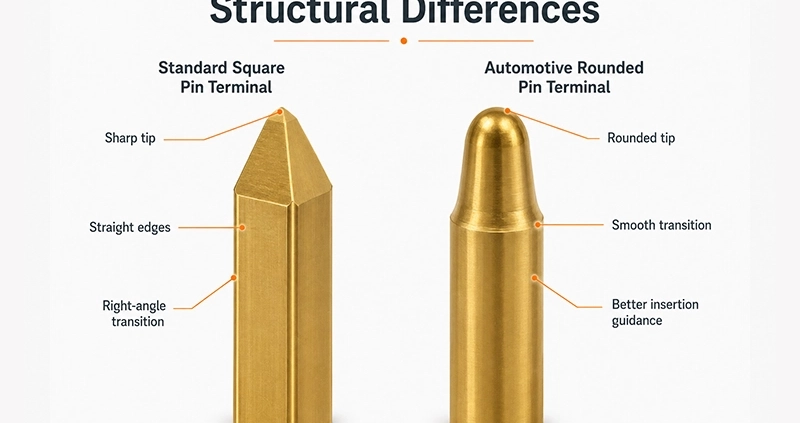
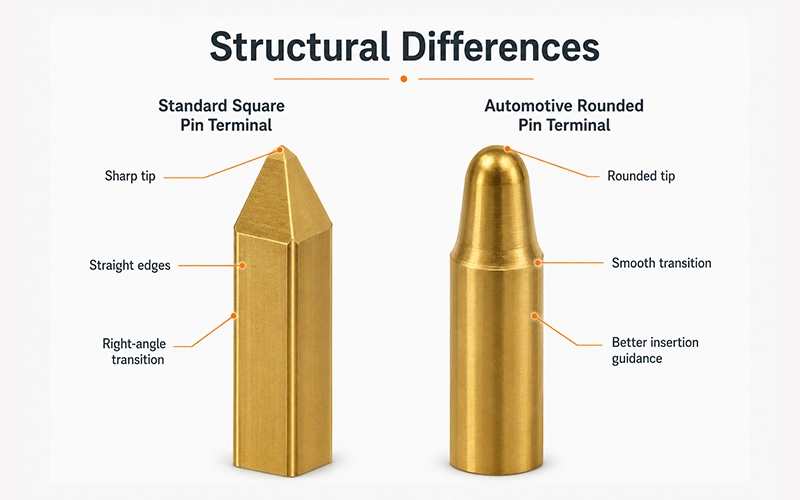
Structural Differences

Square Pin Terminals vs. Automotive Rounded Pin Terminals

Standard Square Pin Terminals

A standard square pin terminal usually has:

  • Tip: Sharp/pyramidal, small flat surface, obvious edges
  • Root: 90° dead-angle
  • Design focus: Easy insertion, low cost, for consumer electronics (low vibration, few insertions)
  • Example applications: PCB headers, low-end electronic devices, DuPont-style wiring

This kind of structure is common in:

  • Board-to-board connections
  • Standard PCB headers
  • Consumer electronics
  • Simple control boards
  • Low-vibration devices

The main benefits are easy insertion, easy manufacturing, and lower cost. But the structure also has limitations. Sharp edges and dead corners can create areas where stress concentrates, and in demanding environments they are less forgiving.

Automotive Rounded Pin Terminals

An automotive rounded pin terminal usually has:

  • Tip: Rounded bullet-head / dome-shaped
  • Root: Smooth tapered transition, no dead corner
  • Pin body: Thicker, stronger
  • Core benefits: Guided insertion, vibration resistance, self-cleaning, short-circuit protection
  • Designed for automotive harsh conditions: ECU, BCM, lighting, window, seat control modules

This design offers several practical advantages:

  • Better insertion guidance
  • Reduced scraping at the mating interface
  • More stable contact behavior
  • Better vibration resistance
  • Lower risk of debris staying in sharp dead corners
  • Improved contact reliability over long service life

Structural Comparison Table

Item Standard Square Pin Terminal Automotive Rounded Pin Terminal
Tip shape Sharp / pyramidal / flat-edged Rounded / bullet-shaped / dome-like
Root transition 90° style transition, dead-corner tendency Smooth tapered transition
Edge condition Obvious corners and flat faces Rounded surface, fewer stress points
Contact style Flat or edge-dominant Arc-guided, more stable engagement
Main design goal Easy insertion, simple structure, lower cost Guidance, vibration resistance, reliability
Typical environment General electronics Automotive low-voltage systems
Debris tolerance Lower Better
Reliability expectation Basic High

Why Rounded Geometry Helps in Automotive Use

The rounded automotive design is not just about appearance. It changes how the terminal behaves during mating and in long-term service.

1. Better Guidance

A rounded tip helps the male terminal find its way into the mating contact more smoothly. This matters when connector tolerances, insertion angle variation, or assembly speed introduce small alignment changes.

2. Better Vibration Resistance

In vehicles, connectors see repeated vibration from engine systems, road conditions, opening and closing actions, and general operating movement. A more robust and better-guided terminal geometry helps maintain a stable contact relationship.

3. Better Self-Cleaning Behavior

When two contacts mate and unmate repeatedly, a rounded guided structure can help wipe the contact area more consistently. FPIC’s internal document specifically notes this self-cleaning advantage as one reason automotive rounded terminals better resist contamination-related issues.

4. Lower Short-Circuit Risk

The internal comparison also notes that the absence of obvious dead-angle geometry helps reduce the chance of debris buildup around the terminal root, which is one of the practical design benefits of the automotive rounded form.

Industry Background and Design Thinking

FPIC’s internal document cites historical automotive field-failure discussions as a turning point in how the industry views low-voltage terminal design. The document explains that older low-voltage connector approaches using more ordinary square-pin-like forms could create higher risk when vibration, thermal cycling, and debris were involved, which pushed the market toward more robust automotive-specific terminal geometry.

Even without repeating every historical claim, the design lesson is clear:

Automotive connectors are not just “stronger consumer connectors.” They are engineered differently because the environment is different.

That view also aligns with the broader work of VDA and USCAR, where connector systems and related specifications are continuously reviewed to meet the demands of safety, durability, and vehicle operating conditions.

Manufacturing Process Differences

The structure difference is only one part of the story. The manufacturing route is also very different.

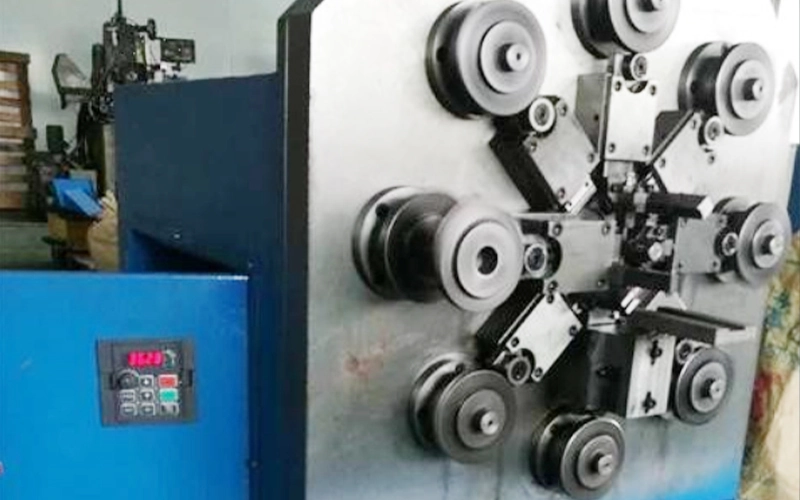
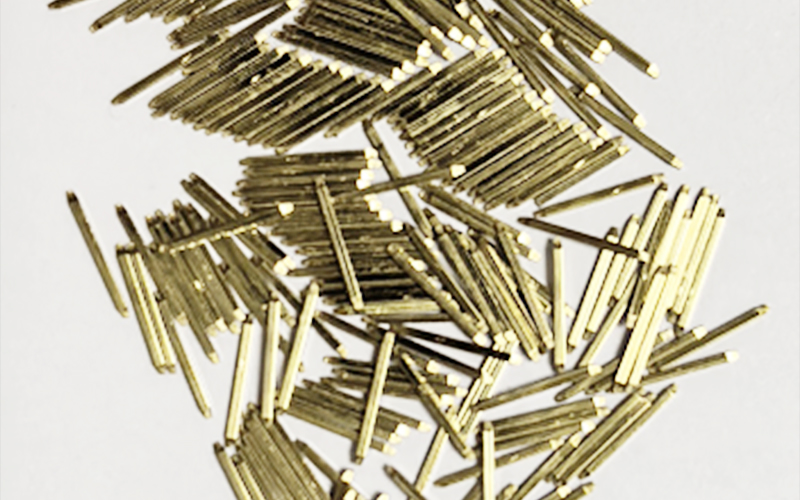
How Standard Square Pin Terminals Are Made

  • Equipment: Multi-wheel forming machines
  • Process: Wire extrusion → straightening → forming → cutting
  • Output: Loose independent pins
  • Automation: Limited
  • Use case: Standard PCB headers

How Standard Square Pin Terminals Are Made

How Standard Square Pin Terminals Are Made

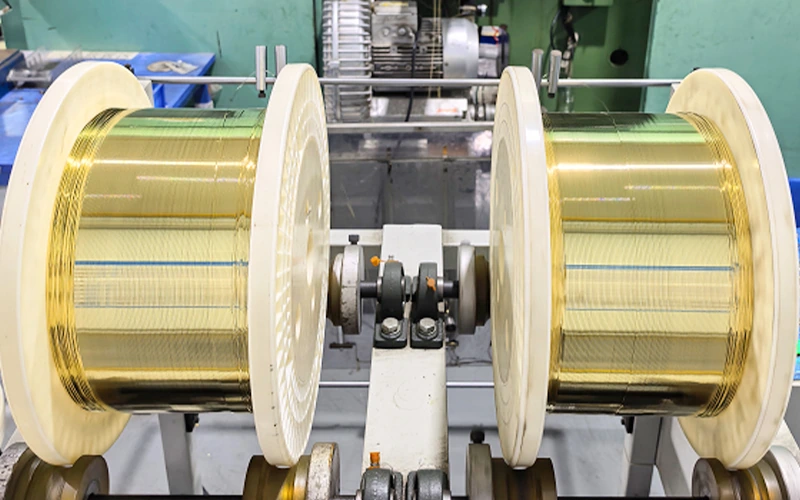
How Automotive Rounded Pin Terminals Are Made

  • Equipment: High-speed precision stamping, continuous progressive dies
  • Process: Brass strip → stamping → punching → bending → forming → cutting
  • Output: Continuous strip carrier for automated assembly
  • Automation: High compatibility, precise dimensions, supports reel-to-reel plating

How Automotive Rounded Pin Terminals Are Made

Manufacturing Comparison Table

Item Standard Square Pin Terminal Automotive Rounded Pin Terminal
Main equipment Multi-wheel square pin forming machine High-speed precision stamping press
Input material Wire stock Copper alloy strip
Core process Extrusion/forming/cutting Progressive stamping/forming
Finished form Loose pin / independent pin Continuous carrier strip
Automation compatibility Medium High
Dimensional control Basic to medium Higher
Mass-production suitability Good for standard electronics Better for automotive-scale process control

Plating Process Differences

The plating route is one of the biggest technical differences, and it directly affects contact quality.

Standard Square Pin Terminal Plating

  • Barrel/batch plating
  • Less uniform coating; edges and tips prone to thin plating
  • Manual sorting required for automation

Automotive Rounded Pin Terminal Plating

  • Reel-to-reel continuous precision plating
  • Uniform thickness, strong adhesion
  • Fully compatible with automated assembly, injection molding, and SMT

Plating Comparison Table

Item Standard Square Pin Terminal Automotive Rounded Pin Terminal
Workpiece form Loose individual pins Continuous strip terminal
Typical plating method Barrel / bulk plating Reel-to-reel precision plating
Thickness consistency Lower Higher
Edge coverage consistency Less stable Better controlled
Adhesion behavior More variation More stable
Automation support Limited Excellent

Performance Comparison

FPIC’s internal technical comparison gives a clear picture of why automotive rounded terminals are chosen for more demanding systems.

Metric Square Pin Rounded Pin
Contact resistance High batch variation Low, ≤±1mΩ
Mating cycles ≤500 >10,000
Vibration resistance Low High, car-grade
Salt spray resistance Poor >10 years in automotive environment
Current carrying Local heating Uniform, stable temperature rise
Temperature tolerance Limited -40°C to +125°C
High-frequency signal Poor LVDS compatible, stable signal

Industry Standards & Background

  1. Early Mercedes W210/W220 ECU/BCM PCB failures due to square pins → large recalls, safety issues
  2. USCAR / VDA / QC/T standards: automotive ≥2-pin low-voltage connectors must use rounded bullet-head terminals
  3. Safety, vibration, long-term reliability, and manufacturing precision are mandatory in automotive-grade terminals

Application Comparison

Best Uses for Standard Square Pin Terminals

A standard square pin terminal is usually a good fit for:

  • PCB headers
  • Consumer electronics
  • Low-vibration control boards
  • Cost-sensitive electronics
  • Standard signal connections

Best Uses for Automotive Rounded Pin Terminals

An automotive rounded pin terminal is usually the better fit for:

  • Automotive low-voltage systems
  • Control modules
  • Lighting systems
  • Window lift systems
  • Power seat systems
  • Multimedia systems
  • Industrial equipment with demanding vibration requirements
  • Long-life signal or low-voltage power transmission

FPIC Engineering Perspective

At FPIC, terminal selection is not treated as an isolated metal-part decision. It is part of the full connector-system design process.

A good connector terminal must be evaluated together with:

  • Housing design
  • Material selection
  • Plating specification
  • Contact force
  • Current path
  • Assembly process
  • Testing method
  • End-use environment

This system-level mindset also matches FPIC’s broader manufacturing strengths. According to FPIC company materials, the company supports connector development through:

  • Product design and tooling development
  • Metal stamping
  • Plastic injection molding
  • Auto assembly with CCD
  • Quality assurance testing
  • Automotive connector manufacturing under IATF 16949-related systems and process control

That manufacturing foundation matters because a good terminal design only delivers real value when it can also be produced consistently.

What Engineers and Buyers Should Ask Before Selecting a Terminal

When reviewing a connector concept, ask these questions:

1) What is the real operating environment?

Will the connector see:

  • Road vibration?
  • Temperature cycling?
  • Moisture?
  • Corrosive conditions?
  • Repeated mating?

If yes, a general square pin may not be the right solution.

2) Is insertion feel important?

Rounded automotive terminals generally provide smoother and more forgiving insertion behavior, especially when alignment is not perfect.

3) How important is long-term consistency?

If the product must stay reliable over years, especially in automotive or industrial systems, terminal geometry and plating consistency become much more important.

4) Will the part be made at scale?

If the project needs high automation, stable dimensions, and controlled plating, strip-based automotive-style terminal production has strong advantages.

Practical Selection Guide

Application Scenario Recommended Choice Why
Standard PCB header Standard square pin terminal Cost-effective and suitable for simple board-level use
Consumer electronics Standard square pin terminal Enough performance for lower-stress environments
Automotive low-voltage connector Automotive rounded pin terminal Better vibration resistance and long-term reliability
Signal connector in harsh industrial equipment Automotive rounded pin terminal Better guidance and contact stability
High-reliability long-life design Automotive rounded pin terminal Better process consistency and service performance

Conclusion

A standard square pin terminal and an automotive rounded pin terminal may look similar at first glance, but they are built for different jobs.

The square pin version is a practical choice for general electronics where cost and simplicity matter most. The automotive rounded version is designed for a tougher world: vibration, temperature change, longer service life, and higher reliability requirements.

So if the project is automotive, or if the application behaves more like automotive in terms of durability demands, the safer decision is usually the automotive rounded terminal.

FAQ

1. Is a pin header the same as an automotive terminal?

No. A pin header usually refers to a connector category used on PCBs, while an automotive terminal refers to a terminal system designed for vehicle-grade electrical connection. Leading supplier catalogs treat them as separate categories.

2. Why are automotive terminals often rounded?

Because the rounded shape improves insertion guidance, reduces sharp-edge stress, supports more stable mating, and performs better in vibration-heavy environments.

3. Are square pin terminals bad?

Not at all. They are a good solution for the right application. The issue is not quality, but fit. They are simply intended for less demanding operating conditions than automotive terminals.

4. Does plating really make a big difference?

Yes. Plating consistency affects contact resistance, corrosion resistance, wear behavior, and long-term performance. Reel-to-reel precision plating generally offers better consistency for automotive terminals.

5. When should I choose the automotive rounded design?

Choose it when the connector must survive vibration, repeated mating, wider temperature exposure, and longer service life requirements.

Ready to choose the right terminal for your automotive or industrial application?

Explore FPIC’s complete range of low-voltage automotive connectors and bullet-head terminals for high-reliability, vibration-resistant, and long-life performance.

View Products: https://fpiconn.com/products/

Contact Sales: info@fpiconn.com

💡 Tip: Our engineering team can help you select the right terminal and connector solution for your exact application, including rapid prototyping and mass-production guidance

Resources

  1. FPIC Internal Technical Document: “Differences Between Automotive Low-Voltage Connector Terminals and Standard Pin Header Terminals”
    This internal FPIC source provided the core technical comparison for structure, process route, plating method, performance differences, and application recommendations used in this article.
  2. Aptiv – Connection Systems Catalog
    Aptiv’s official catalog clearly separates Terminals and Pin Headers into different product categories, which supports the terminology distinction used in this article.
    Link: https://www.aptiv.com/en/solutions/connection-systems/catalog
  3. VDA – Electrical/Electronic Components and General System Requirements
    VDA explains that automotive electrical and electronic components must continuously adapt to requirements involving safety, reliability, vibration, temperature, chemicals, and other operating conditions.
    Link: https://www.vda.de/en/topics/automotive-industry/standardization-and-technical-standards/e-e-components-and-general-system-requirements
  4. USCAR – EWCAP / Connector Validation Context
    USCAR materials help show the broader North American automotive context for connector and terminal validation work.
    Link: https://uscar.org/
Standard Equipment Parameters

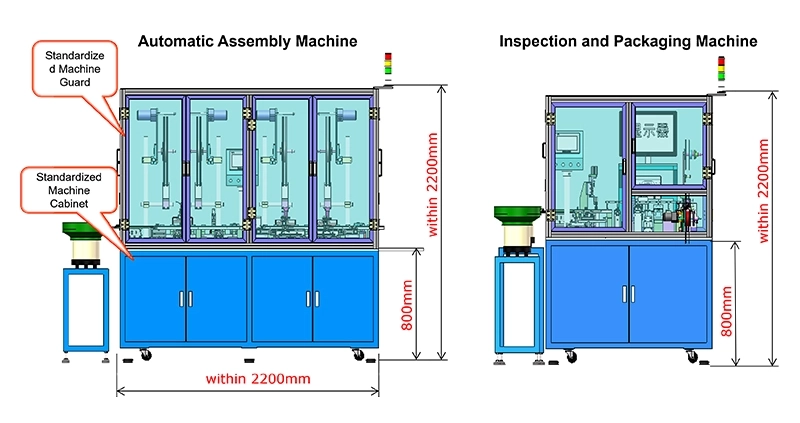
Automation Design Standardization helps connector manufacturers build machines faster, run them more stably, and adapt them more easily to new part numbers. For USB, automotive connectors, and pin header products, modular equipment architecture can reduce engineering repetition, improve spare-part sharing, and support more predictable mass production.

If connector automation equipment is designed with standardized modules, machine builders can shorten development time, improve stability, simplify changeovers, and reduce maintenance complexity. In practice, that means reusing proven feeding, insertion, bending, inspection, and layout modules instead of redesigning each machine from the ground up.

This guide combines FPIC’s internal engineering thinking with broader automation-industry logic. It is written for product engineers, sourcing teams, and manufacturing decision-makers who want to understand why standardized automation equipment matters for connector production.


What Connector Automation Design Standardization Means

In connector manufacturing, automation design standardization means defining a repeatable machine platform: common cabinet dimensions, common hardware brands, common safety and enclosure requirements, and reusable mechanical modules for feeding, insertion, bending, inspection, and packaging.

Instead of creating every machine from scratch, engineering teams reuse mature modules and only customize the few components that truly depend on product geometry.

That is exactly how FPIC’s internal automation presentation frames the subject. The stated purpose of standardization is to improve design efficiency, use mature module mechanisms, protect machine stability, avoid unstable process structures, reduce development cost, and support product quality with a consistent design basis.


Why Standardization Matters in Connector Production

Connector automation is not just about moving parts faster. It is about building machines that can repeatedly handle small parts, tight tolerances, synchronized motion, vision checks, and frequent product-family variation without becoming fragile or expensive to maintain.

Faster Equipment Development

When feeding tracks, insertion units, bending mechanisms, and cabinet layouts are already standardized, engineering teams can launch similar machine platforms much faster.

Better Machine Stability

Mature modules have already been proven in production. Reusing them lowers the risk of introducing weak structures or unstable motion sequences into new equipment.

Easier Model Changeovers

If only a rail, plate, or bending block needs to change, the same machine can support multiple products with minimal redesign.

Lower Spare-Part Complexity

Shared wear parts across similar machine types reduce purchasing complexity, simplify maintenance planning, and shorten downtime.

Better Production-Line Layout

When equipment dimensions, cabinet heights, and machine envelopes are standardized, workshop planning becomes easier.


Start with Standard Equipment Parameters

FPIC’s internal automation design rules define several practical baseline requirements:

  • Machine appearance should be clean and consistent
  • Standard cabinet color should be blue
  • Cabinet height should be about 800 mm
  • Total machine height should stay below 2200 mm
  • Machine length should stay within 2200 mm for elevator access
  • Equipment should include an enclosure for dust protection, sound insulation, and noise reduction
  • Preferred electrical and motion-control brands should be clearly defined, including PLC, pneumatics, servo motor, hardware, and CCD suppliers

Standard Equipment Parameters

Why the Machine Platform Matters

A standardized machine platform improves factory layout, transport planning, installation efficiency, and visual consistency in production.

Why Component Standards Matter

Using defined brands and common control architecture simplifies integration, spare-parts support, training, and troubleshooting.


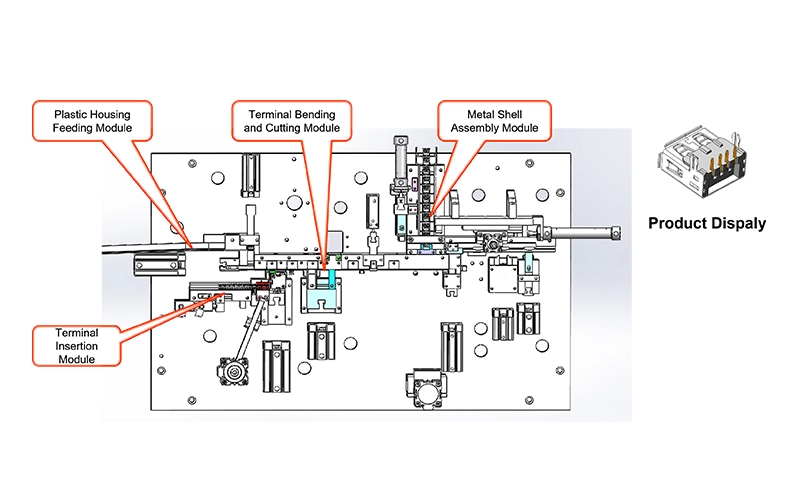
Modular Design in USB Connector Automation

FPIC’s automation standard for the USB series highlights several reusable machine modules:

  • Standardized plastic-core feeding track module
  • Standardized terminal bending and cut-off module
  • Standardized metal shell loading module
  • Standardized terminal insertion module

Modular Design in USB Connector Automation

Why USB Automation Benefits from Standard Modules

Once these modules are standardized, similar USB machines can call the same structures directly.

Easier Changeover for New Part Numbers

For new part numbers, only a small number of parts need to be replaced, and some wear parts can be shared across similar platforms.


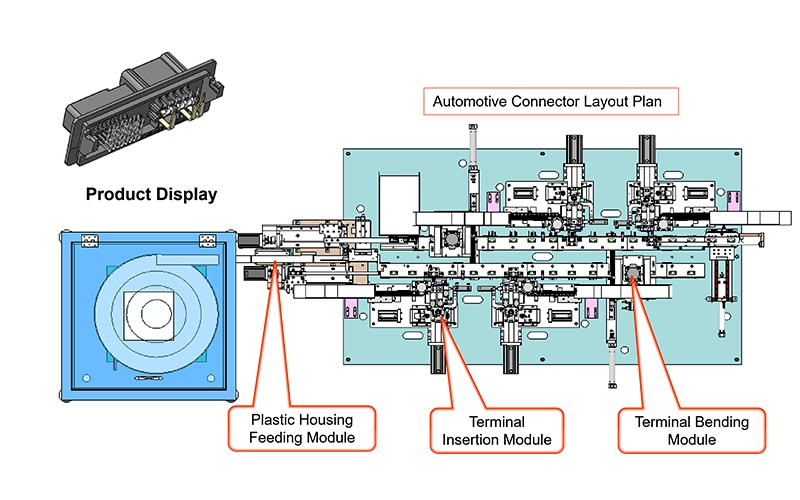
Modular Design in Automotive Connector Automation

Automotive connector production usually demands tighter control over consistency, insertion quality, and equipment uptime. FPIC’s internal standard shows the use of standardized modules for:

  • Plastic housing feeding
  • Terminal insertion
  • Terminal bending
  • Equipment layout planning for automotive connector lines

Modular Design in Automotive Connector Automation

Standardized Insertion Modules

For different terminals, only the terminal-track parts need to change. For different plastic housings, only the housing-track parts need to change.

Why This Matters for Automotive Programs

This type of modularity improves manufacturing agility while keeping the machine concept stable and repeatable.


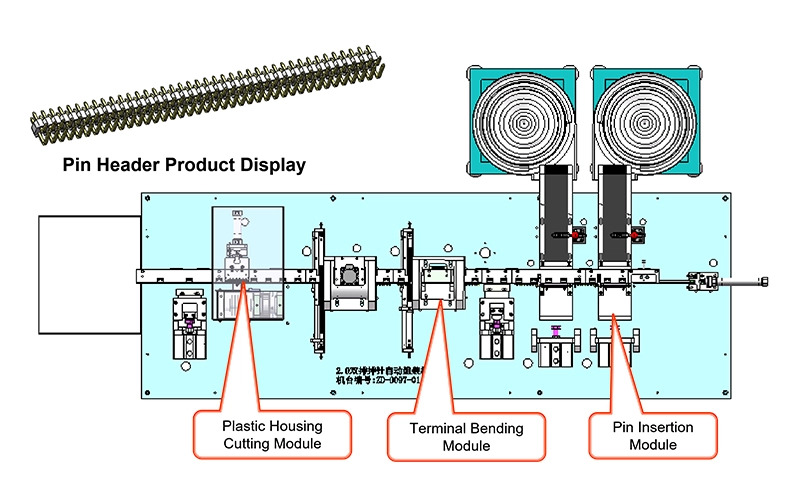
Modular Design in Pin Header Automation

FPIC’s standardization approach also covers pin header automatic machines through modules such as:

  • Plastic housing cutting module
  • Terminal bending module
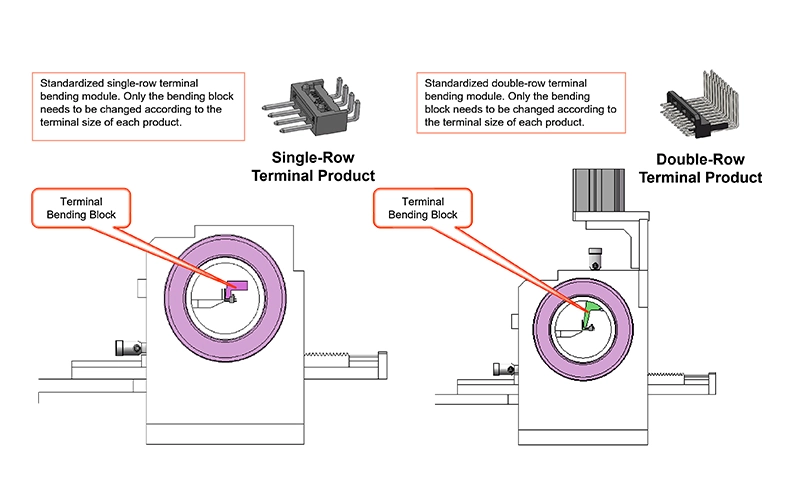
  • Pin insertion module

Modular Design in Pin Header Automation

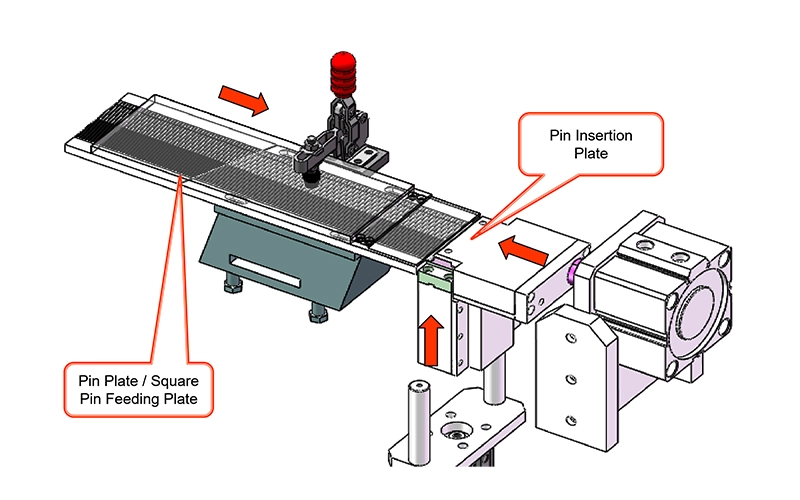
Adaptable Pin Insertion Mechanism

Adaptable Pin Insertion Mechanism

The square-pin feeding and insertion module is suitable for pitches such as 1.27 mm, 2.0 mm, 2.54 mm, and 5.0 mm.

Adaptable Pin Insertion Mechanism (2)

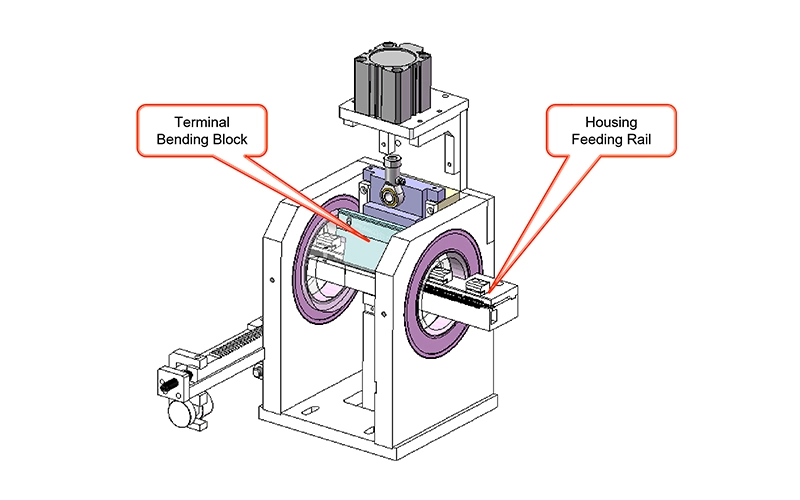
Adaptable Terminal Bending Mechanism

For different pitch products, the machine only needs the corresponding bending block to be replaced.

Adaptable Terminal Bending Mechanism

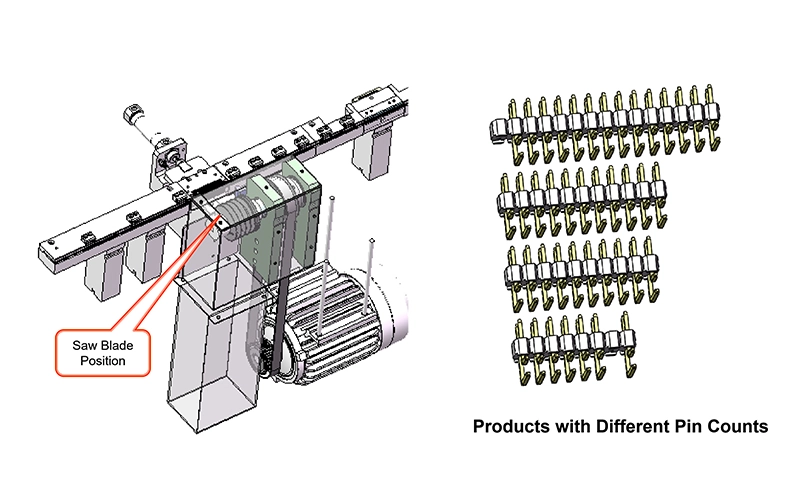
Adaptable Housing Cutting Mechanism

For different pin counts, production can be adjusted by changing the corresponding cutter position.

Adaptable Housing Cutting Mechanism


The Role of Inspection, Protection, and Noise Control

Automation standardization should not stop at motion modules. It also needs to include equipment protection and inspection design.

FPIC’s internal standard requires machine enclosures that support dust prevention, sound insulation, and noise reduction. It also specifies CCD as part of the preferred equipment ecosystem.

Why Enclosures Matter

Machine covers improve cleanliness, reduce noise, and help create a more controlled production environment.

Why Vision Integration Matters

Machine vision helps improve inspection consistency and supports more reliable connector assembly quality.


How Standardized Automation Helps Customers

From the customer side, connector automation design standardization creates several concrete benefits:

More Predictable Lead Times

A standardized machine platform reduces engineering uncertainty and usually shortens development cycles.

Better Consistency in Mass Production

Machines built on proven modules are easier to stabilize and support repeatable production quality.

Faster Support for New Part Numbers

A connector family can often share one machine platform, with only limited tooling changes.

Lower Lifecycle Cost

Shared spare parts, simpler training, and easier maintenance can reduce total cost over time.


A Practical 5-Step Framework for Standardizing Connector Automation

Step 1 – Define the Machine Platform

Set standard dimensions, cabinet structure, enclosure rules, and preferred component brands.

Step 2 – Define Reusable Motion Modules

Standardize feeding, insertion, bending, cutting, and inspection functions wherever possible.

Step 3 – Define Product Changeover Logic

Make clear which parts are common and which must change for a new model.

Step 4 – Define Inspection and Protection Standards

Build machine vision, covers, and noise-control features into the standard platform.

Step 5 – Define Layout Scalability

Ensure machines fit workshop planning, transport limits, and long-term production-line expansion.


Where FPIC Adds Value

At FPIC, we do not treat automation equipment as isolated machinery. We see it as a key part of connector manufacturing capability. Our internal engineering work on connector automation standardization covers machine purpose, technical specifications, modular reuse, and product-family adaptability across USB, automotive connectors, and pin header series.

That matters because customers increasingly need more than a single successful sample. They need a manufacturing partner that can support product evolution, part-number expansion, stable production, and practical engineering response.

If you are developing connector products that require scalable assembly automation, FPIC can support both connector manufacturing and the engineering logic behind stable production systems.


Conclusion

Connector automation design standardization is not only about internal engineering efficiency. It directly affects equipment stability, product quality, changeover speed, and the ability to scale a product family economically.

For USB, automotive connectors, and pin headers, modular machine architecture makes it easier to reuse what works, control what changes, and reduce unnecessary risk. If you are evaluating automation capability as part of your connector supply chain, standardization is one of the best questions to ask.


References / Notes

  1. FPIC internal engineering presentation: Standardized Design of Connector Automation Equipment.ppt (R&D Department, prepared by Qin Qinghua, dated 2026-04-15). This article incorporates FPIC’s internal design logic for machine standardization, technical parameters, and modular automation for USB, automotive connector, and pin header series.
  2. Rockwell Automation, Design Machines and Equipment — consistent, modularized designs reduce design labor and improve manufacturing efficiency.
  3. Rockwell Automation, Develop Machines and Equipment — scalable technology, reusable equipment modules, and simplified integration reduce engineering time and risk.
  4. Rockwell Automation, Solutions for Manufacturing and Assembly OEMs — modular, connected, data-ready machine design supports flexible manufacturing.
  5. Omron, Pin Connector and Cable Inspection — machine vision and modular automation architectures are widely used in electronics manufacturing inspection.
  6. ISA, official site — standards-based technical resources remain foundational in industrial automation.
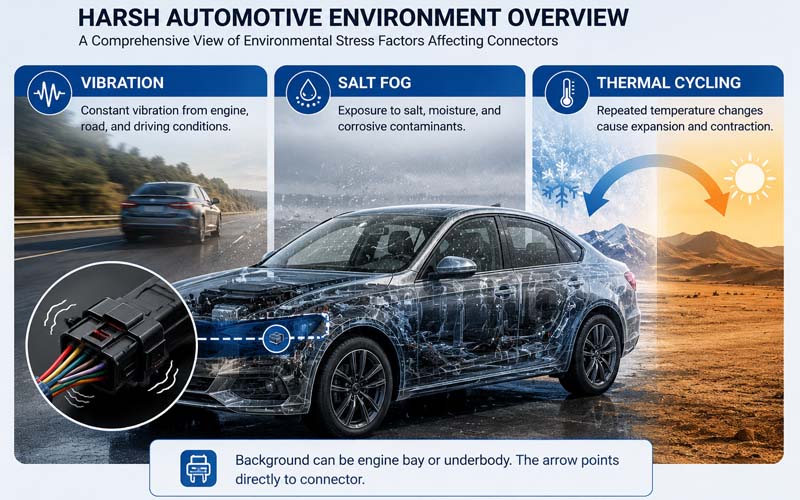
Harsh Automotive Environment Overview

Automotive connectors operate in some of the harshest electrical environments found in modern products. Unlike controlled laboratory conditions, real vehicles expose connectors to continuous vibration, moisture, road salt, thermal cycling, and mechanical stress over many years of operation.

Selecting connectors based only on current rating or pin count is no longer sufficient. Engineers must specify connectors according to the actual environmental stresses they will experience throughout the vehicle lifecycle.

This article explains how to specify automotive connectors for vibration, salt fog, and thermal cycling, and how these factors influence long-term reliability.

Harsh Automotive Environment Overview


Why Environmental Specification Matters

Many connector failures are not caused by immediate design flaws, but by gradual degradation under combined environmental stress.

Typical field failures include:

  • intermittent electrical signals
  • increased contact resistance
  • corrosion-related failures
  • seal degradation
  • terminal back-out or loosening

In many cases, connectors pass standard validation tests but still fail in real vehicle environments because environmental conditions were underestimated during specification.


Understanding the Three Key Stress Factors

1.Vibration

Why Vibration Is Critical

Vehicles generate continuous vibration from:

  • road conditions
  • engine operation
  • chassis movement
  • electric drive systems

This vibration creates micro-motion at the contact interface.

Over time, this can lead to:

  • fretting corrosion
  • plating wear
  • contact resistance drift
  • terminal loosening

Key Connector Features for Vibration Resistance

When specifying connectors for vibration-prone areas, consider:

  • terminal retention strength
  • contact spring stability
  • CPA/TPA secondary locking
  • anti-vibration contact design
  • robust housing structure

High-Risk Installation Areas

  • engine compartment
  • chassis-mounted systems
  • underbody harnesses
  • seat systems with repeated movement

2.Salt Fog and Corrosion Exposure

Why Salt Fog Matters

Road salt and coastal environments introduce highly corrosive conditions.

Salt fog exposure can accelerate:

  • terminal oxidation
  • plating degradation
  • seal deterioration
  • leakage current formation

Corrosion often begins microscopically before visible damage appears.


What to Consider During Specification

Connector Sealing

Use appropriate sealing levels based on installation zone:

  • IP67 for splash-prone environments
  • IP69K for high-pressure wash exposure

Material and Plating Selection

Material choice strongly affects corrosion resistance.

Common options:

  • tin plating → cost-effective but more sensitive to fretting
  • gold plating → better signal stability and corrosion resistance
  • nickel underplating → improved durability

Venting and Drainage

Poor drainage design can trap moisture and accelerate corrosion even in sealed systems.


3.Thermal Cycling

What Is Thermal Cycling?

Thermal cycling refers to repeated heating and cooling during operation.

Typical automotive conditions include:

  • sub-zero winter startup
  • high engine bay temperatures
  • rapid load changes in EV systems

Effects on Connector Reliability

Thermal expansion and contraction can cause:

  • loss of contact force
  • seal fatigue
  • housing deformation
  • micro-cracking in materials

Thermal cycling also accelerates aging of polymers and elastomers.


Important Design Considerations

When specifying connectors:

  • verify operating temperature range
  • evaluate material compatibility
  • consider long-term stress relaxation behavior
  • review current derating at elevated temperatures

Why Combined Stress Matters More Than Individual Tests

In real vehicles, vibration, moisture, and temperature do not occur independently.

Example:

  • vibration damages plating
  • moisture accelerates oxidation
  • thermal cycling weakens contact stability

This creates compounded degradation mechanisms that are much more severe than isolated stress conditions.

This is why combined-environment validation is increasingly important.


Connector Specification by Installation Zone

Installation Zone Main Risk Factors Recommended Connector Strategy
Engine Bay Heat + vibration + moisture Sealed high-temperature connector
Underbody Salt fog + water + debris IP67/IP69K sealed connector
Cabin Electronics Low environmental exposure Cost-optimized unsealed connector
Seat Systems Repeated movement + vibration High-retention LV connector
EV Battery Area Thermal cycling + HV safety HV sealed connector with CPA/TPA

Common Specification Mistakes

Over-Specification

Using overly complex sealed connectors in low-risk zones can:

  • increase cost
  • complicate assembly
  • reduce serviceability

Under-Specification

Using insufficient protection in harsh environments can lead to:

  • premature corrosion
  • intermittent failures
  • warranty issues

Focusing Only on Datasheets

Connector reliability depends on:

  • harness routing
  • installation orientation
  • strain relief
  • assembly quality

System-level factors are often underestimated.


Validation Recommendations

A robust validation plan should include:

  • vibration testing with electrical monitoring
  • thermal cycling under load
  • salt fog exposure testing
  • combined environmental testing
  • post-test contact resistance evaluation

Real installation conditions should be replicated whenever possible.


How FPIC Supports Harsh-Environment Connector Applications

FPIC supports automotive and industrial customers with:

  • connector selection by installation environment
  • custom harness integration
  • sealing and routing optimization
  • validation support for harsh conditions
  • manufacturing consistency control

By aligning connector specification with real-world operating environments, long-term reliability risks can be significantly reduced.


Final Thoughts

Automotive connector specification is no longer just about electrical parameters. Environmental durability has become equally important.

Vibration, salt fog, and thermal cycling create long-term stresses that gradually degrade connector performance.

  • A successful specification strategy requires:
  • understanding installation environments
  • selecting appropriate materials and sealing
  • validating under combined stress conditions
  • considering system-level integration

The best connector is not the most expensive one—it is the connector correctly matched to the real application environment.


FAQ

Why is vibration harmful to connectors?

Because it creates micro-motion at contact interfaces, leading to fretting corrosion and resistance increase.

What does salt fog testing evaluate?

It evaluates corrosion resistance under simulated harsh environmental exposure.

Why is thermal cycling important?

Repeated expansion and contraction can weaken contact force and degrade materials over time.

Are sealed connectors always necessary?

No. Connector type should match the installation zone and environmental exposure level.

What is the biggest connector specification mistake?

Ignoring real-world combined stress conditions during design and validation.


Improve Connector Reliability in Harsh Environments

Choosing the right connector for vibration, corrosion, and thermal stress is essential for long-term reliability.

FPIC provides automotive connector and wire harness solutions optimized for real-world operating conditions.

Contact us to discuss your application requirements.


Resources

Connector Failure Analysis in Vehicles

Automotive connectors are designed to operate reliably for more than a decade under demanding conditions. However, many field failures are not caused by design flaws alone, but by a combination of environmental stress, installation conditions, and long-term degradation mechanisms.

Understanding how and why connectors fail is critical for improving system reliability, reducing warranty costs, and optimizing design decisions early in development.

Among the most common and impactful failure mechanisms in vehicles are fretting corrosion, water ingress, and thermal stress. These factors often act together, accelerating degradation beyond what isolated testing may predict.


Why Connector Failure Analysis Matters

Connector failures rarely occur as sudden events. Most are the result of gradual degradation processes that evolve over time.

Without proper failure analysis:

  • root causes may be misidentified
  • corrective actions may be ineffective
  • the same issues may repeat across projects

A structured failure analysis approach helps engineers link symptoms to underlying mechanisms and implement targeted improvements.

Connector Failure Analysis in Vehicles


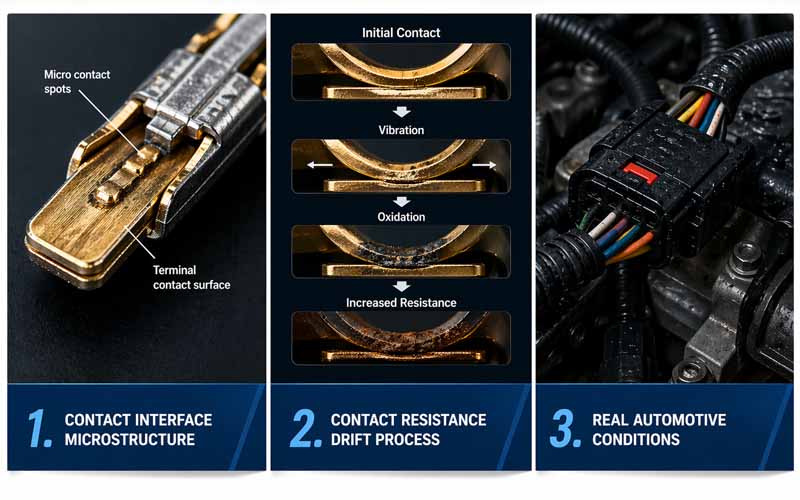
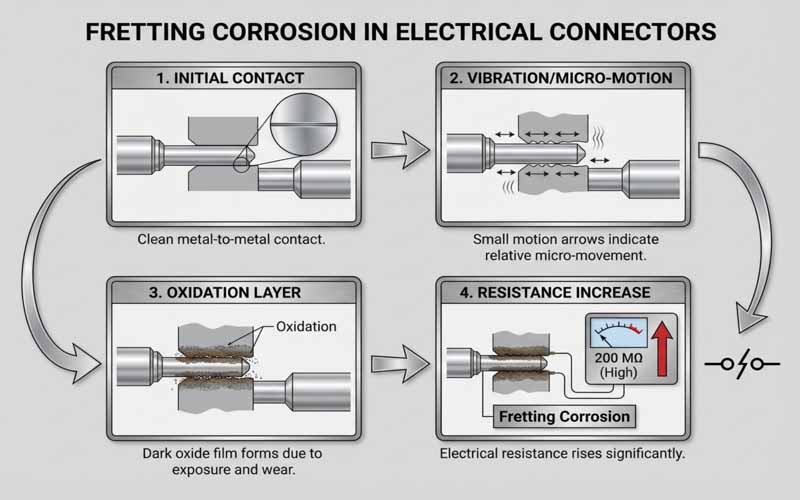
Fretting Corrosion: The Hidden Failure Mechanism

Fretting corrosion is one of the most common causes of intermittent electrical failure in automotive connectors.

How It Happens

  • vibration causes micro-motion between contact surfaces
  • protective plating wears away
  • oxide debris forms at the interface
  • electrical resistance increases

This process is often invisible from the outside, making it difficult to detect during inspection.


Typical Symptoms

  • intermittent signal loss
  • unstable electrical performance
  • increased contact resistance
  • no visible mechanical damage

Where It Occurs

  • engine bay connectors
  • chassis-mounted harnesses
  • high-vibration zones

Water Ingress: The Silent Reliability Killer

Water ingress occurs when moisture penetrates the connector interface or wiring system.

Causes

  • insufficient sealing design
  • damaged or misassembled seals
  • improper connector orientation
  • aging of sealing materials

Effects

  • corrosion of terminals
  • increased contact resistance
  • short circuits or leakage paths
  • long-term degradation of insulation

High-Risk Scenarios

  • underbody applications
  • areas exposed to road spray or pressure washing
  • connectors with compromised sealing integrity

Even connectors with high IP ratings can fail if sealing is not maintained during assembly or service.


Thermal Stress: Long-Term Degradation Driver

Thermal stress results from repeated temperature changes and heat generation during operation.

Sources

  • ambient temperature variation
  • heat from nearby components
  • current-induced heating (I²R losses)

Effects on Connectors

  • material expansion and contraction
  • loss of contact force
  • seal degradation
  • accelerated aging of materials

Combined Effects

Thermal stress often amplifies other failure mechanisms:

  • increased temperature accelerates corrosion
  • material softening reduces mechanical stability
  • cycling creates micro-movements that lead to fretting

Why Failures Are Often Multi-Factor

In real automotive environments, failures are rarely caused by a single factor.

For example:

  • vibration → fretting corrosion
  • moisture → oxidation
  • temperature → material degradation

These factors interact, creating compounded effects that are more severe than individual stresses.

This is why connectors that pass standard tests may still fail in field conditions.


Failure Analysis Methods

A systematic approach to connector failure analysis typically includes:

Visual Inspection

  • check for corrosion, discoloration, or damage

Electrical Testing

  • measure contact resistance
  • check continuity and insulation

Microscopic Analysis

  • identify fretting wear or oxide layers

Environmental Testing

  • reproduce failure under controlled stress conditions

Prevention Strategies

Design Level

  • select appropriate materials and plating
  • ensure sufficient contact force
  • design for sealing and environmental protection

System Level

  • optimize harness routing to reduce vibration
  • avoid water accumulation points
  • ensure proper connector orientation

Manufacturing and Assembly

  • ensure correct seal installation
  • maintain consistent crimp quality
  • control assembly processes

Validation

  • include combined stress testing
  • simulate real installation conditions
  • perform long-term aging tests

How FPIC Supports Failure Prevention

Preventing connector failure requires integration across design, manufacturing, and validation.

FPIC supports customers with:

  • connector and harness design optimization
  • sealing and routing strategy review
  • controlled assembly processes
  • validation aligned with real-world conditions

By addressing failure mechanisms early, long-term reliability can be significantly improved.


Final Thoughts

Connector failures in vehicles are rarely random. They are the result of predictable physical and environmental processes.

Fretting corrosion, water ingress, and thermal stress are among the most critical factors affecting long-term reliability—and they often work together.

Understanding these mechanisms allows engineers to move from reactive troubleshooting to proactive design improvement.


FAQ

What is the most common cause of connector failure in vehicles?

Fretting corrosion caused by vibration is one of the most common causes, especially in high-vibration environments.

Can sealed connectors prevent all water ingress issues?

No. Sealing effectiveness depends on design, assembly quality, and long-term material performance.

How does temperature affect connector reliability?

Thermal cycling can reduce contact force, degrade materials, and accelerate other failure mechanisms.

Why do connectors fail even after passing tests?

Because real-world conditions often involve combined stresses that are not fully replicated in standard testing.

How can connector failures be reduced?

Through proper design, material selection, assembly control, and realistic validation testing.


CTA

Reduce Connector Failure Risk in Your System

Understanding failure mechanisms is the first step toward building reliable systems.

FPIC provides connector and wire harness solutions designed for real-world conditions, helping reduce failure risk and improve long-term performance.

Contact us to discuss your application challenges.


Resources

  1. USCAR-2 – Automotive Connector Performance Specification: defines durability and environmental testing methods for connectors.
  2. TE Connectivity – Fretting Corrosion in Electrical Contacts: explains vibration-induced degradation mechanisms.
  3. Molex – Sealed Connector Design and Water Ingress: discusses sealing strategies and failure risks.
  4. Amphenol – Thermal Effects on Connector Systems: covers temperature-related reliability challenges.
  5. IEC 60512 – Connector Testing Standards: provides standard test methods for electrical connectors.

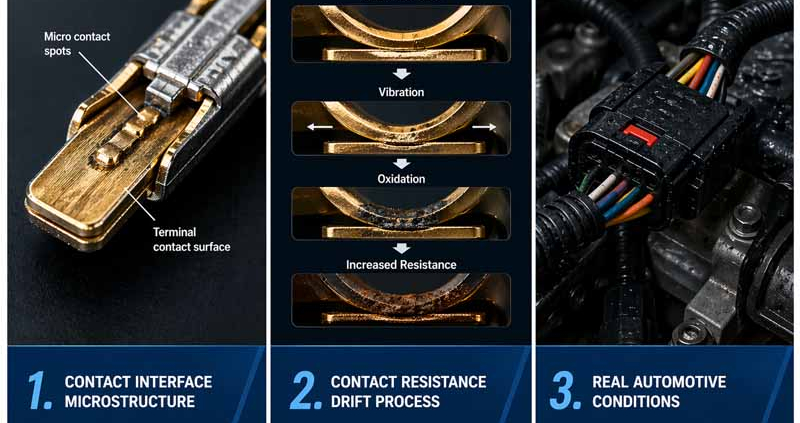
In automotive electrical systems, Automotive connectors performance is often evaluated based on initial specifications—contact resistance, current capacity, and mechanical retention. However, long-term reliability is not determined at time zero. It is shaped by how these parameters evolve over time.

One of the most critical yet often underestimated factors is contact resistance drift.

Contact resistance drift refers to the gradual increase or fluctuation of resistance at the electrical interface between mating terminals. While the change may be small in absolute terms, its impact can be significant—especially in high-current, high-voltage, and signal-sensitive automotive systems.


Understanding Contact Resistance at the Interface Level

Electrical contacts are not perfectly smooth surfaces. Even highly polished terminals only touch at microscopic asperities.

This means:

  • the real contact area is much smaller than the apparent area
  • current flows through discrete micro-contact points
  • resistance is highly sensitive to surface condition and contact force

Any change in these micro-contact conditions—such as oxidation, wear, or reduced contact pressure—can increase resistance.

Over time, these small changes accumulate, resulting in measurable resistance drift.


Why Contact Resistance Drift Matters

Heat Generation and Thermal Runaway Risk

In power circuits, resistance increase leads directly to higher heat generation (I²R losses). This can create a feedback loop:

  • higher resistance → more heat
  • more heat → faster material degradation
  • degradation → further resistance increase

In severe cases, this can lead to localized overheating or even thermal runaway in high-power systems.

Contact Interface Microstructure


Voltage Drop and Efficiency Loss

In EV and power distribution systems, even a small resistance increase can result in:

  • measurable voltage drop
  • reduced energy efficiency
  • performance degradation in motors or inverters

As system voltages rise, maintaining stable connections becomes even more critical.


Signal Integrity Degradation

For low-current signal circuits, resistance drift affects:

  • signal amplitude
  • noise margin
  • communication stability

This is particularly important in CAN, LIN, and automotive Ethernet systems, where stable electrical characteristics are required for reliable data transmission.


Root Causes of Contact Resistance Drift

Contact resistance drift rarely has a single cause. It is typically the result of multiple interacting factors.

Fretting Corrosion

Micro-motion between contact surfaces caused by vibration leads to:

  • wear of protective plating
  • formation of oxide debris
  • increased contact resistance

This is one of the most common failure mechanisms in automotive connectors.


Oxidation and Environmental Exposure

Exposure to oxygen, humidity, and contaminants can form insulating layers on contact surfaces.

Key risk factors include:

  • unsealed connectors
  • harsh environmental conditions
  • long service life

Loss of Contact Force

Contact force is critical for maintaining a stable electrical interface. Over time, it can decrease due to:

  • material creep
  • thermal cycling
  • stress relaxation

Reduced force leads to smaller effective contact area and higher resistance.


Plating Degradation

Surface plating (tin, silver, or gold) is designed to protect against corrosion and ensure conductivity. However:

  • repeated mating cycles can wear plating
  • vibration can accelerate degradation
  • base materials may oxidize once exposed
  • Contact Resistance Drift Process

Real-World Conditions Accelerate Drift

Laboratory testing often evaluates connectors under controlled conditions. However, real automotive environments introduce combined stresses:

  • continuous vibration from road conditions
  • wide temperature fluctuations
  • moisture, dust, and chemicals
  • harness movement and mechanical strain

These factors do not act independently—they interact and accelerate degradation mechanisms.

As a result, contact resistance drift in real applications is often faster and more complex than predicted by isolated testing.


High-Risk Automotive Applications

High-Current Systems

  • battery connections
  • inverter interfaces
  • power distribution units

These systems are sensitive to heat and efficiency loss.


High-Speed Data Systems

  • ADAS sensors
  • communication networks
  • control modules

These systems are sensitive to signal degradation.


Safety-Critical Systems

  • braking systems
  • airbag systems
  • vehicle control electronics

In these applications, even intermittent resistance variation can lead to unacceptable risk.


Strategies to Control Contact Resistance Drift

Optimize Contact Design

  • maintain stable contact force over time
  • design for vibration resistance
  • ensure sufficient contact area

Select Appropriate Materials and Plating

  • use corrosion-resistant materials
  • match plating type to application (tin vs gold)
  • consider mating cycle requirements

Improve Sealing and Environmental Protection

  • use sealed connectors in harsh environments
  • minimize exposure to moisture and contaminants

Control Harness Movement

  • reduce micro-motion through proper routing
  • add strain relief and fixation points
  • avoid unnecessary stress at connectors

Validate Under Realistic Conditions

Testing should include:

  • vibration + temperature combined testing
  • long-term aging simulation
  • real installation conditions

How FPIC Supports Stable Electrical Performance

Ensuring stable contact resistance requires coordination across connector design, cable assembly, and manufacturing processes.

FPIC supports customers with:

  • connector and cable integration design
  • controlled crimping and termination processes
  • application-based validation strategies
  • manufacturing consistency for long-term stability

By addressing both design and process variables, resistance drift can be effectively minimized.


Final Thoughts

Contact resistance drift is a slow but critical failure mechanism in automotive connectors. It does not cause immediate failure—but it gradually reduces system reliability until problems emerge.

As vehicles become more electrified and data-driven, the tolerance for electrical instability continues to decrease.

A robust connector design strategy must go beyond initial specifications and focus on long-term performance under real-world conditions.


FAQ

What is contact resistance drift?

It is the gradual increase or variation of resistance at an electrical contact interface over time.

Why is it important in automotive systems?

Because it affects heat generation, voltage stability, and signal integrity—critical factors in vehicle performance and safety.

What is the most common cause?

Fretting corrosion caused by vibration-induced micro-motion is one of the primary causes.

Can it be completely eliminated?

No, but it can be significantly reduced through design, material selection, and validation.

How is it tested?

Through contact resistance measurement under environmental stress conditions such as vibration and thermal cycling.


Improve Connector Reliability in Real Conditions

If your application involves high-current, high-voltage, or signal-critical systems, controlling contact resistance drift is essential.

FPIC provides custom connector and cable assembly solutions with a focus on long-term electrical stability and real-world reliability.

Contact us to discuss your project requirements.


Resources

  1. USCAR-2 – Performance Specification for Automotive Electrical Connector Systems: includes durability and contact resistance testing methods for automotive connectors.
  2. TE Connectivity – Contact Physics in Electrical Connectors: explains how micro-contact behavior influences resistance stability.
  3. Molex – Fretting Corrosion in Connector Systems: details the mechanisms behind resistance increase under vibration.
  4. Amphenol – Connector Design Fundamentals: covers materials, plating, and environmental considerations affecting electrical performance.
  5. IEC 60512 – Electrical Connector Testing: defines standardized methods for measuring contact resistance and durability.
Automotive connector

In automotive electrical systems, connector reliability is not only determined by material quality or contact design. Assembly accuracy plays an equally important role. Even a well-designed automotive connector can fail if it is not fully seated or if terminals are not properly locked in place.

To address these risks, modern automotive connectors often incorporate CPA (Connector Position Assurance) and TPA (Terminal Position Assurance) features. These mechanisms are designed to prevent assembly errors and ensure that connectors perform reliably under real-world conditions.

This article explains how CPA and TPA work, how they differ, and why they are essential for automotive connector reliability.

Automotive connector


Why Assembly Quality Matters in Connector Performance

Connector failures are often traced back to assembly-related issues rather than design flaws. Common problems include:

  • incomplete connector mating
  • terminal back-out during vibration
  • improper terminal insertion
  • insufficient locking force

These issues can lead to intermittent electrical contact, increased resistance, or complete system failure. In high-vibration automotive environments, even a small assembly defect can develop into a critical failure over time.

CPA and TPA mechanisms are specifically designed to reduce these risks.


What Is CPA (Connector Position Assurance)?

CPA is a secondary locking mechanism that ensures the connector is fully mated.

How CPA Works

The CPA device is typically a sliding or hinged component integrated into the connector housing. It can only be engaged after the connector halves are fully seated.

If the connector is not properly mated:

  • the CPA cannot be locked
  • visual or tactile feedback indicates incomplete assembly

This provides an additional layer of verification beyond the primary latch.

Key Benefits of CPA

  • prevents partial mating
  • provides clear assembly confirmation
  • reduces risk of disconnection under vibration
  • improves assembly consistency in production

CPA is especially important in applications where connectors are difficult to access or inspect after installation.


What Is TPA (Terminal Position Assurance)?

TPA is designed to ensure that individual terminals are fully inserted and properly retained within the connector housing.

How TPA Works

After terminals are inserted into the connector, the TPA component is installed or engaged to lock them in place. It prevents terminals from backing out due to vibration or handling.

If a terminal is not correctly positioned:

  • the TPA cannot be fully engaged
  • assembly is blocked until correction

This ensures proper terminal seating before final assembly.

Key Benefits of TPA

  • prevents terminal back-out
  • ensures correct terminal positioning
  • improves retention force
  • enhances long-term electrical stability

TPA is critical in maintaining contact integrity over the lifecycle of the vehicle.

Automotive connector


CPA vs TPA: Key Differences

Although CPA and TPA serve different functions, they are complementary.

  • CPA ensures the connector halves are fully mated
  • TPA ensures the terminals inside the connector are properly seated

In many automotive connectors, both mechanisms are used together to provide full assembly assurance.


How CPA and TPA Improve Real-World Reliability

Prevent Assembly Errors

Production environments involve manual or semi-automated assembly processes. CPA and TPA reduce human error by making incorrect assembly physically difficult or impossible.

Enhance Vibration Resistance

Automotive systems are exposed to continuous vibration. CPA prevents connectors from loosening, while TPA prevents terminals from shifting inside the housing.

Improve Inspection and Quality Control

Both CPA and TPA provide clear visual or tactile indicators of correct assembly, making inspection faster and more reliable.

Support Long-Term Performance

By ensuring proper initial assembly, CPA and TPA reduce the likelihood of gradual degradation such as fretting corrosion or intermittent contact.


Design Considerations for CPA and TPA Integration

When selecting or designing connectors with CPA and TPA features, engineers should consider:

  • ease of assembly and ergonomics
  • clear visual confirmation of engagement
  • compatibility with automated assembly processes
  • durability under repeated service cycles
  • space constraints within the system

Proper integration ensures that these features add value without increasing complexity.


How FPIC Supports Connector Reliability Solutions

Connector reliability depends on both component design and integration within the wire harness system. Features such as CPA and TPA must be correctly implemented and matched with appropriate terminals, housings, and assembly processes.

FPIC supports automotive and industrial connector projects with:

  • connector selection and application review
  • harness integration design
  • assembly process optimization
  • quality control and inspection support

By focusing on both design and manufacturability, FPIC helps reduce assembly errors and improve long-term reliability.


Final Thoughts

CPA and TPA are small features with a significant impact on automotive connector performance. While they may seem like minor design elements, they play a critical role in preventing assembly errors and maintaining reliable electrical connections.

In modern vehicles, where reliability expectations are extremely high, these mechanisms are essential components of a robust connector design strategy.


FAQ

What does CPA mean in connectors?

CPA stands for Connector Position Assurance, a mechanism that ensures the connector is fully mated.

What does TPA mean in connectors?

TPA stands for Terminal Position Assurance, which ensures terminals are properly inserted and retained.

Do all automotive connectors use CPA and TPA?

Not all connectors include both features, but they are commonly used in critical automotive applications.

Why are CPA and TPA important?

They prevent assembly errors, improve retention, and enhance long-term electrical reliability.

Can CPA and TPA fail?

They are generally reliable, but improper use or damage during assembly can affect their performance.


CTA

Improve Your Connector Reliability Strategy

If your application requires high reliability and consistent assembly quality, selecting connectors with proper assurance mechanisms is critical.

FPIC provides connector and wire harness solutions tailored for automotive and industrial applications.

Contact FPIC to discuss your connector and harness design requirements.


Resources

  1. TE Connectivity – Automotive Connector Design: explains connector locking systems including CPA and terminal retention mechanisms.
  2. Molex – Connector Assembly and Retention: covers terminal retention, connector locking, and assembly quality considerations.
  3. Amphenol Automotive – Connector Solutions: provides insight into connector design features for reliability and harsh environments.
  4. Aptiv – Connection Systems: discusses advanced automotive connection technologies and reliability improvements.
  5. Yazaki – Connector Technology: outlines connector design principles and assembly assurance features in automotive systems.