Connector Contact Resistance Causes and Prevention

Connector contact resistance is a critical electrical parameter that directly affects the reliability and efficiency of an electrical connection.

An ideal connector should provide a stable, low-resistance path between mating conductors. In real applications, however, the actual contact area is much smaller than the apparent physical contact area. Surface roughness, contact force, plating condition, contamination, vibration, temperature, and mechanical deformation can all influence the resistance of the connection.

When contact resistance increases, electrical losses and localized heating increase as well. The relationship can be expressed as:

P = I²R

where P is power loss, I is current, and R is contact resistance.

This becomes particularly important in high-current connectors, automotive systems, industrial automation equipment, energy storage systems, and other applications where connectors must operate reliably under continuous electrical and mechanical stress.

Understanding what causes contact resistance to increase—and how to prevent it—is therefore an important part of connector design and validation.
Connector Contact Resistance Causes and Prevention


1.What Is Connector Contact Resistance?

Connector contact resistance is the electrical resistance introduced at the interface between two mating conductive surfaces.

It is different from the resistance of the wire itself.

A simplified connection can be considered as:

Wire → Crimp → Terminal → Mating Contact → Terminal → Crimp → Wire

Each interface contributes to the overall electrical performance.

The mating contact is particularly important because two metal surfaces do not actually touch across their entire apparent area. Microscopic surface irregularities create localized conductive contact points known as asperities.

The effective electrical contact area is therefore much smaller than the visible mechanical contact area.

This is why contact force, surface condition, material selection, and plating have such a significant influence on connector resistance.


2.Why Low and Stable Contact Resistance Matters

Low contact resistance is important, but stable contact resistance over the connector’s service life is even more important.

A connector may initially show excellent electrical performance but experience increasing resistance after:

  • Repeated mating cycles
  • Vibration
  • Thermal cycling
  • Humidity exposure
  • Corrosion
  • High-current operation
  • Mechanical deformation
  • Surface wear

Increasing resistance can lead to several problems.

Electrical losses

Higher resistance increases voltage drop:

V = I × R

In low-voltage systems, even a small voltage drop can become significant.

Heat generation

Because:

P = I²R

heat generation increases rapidly as current rises.

For example, if current doubles, the resistive heating increases by approximately four times for the same resistance.

Accelerated degradation

Local heating can affect:

  • Contact plating
  • Terminal spring properties
  • Connector housing
  • Insulation
  • Sealing materials

This can create a feedback loop in which electrical degradation leads to additional thermal and mechanical degradation.


3.Contact Force and Contact Resistance

Contact force is one of the most important design factors affecting connector contact resistance.

When mating contacts are pressed together, sufficient force helps establish stable conductive contact points and break through surface films or contamination.

However, simply increasing contact force is not always the correct solution.

Excessive contact force can cause:

  • Higher insertion force
  • Difficult mating
  • Increased wear
  • Terminal deformation
  • Reduced connector service life

The objective is therefore to establish an appropriate contact-force window rather than maximizing force.

Important design factors include:

  • Contact geometry
  • Spring characteristics
  • Terminal material
  • Plating system
  • Contact wipe
  • Mating cycles
  • Required insertion force

A well-designed contact system should maintain adequate force throughout the expected operating life.


4.Contact Plating and Surface Condition

The contact surface plays a major role in electrical stability.

Common contact materials and plating systems are selected based on requirements such as:

  • Electrical conductivity
  • Corrosion resistance
  • Wear resistance
  • Mating frequency
  • Environmental exposure
  • Current level

Gold plating is commonly used where stable low-level electrical performance and corrosion resistance are important.

Tin plating can provide a practical solution for many applications, particularly where cost and current-carrying requirements are important.

However, plating selection should always be considered together with the contact geometry, environment, mating cycles, and application requirements.

Plating failure mechanisms

Contact resistance can increase when the surface experiences:

  • Wear-through
  • Oxidation
  • Corrosion
  • Plating porosity
  • Contamination
  • Mechanical damage

The correct plating system is therefore not simply a material-selection decision. It is part of the overall contact reliability strategy.


5.Fretting Corrosion and Vibration

Vibration can cause microscopic movement between mating contacts.

Although the movement may be too small to notice visually, repeated micro-motion can damage the contact surface.

This phenomenon is commonly associated with fretting corrosion.

A typical progression is:

Vibration → Micro-Motion → Surface Wear → Oxidation/Contamination → Increased Resistance

The problem can be especially challenging because a connector may pass a static resistance test while experiencing intermittent resistance changes during actual vibration.

Prevention strategies

Depending on the application, engineers can consider:

  • Appropriate contact force
  • Stable terminal retention
  • Suitable plating
  • Connector locking
  • Mechanical support
  • Cable strain relief
  • Vibration-resistant mounting

For vibration-sensitive systems, electrical monitoring during mechanical testing can provide more useful information than measuring resistance only before and after the test.


6.Crimp Quality Directly Affects Resistance

The contact interface is not the only resistance-sensitive area.

The wire-to-terminal crimp is another critical electrical connection.

A poor crimp can produce:

  • Higher resistance
  • Localized heating
  • Mechanical weakness
  • Intermittent electrical performance

Common causes include:

  • Incorrect crimp height
  • Wrong tooling
  • Improper conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Incorrect terminal-wire combination

How to control crimp resistance

Production quality control can include:

  • Crimp height measurement
  • Crimp force monitoring
  • Pull-force testing
  • Cross-section inspection
  • Electrical resistance testing

This is especially important for high-current and high-reliability cable assemblies.


7.Contamination and Oxidation

Even a well-designed contact system can experience resistance increases if the mating interface becomes contaminated.

Potential contaminants include:

  • Dust
  • Oil
  • Moisture
  • Chemical residues
  • Oxidation products
  • Assembly debris

Contamination can reduce the effective conductive area and interfere with stable metal-to-metal contact.

Environmental conditions therefore need to be considered during connector selection.

For outdoor or harsh industrial applications, engineers may need to evaluate:

  • Sealing
  • IP protection
  • Plating
  • Housing material
  • Environmental compatibility
  • Corrosion resistance

8.Connector Overheating and Thermal Runaway

High contact resistance is closely related to connector temperature rise.

Consider a high-current connection carrying 100 A.

If contact resistance is:

R = 1 mΩ

then:

P = 100² × 0.001 = 10 W

That means the contact interface is generating approximately 10 W of heat at that resistance.

If resistance increases to:

R = 2 mΩ

the heat generation becomes:

P = 100² × 0.002 = 20 W

The electrical loss has doubled.

This demonstrates why small changes in resistance can have a significant effect in high-current applications.

Thermal design should consider:

  • Current level
  • Number of energized contacts
  • Contact resistance
  • Ambient temperature
  • Duty cycle
  • Wire size
  • Connector housing
  • Heat dissipation
  • Installation conditions

Connector current ratings should therefore not be considered independently from the actual system conditions.


9.Mating Cycles and Contact Wear

Every mating and unmating operation can cause mechanical movement at the contact interface.

The contact surfaces may experience:

  • Sliding
  • Wiping
  • Friction
  • Plating wear
  • Spring deformation

After repeated cycles, the original surface condition may change.

For applications requiring frequent connection and disconnection, engineers should evaluate:

  • Rated mating cycles
  • Contact plating
  • Contact force
  • Wiping action
  • Wear resistance
  • Contact resistance after cycling

A connector should be validated against the actual expected service profile rather than relying solely on an initial resistance measurement.


10.Temperature Effects on Contact Resistance

Temperature can influence both electrical and mechanical properties.

As temperature changes, materials can expand and contract, affecting:

  • Contact dimensions
  • Contact force
  • Terminal alignment
  • Housing geometry
  • Plating interfaces
  • Crimp connections

High temperatures can also accelerate material aging and surface degradation.

Low temperatures may influence material flexibility and contact mechanics.

For connectors operating across wide temperature ranges, thermal cycling should therefore be included in reliability validation.


11.Connector Geometry and Current Distribution

Contact resistance is not determined by material alone.

The geometry of the contact system also matters.

Important design variables include:

  • Contact beam shape
  • Contact area
  • Contact normal force
  • Current path length
  • Terminal thickness
  • Contact alignment
  • Mating depth
  • Current distribution

For high-current applications, engineers need to consider how current flows through the complete terminal system rather than focusing only on the nominal contact area.

Poor geometry can create localized current concentration and thermal hotspots.


12.How to Measure Connector Contact Resistance

Accurate contact resistance measurement requires an appropriate test method.

For very low resistance values, ordinary two-wire measurements can be affected significantly by:

  • Test lead resistance
  • Connection resistance
  • Instrument limitations

A four-wire Kelvin measurement can provide better accuracy for low-resistance measurements because the current and voltage measurement paths are separated.

A simplified test arrangement is:

Current Source → Connector → Current Return

while separate sensing leads measure the voltage drop directly across the contact interface.

The resistance can then be calculated using:

R = V / I

Measurement consistency matters

Testing should define:

  • Test current
  • Test voltage
  • Measurement location
  • Mating condition
  • Stabilization time
  • Temperature
  • Number of samples
  • Acceptance criteria

Without consistent test conditions, resistance results may be difficult to compare.


13.Contact Resistance Testing During Reliability Validation

Initial resistance testing is only one part of connector validation.

A more useful strategy is to measure contact resistance at different stages.

For example:

Initial Measurement

↓

Mating Cycle Test

↓

Vibration Test

↓

Thermal Cycling

↓

Environmental Exposure

↓

Final Resistance Measurement

For demanding applications, electrical performance can also be monitored during mechanical or environmental testing.

This helps identify intermittent changes that may not be visible in a simple before-and-after measurement.


14.Common Connector Contact Resistance Problems

Problem Likely Cause Potential Solution
Initial resistance too high Poor contact geometry Optimize terminal design
Resistance increases after cycling Contact wear Review plating and contact force
Resistance fluctuates during vibration Fretting Improve retention and contact stability
Resistance rises at high current Thermal stress Optimize current capacity and thermal design
High wire-to-terminal resistance Poor crimp Improve tooling and process control
Resistance increases in humid environments Corrosion Improve sealing and plating
Different samples show large variation Process variation Strengthen dimensional and electrical controls
Localized terminal heating Current concentration Review contact geometry and current path

15.How to Prevent High Connector Contact Resistance

Preventing contact resistance problems requires cooperation between electrical, mechanical, material, and manufacturing design.

1.Optimize contact geometry

Design the contact system to maintain stable force and current distribution.

2.Select suitable plating

Match the plating system to electrical requirements, mating cycles, and environmental exposure.

3.Control crimp quality

Use controlled tooling, dimensional inspection, and appropriate mechanical and electrical verification.

4.Protect the contact interface

Use appropriate sealing and environmental protection for the application.

5.Control mechanical movement

Minimize vibration-induced micro-motion through proper locking, retention, mounting, and strain relief.

6.Validate under realistic conditions

Combine contact resistance testing with mating cycles, vibration, thermal cycling, and environmental exposure where applicable.

7.Monitor manufacturing variation

Stable connector performance requires stable production processes.


16.Design Considerations for High-Current Connectors

High-current applications are particularly sensitive to contact resistance.

Examples include:

  • Energy storage systems
  • Battery systems
  • Industrial power equipment
  • Power distribution
  • Automotive electrical systems
  • Inverters
  • Power conversion equipment

In these applications, engineers should evaluate the entire current path:

Cable → Crimp → Terminal → Contact Interface → Terminal → Crimp → Cable

A low-resistance contact interface cannot compensate for a poor crimp or undersized conductor.

The complete assembly therefore needs to be designed as one electrical and thermal system.


17.Manufacturing Controls for Stable Contact Resistance

For mass production, the challenge is not only achieving low resistance on one sample.

The objective is to maintain consistent performance across large production volumes.

Important controls may include:

  • Terminal dimensional inspection
  • Contact-force verification
  • Plating inspection
  • Crimp-height control
  • Crimp-force monitoring
  • Pull-force testing
  • Automated continuity testing
  • Contact resistance testing
  • Visual inspection
  • Traceability

Process data can help identify gradual changes before they become field failures.

For customized connectors and cable assemblies, early control of critical-to-quality characteristics can significantly improve production consistency.


How FPIC Supports Connector Electrical Reliability

FPIC develops customized connector and cable assembly solutions for industrial, automotive, energy, robotics, and other demanding applications.

Contact resistance can be evaluated as part of the complete electrical and mechanical design rather than treated as an isolated specification.

Depending on project requirements, engineering evaluation may cover:

  • Contact geometry
  • Terminal material
  • Plating
  • Contact force
  • Crimp design
  • Current capacity
  • Temperature rise
  • Environmental protection
  • Mating durability
  • Electrical testing
  • Reliability validation

This approach helps customers identify resistance-related risks early and develop connector systems with stable electrical performance throughout their intended service life.


Final Thoughts

Connector contact resistance is a small electrical parameter with potentially significant consequences.

When resistance increases, voltage drop and heat generation increase. In high-current systems, even a small resistance change can create substantial localized heating.

The most effective prevention strategy is therefore not simply to specify a low initial resistance.

Engineers should consider the complete system:

Contact Geometry + Contact Force + Plating + Crimp Quality + Environmental Protection + Mechanical Stability + Thermal Design + Validation

When these factors are controlled together, connector systems can maintain more stable electrical performance and reliability over their expected operating life.


FAQ

What causes connector contact resistance to increase?

Common causes include contact wear, insufficient contact force, damaged plating, fretting corrosion, contamination, oxidation, poor crimping, vibration, thermal cycling, and mechanical deformation.

Why does contact resistance cause connector overheating?

According to P = I²R, electrical power converted into heat increases with resistance and the square of current. High-current applications are therefore particularly sensitive to small resistance increases.

How is connector contact resistance measured?

Low-resistance connector contacts are commonly evaluated using controlled current and voltage measurements. Four-wire Kelvin measurement can improve measurement accuracy by reducing the influence of test lead resistance.

Does contact force affect connector resistance?

Yes. Contact force affects the stability and effective area of the conductive interface. Too little force can increase resistance, while excessive force can increase mating force and accelerate wear.

How can connector contact resistance be reduced?

Key methods include optimizing contact geometry, selecting suitable plating, controlling crimp quality, improving environmental protection, reducing vibration-induced micro-motion, and validating resistance after mechanical and environmental testing.


Need a Reliable Custom Connector Solution?

Looking for a connector solution with stable electrical performance under demanding operating conditions?

FPIC supports custom connector and cable assembly development, including contact design, terminal and plating selection, crimping, electrical testing, and reliability validation.

Contact FPIC to discuss your connector requirements and application conditions.


Resources

  1. TE Connectivity – Connector Solutions
    Technical resources covering connector systems, contacts, terminals, and electrical connection technologies.
    TE Connectivity Connector Solutions
  2. Molex – Connector Solutions
    Technical information covering connector design, contact technologies, and electrical performance considerations.
    Molex Connector Solutions
  3. IPC/WHMA-A-620 – Cable and Wire Harness Assemblies
    Industry requirements and acceptance criteria relevant to cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  4. IEC – International Electrotechnical Commission
    International standards and technical resources for electrical and electronic components and systems.
    IEC Standards
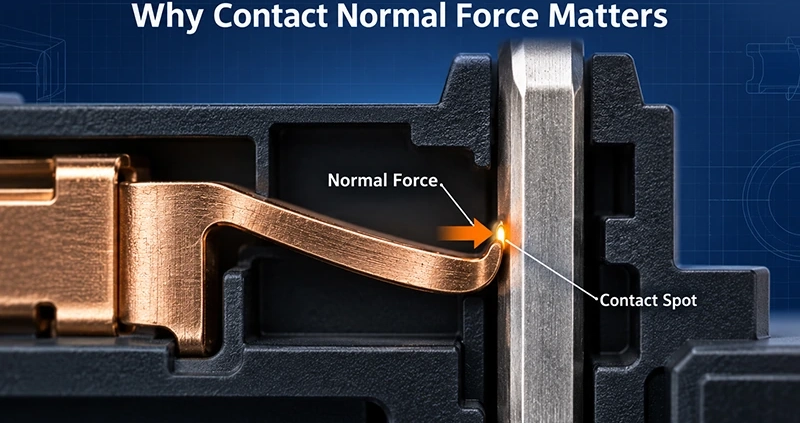
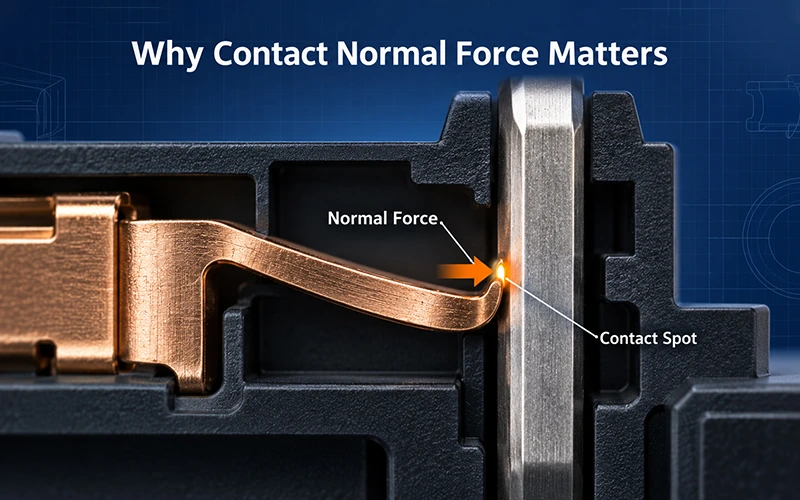
Spring contact applying normal force to a mating connector terminal

Contact normal force is the perpendicular load a spring contact applies to its mating surface. If that force is too low – or falls after heat, wear, or vibration – a connector can pass an initial continuity test yet develop unstable resistance later.

Short answer: A reliable separable contact needs enough normal force to create and preserve microscopic conductive contact spots. Too little force makes the interface more sensitive to surface films and movement. Excessive force increases mating effort, plating wear, and the risk of permanent deformation. The correct target is a controlled force window over the connector’s intended life.

That is why normal force should be treated as a lifetime design parameter, not just a value checked on a new sample.


What Is Contact Normal Force?

When a pin or blade enters a receptacle, the receptacle’s spring feature deflects. The elastic reaction presses the two conductive surfaces together. The component of that load acting perpendicular to the mating surface is the contact normal force.

The term is often confused with three other connector measurements:

Measurement What It Describes Why It Matters
Contact normal force Perpendicular load applied by the spring contact to the mating surface Controls the stability of the separable electrical interface
Mating and unmating force Axial force required to engage or separate the connector halves Affects assembly, serviceability, ergonomics, and wear
Terminal retention force Force required to pull a terminal from its housing cavity Verifies the terminal lock, lance, or secondary retention system
Crimp pull-out force Mechanical strength of the wire-to-terminal crimp Verifies the permanent termination, not the mating interface

A connector can meet terminal-retention and crimp requirements while still having inadequate spring force at the electrical contact point. It can also have acceptable normal force but excessive total mating force because seals, locks, alignment, friction, and multiple circuits add resistance during engagement.

Spring contact applying normal force to a mating connector terminal

How Contact Force Affects Contact Resistance

Metal surfaces may look smooth, but at microscopic scale they touch at small high points called asperities. Current therefore crosses the interface through a limited number of real contact spots rather than the full visible area.

Applying normal load deforms some asperities, increases effective contact area, and can help penetrate or displace oxide and contamination films. This reduces the constriction and film-related components of interface resistance. Research on electrical contact mechanics links constriction resistance to the mechanical stiffness and load of the interface, while also showing that surface films can strongly change the result.

It helps to separate three parts of a connector’s conductive path:

  1. Bulk resistance through the metal contact.
  2. Termination resistance at the crimp, solder joint, or press-fit section.
  3. Interface resistance where the separable contacts meet.

Normal force mainly influences the third part. Changing spring pressure does not repair a poor crimp, undersized conductor, damaged solder joint, or unsuitable base material.

More Force Is Not Always Better

At the low end, insufficient pressure can produce fewer stable contact spots and greater sensitivity to films, contamination, vibration, and tolerance variation. Raising the load generally reduces and stabilizes interface resistance, but the benefit does not continue without limit.

Excessive force can create other problems:

  • High insertion and withdrawal loads, especially in multi-position connectors
  • Faster wear of tin, gold, or other contact finishes
  • Damage to the mating surface during repeated operation
  • Permanent set if the spring exceeds its elastic design range
  • Housing distortion, difficult assembly, or incomplete mating

The engineering objective is therefore not maximum force. It is sufficient retained force with acceptable mating effort, wear, temperature rise, and dimensional margin. The target must be defined for the specific contact geometry, material, plating system, mating counterpart, environment, and required service life.

Spring Geometry and Material Set the Force Window

Within its elastic range, a contact spring behaves approximately as force equals stiffness multiplied by deflection. That simple relationship explains why the male contact, female spring, housing, and manufacturing tolerances must be designed as one system.

Spring stiffness and working stress are influenced by:

  • Beam length, width, thickness, and formed geometry
  • Contact angle and the location of the contact point
  • Bend radii and transitions that concentrate or distribute stress
  • Deflection created by the minimum and maximum mating-contact dimensions
  • Elastic modulus, yield strength, fatigue performance, and material temper
  • Residual stress introduced during stamping and forming

Thickness is especially sensitive in many spring designs because a small dimensional change can cause a much larger change in stiffness. The exact relationship depends on the contact form, so designers should use calculation or simulation together with physical force-displacement measurements.

Material Selection Is a Trade-Off

Brass, phosphor bronze, and higher-performance copper alloys can all be appropriate contact materials in the right design. Selection should consider conductivity, yield strength, formability, fatigue resistance, corrosion behavior, cost, and stress-relaxation performance at the expected temperature.

A highly conductive alloy may help control bulk heating but may not retain spring stress as well as another alloy. A stronger material may allow useful deflection in a compact geometry, but strength alone does not prove long-term force retention. Material temper, grain direction, forming history, and operating temperature also matter.

Production Variation Changes Real Contact Force

The CAD model represents a nominal condition. Production parts contain normal variation from strip thickness, stamping dimensions, forming angles, tool wear, material properties, plating thickness, housing dimensions, and mating-pin size.

These variations form a tolerance stack. At one extreme, the contact may be too loose. At the other, it may be overstressed or difficult to mate. Critical spring dimensions therefore require production controls linked to the force and electrical requirements they influence.

Plating and lubrication also affect friction. They can change total mating force even when spring pressure stays similar, which is another reason not to infer normal force from connector insertion force alone.

Stress Relaxation at High Temperature

Stress relaxation is the gradual loss of stress in a spring held at a substantially constant deflection. In a connector, the contact may remain mated while its spring load slowly decreases. Higher temperature generally accelerates this process, and different copper alloys can retain force at very different rates.

The contact experiences both ambient heat and self-heating. For a current-carrying interface, local power dissipation follows:

P = I²R

If interface resistance rises, local heating can rise. Higher temperature can then accelerate force loss, oxidation, or other degradation mechanisms. This does not mean every connector enters thermal runaway, but it shows why electrical, thermal, and mechanical design cannot be separated.

Designers often allow for expected force loss by starting above the minimum end-of-life requirement. However, simply increasing initial force can raise mating effort and plating wear. A better approach balances spring geometry, alloy, temperature exposure, finish, and required life so that sufficient force remains after aging without creating excessive force when new.

Repeated Mating Changes the Interface

Mating creates a wiping action between the contact surfaces. Controlled wiping can help disrupt surface films and establish a conductive contact region. The same sliding action also creates friction and gradually wears the finish.

Normal force affects both effects. Too little pressure may not create a stable interface. Too much pressure can increase friction and remove plating faster. Once the finish is locally worn through, exposed underplate or base metal may behave differently in humidity, pollutants, or corrosive environments.

Cycle count alone is therefore incomplete. A durability plan should define the mating counterpart, engagement speed, alignment, lubrication condition, environmental exposure, and measurements taken before and after cycling. Contact resistance and force after the required number of operations are more informative than a visual statement that the connector still mates.

Vibration and Micro-Movement

A connector lock prevents the housings from separating, but it does not automatically stop microscopic motion at the contact spot. Vehicle vibration, equipment movement, cable loading, and differential thermal expansion can produce small relative displacements inside a fully mated connector.

This movement can damage surface films and generate wear debris. With susceptible finishes and environments, the debris can oxidize and increase resistance – a process commonly associated with fretting corrosion. The result may be a gradual resistance increase or intermittent discontinuity that does not appear during a static bench check.

Retained normal force and suitable spring stiffness help stabilize the interface, but they are only part of the solution. Contact geometry, finish, lubrication where permitted, housing support, locking, cable strain relief, and vibration spectrum must be considered together.

Why Initial Continuity Does Not Prove Long-Term Reliability

A continuity check confirms that an electrical path exists at the moment of measurement. New, clean contacts can pass even when the design has limited margin against force loss or environmental aging.

An initial test does not by itself reveal:

  • How much normal force remains at the lowest material and dimensional condition
  • Whether high-temperature exposure will relax the spring
  • Whether the finish will survive the specified mating cycles
  • Whether vibration will cause micro-motion or intermittent events
  • Whether corrosion products will increase resistance
  • Whether current-induced heating will remain acceptable

Low-level contact resistance testing provides a more sensitive view of the mated interface than a basic continuity check. It should still be combined with mechanical and environmental conditioning. IEC 60512-2-1 defines a millivolt-level method for measuring resistance across mated contacts, while other parts of the IEC 60512 series address temperature rise, vibration, mechanical operation, and corrosion exposure.

The applicable customer specification may instead reference USCAR, LV214, EIA-364, or another sector-specific standard. The correct sequence, severity, sample preparation, monitoring method, and acceptance limits must come from the product’s detail specification and application requirements.

A Practical Contact Validation Plan

Long-term performance is best evaluated as a sequence rather than a group of unrelated pass/fail checks.

Validation Stage What to Control or Measure Engineering Question
Design input Current, temperature, vibration, mating cycles, environment, mating counterpart What conditions must the interface survive?
Material and dimensions Alloy, temper, strip thickness, spring geometry, plating, housing and mating-contact tolerances Does the full tolerance stack stay within the intended force window?
Baseline mechanics Force-displacement behavior, mating/unmating force, gauge retention where applicable Is the new contact mechanically correct without overstress?
Baseline electrical Low-level contact resistance, voltage drop, temperature rise or current derating as required Does the interface perform before conditioning?
Durability Specified mating cycles followed by force, resistance, and surface review Does wiping or wear change performance?
Thermal and climatic aging High-temperature exposure, thermal cycling, humidity, or corrosive atmosphere as applicable Does the spring retain force and does the finish protect the interface?
Dynamic testing Vibration and shock, with discontinuity monitoring when required Does the mated system remain stable under movement?
Final assessment Repeat mechanical and electrical measurements; inspect contact surfaces Is the design still within its acceptance limits after the full sequence?

IEC 60512-9-1 addresses mechanical operational endurance, IEC 60512-6-4 covers sinusoidal vibration, and IEC 60512-11-7 provides a flowing mixed-gas method for evaluating low-concentration pollutant effects on contacts. These standards define test methods, not universal acceptance values for every connector.

Questions to Resolve During Design Review

Before approving a contact system, engineering and procurement teams should ask:

  • What is the minimum required force after thermal aging and durability testing?
  • What force occurs at the maximum mating-contact dimension?
  • Could any tolerance condition exceed the material’s elastic limit?
  • What ambient temperature, current, and local temperature rise are expected?
  • Which plating system and thickness are specified at the contact zone?
  • How many mating operations must the interface withstand?
  • What vibration, shock, humidity, pollutant, or corrosive exposure applies?
  • How will force and resistance be measured before and after conditioning?
  • Which dimensions and material properties require production monitoring?

These questions turn a vague request for a “reliable terminal” into measurable design and validation requirements.

How FPIC Supports Contact-System Development

For applicable automotive, PCB, wire-to-board, and precision-terminal projects, FPIC can coordinate terminal design review, tooling, stamping, molding, assembly, and project-specific verification. Available laboratory support includes contact-resistance, insertion-and-withdrawal-force, temperature-rise, vibration, and coating-thickness checks according to the agreed validation plan.

The acceptance criteria remain product- and application-specific. Customers should provide the terminal and housing drawings, mating-contact dimensions, material and plating requirements, current, temperature range, mating cycles, environmental conditions, target volume, and applicable standards for technical evaluation.

Conclusion

A contact system needs normal force to remain inside the required window after tolerances, heat, mating wear, and vibration have done their work. Initial continuity is a starting measurement; long-term confidence comes from coordinated spring design, materials, manufacturing control, and sequence-based validation.

To discuss a custom connector, terminal, or PCB interconnect project, contact FPIC at info@fpiconn.com.


Frequently Asked Questions

What is contact normal force in a connector?

Contact normal force is the perpendicular load that a spring contact applies to its mating pin, blade, or pad. It helps establish and maintain the microscopic conductive spots at the separable interface.

Does higher contact force always reduce resistance?

No. Increasing a low force can improve interface stability, but excessive force can raise mating effort, wear the plating, distort the housing, or permanently deform the spring. Designers need a validated operating window rather than the highest possible value.

Is contact normal force the same as insertion force?

No. Normal force acts at the contact surface, while insertion force is measured in the mating direction and also includes friction, contact angle, seals, alignment, locks, and the combined effect of multiple circuits.

How does high temperature affect terminal spring force?

High temperature can accelerate stress relaxation, causing a deflected spring contact to lose load over time. The rate depends on alloy, temper, geometry, stress level, temperature, and exposure duration.

Can a connector pass continuity testing and still fail later?

Yes. A clean new interface may pass continuity even if it has limited margin against thermal relaxation, plating wear, fretting, corrosion, or dimensional variation. Mechanical and environmental conditioning followed by resistance measurement provides stronger evidence.

Which tests help evaluate long-term contact reliability?

The validation plan may include force-displacement measurement, low-level contact resistance, temperature rise or derating, mating durability, thermal aging, temperature cycling, humidity or corrosion exposure, vibration, shock, and post-test surface inspection. The applicable standard and limits depend on the product and application.


Resources

  1. B. N. J. Persson, “On the Electric Contact Resistance,” Tribology Letters, 2022.
  2. Materion, “What Is Stress Relaxation of Materials?” 2024.
  3. Materion, “How Can Connector Insertion Force Be Reduced?” 2024.
  4. Materion, “What Makes a Good Spring Material?” 2024.
  5. IEC 60512-2-1:2002, Contact Resistance – Millivolt Level Method.
  6. IEC 60512-5-1:2002, Temperature Rise.
  7. IEC 60512-6-4:2002, Vibration (Sinusoidal).
  8. IEC 60512-9-1:2010, Mechanical Operation.
  9. IEC 60512-11-7:2003, Flowing Mixed Gas Corrosion Test.
  10. SAE International, USCAR2-9, Performance Specification for Automotive Electrical Connector Systems, 2024.
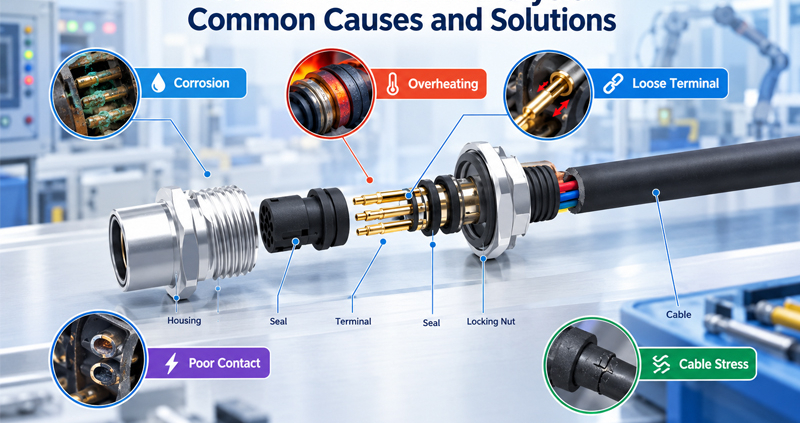
Connector Failure Analysis Common Causes and Solutions

Connectors are designed to provide a reliable electrical and mechanical interface between components, cables, and equipment. However, even a correctly specified connector can fail when electrical, mechanical, environmental, and manufacturing factors interact over time.

A connector failure may appear as a simple open circuit, intermittent signal, increased contact resistance, overheating, or mechanical disconnection. The visible symptom, however, is often not the actual root cause.

Effective connector failure analysis therefore requires more than replacing the failed component. Engineers need to determine why the connector failed, whether the failure originated in the contact system, terminal crimp, housing, sealing system, mating interface, or application environment.

This article examines the most common connector failure causes and explains practical methods for diagnosis, root-cause analysis, prevention, and validation.

Connector Failure Analysis Common Causes and Solutions


Why Connector Failure Analysis Matters

A connector is a system rather than a single component.

Its reliability depends on the interaction of:

  • Contact terminals
  • Plating and base materials
  • Connector housing
  • Crimp or termination system
  • Locking mechanism
  • Sealing components
  • Cable and strain relief
  • Mounting interface
  • Mating and unmating conditions
  • Electrical load
  • Temperature
  • Vibration and mechanical stress
  • Environmental contamination

A failure in any one of these areas can affect the complete electrical connection.

For example, an increase in contact resistance may initially appear to be a terminal problem. However, the actual cause could be insufficient contact force, fretting caused by vibration, damaged plating, terminal misalignment, or excessive thermal cycling.

This is why a structured failure analysis process is essential for demanding industrial and automotive applications.


1.Increased Contact Resistance

One of the most common connector problems is an increase in contact resistance.

When contact resistance rises, electrical losses increase according to:

P = I²R

At high current levels, even a relatively small increase in resistance can generate significant heat.

Common causes include:

  • Contact surface contamination
  • Oxidation or corrosion
  • Insufficient contact force
  • Damaged plating
  • Terminal deformation
  • Poor terminal alignment
  • Fretting corrosion
  • Excessive mating wear

Possible symptoms:

  • Localized heating
  • Voltage drop
  • Intermittent electrical performance
  • Discoloration around the terminal
  • Thermal damage to the housing

Solutions

Engineers should evaluate contact force, plating thickness, terminal geometry, mating cycles, and environmental conditions.

For high-current applications, the connector should also be evaluated under the actual operating current and temperature conditions rather than relying only on room-temperature resistance measurements.


2.Fretting Corrosion and Micro-Motion

Fretting is a particularly important failure mechanism in connectors exposed to vibration.

Small relative movements between mating contact surfaces can repeatedly disturb the contact interface. Over time, this can damage the plating and generate wear debris or oxidation products.

The result may be:

  • Increased contact resistance
  • Intermittent electrical connection
  • Signal instability
  • Progressive contact degradation

Fretting can be difficult to diagnose because the connector may initially pass a standard continuity test.

How to reduce fretting risk

Connector designs should consider:

  • Adequate contact normal force
  • Stable terminal retention
  • Appropriate plating systems
  • Mechanical locking
  • Vibration-resistant mounting
  • Proper cable strain relief

For applications involving continuous vibration, validation should include mechanical vibration testing combined with electrical monitoring.


3.Poor Crimping and Terminal Connection

A connector can contain a high-quality terminal and housing but still fail because the wire-to-terminal connection is defective.

Typical crimping problems include:

  • Insufficient crimp height
  • Excessive crimp height
  • Incorrect conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Improper tooling
  • Incorrect terminal-wire combination

A poor crimp can increase resistance and create mechanical weakness.

Why visual inspection alone is insufficient

A crimp may appear acceptable externally while having an internal defect.

For critical applications, manufacturers may use:

  • Crimp force monitoring
  • Crimp height measurement
  • Pull-force testing
  • Cross-section analysis
  • Electrical resistance testing

These controls help verify both mechanical and electrical integrity.


4.Connector Overheating

Connector overheating is often a secondary effect rather than the original failure.

A typical chain can be:

High Resistance → Heat Generation → Material Degradation → Higher Resistance → Thermal Failure

Potential causes include:

  • Excessive current
  • Undersized contacts
  • Insufficient contact force
  • Poor crimping
  • Contamination
  • Inadequate thermal management
  • Incorrect wire size
  • Loose or partially engaged terminals

How to prevent overheating

Connector selection should consider:

  • Rated current
  • Contact resistance
  • Wire gauge
  • Ambient temperature
  • Temperature rise
  • Duty cycle
  • Number of energized contacts
  • Housing material
  • Heat dissipation

The actual application conditions are particularly important because connector current ratings can depend on temperature and the number of simultaneously loaded circuits.


5.Terminal Back-Out and Poor Retention

A terminal may gradually move backward inside the connector housing if the retention mechanism is inadequate or the terminal is not fully inserted.

This can result in:

  • Reduced contact engagement
  • Intermittent connection
  • Increased resistance
  • Complete circuit interruption

Common causes

  • Incomplete terminal insertion
  • Damaged locking lance
  • Incorrect terminal dimensions
  • Excessive cable pulling force
  • Improper assembly
  • Housing deformation

Prevention

A robust connector system should incorporate reliable primary and secondary terminal locking where appropriate.

Manufacturing processes should also verify terminal insertion and retention rather than relying entirely on operator judgment.


6.Connector Mating and Misalignment Problems

Incorrect mating can cause mechanical and electrical damage.

Typical issues include:

  • Excessive insertion force
  • Cross-mating
  • Misalignment
  • Incomplete engagement
  • Damaged contacts
  • Housing deformation
  • Locking mechanism damage

A connector may appear connected while the terminals are not fully engaged.

Engineering solutions

Good connector design should provide clear mating guidance and positive locking feedback.

Depending on the application, features such as:

  • Polarization
  • Keying
  • Mechanical coding
  • CPA/secondary locks
  • Visual confirmation
  • Audible locking feedback

can reduce assembly errors.


7.Moisture, Dust, and Contamination

Environmental contamination is another major cause of connector degradation.

Moisture can promote corrosion, while dust, oil, chemicals, and other contaminants can affect contact interfaces and sealing performance.

This is particularly important for connectors used in:

  • Industrial automation
  • Outdoor equipment
  • Robotics
  • Automotive systems
  • Energy storage equipment
  • Medical equipment
  • Heavy machinery

Common symptoms

  • Corrosion
  • Leakage current
  • Increased contact resistance
  • Intermittent signals
  • Insulation degradation
  • Seal deterioration

Solutions

The connector’s environmental protection should match the actual application.

Depending on the system, engineers may need to evaluate:

  • IP protection
  • Seal material
  • Cable jacket compatibility
  • Connector material
  • Plating
  • Drainage
  • Chemical exposure
  • Temperature cycling

Waterproof performance should be validated under realistic environmental conditions rather than assumed from the connector specification alone.


8.Contact Plating Failure

Contact plating plays a critical role in long-term connector performance.

The plating system influences:

  • Corrosion resistance
  • Wear resistance
  • Contact stability
  • Mating durability
  • Environmental performance

A plating system that works well in a clean indoor application may not provide the same performance in a high-humidity, high-vibration, or corrosive environment.

Failure mechanisms may include:

  • Plating wear
  • Porosity
  • Oxidation
  • Corrosion
  • Base-metal exposure
  • Excessive mating wear

Therefore, plating selection should be based on the electrical requirements, mating cycles, environment, current level, and expected service life.


9.Mechanical Damage and Cable Strain

Connector failures do not always originate inside the connector.

Cable routing and mechanical loading can transfer excessive stress to the connector interface.

Typical causes include:

  • Excessive cable bending
  • Sharp routing angles
  • Insufficient strain relief
  • Pulling forces
  • Twisting
  • Repeated flexing
  • Incorrect mounting

Over time, these forces can damage terminals, seals, housings, or solder/crimp connections.

Prevention

A reliable connector assembly should consider the complete mechanical load path:

Cable → Strain Relief → Connector Housing → Terminal → Mating Interface

Proper strain relief and cable routing are therefore essential parts of connector reliability.


10.Thermal Cycling and Material Mismatch

Connectors used in industrial and automotive environments may experience repeated temperature changes.

Different materials expand and contract at different rates.

Repeated thermal cycling can influence:

  • Contact force
  • Terminal position
  • Housing dimensions
  • Seal compression
  • Crimp interfaces
  • Plating durability

A connector that performs well at room temperature may therefore experience degradation after repeated thermal cycles.

Recommended validation

Depending on the application, engineers may combine:

  • Thermal cycling
  • Temperature rise testing
  • Contact resistance measurement
  • Insulation resistance testing
  • Mechanical inspection

This helps determine whether electrical performance remains stable throughout the expected temperature range.


11.Vibration and Mechanical Shock

For industrial and automotive connectors, vibration can be a major reliability factor.

Repeated mechanical movement can affect:

  • Contact interfaces
  • Terminal retention
  • Housing locks
  • Cable terminations
  • Shielding connections

The key issue is that mechanical stress can eventually create an electrical failure.

Better validation strategy

Instead of performing vibration testing alone, combine mechanical vibration with continuous electrical monitoring.

For example:

Vibration → Electrical Monitoring → Contact Resistance Analysis → Physical Inspection

This approach can reveal intermittent failures that a simple post-test continuity check may miss.


12.A Structured Connector Failure Analysis Process

When a connector fails in the field or during testing, replacing the connector immediately can remove important evidence.

A structured investigation is more effective.

Step 1: Record the Failure Condition

Document:

  • Operating current
  • Voltage
  • Temperature
  • Environmental conditions
  • Mating cycles
  • Vibration exposure
  • Installation condition
  • Failure time
  • Electrical symptoms

Step 2: Perform Visual Inspection

Check for:

  • Discoloration
  • Melting
  • Corrosion
  • Cracks
  • Terminal displacement
  • Seal damage
  • Housing deformation

Step 3: Perform Electrical Testing

Depending on the failure mode:

  • Contact resistance
  • Continuity
  • Insulation resistance
  • HiPot
  • Voltage drop
  • Temperature rise

Step 4: Inspect the Terminal and Crimp

Evaluate:

  • Crimp geometry
  • Conductor placement
  • Pull strength
  • Terminal deformation
  • Contact surface condition

Cross-section analysis can be particularly useful for identifying internal crimp defects.

Step 5: Analyze the Environment

Determine whether the connector experienced:

  • Moisture
  • Dust
  • Chemicals
  • Salt exposure
  • Vibration
  • Thermal cycling
  • Mechanical stress

Step 6: Identify the Root Cause

Separate the failure symptom from the root cause.

For example:

  • Symptom: Connector terminal overheated
  • Immediate cause: Increased contact resistance
  • Root cause: Insufficient terminal contact force

This distinction is essential when developing corrective actions.


13.Connector Failure Analysis: Symptom vs Root Cause

Failure Symptom Possible Root Causes Recommended Investigation
High contact resistance Wear, corrosion, low contact force Contact resistance + terminal inspection
Connector overheating Excess current, poor contact, bad crimp Temperature rise + resistance test
Intermittent signal Fretting, vibration, terminal movement Vibration test + electrical monitoring
Terminal back-out Poor retention, incomplete insertion Retention and insertion inspection
Corrosion Moisture, chemicals, poor sealing Environmental and seal inspection
Broken housing Mechanical stress, impact, material issue Mechanical inspection
Crimp failure Incorrect tooling or wire positioning Crimp cross-section + pull test
Insulation failure Damage, contamination, thermal aging IR + HiPot + visual inspection

14.Preventing Connector Failures During Product Development

Failure analysis should not only be performed after a product fails.

The most effective approach is to integrate reliability thinking into the design stage.

Design Review

Evaluate:

  • Current and voltage requirements
  • Contact system
  • Plating
  • Housing material
  • Environmental protection
  • Locking system
  • Strain relief
  • Mating cycles
  • Vibration
  • Temperature range

DFM and Assembly Review

Check:

  • Terminal insertion
  • Crimp process
  • Assembly sequence
  • Error-proofing
  • Inspection points
  • Test coverage

Reliability Validation

Depending on the application, validation may include:

  • Contact resistance testing
  • Temperature rise testing
  • Mating cycle testing
  • Vibration
  • Mechanical shock
  • Thermal cycling
  • Humidity
  • Salt spray
  • Waterproof testing
  • Insulation resistance
  • HiPot testing

The exact test plan should be based on the connector’s application and applicable customer or industry requirements.


15.Manufacturing Quality Control Is Part of Connector Reliability

Many connector failures originate from process variation rather than fundamental product design.

Important production controls include:

  • Terminal dimensional inspection
  • Plating inspection
  • Crimp height monitoring
  • Crimp force monitoring
  • Pull-force testing
  • Terminal retention testing
  • Housing dimensional control
  • Automated electrical testing
  • Visual inspection
  • Traceability

For high-reliability applications, process capability and traceability are particularly important because they help manufacturers identify whether a failure is an isolated defect or part of a larger production trend.


How FPIC Supports Connector Reliability

FPIC supports customized connector solutions for demanding industrial and automotive applications.

Our engineering approach considers connector performance across the complete product lifecycle—from component selection and structural design to manufacturing, inspection, electrical testing, and reliability validation.

Depending on project requirements, connector development can include evaluation of:

  • Terminal and contact design
  • Contact plating
  • Housing materials
  • Sealing systems
  • Locking mechanisms
  • Crimp quality
  • Shield termination
  • Environmental protection
  • Electrical performance
  • Mechanical reliability

For automotive connector applications, FPIC also applies controlled manufacturing and quality processes designed for demanding production requirements.

This engineering-focused approach helps customers identify potential failure mechanisms earlier and develop connector solutions with more stable long-term performance.


Final Thoughts

Connector failure is rarely caused by a single factor.

Electrical loading, contact force, plating, crimp quality, vibration, temperature, contamination, sealing, and mechanical stress can interact throughout the connector’s service life.

A professional connector failure analysis process therefore needs to move beyond identifying the visible symptom. Engineers should determine the failure mechanism, trace it back to the root cause, and then verify that the corrective action actually eliminates the problem.

For critical applications, the best strategy is to combine design review, manufacturing process control, electrical testing, environmental validation, and failure analysis from the beginning of the product development cycle.


FAQ

What are the most common causes of connector failure?

Common causes include increased contact resistance, fretting corrosion, poor crimping, overheating, terminal back-out, contamination, vibration, thermal cycling, and mechanical stress.

How can connector overheating be prevented?

Select an appropriate connector and terminal system for the actual current, temperature, duty cycle, and environmental conditions. Contact resistance and temperature rise should also be validated.

Why do connectors develop intermittent failures?

Intermittent failures are often related to vibration, fretting corrosion, insufficient contact force, terminal movement, poor retention, or mechanical stress.

How can a bad connector crimp be identified?

Crimp height, crimp force, pull strength, electrical resistance, and cross-section analysis can be used to evaluate crimp quality.

Is visual inspection enough for connector quality control?

No. Visual inspection is useful but cannot detect every internal or electrical defect. Depending on the application, electrical testing, dimensional inspection, crimp analysis, and reliability testing may also be required.


Need a Reliable Custom Connector Solution?

Looking for a connector supplier that can support custom design, terminal development, connector assembly, electrical testing, and reliability validation?

FPIC can help evaluate your application requirements and develop connector solutions for industrial automation, automotive, robotics, energy systems, and other demanding applications.

Contact FPIC to discuss your connector project and reliability requirements.


Resources

  1. USCAR-2 – Performance Specification for Automotive Electrical Connector Systems
    A widely referenced specification for evaluating automotive connector performance and durability.
    USCAR-2 Information
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    Provides industry requirements and acceptance criteria for cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  3. TE Connectivity – Connector Solutions
    Technical information covering connector systems, terminals, contact technologies, and application requirements.
    TE Connectivity Connector Solutions
  4. Molex – Connector Solutions
    Technical resources covering connector design, electrical performance, reliability, and application engineering.
    Molex Connector Solutions
  5. IEC – International Electrotechnical Commission
    International standards and technical resources relevant to electrical and electronic component reliability and testing.
    IEC Standards
Connector Shielding Design for EMI Protection

As industrial equipment becomes faster, more compact, and more electronically integrated, electromagnetic interference (EMI) is becoming a more important design challenge. High-speed communication, servo drives, switching power supplies, motors, inverters, sensors, and control systems may all operate within the same equipment.

A connector is often treated as a simple interface between a cable and a device. However, in an EMC-sensitive system, the connector is also part of the shielding path.

A cable may have an effective shield, but if that shield is poorly terminated at the connector, EMI can still enter or leave the system through the connection point. This is why connector shielding should be considered as part of the complete cable and enclosure design rather than as an isolated connector feature.

This article explains the key principles of connector shielding design, including shield termination, 360° shielding, grounding, backshell selection, mechanical integration, and validation.

Connector Shielding Design for EMI Protection


Why Connector Shielding Matters for EMI Protection

EMI can affect electronic systems through conducted coupling, capacitive or inductive coupling, and radiated electromagnetic fields. Shielded cables are commonly used to reduce the exposure of signal conductors to external interference and to limit unwanted radiation from the cable.

However, the cable shield is only one part of the overall protection system.

A typical shielded connection may include:

  • Shielded cable
  • Connector shell
  • Shield termination
  • Backshell
  • Equipment enclosure
  • Ground or chassis connection

If one section has significantly higher impedance or poor mechanical contact, the effectiveness of the entire shielding system can be reduced.

TE Connectivity notes that shield termination at the backshell can provide a grounding path and that the complete circumference of a cable shield can be connected to the backshell to create a more continuous shielding structure.

This leads to an important design principle:

EMI protection depends on the continuity of the entire shielding path, not simply on whether a cable is labeled “shielded.”


Connector Shielding Starts With the Complete EMC Architecture

Connector selection should not happen independently from the cable, PCB, enclosure, and grounding strategy.

Before selecting a shielded connector, engineers should understand:

  • operating frequency range
  • signal type and data rate
  • cable construction
  • shielding method
  • enclosure material
  • grounding architecture
  • environmental conditions
  • vibration and mechanical requirements

A connector that performs well in one application may not provide the same EMC performance in another system.

For example, a high-speed industrial Ethernet application may have very different shielding requirements from a low-frequency sensor cable or a motor power connection.

Therefore, connector shielding should be designed as a complete signal path.


360° Shield Termination vs Partial Shield Termination

One of the most important considerations in connector shielding is how the cable shield is terminated.

A partial shield connection may create gaps or discontinuities around the connector interface. At higher frequencies, these discontinuities can become increasingly important because the shielding system must control electromagnetic fields rather than simply provide a low-frequency electrical connection.

A 360° termination connects the cable shield around its circumference to the connector shell or backshell.

This approach can provide a more continuous shielding path between the cable and connector.

TE Connectivity provides several connector and backshell solutions using 360° screen termination for EMI/RFI applications.

Why 360° Termination Is Important

A properly designed 360° termination can help:

  • reduce shielding discontinuities
  • maintain shield continuity through the connector
  • reduce unwanted radiation
  • improve immunity against external interference
  • support more consistent EMC performance

The exact termination method still needs to be selected according to cable construction, frequency range, environmental requirements, and mechanical constraints.

360° termination should therefore be considered a design strategy rather than a universal solution for every application.


The Connector Shell Is Part of the Shielding Path

For a shielded connector system, the metallic shell should not be treated simply as a mechanical housing.

It can form part of the electromagnetic shielding path between:

Cable Shield → Connector Shell → Equipment Interface → Chassis / Enclosure

Any discontinuity within this path can reduce the effectiveness of the overall shielding structure.

Important design considerations include:

  • conductive shell material
  • shell-to-shell contact
  • plating compatibility
  • contact pressure
  • surface contamination
  • connector mating stability
  • connection to the equipment chassis

For industrial applications exposed to vibration, the shielding interface must also remain electrically stable over the intended service life.

A connector may initially show good electrical continuity but lose performance if mechanical movement causes the shielding contact to degrade.


Backshell Design Has Multiple Functions

The backshell is another important component in connector shielding design.

Depending on the application, a backshell may provide:

  • EMI/RFI shield termination
  • cable strain relief
  • mechanical cable support
  • environmental sealing
  • cable routing control
  • connection between cable shield and connector shell

TE Connectivity describes backshells as components that can combine strain relief, EMI shielding, and environmental protection.

This makes backshell selection especially important for industrial equipment, robotics, servo systems, and other applications where cables experience vibration or repeated movement.

Select the Backshell Based on the Cable

A common design mistake is selecting a connector first and treating the backshell as an accessory afterward.

The backshell should be evaluated together with:

  • cable diameter
  • braid construction
  • foil or braid shield
  • number of shield layers
  • bend radius
  • required strain relief
  • sealing requirements
  • installation process

For example, a braided cable may require a different shield termination mechanism from a foil-shielded cable.


Shield Termination Must Balance EMI and Mechanical Reliability

A shielding connection is not useful if it cannot survive the mechanical environment.

Industrial harnesses may experience:

  • continuous vibration
  • repeated bending
  • torsion
  • temperature cycling
  • connector mating and unmating
  • cable pulling forces

The shield termination must therefore maintain electrical continuity while also providing sufficient mechanical retention.

A good design should prevent the cable shield from carrying mechanical loads that should instead be handled by the strain-relief system.

This distinction is important:

Shield termination provides electrical continuity; strain relief manages mechanical forces.

Combining these functions without proper design can create long-term reliability problems.


Grounding Strategy Is Critical

A shielded connector cannot provide effective EMI protection without a suitable grounding or chassis strategy.

The design team should determine where the shield should connect and how the shielding structure interacts with the system enclosure.

Possible considerations include:

  • chassis grounding
  • equipment enclosure bonding
  • connector shell grounding
  • cable shield termination
  • PCB ground connection
  • single-point or multi-point grounding strategy depending on frequency and system architecture

There is no universal grounding configuration for every application. The correct approach depends on the system topology, operating frequency, EMC requirements, and intended current paths.

For high-frequency systems, maintaining a low-impedance shielding path is often more important than simply achieving a low DC resistance measurement.


Avoid Pigtail Shield Termination When High-Frequency Performance Matters

A pigtail termination connects the cable shield to the connector or ground using a short wire.

Although simple and easy to manufacture, a long pigtail can introduce additional inductance into the shielding path. As frequency increases, that inductive impedance can become more significant.

This is why applications with demanding EMC or high-speed signal requirements often use shorter, wider, or circumferential shield termination methods instead of long pigtails.

The design decision should consider the actual frequency range and system requirements rather than applying one termination method universally.


Connector Shielding for High-Speed Industrial Communication

High-speed communication systems are particularly sensitive to shielding discontinuities.

Applications such as:

  • Industrial Ethernet
  • machine vision
  • industrial cameras
  • robotics
  • servo drives
  • motion control
  • high-speed sensors

can require carefully controlled shielding and grounding.

For example, TE Connectivity’s M12 X-Code connector solutions use a full metal shell and 360° cable shield termination to support high-speed data transmission and EMI protection.

This illustrates an important point: shielding design must support the complete transmission channel rather than focusing only on the connector contact itself.


Mechanical Design and EMC Performance Must Work Together

Connector shielding cannot be separated from mechanical design.

An industrial connector may need to withstand:

  • vibration
  • shock
  • repeated mating cycles
  • cable movement
  • temperature changes
  • moisture and dust

At the same time, it must maintain a stable shielding connection.

A loose shell, insufficient cable retention, or poorly controlled backshell assembly can gradually affect the shielding path.

For this reason, connector design should evaluate electrical and mechanical performance together.


Environmental Protection Can Affect Shielding Performance

Industrial connectors may operate in environments containing:

  • moisture
  • dust
  • oil
  • chemicals
  • condensation
  • salt contamination

These factors can affect conductive surfaces and mechanical interfaces.

Environmental sealing is therefore not completely separate from EMC design. A connector may require both:

EMI shielding + mechanical protection + environmental sealing

For example, a backshell may combine shield termination with a heat-shrink boot or other sealing structure. TE Connectivity’s backshell solutions demonstrate how shielding, strain relief, and environmental protection can be integrated into a single termination system.


How to Validate Connector Shielding Performance

Connector shielding should be validated as part of the complete cable assembly rather than only at component level.

Depending on the application, validation may include:

  • shield continuity testing
  • low-resistance measurement
  • EMC testing
  • radiated emission testing
  • conducted emission testing
  • immunity testing
  • vibration testing
  • temperature cycling
  • environmental exposure
  • connector mating-cycle testing

The validation method should reflect the actual application frequency range and operating environment.

A connector that passes a simple continuity test does not automatically provide adequate high-frequency EMI performance.


Common Connector Shielding Design Mistakes

Several common mistakes can reduce the effectiveness of an otherwise well-designed shielded cable assembly.

Using a shielded cable with an unshielded connector

The cable may have excellent shielding performance, but the connector interface creates an exposed section.

Terminating only part of the shield

Partial termination can create discontinuities that reduce overall shielding effectiveness.

Using excessive pigtail length

A long pigtail can add inductive impedance, particularly at higher frequencies.

Ignoring connector-to-chassis bonding

The connector shell needs an appropriate electrical relationship with the equipment enclosure.

Treating the backshell as only mechanical protection

A backshell may be a critical part of the EMI shielding and strain-relief system.

Ignoring manufacturing variation

A shielding concept that works in a prototype may perform differently if shield preparation, termination length, crimp force, or assembly position varies during mass production.


How FPIC Supports Shielded Connector and Cable Assembly Projects

For custom connector and cable assembly projects, shielding performance depends on the interaction between the connector, cable, shield termination, backshell, and assembly process.

FPIC supports custom connector and cable assembly development for industrial and other demanding applications, where connector selection, cable construction, shielding, sealing, and manufacturing consistency need to be considered together.

For applications such as industrial automation, robotics, industrial cameras, and control systems, early review of the complete cable-to-connector interface can help reduce EMC and reliability risks before mass production.

The objective is not simply to select a “shielded connector,” but to develop a complete interconnect system with a controlled electrical and mechanical shielding path.


Final Thoughts

Effective connector shielding design is about maintaining a continuous and controlled electromagnetic barrier from the cable through the connector and into the equipment enclosure.

The most important design considerations include:

  • appropriate connector shell construction
  • reliable shield termination
  • 360° shielding where required
  • suitable backshell design
  • controlled grounding and bonding
  • mechanical strain relief
  • environmental protection
  • validation under realistic operating conditions

For high-speed industrial equipment and EMC-sensitive systems, the connector should be treated as an active part of the shielding architecture.

A well-designed connector interface can help protect signal integrity, reduce EMI-related failures, and improve the long-term reliability of the complete cable assembly.


FAQ

What is connector shielding?

Connector shielding is the use of conductive connector shells, backshells, shield termination methods, and grounding structures to reduce electromagnetic interference entering or leaving an electrical connection.

Why is 360° shield termination important?

A 360° termination provides a continuous circumferential connection between the cable shield and connector shielding structure. It can help reduce shielding discontinuities and support more consistent EMI performance, particularly in demanding applications.

Is a metal connector enough for EMI protection?

No. A metal connector shell alone does not guarantee effective EMI protection. Cable shield termination, shell bonding, backshell design, grounding, cable construction, and assembly quality all influence the final shielding performance.

What is the difference between shield termination and strain relief?

Shield termination establishes electrical continuity between the cable shield and connector shielding structure. Strain relief manages mechanical forces on the cable. These functions should work together but should not be treated as the same function.

Are shielded connectors necessary for industrial Ethernet?

They may be necessary depending on the system architecture, data rate, EMC environment, cable construction, and applicable requirements. High-speed industrial communication systems often require carefully controlled shielding and grounding to maintain signal integrity.

How can connector shielding performance be tested?

Depending on the application, validation can include shield continuity, low-resistance measurement, EMC testing, radiated and conducted emissions, immunity testing, vibration, thermal cycling, and environmental testing.


Need a Custom Shielded Connector or Cable Assembly?

If your application requires reliable EMI protection for industrial automation, robotics, industrial cameras, motion control, or other demanding systems, connector and cable shielding should be considered together from the beginning.

FPIC supports custom connector and cable assembly projects with engineering review, connector integration, cable assembly, and production support.

Contact FPIC to discuss your connector shielding requirements.


Resources

  1. TE Connectivity – INTERCONTEC Connectors: provides examples of industrial connectors using 360° EMC shield termination for motor and industrial applications.
  2. TE Connectivity – Tinel-Lock Backshells for Military Applications: explains shield termination, backshell design, electrical continuity, strain relief, and 360° braid termination for demanding environments.
  3. TE Connectivity – M12 X-Code Connector Series: provides an industrial M12 example using a full metal shell and 360° cable shield termination for high-speed data applications.
  4. TE Connectivity – Space-Grade Backshells for Micro-D and D-Sub Connectors: discusses the relationship between EMI shielding, grounding, backshells, strain relief, and environmental protection.
  5. TE Connectivity – Screened Backshells and Adapters: provides examples of braided, banded, and 360° shield termination solutions for screened cable assemblies.
How Connector Plating Affects Performance and Lifetime

Connector contacts may look like simple metal components, but their surface finish plays a critical role in long-term electrical and mechanical performance.

A connector can have the correct housing design, terminal geometry and contact force, yet still experience reliability problems if the plating system is not appropriate for its application.

Connector plating influences:

  • Contact resistance
  • Corrosion resistance
  • Wear resistance
  • Mating performance
  • Electrical stability
  • Environmental durability
  • Contact lifetime

For automotive electronics, industrial automation, robotics, energy storage and other demanding applications, plating should therefore be treated as part of the overall connector reliability strategy.


1.Why Connector Plating Matters

The base metal of a contact provides the mechanical and electrical foundation, but its exposed surface interacts directly with the surrounding environment.

During service, a connector may encounter:

  • Humidity
  • Oxygen
  • Salt contamination
  • Dust
  • Chemicals
  • Temperature cycling
  • Mechanical vibration
  • Repeated mating and unmating
  • Electrical current

Without an appropriate surface finish, the contact interface can gradually deteriorate.

Typical consequences include:

Surface oxidation → higher contact resistance → localized heating → unstable electrical performance

In signal applications, surface deterioration can also contribute to intermittent electrical behavior.

This is why connector plating is not simply a cosmetic treatment. It is an engineered interface between the terminal and its operating environment.

How Connector Plating Affects Performance and Lifetime


2.What Is Connector Contact Plating?

Connector contact plating is a metallic coating applied to the surface of a conductive contact.

A typical contact system may contain several layers:

Base Contact Alloy

↓

Underplating

↓

Surface Plating

The base alloy provides the structural and electrical properties of the terminal.

The underplating can provide a barrier between the base material and surface plating while supporting adhesion and durability.

The surface plating is the layer that directly interacts with the mating interface and environment.

The performance of the complete system depends on how these layers work together.


3.Common Connector Plating Materials

Three commonly used plating materials are:

Plating Typical Characteristics Common Considerations
Tin Cost-effective, good conductivity, widely used Oxidation and wear must be considered
Gold Excellent corrosion resistance and stable contact interface Higher material cost
Silver High electrical conductivity Environmental and application conditions must be evaluated

The correct choice depends on the electrical, mechanical and environmental requirements rather than simply choosing the highest-value material.


4.Tin Plating

Tin is widely used for connector terminals because it provides a practical balance between performance and cost.

It is commonly considered for applications where:

  • Cost efficiency is important
  • Current levels are moderate to high
  • The connector operates in controlled environments
  • Mating frequency is limited or appropriately managed

Tin-plated contacts are often used in automotive and industrial electrical systems.

However, engineers should consider surface condition, contact force, oxidation behavior and mechanical wear.

For applications involving frequent mating or demanding environmental exposure, the complete plating design should be evaluated rather than looking only at the presence of tin plating.


5.Gold Plating

Gold is widely recognized for its excellent resistance to corrosion and stable surface characteristics.

It is particularly valuable where reliable low-level electrical contact is important.

Typical applications may include:

  • Signal connectors
  • Control electronics
  • Communication equipment
  • Industrial sensors
  • Medical electronics
  • High-reliability electronic systems

Gold plating can help maintain a stable contact interface under challenging environmental conditions.

However, gold plating is not automatically the best choice for every connector.

Engineers should also consider:

  • Plating thickness
  • Underplating
  • Contact force
  • Mating cycles
  • Base material
  • Operating environment
  • Cost target

A thin gold layer and a properly engineered gold-plating system are not necessarily equivalent.


6.Silver Plating

Silver has very high electrical conductivity and can be considered for applications where electrical performance and current handling are important.

However, silver surfaces can be affected by environmental exposure and surface contamination.

Therefore, silver plating should be evaluated according to:

  • Operating temperature
  • Current level
  • Environmental conditions
  • Contact geometry
  • Exposure to contaminants
  • Required service life

The key engineering principle is the same:

Select the plating system according to the actual operating environment.


7.How Plating Affects Contact Resistance

Contact resistance is one of the most important electrical characteristics of a connector.

Even when the bulk resistance of the terminal is low, the actual mating interface can introduce additional resistance.

A reliable plating system helps maintain a stable contact interface.

If the surface deteriorates through oxidation, corrosion or wear, contact resistance can increase.

Higher contact resistance can contribute to:

Electrical loss → Heat generation → Further degradation

This becomes especially important in higher-current applications.

For this reason, engineers should evaluate plating together with:

  • Contact force
  • Contact geometry
  • Current level
  • Terminal material
  • Surface condition
  • Temperature

Plating cannot compensate for an incorrectly designed contact system.


8.Why Plating Thickness Matters

One of the most common mistakes is evaluating plating only by material type.

For example:

Gold plated

does not fully describe the performance of a gold-plated contact.

Engineers should also consider the plating thickness and overall plating structure.

Plating thickness can influence:

  • Corrosion protection
  • Wear resistance
  • Surface durability
  • Mating lifetime
  • Barrier performance
  • Long-term contact stability

However, thicker plating is not automatically better.

Increasing plating thickness may increase cost without providing meaningful additional performance for a specific application.

The correct approach is to establish the required performance first and then define an appropriate plating system.


9.Gold Plating Thickness and Mating Cycles

For connectors with frequent mating and unmating, mechanical wear becomes a major consideration.

Every mating cycle can generate mechanical interaction between the contact surfaces.

Over time, repeated movement can gradually wear the plating.

Therefore, engineers should evaluate:

Plating Thickness + Contact Geometry + Contact Force + Mating Cycles

rather than considering plating thickness independently.

For example, a connector designed for frequent maintenance may require a different surface treatment strategy from a connector that is assembled once and expected to remain connected throughout its service life.


10.The Role of Underplating

Underplating is often overlooked because it is not visible from the finished connector surface.

However, it can play an important role in the plating system.

A properly selected underlayer can help:

  • Improve the barrier between base metal and surface plating
  • Support plating adhesion
  • Reduce migration between material layers
  • Improve long-term plating stability

The exact layer structure depends on the contact material, plating technology and application requirements.

Therefore, plating should be evaluated as a layered system, not as a single metallic coating.


11.Connector Plating and Corrosion Resistance

Corrosion is one of the major causes of connector degradation.

Environmental factors can include:

  • Moisture
  • Salt
  • Humidity
  • Industrial chemicals
  • Pollutants
  • Condensation

Corrosion at the contact interface can change the surface condition and increase electrical resistance.

For connectors used in harsh environments, engineers should consider the combined effect of:

Plating + Sealing + Housing + Environmental Protection

This is particularly important for automotive and industrial connectors installed outside protected electronic enclosures.


12.Connector Plating and Wear

Corrosion is not the only threat to plating.

Mechanical wear can also remove or damage the surface layer.

Common sources include:

  • Repeated mating
  • Vibration
  • Sliding contact movement
  • Cable movement
  • Terminal deformation
  • Assembly processes

A connector designed for high mating-cycle performance needs a plating system that can withstand the expected mechanical interaction.

This means plating selection should be connected to the connector’s mechanical design.


13.Connector Plating for High-Current Applications

High-current connectors introduce additional considerations.

As current increases, even a small increase in contact resistance can become more significant because electrical power dissipation at the contact interface increases with resistance.

Therefore, high-current connector design should consider:

  • Contact material
  • Contact cross-section
  • Contact force
  • Contact area
  • Plating
  • Thermal management
  • Terminal connection quality

For energy storage, power distribution and industrial equipment, plating should be evaluated together with the complete current-carrying system.

Plating alone does not determine current capacity.


14.Connector Plating for Signal Applications

Signal connectors have a different set of priorities.

Very low-level electrical signals can be sensitive to surface contamination and contact instability.

For these applications, engineers may prioritize:

  • Stable contact resistance
  • Corrosion resistance
  • Surface cleanliness
  • Low-level signal reliability
  • Mating-cycle performance

Gold plating is often considered in applications where maintaining a stable contact interface is particularly important.

However, the final selection still depends on connector design and operating conditions.


15.Automotive Connector Plating

Automotive connectors can experience challenging conditions, including:

  • Vibration
  • Temperature cycling
  • Humidity
  • Contamination
  • Repeated electrical loading
  • Long service periods

Therefore, plating selection must be integrated into the overall connector design.

Engineers should evaluate:

  • Terminal Material
  • Plating System
  • Contact Force
  • Sealing
  • Mechanical Retention
  • Environmental Requirements

For automotive connector production, consistent plating quality is also important because variations in surface condition can affect electrical and mechanical performance.


16.Industrial Connector Plating

Industrial connectors may be exposed to:

  • Dust
  • Oil
  • Chemicals
  • Humidity
  • Vibration
  • Frequent maintenance

Applications such as automation equipment, robotics, sensors and control cabinets may also require repeated connector service.

Therefore, plating selection should consider both environmental resistance and mechanical wear.

A connector that performs well in a clean indoor environment may require a different plating strategy when used in a factory environment with vibration, contamination or frequent maintenance.


17.Connector Plating Selection Matrix

Application Requirement Key Plating Consideration
Low-cost electrical connection Cost-effective plating system
High corrosion resistance Stable corrosion-resistant surface
Frequent mating Wear resistance + plating thickness
Low-level signals Stable contact interface
High current Contact resistance + thermal performance
High humidity Corrosion resistance + sealing
Industrial environment Chemical and contamination resistance
Automotive application Environmental + mechanical durability
Long service life Complete plating system validation

The table should be used as an engineering starting point rather than a universal material-selection rule.


18.Common Connector Plating Selection Mistakes

Mistake 1: Choosing plating only by material

Selecting “gold” or “tin” without considering thickness, base material and application requirements can lead to an incomplete specification.

Mistake 2: Assuming thicker is always better

More plating may increase cost without providing proportional performance benefits.

Mistake 3: Ignoring mating cycles

A plating system suitable for one-time assembly may not be suitable for repeated maintenance.

Mistake 4: Ignoring the environment

Humidity, salt, chemicals and contamination can significantly influence surface durability.

Mistake 5: Evaluating plating separately from contact design

Contact force, geometry and plating work together to determine interface performance.

Mistake 6: Focusing only on initial electrical performance

A connector may pass initial electrical testing but still experience degradation during long-term environmental or mechanical exposure.


19.How to Define a Connector Plating Specification

A practical engineering specification should include more than the plating material.

Consider defining:

1.Base Contact Material

Examples include brass, phosphor bronze and other copper alloys.

2.Underplating

Define the required layer structure according to the manufacturing process and application.

3.Surface Plating

Specify tin, gold, silver or another suitable finish.

4.Plating Thickness

Define the required thickness according to performance requirements.

5.Mating Requirements

Specify expected mating and unmating cycles.

6.Environmental Requirements

Consider temperature, humidity, corrosion, chemicals and contamination.

7.Electrical Requirements

Evaluate current, voltage, contact resistance and signal characteristics.

8.Validation Requirements

Define the appropriate electrical, mechanical and environmental tests.

This creates a much stronger specification than simply stating:

“Gold plated connector.”


20.Connector Plating Quality Control

For mass production, plating quality needs to be controlled consistently.

Depending on the product and specification, manufacturers may monitor:

  • Plating thickness
  • Surface appearance
  • Adhesion
  • Contact resistance
  • Corrosion performance
  • Mechanical wear
  • Terminal dimensions
  • Base material consistency

Process control is particularly important because plating variation can affect the finished contact interface.

A robust quality system should connect:

Incoming Material → Stamping → Plating → Terminal Processing → Assembly → Electrical Testing → Final Inspection

This helps identify potential variation before products reach the customer.


21.How FPIC Supports Connector Plating and Reliability

For custom connector projects, plating should be considered during the engineering and DFM stages rather than added as a final specification.

FPIC can support connector development by evaluating the relationship between:

  • Contact material
  • Plating system
  • Terminal geometry
  • Contact force
  • Connector structure
  • Application environment
  • Manufacturing requirements
  • Electrical performance

For automotive connector applications, FPIC operates an IATF 16949 quality management system and applies controlled manufacturing and inspection processes to support consistent connector production.

The objective is not simply to provide a specific plating material, but to develop a plating and contact system that matches the customer’s actual operating requirements.


22.A Practical Connector Plating Selection Workflow

A useful engineering workflow is:

Step 1 — Define the Application

Automotive, industrial, robotics, energy storage, medical or electronics.

↓

Step 2 — Define the Environment

Temperature, humidity, corrosion, chemicals and contamination.

↓

Step 3 — Define Electrical Requirements

Current, voltage, contact resistance and signal requirements.

↓

Step 4 — Define Mechanical Requirements

Mating cycles, vibration, insertion force and contact movement.

↓

Step 5 — Select the Contact Material

Choose an appropriate conductive alloy based on mechanical and electrical requirements.

↓

Step 6 — Select the Plating System

Evaluate surface plating, underplating and thickness.

↓

Step 7 — Validate

Conduct appropriate electrical, mechanical and environmental testing.

This approach reduces the risk of selecting plating based solely on material name or initial cost.


23.Final Thoughts

Connector plating is a small physical layer with a major impact on long-term connector performance.

The right plating system can help maintain:

  • Stable contact resistance
  • Corrosion resistance
  • Mechanical durability
  • Mating performance
  • Electrical reliability
  • Long service life

But plating should never be evaluated independently.

The final performance depends on the complete system:

Contact Material + Plating + Thickness + Contact Force + Geometry + Sealing + Environment

For engineers designing reliable connectors, the key question is not:

“Which plating is best?”

It is:

“Which plating system provides the required performance for this application throughout the expected service life?”


FAQ

What is connector plating?

Connector plating is a metallic surface coating applied to electrical contacts to improve properties such as corrosion resistance, contact stability and wear performance.

Is gold plating better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact characteristics, while tin can offer a practical balance between performance and cost. The correct choice depends on the application.

Why does connector plating thickness matter?

Plating thickness can affect corrosion protection, wear resistance and service life. However, thicker plating is not automatically better because cost and application requirements must also be considered.

Does plating affect connector contact resistance?

Yes. Surface condition and plating can influence the stability of the contact interface and therefore affect contact resistance over the connector’s service life.

What plating is suitable for high-current connectors?

There is no single plating material that is universally best for high-current connectors. Engineers should evaluate plating together with contact material, geometry, contact force, resistance and thermal requirements.

How does plating affect mating cycles?

Repeated mating creates mechanical wear at the contact interface. The plating material, thickness, contact geometry and force all influence how well the surface withstands repeated cycles.

Should connector plating be specified during DFM?

Yes. Plating should be considered during connector design and DFM because it affects material selection, manufacturing processes, cost and long-term reliability.


Need Help Selecting the Right Connector Plating?

Choosing the right plating system requires more than selecting gold, tin or silver.

FPIC can help evaluate contact material, plating, terminal design, environmental requirements and manufacturing considerations for custom connector applications.

Talk to our engineering team about your connector requirements.


Resources

  • IPC/WHMA-A-620 — Requirements and Acceptance for Cable and Wire Harness Assemblies
  • SAE — Automotive engineering standards and specifications
  • IEC — International electrotechnical standards
  • IATF 16949 — Automotive quality management system requirements
Connector Material Selection Guide for Engineers

A connector may look simple from the outside, but its reliability depends heavily on the materials used throughout the assembly.

A typical connector includes several material systems:

Housing + Contacts + Plating + Seals + Locks + Secondary Components

Each material has a different function.

The housing must provide insulation and mechanical protection. The contact system must maintain stable electrical performance. Plating must protect the contact interface from corrosion and wear. Seals must maintain environmental protection without compromising assembly performance.

Selecting materials based only on cost or a single specification can create reliability problems later in the product lifecycle.

For demanding applications such as automotive electronics, industrial automation, robotics, medical equipment, and energy systems, material selection should therefore be treated as a system-level engineering decision.

The objective is to balance:

Electrical Performance + Mechanical Strength + Thermal Stability + Environmental Resistance + Manufacturability + Cost

Connector Material Selection Guide for Engineers


Why Connector Material Selection Matters

Connector materials directly influence how a connector performs throughout its service life.

Poor material selection can contribute to:

  • Contact resistance increase
  • Corrosion
  • Terminal deformation
  • Housing cracking
  • Seal degradation
  • Insulation failure
  • Poor mating performance
  • Reduced vibration resistance
  • Premature connector failure

For example, a housing material may meet the required temperature rating but lack sufficient mechanical strength.

Likewise, a contact alloy may provide excellent conductivity but require a different plating system to achieve the required corrosion and wear resistance.

This is why engineers should evaluate the complete material combination, rather than selecting each material independently.


1.Connector Housing Material Selection

The connector housing provides:

  • Electrical insulation
  • Mechanical support
  • Terminal positioning
  • Mating alignment
  • Environmental protection
  • Structural protection

The housing material therefore needs to withstand the expected electrical, thermal, mechanical, and environmental conditions.

Common connector housing materials include:

  • PA / Nylon
  • PBT
  • PPS
  • LCP
  • PEEK
  • PC and other engineering polymers

The best material depends on the application rather than simply its nominal strength.


2.PA / Nylon

Polyamide materials are widely used in connector housings because they can provide a useful combination of:

  • Mechanical strength
  • Impact resistance
  • Processability
  • Cost efficiency

However, different grades can behave differently in terms of:

  • Water absorption
  • Dimensional stability
  • Temperature resistance
  • Chemical resistance

For applications involving humidity or significant temperature variation, engineers should evaluate the specific PA grade rather than treating all nylon materials as equivalent.


3.PBT

Polybutylene terephthalate, or PBT, is commonly used for electrical and automotive connector housings.

Potential advantages include:

  • Good dimensional stability
  • Electrical insulation
  • Chemical resistance
  • Suitable molding characteristics
  • Good temperature performance for many applications

PBT can be attractive where dimensional precision and electrical insulation are important.


4.PPS for Higher-Temperature Applications

Polyphenylene sulfide (PPS) is an engineering polymer commonly considered for demanding thermal and chemical environments.

Potential characteristics include:

  • High temperature resistance
  • Low moisture absorption
  • Good dimensional stability
  • Chemical resistance
  • Electrical insulation

PPS can be useful when the connector must maintain dimensional stability under elevated temperatures.

However, material selection should always consider the actual temperature profile, not simply the maximum advertised material temperature.


5.LCP for Fine-Pitch Connectors

Liquid crystal polymer (LCP) is often considered for compact and fine-pitch connector designs.

Its characteristics can support applications requiring:

  • Thin-wall molding
  • Dimensional precision
  • Fine-pitch structures
  • Good thermal performance
  • Low moisture absorption

As connector dimensions decrease, housing dimensional stability becomes increasingly important.

A material suitable for a large connector may not necessarily be the best choice for a miniature high-density connector.


6.PEEK for Highly Demanding Applications

PEEK is a high-performance engineering polymer used in applications requiring demanding combinations of:

  • Temperature resistance
  • Chemical resistance
  • Mechanical strength
  • Dimensional stability

Its higher material cost means it is generally considered when standard engineering plastics cannot adequately meet the application requirements.

Material selection should therefore consider total system requirements, rather than simply selecting the highest-performance material available.


7.Flame Retardancy

For many electronic and industrial applications, connector housing materials may need to meet specific flammability requirements.

Engineers should consider:

  • Applicable safety requirements
  • Electrical application
  • Equipment enclosure
  • Operating voltage
  • Installation environment

A flame-retardant grade can affect other material characteristics such as:

  • Mechanical strength
  • Flow behavior
  • Moldability
  • Cost

Therefore, flame retardancy should be evaluated together with the overall material specification.


8.Connector Contact Material Selection

The contact system is responsible for maintaining the electrical interface.

Common contact alloys include:

  • Copper
  • Brass
  • Phosphor bronze
  • Copper alloys
  • Beryllium copper for specialized applications

The selected material affects:

  • Electrical conductivity
  • Spring properties
  • Contact force
  • Fatigue resistance
  • Thermal behavior
  • Corrosion resistance
  • Manufacturability

A connector contact must provide both electrical performance and mechanical reliability.


9.Brass Contacts

Brass is widely used for connector terminals because it provides a practical balance of:

  • Conductivity
  • Strength
  • Formability
  • Cost

It can be suitable for many general-purpose connector applications.

However, for high-flex or high-contact-force applications, another copper alloy may provide more suitable mechanical properties.


10.Phosphor Bronze Contacts

Phosphor bronze can provide good spring characteristics and fatigue resistance.

It is often considered when the contact must maintain stable mechanical behavior during repeated mating or long-term operation.

Potential applications include:

  • Signal connectors
  • Control connectors
  • Industrial equipment
  • Repeated mating interfaces

The final choice depends on the required contact force, conductivity, mating cycles, and environmental conditions.


11.Beryllium Copper

Beryllium copper can provide excellent spring properties and good electrical conductivity.

It may be considered for applications requiring:

  • High contact force
  • Miniaturized contacts
  • Repeated mating
  • Strong elastic recovery

Because material cost and processing considerations can be higher, engineers should use it when its performance advantages justify the additional complexity.


12.Contact Plating Selection

Contact plating forms the actual surface interface between mating contacts.

Common plating materials include:

Tin

Tin is widely used for cost-sensitive applications and can provide practical performance for many power connections.

Gold

Gold plating provides excellent corrosion resistance and stable contact behavior.

It is particularly useful where:

  • Low-level signals are involved
  • Long-term contact stability is important
  • Corrosive environments are present
  • High mating-cycle performance is required

Silver

Silver has excellent electrical conductivity and can be considered for certain power and high-current applications.

However, its behavior under specific environmental conditions must be carefully evaluated.


13.Gold Plating Thickness Matters

Simply specifying “gold plated” is not enough.

Engineers should also consider:

  • Gold thickness
  • Plating area
  • Underplating
  • Contact force
  • Mating cycles
  • Operating environment

A thin decorative gold layer and an engineered contact plating system do not necessarily provide the same long-term performance.

For demanding applications, plating specifications should be clearly defined in the connector drawing or technical specification.


14.Underplating Matters Too

The plating system can include multiple layers.

For example:

Base Contact Alloy → Underplating → Gold Surface

The underplating can help provide:

  • Corrosion protection
  • Diffusion resistance
  • Better plating stability

The complete plating structure should therefore be evaluated rather than looking only at the visible surface material.


15.Connector Seal Material Selection

Seals become critical when connectors must resist:

  • Water
  • Dust
  • Oil
  • Chemicals
  • Temperature cycling

Common sealing materials include:

  • Silicone rubber
  • EPDM
  • Fluoroelastomer materials
  • Other application-specific elastomers

The correct seal depends heavily on the environment.


16.Silicone Seals

Silicone can provide good flexibility across a broad temperature range.

It is commonly considered where connectors must tolerate:

  • Temperature variation
  • Repeated assembly
  • Flexible sealing interfaces

However, chemical compatibility must still be evaluated for the actual application.


17.EPDM Seals

EPDM can provide good resistance to:

  • Water
  • Weathering
  • Ozone
  • Certain environmental conditions

It may be suitable for outdoor or automotive environments depending on the specific fluid and temperature exposure.


18.Chemical Compatibility Is Critical

A connector material may perform well in a laboratory but degrade when exposed to the actual application environment.

Potential contaminants include:

  • Automotive fluids
  • Lubricants
  • Cleaning agents
  • Coolants
  • Hydraulic fluids
  • Industrial chemicals

Material compatibility should therefore be validated against the actual chemicals and concentrations expected during the connector’s service life.


19.Temperature Selection Should Consider the Complete System

Connector temperature performance is not determined by housing material alone.

The complete system includes:

Current → Contact Resistance → Heat Generation → Housing → Surrounding Environment

Higher current can increase temperature at the contact interface.

This means the connector must be evaluated under realistic electrical loading.

Engineers should consider:

  • Ambient temperature
  • Current load
  • Number of loaded circuits
  • Contact resistance
  • Heat dissipation
  • Housing material
  • Installation conditions

20.Material Selection for High-Current Connectors

High-current connectors place greater demands on the contact system.

Important factors include:

  • Contact resistance
  • Conductivity
  • Contact force
  • Terminal cross-section
  • Plating
  • Temperature rise
  • Thermal dissipation

Simply choosing a highly conductive alloy does not automatically create a reliable high-current connector.

The complete contact geometry and mechanical interface also matter.


21.Material Selection for Fine-Pitch Connectors

Miniaturized connectors create different material challenges.

As pitch decreases:

  • Housing walls become thinner
  • Terminal spacing decreases
  • Dimensional tolerances become tighter
  • Mating alignment becomes more sensitive

Materials with good dimensional stability and molding precision may therefore become increasingly important.

This is one reason material selection should be performed together with connector geometry and manufacturing process development.


22.Material Selection for Automotive Connectors

Automotive connectors may encounter:

  • Temperature cycling
  • Vibration
  • Humidity
  • Dust
  • Oil
  • Chemical exposure
  • Long service life requirements

Material selection should therefore consider the complete automotive environment.

For automotive connector products, FPIC applies IATF 16949 quality management requirements and supports production processes designed for demanding automotive applications.


23.Material Selection for Industrial Connectors

Industrial connectors may be exposed to:

  • Continuous vibration
  • Machinery movement
  • Oil
  • Dust
  • Chemicals
  • Outdoor environments

Industrial connector material selection should consider not only IP protection but also mechanical durability and chemical compatibility.

For example, an industrial connector used near motors may require different mechanical characteristics from one installed inside a protected control cabinet.


24.Material Selection for Medical Connectors

Medical applications may place additional requirements on:

  • Biocompatibility
  • Cleaning resistance
  • Chemical exposure
  • Sterilization
  • Reliability
  • Traceability

The material selection process should therefore begin with the applicable medical device requirements and cleaning or sterilization process.


25.Manufacturing Must Be Considered

A material with excellent laboratory performance may still be difficult to manufacture.

Engineers should evaluate:

  • Injection molding behavior
  • Shrinkage
  • Warpage
  • Flow characteristics
  • Terminal stamping
  • Plating process
  • Crimp compatibility
  • Assembly tolerances

Material selection should support not only prototype performance but also stable mass production.


Connector Material Selection Matrix

Component Common Materials Main Selection Factors
Housing PA, PBT, PPS, LCP, PEEK Temperature, insulation, strength, chemicals
Contact Brass, phosphor bronze, copper alloys Conductivity, spring force, fatigue
Plating Tin, gold, silver Corrosion, current, mating cycles
Seal Silicone, EPDM, fluoroelastomer Temperature, water, chemicals
Locking Parts Engineering plastics / metals Retention, vibration, durability
Shielding Copper alloys / metal shells EMC, grounding, mechanical strength

Common Connector Material Selection Mistakes

Mistake Potential Consequence
Selecting housing only by temperature rating Mechanical or dimensional problems
Treating all nylon grades as identical Unexpected moisture or thermal behavior
Selecting contact material only by conductivity Insufficient spring performance
Specifying gold plating without thickness Unclear contact durability
Ignoring underplating Corrosion or diffusion concerns
Selecting seals without chemical testing Swelling or degradation
Ignoring current-related heat generation Excessive temperature rise
Choosing materials without DFM review Molding or assembly problems
Selecting the highest-performance material automatically Unnecessary cost
Evaluating materials independently System-level compatibility problems

A Practical Connector Material Selection Workflow

Step 1: Define the Environment

Identify:

  • Temperature
  • Humidity
  • Water
  • Dust
  • Chemicals
  • Vibration
  • UV exposure

Step 2: Define Electrical Requirements

Identify:

  • Current
  • Voltage
  • Signal type
  • Contact resistance
  • Mating cycles

Step 3: Define Mechanical Requirements

Consider:

  • Contact force
  • Mating force
  • Retention
  • Shock
  • Vibration
  • Connector size

Step 4: Select Housing Material

Match:

Temperature + Insulation + Mechanical + Environmental Requirements

Step 5: Select Contact Alloy

Match:

Conductivity + Spring Properties + Fatigue + Formability

Step 6: Select Plating

Match:

Corrosion + Wear + Current + Signal + Mating Cycles

Step 7: Select Seal Material

Match:

Temperature + Fluids + Water + Chemical Exposure

Step 8: Validate the Complete Connector

Evaluate:

  • Electrical performance
  • Mechanical performance
  • Temperature rise
  • Environmental resistance
  • Mating cycles
  • Dimensional stability
  • Production consistency

Material Selection Should Follow Application Requirements

A common mistake is starting with a preferred material and trying to make it fit the application.

A better approach is:

Application → Requirements → Material Properties → Component Design → Validation

For example, if a connector operates in a high-temperature environment, engineers should not simply select the highest-temperature housing material.

They should first ask:

  • What is the actual temperature profile?
  • How much current flows through the contacts?
  • How long is the exposure?
  • Is vibration present?
  • Are chemicals present?
  • How many mating cycles are required?

The answers determine the appropriate material combination.


Why Material Compatibility Matters

A connector is a multi-material system.

Consider:

Housing + Contact Alloy + Plating + Seal + Cable + Mating Connector

Changing one material can influence another.

For example:

  • Housing shrinkage can affect terminal position.
  • Contact force can affect plating wear.
  • Seal hardness can affect mating force.
  • Temperature can affect housing dimensions.
  • Chemical exposure can affect both housing and seals.

This is why reliable connector development requires cross-functional material engineering.


How FPIC Supports Connector Material Selection

FPIC provides customized connector development and manufacturing solutions covering:

  • Connector housing materials
  • Contact materials
  • Contact plating
  • Sealing systems
  • Terminal stamping
  • Connector assembly
  • Electrical testing
  • Dimensional inspection
  • Reliability validation

FPIC’s automotive connector products are manufactured under IATF 16949 quality management requirements.

For automotive connector production, FPIC also supports mass-production cleanliness requirements aligned with VDA 19.1 / ISO 16232 practices.

Material and component selection can be evaluated together with connector geometry, tooling, assembly, and testing requirements.

This system-level approach helps OEM customers develop connectors that balance performance, reliability, manufacturability, and cost.


Final Thoughts

Connector material selection is not simply a question of choosing the strongest plastic, most conductive metal, or thickest plating.

The correct material combination depends on the complete application.

Engineers should evaluate:

Housing + Contact + Plating + Seal + Environment + Electrical Load + Mechanical Requirements

The best connector material is the one that provides the required performance throughout the expected service life while remaining manufacturable and commercially practical.

A structured selection process can help reduce:

  • Corrosion risk
  • Thermal problems
  • Mechanical failure
  • Seal degradation
  • Manufacturing variation
  • Lifecycle cost

Ultimately, successful connector design begins with understanding the application and selecting materials that work together as a complete system.


FAQ

What is the most important factor in connector material selection?

There is no single factor. Temperature, current, environment, mechanical loading, mating cycles, dimensional requirements, and manufacturing conditions should all be considered together.

Which material is commonly used for connector housings?

PA and PBT are widely used for many connector applications, while PPS, LCP, PEEK, and other engineering polymers may be considered for more demanding thermal, dimensional, or chemical requirements.

What materials are commonly used for connector contacts?

Brass, phosphor bronze, and other copper alloys are commonly used. The selection depends on conductivity, spring properties, contact force, fatigue resistance, and application requirements.

Is gold plating always better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact performance, but it can increase cost. Tin may be suitable for many power applications. The correct plating depends on current, signal type, environment, and mating requirements.

How should connector seal material be selected?

Seal material should be evaluated against the actual temperature range, water exposure, chemicals, oils, cleaning agents, and expected service life.

Does connector housing material affect electrical reliability?

Yes. Housing material affects insulation, terminal positioning, dimensional stability, heat resistance, and mechanical protection, all of which can influence connector reliability.

Why should material selection consider manufacturing?

A material may perform well technically but create molding, stamping, plating, assembly, or cost problems at production volume. DFM should therefore be included early in the material selection process.


Need Help Selecting Materials for Your Connector?

FPIC supports OEM and engineering teams with connector design and manufacturing from material selection and tooling through assembly, testing, and mass production.

Whether you need a compact fine-pitch connector, high-current connector, automotive connector, industrial connector, or customized interconnection solution, our engineering team can evaluate the complete material and application requirements.

Contact FPIC to discuss your connector development project.


Resources

  1. IEC
    https://www.iec.ch/
    International standards and technical resources covering electrical and electronic technologies.
  2. SAE International
    https://www.sae.org/
    Automotive engineering standards and technical resources.
  3. IPC
    https://www.ipc.org/
    Industry standards and resources for electronic interconnection and manufacturing.
  4. IATF Global Oversight
    https://www.iatfglobaloversight.org/
    Resources related to IATF 16949 automotive quality management requirements.
How Vibration Affects Automotive Connectors

An automotive connector can pass continuity, contact resistance, insulation, and mating checks during initial inspection and still develop an electrical failure after months or years of vehicle operation.

The reason is that initial testing evaluates the connection at a specific moment. Vehicle vibration, thermal expansion, harness movement, and repeated mechanical stress can gradually change the contact interface, terminal position, locking condition, and surrounding connection system.

Quick Answer:
An automotive connector can pass initial electrical testing but fail after long-term vibration because microscopic movement at the contact interface can cause plating wear, fretting corrosion, and higher contact resistance. Vibration can also affect terminal retention, connector locking, solder joints, and wire-harness strain, eventually causing intermittent or permanent electrical failure.

The key engineering question is therefore not simply:

“Does the connector work now?”

It is:

“Will the electrical interface remain stable after long-term mechanical and environmental stress?”

How Vibration Affects Automotive Connectors


Why Vibration Creates Long-Term Connector Failures

Automotive connectors operate in an environment that is very different from a stationary bench test.

Depending on their location in the vehicle, they may experience combinations of:

  • road-induced vibration;
  • drivetrain and motor vibration;
  • mechanical shock;
  • temperature cycling;
  • cable and harness movement;
  • assembly preload;
  • moisture and contamination;
  • repeated thermal expansion and contraction.

TE Connectivity describes connectors for demanding applications as needing to withstand mechanical stresses that include heavy vibration, while secure locking and positive contact retention are important characteristics for harsh-environment connections.

The critical issue is often not large visible movement of the complete connector.

Instead, very small relative movements may occur between the mating contact surfaces.

These movements can gradually change an interface that initially showed excellent electrical performance.

A simplified failure path is:

Vehicle Vibration → Contact Micro-Movement → Surface Wear → Fretting Corrosion → Contact Resistance Growth → Intermittent or Permanent Failure

Other mechanical paths may occur at the same time:

Vibration → Terminal Movement → Retention Loss

and:

Harness Movement → Connector Load → Housing and Locking Stress

This is why automotive connector vibration reliability must be evaluated as a system rather than as a single material property.

Quality Built Around Customer Requirements


How Contact Micro-Movement Leads to Fretting Corrosion

When male and female terminals mate, electrical current does not necessarily flow uniformly through the entire visible contact surface.

At microscopic scale, current passes through multiple contact points created by the pressure between the mating surfaces.

If vibration or thermal expansion causes repeated small relative movements, the contact surfaces may begin to wear.

This process can:

  1. disturb or remove part of the surface plating;
  2. generate metallic wear debris;
  3. expose material that can oxidize;
  4. reduce the quality of the effective conductive interface;
  5. increase contact resistance.

TE identifies fretting corrosion as a traditional failure mechanism in tin-plated connections and explains that relative movement caused by vibration and thermal expansion can occur between male and female contacts. Its Micro-MaTch design uses an additional positioning spring specifically to absorb this movement.

The important point is that the connector may still appear mechanically intact.

There may be:

  • no broken housing;
  • no visibly bent terminal;
  • no disconnected plug.

Yet electrical resistance at the microscopic contact interface may already be changing.

That is why long-term connector reliability cannot be judged only through visual inspection.


Why Increasing Contact Resistance Matters

A gradual increase in contact resistance can create several consequences.

Voltage Drop

More resistance at the interface increases voltage drop across the connection.

For low-voltage automotive circuits, even relatively small changes may affect sensitive electronics, sensors, control modules, or signal references.

Local Heating

Electrical resistance also creates heat when current flows.

This links vibration reliability directly to thermal reliability.

Vibration itself does not necessarily create significant electrical heat. The thermal risk develops when vibration changes the contact condition and causes resistance to rise.

In higher-current circuits, this can become increasingly important because resistive power loss grows rapidly as current increases.

Intermittent Electrical Signals

Micro-movement can also create temporary changes in contact continuity.

A connector may therefore show:

  • intermittent signal loss;
  • sporadic control faults;
  • communication errors;
  • unstable sensor readings.

These failures can be difficult to diagnose because the connection may work normally when the vehicle is stationary or when the connector is inspected in the workshop.

IEC 60512-2-3 defines a method for determining contact resistance variation under specified dynamic conditions, while IEC 60512-2-5 addresses detection of contact disturbance under dynamic conditions.

This illustrates an important difference between measuring static contact resistance and verifying whether that resistance remains stable during mechanical stress.


Contact Force Must Remain Stable Under Vibration

Contact normal force is one of the key variables that controls the electrical interface.

The female terminal normally incorporates a spring structure that presses against the mating male contact.

That force must be sufficient to maintain a stable conductive interface.

If contact pressure is too low, the system may become more sensitive to:

  • vibration;
  • surface contamination;
  • oxidation;
  • fretting;
  • resistance variation.

However, simply maximizing contact force is not the solution.

Excessive contact load can create other problems, including:

  • higher mating force;
  • accelerated plating wear;
  • greater terminal stress;
  • housing deformation;
  • reduced mating-cycle life.

Molex notes that insufficient pressure increases contact resistance and vulnerability to fretting corrosion and signal dropouts under vibration, while excessive contact load may accelerate plating wear or overstress connector components.

The engineering target is therefore:

Stable Contact Force + Controlled Mating Force + Long-Term Electrical Reliability

This is particularly important in multi-contact automotive connectors where the operating force of many individual terminals combines into the total connector mating force.


Mating Force and Contact Force Are Not the Same

These terms are sometimes treated as interchangeable, but they describe different aspects of connector performance.

Contact normal force is the mechanical pressure acting at the electrical contact interface.

Connector mating force is the total force required to engage the complete connector.

Total mating force can include contributions from:

  • terminal spring force;
  • contact friction;
  • seals;
  • housing alignment;
  • locking structures;
  • multiple simultaneously engaging terminals.

A connector may therefore be optimized for lower operating effort while still maintaining sufficient contact pressure.

The objective is not simply to make a connector “tight.”

The objective is to create a predictable mechanical interface that maintains stable electrical contact over the intended service life.


Terminal Retention Is a Separate Reliability Requirement

Contact force controls the interface between mating conductive surfaces.

Terminal retention performs a different job.

It keeps the terminal correctly positioned inside the connector housing.

This distinction is important because an electrically good contact cannot remain reliable if the terminal begins to move backward inside the housing.

Under vibration or wire-harness load, insufficient retention may result in:

  • terminal back-out;
  • reduced mating depth;
  • partial contact engagement;
  • intermittent continuity;
  • complete circuit interruption.

Molex describes contact retention as the mechanical means used to keep connector elements secured so electrical continuity can be maintained under stresses such as vibration and thermal cycling.

Design Factor Primary Function
Contact normal force Maintains the conductive contact interface
Terminal retention Keeps the terminal correctly seated in the housing
Connector locking Keeps plug and receptacle fully mated

A robust automotive connector must control all three.


How TPA and CPA Improve Connector Security

Automotive connectors frequently use additional locking or assurance structures.

A primary terminal lock normally retains the contact inside the housing, while secondary systems can provide additional security.

Two terms commonly used in automotive connector design are:

TPA — Terminal Position Assurance

TPA helps verify and secure the correct position of terminals inside the connector housing.

Its purpose is to reduce the risk of a terminal being incompletely inserted or moving out of its intended position.

CPA — Connector Position Assurance

CPA helps confirm and secure the mated condition of the connector itself.

Its purpose is different from terminal retention: it acts at the plug-to-receptacle connection level.

FPIC’s automotive connector technical materials distinguish CPA as a connector-position assurance structure and TPA as a terminal-position assurance structure.

These secondary structures are particularly valuable where vibration, harness loads, difficult assembly access, or safety requirements make incomplete engagement unacceptable.


Housing and Locking Design Matter Under Vibration

An automotive connector housing is not simply a plastic shell.

It performs several mechanical functions simultaneously:

  • terminal positioning;
  • mating guidance;
  • polarization;
  • retention;
  • connector locking;
  • protection against mismating;
  • environmental sealing where required.

A well-designed terminal cannot provide reliable service if the housing allows excessive relative movement or the connector lock disengages under vibration.

For harsh environments, TE highlights secure locking and positive contact-retention systems as important characteristics of rugged connectors.

Engineers should therefore evaluate:

  • primary latch geometry;
  • secondary locking;
  • CPA design where required;
  • housing stiffness;
  • material creep and stress relaxation;
  • connector-to-device mounting;
  • seal compression;
  • tolerance accumulation;
  • mating alignment.

The complete locking architecture must remain stable throughout the expected mechanical and environmental lifecycle.


Harness Strain Can Amplify Connector Stress

The connector does not operate independently from the wire harness.

This is especially important in automotive applications.

A wire harness can introduce mechanical forces through:

  • cable weight;
  • routing tension;
  • tight bending;
  • engine or vehicle movement;
  • incorrect clip spacing;
  • assembly preload;
  • unsupported cable length;
  • vibration transmitted along the conductors.

If the harness is not properly supported, these forces can reach the rear of the connector and eventually affect the terminals.

A simplified mechanical path is:

Harness Movement → Cable Load → Terminal Stress → Contact Micro-Movement

For this reason, automotive connection reliability should consider the complete relationship between:

  • connector;
  • terminal;
  • conductor;
  • seal;
  • strain relief;
  • harness clips;
  • cable exit direction;
  • equipment mounting.

Cable Exit Direction

A harness that leaves the connector at an unsuitable angle can continuously load the terminal or housing.

Bend Radius

Forcing the cable into a very tight bend near the connector can introduce long-term mechanical stress.

Harness Fixing Points

Correctly positioned clips or supports reduce the amount of cable movement transferred to the connector.

Conductor Size

Larger conductors have greater stiffness and can transmit more mechanical force to the connection.

This is one reason why connector and wire-harness engineering should be considered together rather than purchased as completely independent components.


PCB Headers Have Additional Vibration Risks

Automotive PCB connectors require another level of analysis.

For a wire-to-wire connector, engineers primarily consider:

Harness → Terminal → Contact → Housing → Connector Lock

A PCB header adds another chain:

Receptacle → Header Contact → PCB Pin → Solder Joint → PCB

This introduces additional potential vibration interfaces.

Pin Position and Alignment

Poor pin positioning can create mechanical preload during mating or soldering.

Solder-Joint Stress

Vibration transmitted through the connector body can eventually reach the solder joints.

PCB Movement

The printed circuit board itself can flex under vibration.

Housing Retention

The header housing must remain mechanically stable relative to the PCB.

Harness Leverage

A harness attached to the mating receptacle may create bending or leverage forces on the header.

This is particularly important in control modules, lighting systems, power-seat electronics, window-control modules, multimedia systems, and other vehicle electronics.

For an automotive PCB connector, vibration reliability is a system property rather than a terminal-only property.

FPIC’s internal automotive connector materials define header connectors as structures containing fixed male contacts that normally connect to the PCB or directly to internal equipment circuits.

This is why PCB-header validation should consider both contact reliability and board-level mechanical integrity.


Terminal Material Influences Vibration Performance

Automotive terminal material selection requires a balance between electrical and mechanical properties.

Important characteristics include:

  • electrical conductivity;
  • spring strength;
  • yield behavior;
  • fatigue resistance;
  • formability;
  • stress-relaxation resistance;
  • corrosion behavior.

Typical connector contact materials include different copper alloys selected according to application requirements.

A highly conductive material alone may not be sufficient if it cannot maintain the required spring behavior after repeated mechanical and thermal stress.

Conversely, a highly elastic material may introduce unnecessary electrical resistance or cost if used without considering current and signal requirements.

The terminal geometry, material, heat treatment, contact pressure, and plating system should therefore be developed together.


Plating Selection Affects Fretting Resistance

Contact plating influences:

  • resistance;
  • wear;
  • oxidation;
  • corrosion;
  • friction;
  • mating durability.

Gold and tin are widely used in connector systems, but they behave differently.

Molex recommends carefully matching contact finishes and notes that tin-to-tin systems require validation for fretting corrosion, oxidation, and related long-term effects, while mismatched gold-to-tin interfaces can introduce additional reliability risk.

This does not mean that one plating material is universally better.

The appropriate system depends on:

  • signal or power level;
  • contact force;
  • environment;
  • mating-cycle requirement;
  • temperature;
  • vibration;
  • cost;
  • customer specification.

The important principle is:

Plating should be selected as part of the contact system, not as an isolated specification.


Why Initial Electrical Testing Is Not Enough

Initial testing is essential.

But it answers only part of the reliability question.

Initial tests can verify:

  • continuity;
  • contact resistance;
  • insulation resistance;
  • withstand voltage;
  • pin position;
  • dimensional conformity.

These measurements answer:

“Does the connector meet requirements now?”

Reliability testing asks a different question:

“Will the connector still meet those requirements after mechanical and environmental stress?”

That distinction is fundamental.

A connector may initially have:

  • correct contact force;
  • low resistance;
  • proper terminal seating;
  • correct housing lock.

Long-term vibration can gradually change one or more of these conditions.

Therefore, a robust validation program should compare electrical and mechanical performance before and after stress, and in some cases monitor electrical continuity while the stress is being applied.


How Vibration Testing Should Be Evaluated

A vibration test should not be treated simply as:

Run the machine for a specified number of hours and check whether the connector broke.

A useful validation plan defines what must be measured before, during, and after the test.

Before Vibration Testing

Typical checks may include:

  • visual inspection;
  • terminal position;
  • locking condition;
  • contact resistance;
  • continuity;
  • mating condition;
  • dimensional checks where necessary.

During Vibration Testing

Depending on the specification, the test may monitor:

  • transient discontinuity;
  • contact disturbance;
  • resistance variation;
  • connector movement.

IEC 60512-6-5 defines a method intended to assess the ability of components to withstand specified levels of random vibration.

IEC 60512-2-3 covers contact-resistance variation under dynamic conditions, while IEC 60512-2-5 addresses contact disturbance.

The exact test severity, mounting arrangement, frequency range, acceleration, duration, monitoring requirements, and acceptance limits must follow the applicable product specification or customer requirement.

After Vibration Testing

The connector should be evaluated again for possible changes such as:

  • increased contact resistance;
  • terminal back-out;
  • housing damage;
  • lock deterioration;
  • contact wear;
  • seal displacement;
  • wire or crimp damage;
  • solder-joint damage in PCB applications.

The engineering value comes from comparing the connector condition before and after exposure.

Vibration and Thermal Cycling Should Be Considered Together

Vehicles do not experience vibration in isolation.

Temperature also changes during operation.

Different materials expand and contract at different rates, including:

  • copper-alloy terminals;
  • plastic housings;
  • PCB laminates;
  • seals;
  • wire insulation;
  • connector plating.

Repeated temperature changes can therefore create additional relative movement between contact surfaces.

TE specifically identifies vibration and thermal expansion as sources of relative contact movement associated with fretting-corrosion risk.

This interaction explains why a connector that performs acceptably in a short room-temperature mechanical test may require broader environmental validation for automotive use.

Depending on the application, a reliability plan may therefore combine:

  • vibration;
  • thermal cycling;
  • thermal shock;
  • humidity;
  • salt spray;
  • electrical measurements.

Crimp Quality Also Influences Vibration Reliability

For wire-to-connector applications, the crimp is another critical mechanical and electrical interface.

A properly controlled crimp should provide a stable connection between the conductor and terminal.

Important controls can include:

  • conductor crimp height;
  • crimp width;
  • conductor position;
  • insulation support;
  • bellmouth condition;
  • strand integrity;
  • pull force;
  • crimp cross-section.

An excessively loose crimp may allow conductor movement.

An excessively tight crimp can damage strands or weaken the conductor.

Either condition may reduce the connection’s ability to tolerate vibration.

FPIC’s internal crimping standards include controls for conductor crimp height, insulation crimping, conductor position, pull-force testing, and cross-section analysis.

This reinforces an important reliability principle:

The terminal contact and the wire termination must both remain mechanically stable.


A Practical Automotive Connector Reliability Checklist

Before selecting or developing an automotive connector, engineers should define the complete operating environment.

Design Area Questions to Confirm
Electrical circuit Signal, low-current power, or higher-current circuit?
Contact system What normal force and contact geometry are required?
Terminal material Does it balance conductivity and spring performance?
Plating Is it suitable for vibration, wear, environment, and lifecycle?
Terminal retention How is terminal back-out prevented?
Connector locking Is primary or secondary locking required?
PCB interface Is it wire-to-wire, wire-to-board, or PCB header?
Harness What conductor size, cable weight, and exit direction apply?
Strain relief How is harness movement isolated from the terminals?
Environment What vibration, temperature, moisture, and contamination occur?
Testing What electrical measurements are required before and after vibration?
Production How are terminal position, crimping, assembly, and traceability controlled?

A complete specification helps prevent the common mistake of evaluating vibration resistance as a single connector feature.


How FPIC Supports Automotive Connector Reliability

FPIC supports customized automotive low-voltage connectors, automotive PCB headers and receptacles, terminals, stamped components, and related cable assemblies.

Our automotive connector development and manufacturing capabilities cover multiple stages of the connection system.

Contact and Terminal Development

FPIC supports terminal structure, material, plating, retention, and manufacturing evaluation according to the application requirements.

Housing and Locking Development

Connector housing, keying, terminal retention, mating alignment, and locking structures can be evaluated during custom product development.

Automotive PCB Headers

FPIC develops customized board-side automotive connector solutions for vehicle electronic modules, including applications such as lighting control, power seats, window-lift systems, multimedia, and related control electronics.

Wire Harness Integration

Where the project requires a complete connection assembly, connector, terminal, conductor, crimping, strain relief, and harness routing requirements can be evaluated together.

In-House Manufacturing Processes

FPIC’s manufacturing platform includes:

  • precision stamping;
  • plastic injection molding;
  • insert molding;
  • tooling development;
  • automated connector assembly;
  • wire processing;
  • cable assembly;
  • CCD-supported inspection.

Reliability Testing

FPIC’s internal laboratory capability includes equipment for:

  • contact impedance testing;
  • insertion and extraction force testing;
  • temperature-rise testing;
  • vibration testing;
  • thermal shock;
  • withstand voltage;
  • insulation testing;
  • dimensional measurement;
  • X-ray inspection.

FPIC’s technical materials also identify automotive connector validation areas including contact resistance, temperature rise, mating force, terminal retention, vibration, high- and low-temperature exposure, temperature/humidity cycling, solder-heat resistance, and salt spray.

Company capability materials list vibration equipment, contact-impedance testers, temperature-rise testers, insertion/extraction-force equipment, thermal-shock chambers, X-ray systems, and dimensional inspection equipment.

For automotive projects, FPIC operates under IATF 16949 and supports product-development and manufacturing controls appropriate to customized automotive connector programs.

The objective is not merely to manufacture a connector that passes an initial continuity check.

It is to establish a controlled development and production process that supports stable connection performance through the intended operating environment.


Frequently Asked Questions

1. Why can an automotive connector pass continuity testing but fail under vibration?

Initial continuity testing confirms that the electrical path is complete at the time of measurement. Long-term vibration can create microscopic contact movement, plating wear, fretting corrosion, terminal movement, or locking stress that gradually changes the connection and may eventually cause intermittent or permanent failure.

2. What is fretting corrosion in an automotive connector?

Fretting corrosion is degradation that occurs when loaded mating surfaces experience very small repeated relative movements. In electrical contacts, this movement can disturb plating, generate wear debris and oxidation products, and increase contact resistance.

3. How does vibration increase connector contact resistance?

Vibration can create repeated micro-movement at the contact interface. Over time, this may wear the contact surface, change the effective conductive contact area, and promote oxidation or fretting debris, causing resistance to increase.

4. What prevents an automotive terminal from backing out?

Terminal retention normally depends on the primary terminal-locking structure, correct terminal insertion, and, in many automotive systems, a secondary Terminal Position Assurance (TPA) feature.

5. What is the difference between TPA and CPA?

TPA helps secure and verify terminal position inside the connector housing. CPA helps secure and verify the fully mated position of the plug and receptacle.

6. Does higher contact force always improve vibration reliability?

No. Insufficient force can increase resistance and micro-movement risk, but excessive contact force may increase mating effort, wear, and spring stress. The contact system should be optimized for stable force throughout the required service life.

7. Why does the wire harness affect connector vibration reliability?

The harness can transfer cable weight, bending force, and vibration into the connector. Improper routing, insufficient strain relief, or unsuitable fixing points can increase load on the terminal and contact interface.

8. Are automotive PCB headers affected by vibration differently from wire-to-wire connectors?

Yes. PCB headers introduce additional interfaces such as header pins, solder joints, PCB movement, and board mounting. Their vibration reliability must therefore be evaluated at both the contact and PCB levels.


Conclusion

Automotive connector reliability cannot be judged only by whether a new connector passes an initial electrical test.

Long-term vibration can affect several parts of the connection system:

Contact Interface → Terminal Retention → Housing Locking → PCB Interface → Wire Harness

Microscopic contact movement can lead to fretting corrosion and resistance growth. Terminal movement can reduce mating depth. Harness strain can transfer mechanical loads into the connector. PCB headers introduce additional solder-joint and board-level stresses.

For this reason, reliable automotive connection design requires electrical, mechanical, material, harness, and validation requirements to be considered together.

FPIC supports automotive connector projects from terminal and housing development through PCB-header design, cable integration, tooling, manufacturing, testing, and repeat production.


Discuss Your Automotive Connector Project

Developing a customized automotive connector, PCB header, terminal, or related cable assembly?

Send FPIC your 2D or 3D drawings, electrical requirements, mating interface, wire specification, operating environment, validation requirements, and forecast demand for engineering evaluation.

Email: info@fpiconn.com


Resources

  • TE Connectivity — Micro-MaTch Miniature Ribbon Cable Connectors and Fretting Corrosion Resistance.
  • TE Connectivity — Rugged Connectors for Harsh Conditions.
  • Molex — Engineering Contact Engagement and Normal Force for Connector Performance.
  • Molex — Connector Contact Retention Guide.
  • Molex — Gold or Tin vs. Gold and Tin Contact Finishes.
  • IEC 60512-2-1 — Contact Resistance — Millivolt Level Method.
  • IEC 60512-2-3 — Contact Resistance Variation Under Dynamic Conditions.
  • IEC 60512-2-5 — Contact Disturbance Under Dynamic Conditions.
  • IEC 60512-6-5 — Random Vibration Test Method.
Connector Miniaturizationfor Modern Electronics

Modern electronic systems are becoming smaller, lighter, and more integrated.

Devices that once had plenty of internal space now need to accommodate more functions within increasingly compact packages.

This trend has created strong demand for smaller and higher-density connectors.

However, making a connector smaller is not simply a matter of reducing the housing dimensions.

As connector size decreases, the available space for contacts, insulation, mechanical structures, sealing, and assembly also becomes smaller.

At the same time, electrical and mechanical requirements often remain the same—or become more demanding.

Connector miniaturization therefore requires a careful balance between:

Size + Electrical Performance + Mechanical Reliability + Manufacturability

For applications such as automotive electronics, industrial automation, medical equipment, consumer electronics, robotics, and compact control systems, successful miniaturization requires engineering optimization at every stage.

Connector Miniaturizationfor Modern Electronics


What Is Connector Miniaturization?

Connector miniaturization refers to reducing the physical size, pitch, height, or overall footprint of a connector while maintaining its required functional performance.

Miniaturization may involve:

  • Smaller housing dimensions
  • Reduced contact pitch
  • Smaller terminals
  • Lower connector height
  • Higher contact density
  • Reduced mounting footprint

The goal is usually to achieve:

More electrical functionality in less physical space.

However, reducing dimensions can create new engineering constraints.


Why Are Connectors Becoming Smaller?

Several market trends are driving connector miniaturization.

Smaller Electronic Devices

Electronic products increasingly require:

  • Compact control units
  • Smaller sensors
  • Reduced PCB size
  • Higher functional density

Connectors must fit within these increasingly constrained spaces.


Higher Functional Integration

A single electronic module may now integrate:

  • Power
  • Data
  • Sensors
  • Control signals
  • Communication interfaces

This increases the number of electrical connections required within the same physical space.


Weight Reduction

In automotive and portable equipment, reducing component size can also contribute to overall weight reduction.

Smaller connectors can help optimize:

  • Wiring space
  • Module dimensions
  • Packaging
  • System weight

1.Contact Pitch Becomes More Challenging

One of the biggest challenges in connector miniaturization is reducing contact pitch.

As the distance between contacts decreases, engineers must maintain sufficient:

  • Electrical isolation
  • Mechanical strength
  • Positioning accuracy
  • Insulation performance

A smaller pitch leaves less room for dimensional variation.

This makes:

Terminal Position + Housing Accuracy + Manufacturing Tolerance

increasingly important.


2.Electrical Clearance Becomes More Limited

When contacts are positioned closer together, the available electrical spacing decreases.

Engineers need to evaluate:

  • Clearance
  • Creepage
  • Insulation thickness
  • Working voltage
  • Pollution environment

For higher-voltage applications, simply reducing contact spacing may not be possible without changing the connector architecture.

This creates a fundamental design challenge:

How can the connector become smaller without compromising electrical safety?


3.Current Density Can Increase

Miniaturization can also increase current density.

If the same current must pass through a smaller terminal, the available conductive cross-section may decrease.

This can increase:

  • Current density
  • Joule heating
  • Contact temperature
  • Thermal stress

The design must therefore balance:

Contact Size + Material Conductivity + Contact Resistance + Current Rating

A smaller connector is not automatically suitable for the same current level as a larger connector.


4.Thermal Management Becomes More Difficult

Heat generated at a connector contact must be transferred away from the contact interface.

When connector dimensions decrease:

  • Thermal paths may become smaller
  • Contact spacing may decrease
  • Heat concentration can increase
  • Cooling space may be reduced

This can become particularly important in:

  • High-current applications
  • Compact automotive modules
  • Industrial control systems
  • Power electronics

Thermal design should therefore be considered alongside electrical design.


5.Contact Spring Design Becomes More Sensitive

Smaller terminals have less physical space for spring structures.

However, the contact still needs sufficient force to maintain reliable electrical connection.

The challenge becomes:

Small Contact + Controlled Spring Force + Long-Term Reliability

If spring force is too low:

  • Contact resistance may increase
  • Vibration resistance may decrease
  • Intermittent connections may occur

If spring force is too high:

  • Mating force increases
  • Contact wear may accelerate
  • Mating cycle life may decrease

Miniaturization therefore requires highly controlled contact geometry.


6.Mechanical Strength Can Be Reduced

Reducing terminal and housing dimensions can reduce structural strength.

Miniature connectors may be more sensitive to:

  • Insertion force
  • Extraction force
  • Cable pulling
  • Side loading
  • Vibration
  • Shock

The housing must therefore maintain sufficient:

  • Retention strength
  • Locking performance
  • Terminal support
  • Mechanical stability

Miniaturization should never compromise the mechanical integrity of the connector.


7.Manufacturing Tolerances Become More Critical

As components become smaller, the same absolute dimensional variation represents a larger percentage of the total geometry.

For example, a small terminal-position variation may have little effect in a large connector but become significant in a fine-pitch connector.

Critical areas include:

  • Terminal pitch
  • Terminal position
  • Housing cavities
  • Locking features
  • Contact geometry
  • Seal interfaces

This makes precision manufacturing and tolerance control increasingly important.


8.Assembly Becomes More Difficult

Smaller connector components can be more challenging to assemble.

Potential problems include:

  • Terminal misalignment
  • Incomplete terminal insertion
  • Seal damage
  • Housing deformation
  • Locking errors

Manual assembly becomes more difficult as component size decreases.

For high-volume production, manufacturers may need:

  • Precision assembly fixtures
  • Automated insertion
  • Vision inspection
  • Automated electrical testing

9.Inspection Becomes More Challenging

Miniaturized features may be difficult to inspect using conventional measurement methods.

Traditional tools may not provide sufficient resolution or repeatability.

Manufacturers may therefore use:

  • Optical inspection
  • CCD systems
  • Microscopic inspection
  • Coordinate measurement
  • Automated dimensional analysis

Inspection strategies must be designed around the actual critical features of the connector.


10.Miniaturization Can Affect Mating Reliability

Smaller connectors may have less mechanical tolerance for misalignment.

During mating, even a small angular or positional deviation can influence:

  • Insertion force
  • Terminal engagement
  • Contact wipe
  • Housing alignment

Good guiding features become increasingly important.

Common design solutions include:

  • Polarization keys
  • Guide posts
  • Chamfered mating surfaces
  • Self-alignment structures

These features help reduce the risk of incorrect or incomplete mating.


11.Sealing Becomes More Difficult

For miniature waterproof connectors, the available space for seals is limited.

Yet the connector may still need to achieve:

  • IP67
  • IP68
  • Other application-specific sealing requirements

Engineers must optimize:

  • Seal geometry
  • Compression
  • Housing interfaces
  • Cable diameter
  • Material selection

Reducing the connector size without compromising sealing performance can be challenging.


12.Miniaturization and Mating Cycles

A smaller connector does not necessarily have a shorter mating life, but reducing contact dimensions can make wear management more difficult.

Each mating cycle may affect:

  • Contact plating
  • Spring structure
  • Contact surface
  • Housing alignment

For applications requiring frequent connection and disconnection, engineers should validate:

  • Insertion force
  • Extraction force
  • Contact resistance
  • Wear
  • Mating cycle performance

13.Material Selection Becomes More Important

Material selection can become more critical as connector dimensions decrease.

The housing material must provide appropriate:

  • Mechanical strength
  • Dimensional stability
  • Temperature resistance
  • Electrical insulation

Contact materials must provide:

  • Conductivity
  • Elasticity
  • Fatigue resistance
  • Corrosion resistance

For miniature connectors, small changes in material performance can have a noticeable impact on the overall system.


14.Miniaturization Requires Better Thermal and Electrical Simulation

For advanced connector designs, simulation can help evaluate potential problems before tooling.

Depending on the application, engineers may evaluate:

Electrical

  • Current density
  • Voltage distribution
  • Contact resistance

Thermal

  • Temperature rise
  • Heat concentration
  • Thermal paths

Mechanical

  • Contact deformation
  • Stress distribution
  • Mating force

Simulation does not replace physical testing, but it can help identify design risks earlier.


Miniaturization Trade-Offs

Connector miniaturization is fundamentally an optimization problem.

Design Goal Potential Challenge
Smaller housing Less internal space
Higher contact density Reduced spacing
Higher current Greater heat generation
Lower mating force Potentially lower contact force
Smaller terminals Reduced mechanical strength
Smaller seals More difficult sealing
Tight tolerances Higher manufacturing cost
More features More complex assembly

The objective is not simply:

Make It Smaller.

The objective is:

Make It Smaller Without Losing Performance.


Application Considerations

Different applications have different miniaturization priorities.

Application Key Miniaturization Challenge
Automotive Electronics Space, vibration, temperature
Medical Equipment Compactness, reliability, cleanliness
Industrial Automation Density, mechanical durability
Robotics Size, movement, mating cycles
Consumer Electronics Space and high-density interconnection
Sensors Compact size and environmental protection
Control Modules Density, thermal management, assembly

How to Approach Miniature Connector Design

A successful miniature connector development process should include:

Step 1: Define the Application

Identify:

  • Voltage
  • Current
  • Signal type
  • Temperature
  • Vibration
  • Mating cycles
  • Environmental exposure

Step 2: Establish the Size Target

Define:

  • Maximum housing dimensions
  • Contact pitch
  • Mounting footprint
  • Connector height

Step 3: Design the Contact System

Optimize:

  • Contact geometry
  • Spring force
  • Contact material
  • Plating
  • Current capacity

Step 4: Analyze Thermal and Electrical Performance

Evaluate:

  • Contact resistance
  • Temperature rise
  • Current density
  • Clearance
  • Creepage

Step 5: Perform Tolerance Analysis

Review:

  • Terminal position
  • Housing dimensions
  • Mating alignment
  • Locking features
  • Seal interfaces

Step 6: Validate Through Testing

Typical validation can include:

  • Contact resistance
  • Temperature rise
  • Insertion/extraction force
  • Mating cycles
  • Vibration
  • Thermal cycling
  • Environmental testing

Common Connector Miniaturization Mistakes

Mistake Potential Result
Reducing size without thermal analysis Excessive temperature rise
Reducing contact pitch excessively Electrical clearance problems
Undersized terminal Higher current density
Insufficient spring force Unstable contact
Excessive spring force High mating force
Ignoring tolerance stack-up Mating problems
Weak housing structure Mechanical failure
Poor seal design Water or dust ingress
Insufficient inspection Manufacturing variation

How FPIC Supports Connector Miniaturization

FPIC supports customized connector development with engineering capabilities covering:

✔ Contact system design

✔ Housing design

✔ Terminal stamping

✔ Precision injection molding

✔ Tolerance control

✔ Electrical testing

✔ Mechanical reliability testing

✔ CCD/visual inspection

✔ Automated assembly and packaging

For demanding automotive applications, FPIC’s connector manufacturing capabilities are supported by IATF 16949 quality management requirements.

Connector production can also incorporate controlled cleanliness practices aligned with VDA 19.1 / ISO 16232 requirements where applicable.

The engineering objective is to optimize connector size without sacrificing:

  • Electrical performance
  • Mechanical reliability
  • Manufacturing consistency
  • Service life

Final Thoughts

Connector miniaturization is one of the most important trends in modern electronics.

But reducing connector dimensions creates a chain of engineering challenges.

Smaller connectors require careful control of:

Contact Density + Electrical Clearance + Thermal Performance + Spring Force + Mechanical Strength + Manufacturing Tolerance

The best miniature connector is not simply the smallest possible connector.

It is the smallest connector that can reliably meet its electrical, mechanical, environmental, manufacturing, and lifecycle requirements.

Successful miniaturization therefore requires a system-level approach:

Define → Design → Simulate → Manufacture → Test → Validate

When size reduction is combined with disciplined engineering and manufacturing control, miniature connectors can deliver high-density performance without compromising reliability.


FAQ

What is connector miniaturization?

Connector miniaturization is the process of reducing connector size, contact pitch, height, or mounting footprint while maintaining required electrical and mechanical performance.

What is the biggest challenge in miniature connector design?

There is no single challenge. Contact density, electrical clearance, thermal management, mechanical strength, manufacturing tolerance, and assembly precision often become more difficult simultaneously.

Does a smaller connector support less current?

Not necessarily, but reducing terminal size and conductive area can increase current density and heat generation. Current capability must be evaluated based on the complete contact design and application conditions.

Why are manufacturing tolerances important for miniature connectors?

As connector features become smaller, the same dimensional variation can have a greater functional impact, especially on terminal alignment, mating, and contact performance.

How can miniature connectors maintain reliability?

Reliable miniature connectors require optimized contact geometry, suitable materials and plating, controlled tolerances, appropriate thermal design, precise manufacturing, and application-specific validation.


Need a Compact Connector for a Space-Constrained Application?

FPIC supports custom connector development from contact design and tooling through precision manufacturing, testing, and mass production.

Whether you need compact signal connectors, circular connectors, automotive connectors, or customized high-density solutions, our engineering team can help balance size, performance, reliability, and manufacturability.

Contact FPIC to discuss your miniature connector requirements.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    International testing framework for electrical and mechanical performance of connectors.
  2. USCAR Standards
    https://www.uscar.org/
    Automotive connector performance and validation resources.
  3. IPC Standards
    https://www.ipc.org/
    Industry standards and technical resources for electronic interconnection and manufacturing.
  4. IATF 16949
    https://www.iatfglobaloversight.org/
    Automotive quality management requirements for organizations in the automotive supply chain.
Connector Tolerance Control in Mass Production

A connector can meet its nominal drawing dimensions and still create problems during mass production if dimensional tolerances are not properly controlled.

Connector performance depends on multiple components working together:

  • Housing
  • Terminals
  • Seals
  • Locks
  • Contact interfaces
  • Mating features

Each component has its own dimensional variation.

When these variations accumulate, the final assembly can behave differently from the nominal design.

This is why tolerance control is not simply a drawing requirement.

It is a critical part of connector manufacturing quality.

Poor tolerance control can result in:

  • Difficult mating
  • Excessive insertion force
  • Loose connections
  • Contact instability
  • Seal leakage
  • Assembly interference
  • Poor interchangeability
  • Increased production scrap

For automotive, industrial, medical, energy storage, and other demanding applications, controlling dimensional variation from design through mass production is essential for consistent field performance.

Connector Tolerance Control in Mass Production


What Is Connector Tolerance Control?

Tolerance control defines the acceptable dimensional variation of connector components and ensures that manufacturing processes remain within those limits.

Typical controlled dimensions include:

  • Terminal position
  • Contact pitch
  • Housing dimensions
  • Locking features
  • Connector alignment
  • Seal compression
  • Mounting dimensions
  • Mating interfaces

For example, a connector may have a nominal terminal position specified on the drawing.

During manufacturing, the actual position will naturally vary within a defined tolerance.

The engineering challenge is ensuring that this variation does not negatively affect:

Mating + Electrical Contact + Mechanical Retention + Sealing


Why Nominal Dimensions Are Not Enough

One common mistake is designing around nominal dimensions without considering actual manufacturing variation.

Suppose two mating connector components each have dimensional tolerances.

Even if both are individually within specification, their combined variation may produce:

  • Excessive interference
  • Excessive clearance
  • Misalignment
  • Increased insertion force

This is known as tolerance stack-up.

Mass production makes this issue especially important because thousands or millions of parts may be produced.

A small dimensional issue that occurs only occasionally can become a significant quality problem at production scale.


1.Tolerance Stack-Up Can Affect Mating Performance

Connector mating requires several features to align correctly.

For example:

Housing → Guide Feature → Terminal → Contact Interface

Each feature contributes to the final position.

If multiple tolerances shift in the same direction, the accumulated variation can become significant.

Potential consequences include:

  • Difficult mating
  • Excessive insertion force
  • Connector misalignment
  • Terminal deformation
  • Housing interference

Engineers should therefore evaluate tolerance stack-up during the design phase.


2.Terminal Position Tolerance Is Critical

Terminal position directly affects electrical and mechanical performance.

If terminals are not positioned consistently:

  • Contact alignment may change
  • Mating force may vary
  • Contact wipe may become inconsistent
  • Adjacent terminals may have reduced clearance

This becomes particularly important for:

  • High-density connectors
  • Fine-pitch connectors
  • Multi-pin automotive connectors
  • Signal connectors

Precise terminal positioning helps maintain consistent contact behavior across production lots.


3.Housing Tolerance Affects Alignment

The connector housing provides the mechanical framework for the terminal system.

Important dimensions can include:

  • Terminal cavities
  • Guide rails
  • Keying features
  • Locking structures
  • Mating interfaces
  • Mounting holes

If housing dimensions vary excessively, the terminal system may not remain in the intended position.

This can affect:

  • Mating accuracy
  • Contact alignment
  • Connector retention
  • Assembly consistency

4.Contact Tolerance Affects Electrical Reliability

Electrical performance depends on stable contact geometry.

Small dimensional changes can influence:

  • Contact force
  • Contact area
  • Contact wipe
  • Contact resistance

For example, if a terminal beam is slightly outside its intended geometry, the resulting spring force may differ from the design target.

This can create variation in electrical performance between individual connectors.

Therefore:

Dimensional Control → Contact Geometry → Contact Force → Electrical Reliability


5.Seal Tolerance Affects Waterproofing

For sealed connectors, dimensional tolerance becomes even more important.

Sealing performance depends on controlled compression between:

  • Seal
  • Housing
  • Cable
  • Mating connector

Insufficient compression may cause leakage.

Excessive compression may cause:

  • High insertion force
  • Seal deformation
  • Assembly difficulty
  • Premature seal wear

Proper tolerance analysis helps ensure that the sealing system remains within its intended operating range.

This is especially important for:

  • Automotive connectors
  • Outdoor equipment
  • Industrial machinery
  • Agricultural equipment
  • IP67/IP68 applications

6.Locking Features Require Consistent Tolerances

Connector locks need to provide reliable retention while remaining practical for assembly and service.

If the locking geometry is inconsistent:

Too Tight

The operator may experience:

  • Difficult locking
  • High assembly force
  • Component deformation

Too Loose

Potential problems include:

  • Insufficient retention
  • Connector separation
  • Poor vibration resistance

Tolerance control helps maintain the intended balance between retention force and usability.


7.Tolerance Control Improves Assembly Consistency

Mass production requires thousands of assemblies to behave similarly.

If connector dimensions vary too much, operators may encounter:

  • Different insertion forces
  • Different locking forces
  • Different terminal positions
  • Different connector fit

This can increase:

  • Assembly time
  • Rework
  • Scrap
  • Production complaints

Consistent dimensional control improves manufacturing repeatability.


8.Tolerance Control Supports Interchangeability

OEM customers often expect components manufactured at different times to remain interchangeable.

For example:

  • Connector A from Lot 1
  • Connector B from Lot 2

should still mate correctly when both comply with the approved design.

This requires consistent control of critical dimensions.

Interchangeability is particularly important for:

  • Service replacement
  • Global manufacturing
  • Multiple production lines
  • Multiple suppliers

9.Critical-to-Function Dimensions Need More Attention

Not every connector dimension has the same impact on performance.

A practical approach is to identify:

Critical Dimensions

Dimensions directly affecting:

  • Contact performance
  • Mating
  • Sealing
  • Retention
  • Safety

Important Dimensions

Dimensions affecting:

  • Assembly
  • Positioning
  • Manufacturing consistency

General Dimensions

Dimensions with relatively low functional impact.

This allows engineering and quality teams to focus measurement resources where they create the greatest value.


10.Statistical Process Control Helps Maintain Tolerance

Mass production requires more than checking finished parts.

Manufacturing processes should be monitored continuously.

Common methods include:

  • SPC
  • Process capability analysis
  • Control charts
  • Sampling inspection
  • Automated dimensional inspection

Two commonly discussed capability indicators are:

Cp

and

Cpk

These help evaluate whether a manufacturing process can consistently produce parts within specification.

The specific acceptance criteria should be defined according to the product, drawing requirements, customer standards, and quality plan.


11.Measurement Equipment Matters

Tolerance control is only meaningful when measurement systems are appropriate.

Depending on the feature, manufacturers may use:

  • Calipers
  • Micrometers
  • Height gauges
  • Coordinate measuring machines
  • Optical measurement systems
  • Vision inspection
  • Go/No-Go gauges

For high-volume connector production, automated optical inspection can help monitor dimensional features efficiently.

Measurement systems should also be properly calibrated and maintained.


12.Mold and Stamping Processes Affect Connector Tolerances

Connector mass production often involves multiple manufacturing processes.

Injection Molding

Housing dimensions can be affected by:

  • Material shrinkage
  • Mold condition
  • Processing temperature
  • Injection parameters
  • Cooling conditions

Terminal Stamping

Terminal geometry can be influenced by:

  • Tool wear
  • Material thickness
  • Stamping accuracy
  • Progressive die condition

Assembly

Final connector dimensions can also be affected by:

  • Terminal insertion
  • Seal installation
  • Locking components
  • Assembly fixtures

Tolerance control therefore requires coordination across the entire manufacturing process.


13.Design for Manufacturability Starts With Tolerance Analysis

Tolerance control should begin before mass production.

During DFM review, engineers should ask:

  • Which dimensions are function-critical?
  • Which tolerances are realistically manufacturable?
  • Where can tolerance stack-up occur?
  • Which dimensions require automated inspection?
  • Can the process maintain the required capability?
  • Are overly tight tolerances adding unnecessary cost?

An unnecessarily tight tolerance can increase:

  • Tooling cost
  • Inspection requirements
  • Production cycle time
  • Scrap rate

The goal is not to make every dimension extremely precise.

The goal is to apply the right tolerance to the right feature.


14.Tolerance Control and Cost

Tolerance and cost are closely related.

In general, tighter tolerances may require:

  • More precise tooling
  • More process control
  • More inspection
  • Higher manufacturing cost

However, loose tolerances can create:

  • Higher defect rates
  • Assembly problems
  • Field failures
  • Customer complaints

Therefore, effective tolerance design balances:

Performance + Manufacturability + Cost

This is one of the most important principles of connector DFM.


Connector Tolerance Control Example

Consider a multi-pin connector with:

  • Housing
  • Terminals
  • Seals
  • Locking mechanism

The final mating condition depends on multiple dimensions.

A simplified tolerance chain might be:

Housing Position

↓

Terminal Position

↓

Contact Alignment

↓

Contact Force

↓

Electrical Reliability

If any critical dimension is poorly controlled, the final performance can shift.

This illustrates why connector tolerance control must be treated as a system-level engineering issue.


Common Connector Tolerance Control Mistakes

Mistake Potential Result
Designing only around nominal dimensions Unexpected production variation
Ignoring tolerance stack-up Mating problems
Overly tight tolerances Higher cost and scrap
Loose terminal positioning Contact instability
Poor seal tolerance control Leakage
Insufficient process monitoring Lot-to-lot variation
Inadequate measurement systems Undetected dimensional problems
Ignoring tooling wear Gradual dimensional drift

Connector Tolerance Control Checklist

Before releasing a connector for mass production, engineering and quality teams should review:

Design

✔ Are critical dimensions identified?

✔ Has tolerance stack-up been analyzed?

✔ Are tolerances function-based?

Tooling

✔ Can the mold maintain the required dimensions?

✔ Is stamping-tool wear monitored?

Manufacturing

✔ Are critical dimensions measured?

✔ Are process parameters controlled?

✔ Is SPC applied where appropriate?

Assembly

✔ Are terminal positions consistent?

✔ Are seals correctly installed?

✔ Are locking features functioning consistently?

Validation

✔ Is mating force within the intended range?

✔ Is contact resistance stable?

✔ Is sealing performance validated?

✔ Is interchangeability verified?


How FPIC Controls Connector Quality in Mass Production

FPIC applies engineering and manufacturing controls throughout connector production.

Quality management can include:

✔ Dimensional inspection

✔ Terminal position control

✔ Injection molding process control

✔ Stamping process monitoring

✔ Assembly verification

✔ Electrical testing

✔ Visual inspection

✔ Reliability validation

For automotive connector production, FPIC operates under IATF 16949 quality requirements and applies controlled manufacturing processes to support consistent product performance.

For customers requiring demanding cleanliness requirements, mass production can also be managed in accordance with VDA 19.1 / ISO 16232 practices where applicable.

The objective is not simply to produce connectors within drawing dimensions.

It is to maintain consistent performance across production batches.


Final Thoughts

Connector tolerance control is one of the foundations of reliable mass production.

A connector is a system of interacting components, and small dimensional variations can influence:

  • Mating
  • Contact force
  • Contact resistance
  • Sealing
  • Retention
  • Assembly consistency
  • Interchangeability

Effective tolerance engineering does not mean making every dimension as tight as possible.

It means identifying the dimensions that matter most and controlling them with the right manufacturing and inspection methods.

The best connector designs balance:

Function + Tolerance + Process Capability + Cost

When these elements are aligned from the beginning, manufacturers can achieve more consistent production and OEM customers can gain greater confidence in connector performance.


FAQ

Why is tolerance control important in connector manufacturing?

Tolerance control ensures that connector components consistently fit, mate, seal, and maintain electrical performance throughout mass production.

What is connector tolerance stack-up?

Tolerance stack-up is the cumulative effect of dimensional variations from multiple components or features that contribute to a final functional dimension.

Does tighter tolerance always mean better connector quality?

No. Excessively tight tolerances can increase manufacturing cost and scrap without providing additional functional benefits. Tolerances should be based on actual performance requirements.

Which connector dimensions are most critical?

Terminal position, contact geometry, mating features, locking structures, sealing interfaces, and other dimensions directly affecting electrical, mechanical, or sealing performance are typically critical.

How is connector dimensional tolerance controlled during mass production?

Manufacturers can use calibrated measurement equipment, automated inspection, SPC, process capability analysis, tooling control, and defined quality control plans.


Looking for Consistent Connector Quality in Mass Production?

FPIC supports OEM customers with connector design, tooling, precision manufacturing, assembly, testing, and quality control.

From DFM and tolerance analysis to mass production and inspection, our engineering team focuses on consistent connector performance and manufacturing reliability.

Contact FPIC to discuss your custom connector project.


Resources

  1. IATF 16949 – Automotive Quality Management Systems
    https://www.iatfglobaloversight.org/
    Quality management framework widely used across the automotive supply chain.
  2. ISO 9001 – Quality Management Systems
    https://www.iso.org/iso-9001-quality-management.html
    International framework for quality management and process control.
  3. ISO 16232 / VDA 19.1 – Technical Cleanliness
    https://www.iso.org/
    Standards and practices for technical cleanliness in automotive components.
  4. AIAG Core Tools
    https://www.aiag.org/
    Industry resources covering APQP, PPAP, FMEA, MSA, SPC, and related quality methodologies.
FPIC 2000V 450A connector for BESS battery interconnection

Battery energy storage systems are moving toward higher power density, larger blocks, and more demanding DC architectures. For next-generation BESS, 2000V connectors can support a platform that transmits the same power at lower current than a 1500V design, creating opportunities to reduce resistive loss, simplify parallel current paths, or increase power capacity within a defined system envelope.

That benefit is not automatic. Raising the DC voltage also increases the demands placed on insulation coordination, connector geometry, cable construction, switching protection, assembly control, and system-level validation. A 2000V-rated connection only delivers value when the battery, busbars, cables, fuses, contactors, power conversion system, enclosure, and service procedures are engineered for the same voltage class.

Direct answer: At the same transmitted power, increasing the DC voltage from 1500V to 2000V reduces current by 25%. If the total path resistance remains unchanged, the calculated resistive loss falls by 43.75%. Actual BESS performance still depends on the complete electrical and thermal design.


2000V Is a System Architecture, Not Just a Connector Rating

Recent product roadmaps show that the 2000V class is becoming a practical development direction across high-voltage energy systems. In June 2026, CATL stated that its TENER Sodium energy storage platform reserves an upgrade path to a 2000V architecture. Amphenol’s TS1 connector platform, introduced in December 2025 for high-power electrification applications including energy storage, supports up to 2000V and 450A in selected configurations. Amphenol also expanded its photovoltaic connector platform to 2000V in August 2026 for high-voltage PV and solar-plus-storage architectures.

These developments do not mean that every new BESS should immediately move beyond 1500V. They show that battery, power-electronics, cable, protection, and connector suppliers are preparing for a higher-voltage ecosystem. Whether the change makes commercial sense depends on the system topology, maximum operating voltage, power level, cooling strategy, certification route, installation conditions, and balance-of-system cost.

For engineering and procurement teams, the correct question is therefore not simply, “Is 2000V better?” It is, “Does a higher-voltage architecture improve this system after every affected component and risk is included?”

What Changes Electrically from 1500V to 2000V?

For a DC power path, the basic relationship is:

Power = Voltage × Current

If power remains constant, increasing voltage reduces the current required. The following comparison uses an ideal 1 MW DC transfer point.

Parameter 1500V Architecture 2000V Architecture
DC power 1 MW 1 MW
Calculated current 666.7A 500A
Current relative to 1500V 100% 75%
Relative (I^2R) loss at the same resistance 100% 56.25%

This calculation shows two important points. First, the current reduction is 25%, not one-third. Second, because conductor and contact loss follows (P_{loss}=I^2R), the theoretical resistive loss falls faster than the current—provided the resistance is genuinely unchanged.

Real systems are more complicated. Converter efficiency, busbar geometry, cable length, conductor cross-section, connector contact resistance, ambient temperature, enclosure airflow, and duty cycle all affect the final result. Higher voltage can reduce current-related loss, but it does not eliminate conversion losses or thermal constraints elsewhere in the BESS.

At a fixed current, a 2000V path can also transmit 33.3% more power than a 1500V path. That may support higher power density, but only when the connector, conductor, protection devices, and cooling system remain within their verified limits.

FPIC 2000V 450A connector for BESS battery interconnection

Does Higher Voltage Allow a Smaller Cable?

Potentially, but cable cross-section should never be selected from voltage and power alone.

A lower operating current may allow engineers to reduce conductor area or the number of parallel paths. The final cable decision must still account for:

  • continuous current and peak-current duration;
  • allowable conductor and terminal temperature;
  • insulation voltage and temperature rating;
  • ambient temperature and enclosure cooling;
  • cable grouping and installation method;
  • voltage drop and total path length;
  • bend radius, routing space, and mechanical stress;
  • applicable derating and end-equipment requirements.

A higher-voltage cable may require different insulation construction, wall thickness, jacket material, or spacing. As a result, a 25% current reduction does not automatically translate into a 25% reduction in cable size, copper use, or installed cost.

The connector and cable must also be evaluated as a matched termination system. A large conductor cannot compensate for a poorly controlled crimp, unstable contact interface, or unsuitable thermal path.


Why Insulation Design Becomes More Demanding

The move to a higher DC voltage changes more than the printed rating on the housing. It affects the physical distances, insulating materials, environmental assumptions, and protective measures used throughout the connection.

Clearance

Clearance is the shortest distance through air between conductive parts. The required value is influenced by working voltage, transient overvoltage, altitude, and the applicable insulation-coordination rules. Air has lower dielectric strength at higher altitude, so a connection that works at one installation elevation may require additional spacing or evaluation at another.

Creepage Distance

Creepage is the shortest path along the surface of an insulating material. It is affected by working voltage, pollution degree, condensation risk, surface geometry, and the material’s resistance to tracking. Dust, moisture, salt, and process contamination can turn an apparently clean surface into a more conductive path.

Solid Insulation and Material Selection

Housing materials must be evaluated for electrical, thermal, mechanical, and flammability requirements relevant to the product. Comparative tracking index can support material grouping, but it does not by itself establish a safe creepage distance. Wall thickness, molded features, material aging, and manufacturing consistency also matter.

IEC 60664-1 provides widely used principles for clearance, creepage, solid insulation, pollution degree, altitude, and overvoltage assessment. Its stated scope covers equipment up to 1500V DC, however. A 2000V design therefore requires the applicable product and end-equipment requirements, together with guidance from the responsible certification body; simply extending a 1500V spacing table is not a sufficient validation method.


Contact Resistance and Temperature Rise Still Control Current Capability

Higher system voltage can reduce current for a fixed power target, but it does not make contact resistance less important. Heat generated at a connection follows the same (I^2R) relationship as cable loss.

Consider an illustrative contact-interface resistance of 0.1 mΩ. At 450A, that interface would dissipate approximately 20.25W:

450A × 450A × 0.0001Ω = 20.25W

This example is not an FPIC product specification. It shows why a small change in resistance can create meaningful heat at high current.

Contact resistance can be influenced by terminal geometry, contact force, plating system, surface condition, crimp quality, conductor preparation, mating alignment, vibration, thermal cycling, and long-term stress relaxation. Temperature-rise testing should therefore use the intended conductor, termination process, ambient condition, enclosure arrangement, mounting orientation, and load profile. A current rating should not be treated as independent of those conditions.

For a deeper thermal-design discussion, see How Temperature Rise Affects High-Current Connectors.

What Should Be Verified for a 2000V BESS Connection?

UL 4128 is an important North American reference for intercell and intertier connectors used in electrochemical battery systems. The current scope covers cable connectors, cable, and mating inlets rated up to 3000V DC, and it states that these devices are not intended to be connected or disconnected under load.

The final verification plan must follow the applicable standard and end-use application. For a high-voltage battery interconnection, engineering teams should normally establish evidence for the following areas:

Verification area Question to answer Typical evidence
Voltage rating Can the complete mated interface withstand the defined working voltage and overvoltage conditions? Insulation design review, dielectric test, certification report
Insulation resistance Does electrical isolation remain acceptable before and after relevant conditioning? Insulation-resistance results under specified conditions
Thermal performance Does the interface stay within material and conductor temperature limits at the intended load? Temperature-rise test using the defined cable, ambient, and duty cycle
Contact stability Does resistance remain controlled after mechanical and environmental stresses? Initial and post-conditioning resistance measurements
Termination quality Can the cable, crimp, or busbar interface withstand assembly and service loads? Cross-section review, crimp records, pull or mechanical retention tests
Mating safety Are polarity, keying, locking, and touch-protection measures suitable for the equipment design? Dimensional inspection and functional verification
Environment Will humidity, contamination, vibration, thermal cycling, and ingress affect performance? Application-specific environmental tests; IP testing only when claimed
End-use integration Is the recognized component acceptable inside the complete BESS? Conditions-of-acceptability review and system-level evaluation

A component certificate is valuable evidence, but it is not a substitute for complete-system certification. UL explains that UL 9540 evaluates the energy storage system as an assembly, including charging, discharging, protection, controls, communications, and interaction among devices.


What FPIC’s 2000V 450A UL Recognition Covers

Representative samples of FPIC’s energy storage connector series were evaluated by UL to UL 4128 for electrochemical battery system applications. The UL documentation identifies the series under category BBTH2, with certificate number UL-US-26118764-0 and report reference E533832-20260524, issued on May 25, 2026.

The evaluated series includes insulated, single-pole cable connectors and panel-mounted inlets rated 2000V DC and 450A. For the cable-connector configuration, the evaluated conductor size is 300 kcmil. The panel-mounted versions are intended for factory assembly to suitable copper conductors or copper/copper-alloy busbars in battery equipment.

  • The scope and limitations are equally important:
  • the products are UL Recognized Components, not complete end-use equipment;
  • they are not suitable for disconnecting under load;
  • the evaluated products are intended for use within complete equipment;
  • the FPIC report states that they were not investigated for an environmental rating or for use outside an equipment enclosure;
  • acceptability must be determined in the final application.

This recognition gives BESS engineers a verified component-level reference for a 2000V, 450A intercell/intertier connection. It should not be interpreted as blanket approval for every cable, enclosure, ambient condition, or storage-system design.


A Practical Checklist Before Specifying the Connection

Before requesting a sample or quotation, define the actual operating envelope rather than providing only a voltage and current target. FPIC’s separate guide on selecting a 2000V 450A BESS connector provides additional product-screening questions.

  1. Electrical requirements: nominal voltage, maximum continuous DC voltage, transient conditions, continuous current, peak current, and duty cycle.
  2. Conductor interface: cable size and construction, busbar material and thickness, terminal temperature rating, and preferred termination method.
  3. Thermal environment: cabinet ambient temperature, cooling method, neighboring heat sources, mounting orientation, and allowable temperature rise.
  4. Installation conditions: indoor or outdoor location, enclosure protection, altitude, pollution, condensation, chemical exposure, vibration, and shock.
  5. Safety functions: polarity, mechanical keying, touch protection, locking, service isolation, and any high-voltage interlock requirement.
  6. Compliance route: target country, component standard, end-equipment standard, marking requirement, and certification-body expectations.
  7. Project inputs: drawings, 2D/3D files, cable specifications, mating layout, samples, forecast volume, and development schedule.

This information allows the connector, cable, termination, and installation method to be reviewed together. It also prevents a nominal rating from being applied outside the configuration in which it was verified.


Conclusion: 2000V Creates an Opportunity—and a Higher Design Burden

The main advantage of a 2000V BESS architecture is straightforward: more power can be transmitted with less current, or more power can be carried at the same current. This can reduce current-related losses and may simplify some conductor paths.

The engineering burden rises at the same time. Insulation coordination, creepage and clearance, material behavior, contact resistance, cable matching, service procedures, protection devices, and complete-system validation all require closer control.

FPIC’s 2000V 450A UL Recognized connector series provides a verified component option for defined electrochemical battery equipment applications. Explore FPIC’s broader energy storage connector range or request a custom connector evaluation using your maximum operating voltage, load profile, cable or busbar details, installation environment, drawings, and target compliance requirements.

Discuss your BESS interconnection project: info@fpiconn.com


FAQ

1.Does a 2000V architecture automatically make a BESS more efficient?

No. Higher voltage reduces current at the same power, which can lower resistive losses, but actual efficiency also depends on the PCS, conductors, connectors, cooling, topology, and operating profile.

2.How much does current decrease when moving from 1500V to 2000V?

Current decreases by 25% at the same power. For an ideal 1 MW DC path, current changes from approximately 666.7A at 1500V to 500A at 2000V.

3.Can a 1500V connector be used in a 2000V battery system?

No. A connection is limited by its lowest-rated component. The connector, cable, protection devices, busbars, and related equipment must all be suitable for the system’s maximum voltage and applicable transient conditions.

4.Does a 450A rating apply to every cable size and ambient temperature?

No. Current capability depends on the evaluated conductor, termination, ambient temperature, enclosure, cooling, duty cycle, and applicable derating. FPIC’s UL-evaluated cable-connector configuration uses a 300 kcmil conductor.

5.Is UL 4128 recognition the same as certification of a complete BESS?

No. UL 4128 addresses the defined intercell/intertier connector component. The complete energy storage system must be evaluated under the applicable end-equipment and installation requirements.

6.Can the FPIC connector be disconnected while current is flowing?

No. The UL documentation states that the recognized connector is not suitable for disconnecting under load. The equipment must provide an appropriate isolation and service procedure.


Resources

  1. CATL: TENER Sodium Energy Storage System and 2000V Upgrade Path, June 22, 2026.
  2. Amphenol Industrial Operations: TS1 High-Voltage, High-Current Connector, December 2025.
  3. Amphenol Industrial Operations: H4 Plus P2KV 2000V Expansion, August 20, 2026.
  4. IEC 60664-1:2020 — Insulation Coordination for Low-Voltage Supply Systems, including Amendment 1:2025.
  5. UL Standards & Engagement: UL 4128, Edition 6, published June 16, 2026.
  6. UL Solutions: Energy Storage System Testing and UL 9540 Certification.