Tag Archive for: Industrial Connector

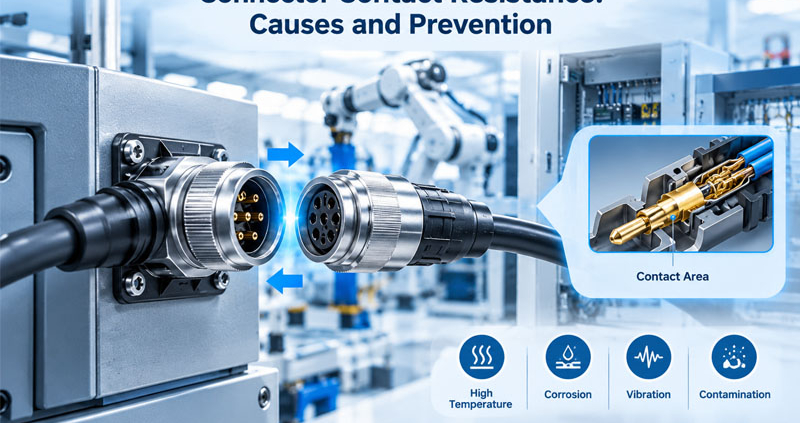
Connector Contact Resistance Causes and Prevention

Connector contact resistance is a critical electrical parameter that directly affects the reliability and efficiency of an electrical connection.

An ideal connector should provide a stable, low-resistance path between mating conductors. In real applications, however, the actual contact area is much smaller than the apparent physical contact area. Surface roughness, contact force, plating condition, contamination, vibration, temperature, and mechanical deformation can all influence the resistance of the connection.

When contact resistance increases, electrical losses and localized heating increase as well. The relationship can be expressed as:

P = I²R

where P is power loss, I is current, and R is contact resistance.

This becomes particularly important in high-current connectors, automotive systems, industrial automation equipment, energy storage systems, and other applications where connectors must operate reliably under continuous electrical and mechanical stress.

Understanding what causes contact resistance to increase—and how to prevent it—is therefore an important part of connector design and validation.
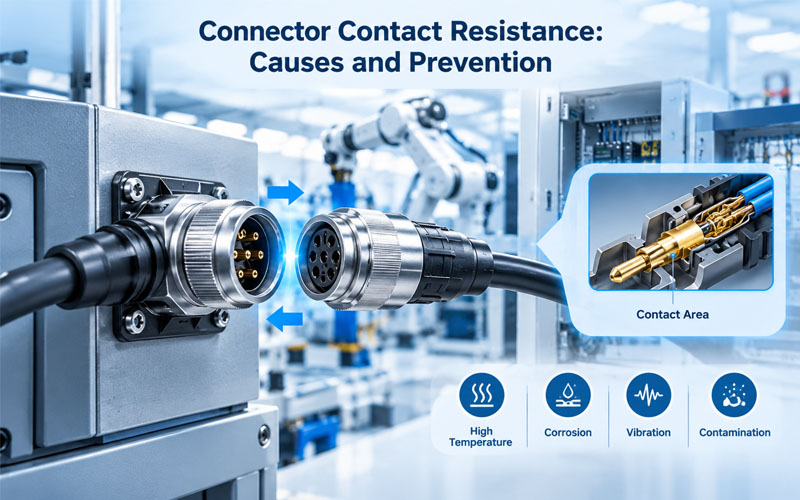
Connector Contact Resistance Causes and Prevention


1.What Is Connector Contact Resistance?

Connector contact resistance is the electrical resistance introduced at the interface between two mating conductive surfaces.

It is different from the resistance of the wire itself.

A simplified connection can be considered as:

Wire → Crimp → Terminal → Mating Contact → Terminal → Crimp → Wire

Each interface contributes to the overall electrical performance.

The mating contact is particularly important because two metal surfaces do not actually touch across their entire apparent area. Microscopic surface irregularities create localized conductive contact points known as asperities.

The effective electrical contact area is therefore much smaller than the visible mechanical contact area.

This is why contact force, surface condition, material selection, and plating have such a significant influence on connector resistance.


2.Why Low and Stable Contact Resistance Matters

Low contact resistance is important, but stable contact resistance over the connector’s service life is even more important.

A connector may initially show excellent electrical performance but experience increasing resistance after:

  • Repeated mating cycles
  • Vibration
  • Thermal cycling
  • Humidity exposure
  • Corrosion
  • High-current operation
  • Mechanical deformation
  • Surface wear

Increasing resistance can lead to several problems.

Electrical losses

Higher resistance increases voltage drop:

V = I × R

In low-voltage systems, even a small voltage drop can become significant.

Heat generation

Because:

P = I²R

heat generation increases rapidly as current rises.

For example, if current doubles, the resistive heating increases by approximately four times for the same resistance.

Accelerated degradation

Local heating can affect:

  • Contact plating
  • Terminal spring properties
  • Connector housing
  • Insulation
  • Sealing materials

This can create a feedback loop in which electrical degradation leads to additional thermal and mechanical degradation.


3.Contact Force and Contact Resistance

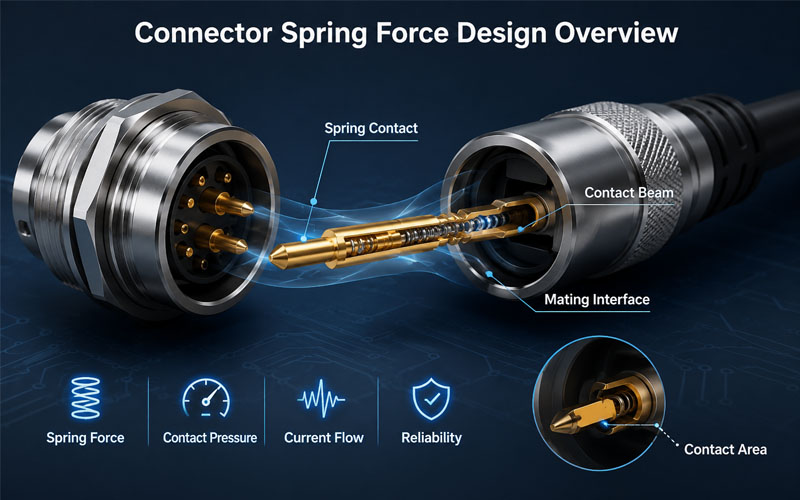
Contact force is one of the most important design factors affecting connector contact resistance.

When mating contacts are pressed together, sufficient force helps establish stable conductive contact points and break through surface films or contamination.

However, simply increasing contact force is not always the correct solution.

Excessive contact force can cause:

  • Higher insertion force
  • Difficult mating
  • Increased wear
  • Terminal deformation
  • Reduced connector service life

The objective is therefore to establish an appropriate contact-force window rather than maximizing force.

Important design factors include:

  • Contact geometry
  • Spring characteristics
  • Terminal material
  • Plating system
  • Contact wipe
  • Mating cycles
  • Required insertion force

A well-designed contact system should maintain adequate force throughout the expected operating life.


4.Contact Plating and Surface Condition

The contact surface plays a major role in electrical stability.

Common contact materials and plating systems are selected based on requirements such as:

  • Electrical conductivity
  • Corrosion resistance
  • Wear resistance
  • Mating frequency
  • Environmental exposure
  • Current level

Gold plating is commonly used where stable low-level electrical performance and corrosion resistance are important.

Tin plating can provide a practical solution for many applications, particularly where cost and current-carrying requirements are important.

However, plating selection should always be considered together with the contact geometry, environment, mating cycles, and application requirements.

Plating failure mechanisms

Contact resistance can increase when the surface experiences:

  • Wear-through
  • Oxidation
  • Corrosion
  • Plating porosity
  • Contamination
  • Mechanical damage

The correct plating system is therefore not simply a material-selection decision. It is part of the overall contact reliability strategy.


5.Fretting Corrosion and Vibration

Vibration can cause microscopic movement between mating contacts.

Although the movement may be too small to notice visually, repeated micro-motion can damage the contact surface.

This phenomenon is commonly associated with fretting corrosion.

A typical progression is:

Vibration → Micro-Motion → Surface Wear → Oxidation/Contamination → Increased Resistance

The problem can be especially challenging because a connector may pass a static resistance test while experiencing intermittent resistance changes during actual vibration.

Prevention strategies

Depending on the application, engineers can consider:

  • Appropriate contact force
  • Stable terminal retention
  • Suitable plating
  • Connector locking
  • Mechanical support
  • Cable strain relief
  • Vibration-resistant mounting

For vibration-sensitive systems, electrical monitoring during mechanical testing can provide more useful information than measuring resistance only before and after the test.


6.Crimp Quality Directly Affects Resistance

The contact interface is not the only resistance-sensitive area.

The wire-to-terminal crimp is another critical electrical connection.

A poor crimp can produce:

  • Higher resistance
  • Localized heating
  • Mechanical weakness
  • Intermittent electrical performance

Common causes include:

  • Incorrect crimp height
  • Wrong tooling
  • Improper conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Incorrect terminal-wire combination

How to control crimp resistance

Production quality control can include:

  • Crimp height measurement
  • Crimp force monitoring
  • Pull-force testing
  • Cross-section inspection
  • Electrical resistance testing

This is especially important for high-current and high-reliability cable assemblies.


7.Contamination and Oxidation

Even a well-designed contact system can experience resistance increases if the mating interface becomes contaminated.

Potential contaminants include:

  • Dust
  • Oil
  • Moisture
  • Chemical residues
  • Oxidation products
  • Assembly debris

Contamination can reduce the effective conductive area and interfere with stable metal-to-metal contact.

Environmental conditions therefore need to be considered during connector selection.

For outdoor or harsh industrial applications, engineers may need to evaluate:

  • Sealing
  • IP protection
  • Plating
  • Housing material
  • Environmental compatibility
  • Corrosion resistance

8.Connector Overheating and Thermal Runaway

High contact resistance is closely related to connector temperature rise.

Consider a high-current connection carrying 100 A.

If contact resistance is:

R = 1 mΩ

then:

P = 100² × 0.001 = 10 W

That means the contact interface is generating approximately 10 W of heat at that resistance.

If resistance increases to:

R = 2 mΩ

the heat generation becomes:

P = 100² × 0.002 = 20 W

The electrical loss has doubled.

This demonstrates why small changes in resistance can have a significant effect in high-current applications.

Thermal design should consider:

  • Current level
  • Number of energized contacts
  • Contact resistance
  • Ambient temperature
  • Duty cycle
  • Wire size
  • Connector housing
  • Heat dissipation
  • Installation conditions

Connector current ratings should therefore not be considered independently from the actual system conditions.


9.Mating Cycles and Contact Wear

Every mating and unmating operation can cause mechanical movement at the contact interface.

The contact surfaces may experience:

  • Sliding
  • Wiping
  • Friction
  • Plating wear
  • Spring deformation

After repeated cycles, the original surface condition may change.

For applications requiring frequent connection and disconnection, engineers should evaluate:

  • Rated mating cycles
  • Contact plating
  • Contact force
  • Wiping action
  • Wear resistance
  • Contact resistance after cycling

A connector should be validated against the actual expected service profile rather than relying solely on an initial resistance measurement.


10.Temperature Effects on Contact Resistance

Temperature can influence both electrical and mechanical properties.

As temperature changes, materials can expand and contract, affecting:

  • Contact dimensions
  • Contact force
  • Terminal alignment
  • Housing geometry
  • Plating interfaces
  • Crimp connections

High temperatures can also accelerate material aging and surface degradation.

Low temperatures may influence material flexibility and contact mechanics.

For connectors operating across wide temperature ranges, thermal cycling should therefore be included in reliability validation.


11.Connector Geometry and Current Distribution

Contact resistance is not determined by material alone.

The geometry of the contact system also matters.

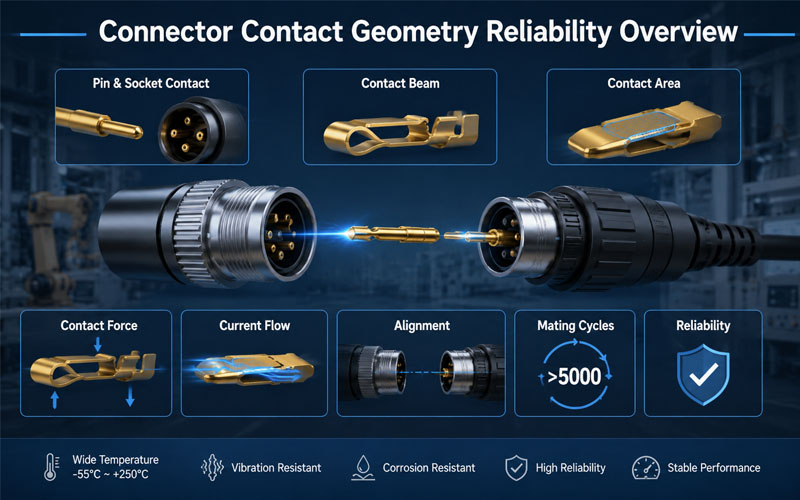
Important design variables include:

  • Contact beam shape
  • Contact area
  • Contact normal force
  • Current path length
  • Terminal thickness
  • Contact alignment
  • Mating depth
  • Current distribution

For high-current applications, engineers need to consider how current flows through the complete terminal system rather than focusing only on the nominal contact area.

Poor geometry can create localized current concentration and thermal hotspots.


12.How to Measure Connector Contact Resistance

Accurate contact resistance measurement requires an appropriate test method.

For very low resistance values, ordinary two-wire measurements can be affected significantly by:

  • Test lead resistance
  • Connection resistance
  • Instrument limitations

A four-wire Kelvin measurement can provide better accuracy for low-resistance measurements because the current and voltage measurement paths are separated.

A simplified test arrangement is:

Current Source → Connector → Current Return

while separate sensing leads measure the voltage drop directly across the contact interface.

The resistance can then be calculated using:

R = V / I

Measurement consistency matters

Testing should define:

  • Test current
  • Test voltage
  • Measurement location
  • Mating condition
  • Stabilization time
  • Temperature
  • Number of samples
  • Acceptance criteria

Without consistent test conditions, resistance results may be difficult to compare.


13.Contact Resistance Testing During Reliability Validation

Initial resistance testing is only one part of connector validation.

A more useful strategy is to measure contact resistance at different stages.

For example:

Initial Measurement

↓

Mating Cycle Test

↓

Vibration Test

↓

Thermal Cycling

↓

Environmental Exposure

↓

Final Resistance Measurement

For demanding applications, electrical performance can also be monitored during mechanical or environmental testing.

This helps identify intermittent changes that may not be visible in a simple before-and-after measurement.


14.Common Connector Contact Resistance Problems

ProblemLikely CausePotential Solution
Initial resistance too highPoor contact geometryOptimize terminal design
Resistance increases after cyclingContact wearReview plating and contact force
Resistance fluctuates during vibrationFrettingImprove retention and contact stability
Resistance rises at high currentThermal stressOptimize current capacity and thermal design
High wire-to-terminal resistancePoor crimpImprove tooling and process control
Resistance increases in humid environmentsCorrosionImprove sealing and plating
Different samples show large variationProcess variationStrengthen dimensional and electrical controls
Localized terminal heatingCurrent concentrationReview contact geometry and current path

15.How to Prevent High Connector Contact Resistance

Preventing contact resistance problems requires cooperation between electrical, mechanical, material, and manufacturing design.

1.Optimize contact geometry

Design the contact system to maintain stable force and current distribution.

2.Select suitable plating

Match the plating system to electrical requirements, mating cycles, and environmental exposure.

3.Control crimp quality

Use controlled tooling, dimensional inspection, and appropriate mechanical and electrical verification.

4.Protect the contact interface

Use appropriate sealing and environmental protection for the application.

5.Control mechanical movement

Minimize vibration-induced micro-motion through proper locking, retention, mounting, and strain relief.

6.Validate under realistic conditions

Combine contact resistance testing with mating cycles, vibration, thermal cycling, and environmental exposure where applicable.

7.Monitor manufacturing variation

Stable connector performance requires stable production processes.


16.Design Considerations for High-Current Connectors

High-current applications are particularly sensitive to contact resistance.

Examples include:

  • Energy storage systems
  • Battery systems
  • Industrial power equipment
  • Power distribution
  • Automotive electrical systems
  • Inverters
  • Power conversion equipment

In these applications, engineers should evaluate the entire current path:

Cable → Crimp → Terminal → Contact Interface → Terminal → Crimp → Cable

A low-resistance contact interface cannot compensate for a poor crimp or undersized conductor.

The complete assembly therefore needs to be designed as one electrical and thermal system.


17.Manufacturing Controls for Stable Contact Resistance

For mass production, the challenge is not only achieving low resistance on one sample.

The objective is to maintain consistent performance across large production volumes.

Important controls may include:

  • Terminal dimensional inspection
  • Contact-force verification
  • Plating inspection
  • Crimp-height control
  • Crimp-force monitoring
  • Pull-force testing
  • Automated continuity testing
  • Contact resistance testing
  • Visual inspection
  • Traceability

Process data can help identify gradual changes before they become field failures.

For customized connectors and cable assemblies, early control of critical-to-quality characteristics can significantly improve production consistency.


How FPIC Supports Connector Electrical Reliability

FPIC develops customized connector and cable assembly solutions for industrial, automotive, energy, robotics, and other demanding applications.

Contact resistance can be evaluated as part of the complete electrical and mechanical design rather than treated as an isolated specification.

Depending on project requirements, engineering evaluation may cover:

  • Contact geometry
  • Terminal material
  • Plating
  • Contact force
  • Crimp design
  • Current capacity
  • Temperature rise
  • Environmental protection
  • Mating durability
  • Electrical testing
  • Reliability validation

This approach helps customers identify resistance-related risks early and develop connector systems with stable electrical performance throughout their intended service life.


Final Thoughts

Connector contact resistance is a small electrical parameter with potentially significant consequences.

When resistance increases, voltage drop and heat generation increase. In high-current systems, even a small resistance change can create substantial localized heating.

The most effective prevention strategy is therefore not simply to specify a low initial resistance.

Engineers should consider the complete system:

Contact Geometry + Contact Force + Plating + Crimp Quality + Environmental Protection + Mechanical Stability + Thermal Design + Validation

When these factors are controlled together, connector systems can maintain more stable electrical performance and reliability over their expected operating life.


FAQ

What causes connector contact resistance to increase?

Common causes include contact wear, insufficient contact force, damaged plating, fretting corrosion, contamination, oxidation, poor crimping, vibration, thermal cycling, and mechanical deformation.

Why does contact resistance cause connector overheating?

According to P = I²R, electrical power converted into heat increases with resistance and the square of current. High-current applications are therefore particularly sensitive to small resistance increases.

How is connector contact resistance measured?

Low-resistance connector contacts are commonly evaluated using controlled current and voltage measurements. Four-wire Kelvin measurement can improve measurement accuracy by reducing the influence of test lead resistance.

Does contact force affect connector resistance?

Yes. Contact force affects the stability and effective area of the conductive interface. Too little force can increase resistance, while excessive force can increase mating force and accelerate wear.

How can connector contact resistance be reduced?

Key methods include optimizing contact geometry, selecting suitable plating, controlling crimp quality, improving environmental protection, reducing vibration-induced micro-motion, and validating resistance after mechanical and environmental testing.


Need a Reliable Custom Connector Solution?

Looking for a connector solution with stable electrical performance under demanding operating conditions?

FPIC supports custom connector and cable assembly development, including contact design, terminal and plating selection, crimping, electrical testing, and reliability validation.

Contact FPIC to discuss your connector requirements and application conditions.


Resources

  1. TE Connectivity – Connector Solutions
    Technical resources covering connector systems, contacts, terminals, and electrical connection technologies.
    TE Connectivity Connector Solutions
  2. Molex – Connector Solutions
    Technical information covering connector design, contact technologies, and electrical performance considerations.
    Molex Connector Solutions
  3. IPC/WHMA-A-620 – Cable and Wire Harness Assemblies
    Industry requirements and acceptance criteria relevant to cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  4. IEC – International Electrotechnical Commission
    International standards and technical resources for electrical and electronic components and systems.
    IEC Standards
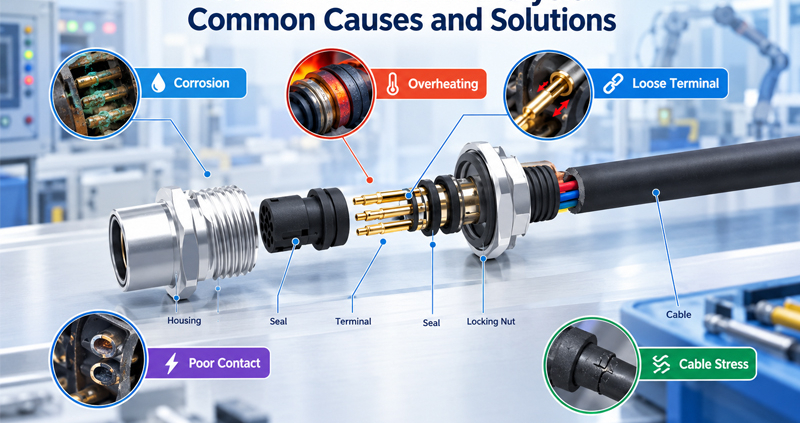
Connector Failure Analysis Common Causes and Solutions

Connectors are designed to provide a reliable electrical and mechanical interface between components, cables, and equipment. However, even a correctly specified connector can fail when electrical, mechanical, environmental, and manufacturing factors interact over time.

A connector failure may appear as a simple open circuit, intermittent signal, increased contact resistance, overheating, or mechanical disconnection. The visible symptom, however, is often not the actual root cause.

Effective connector failure analysis therefore requires more than replacing the failed component. Engineers need to determine why the connector failed, whether the failure originated in the contact system, terminal crimp, housing, sealing system, mating interface, or application environment.

This article examines the most common connector failure causes and explains practical methods for diagnosis, root-cause analysis, prevention, and validation.

Connector Failure Analysis Common Causes and Solutions


Why Connector Failure Analysis Matters

A connector is a system rather than a single component.

Its reliability depends on the interaction of:

  • Contact terminals
  • Plating and base materials
  • Connector housing
  • Crimp or termination system
  • Locking mechanism
  • Sealing components
  • Cable and strain relief
  • Mounting interface
  • Mating and unmating conditions
  • Electrical load
  • Temperature
  • Vibration and mechanical stress
  • Environmental contamination

A failure in any one of these areas can affect the complete electrical connection.

For example, an increase in contact resistance may initially appear to be a terminal problem. However, the actual cause could be insufficient contact force, fretting caused by vibration, damaged plating, terminal misalignment, or excessive thermal cycling.

This is why a structured failure analysis process is essential for demanding industrial and automotive applications.


1.Increased Contact Resistance

One of the most common connector problems is an increase in contact resistance.

When contact resistance rises, electrical losses increase according to:

P = I²R

At high current levels, even a relatively small increase in resistance can generate significant heat.

Common causes include:

  • Contact surface contamination
  • Oxidation or corrosion
  • Insufficient contact force
  • Damaged plating
  • Terminal deformation
  • Poor terminal alignment
  • Fretting corrosion
  • Excessive mating wear

Possible symptoms:

  • Localized heating
  • Voltage drop
  • Intermittent electrical performance
  • Discoloration around the terminal
  • Thermal damage to the housing

Solutions

Engineers should evaluate contact force, plating thickness, terminal geometry, mating cycles, and environmental conditions.

For high-current applications, the connector should also be evaluated under the actual operating current and temperature conditions rather than relying only on room-temperature resistance measurements.


2.Fretting Corrosion and Micro-Motion

Fretting is a particularly important failure mechanism in connectors exposed to vibration.

Small relative movements between mating contact surfaces can repeatedly disturb the contact interface. Over time, this can damage the plating and generate wear debris or oxidation products.

The result may be:

  • Increased contact resistance
  • Intermittent electrical connection
  • Signal instability
  • Progressive contact degradation

Fretting can be difficult to diagnose because the connector may initially pass a standard continuity test.

How to reduce fretting risk

Connector designs should consider:

  • Adequate contact normal force
  • Stable terminal retention
  • Appropriate plating systems
  • Mechanical locking
  • Vibration-resistant mounting
  • Proper cable strain relief

For applications involving continuous vibration, validation should include mechanical vibration testing combined with electrical monitoring.


3.Poor Crimping and Terminal Connection

A connector can contain a high-quality terminal and housing but still fail because the wire-to-terminal connection is defective.

Typical crimping problems include:

  • Insufficient crimp height
  • Excessive crimp height
  • Incorrect conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Improper tooling
  • Incorrect terminal-wire combination

A poor crimp can increase resistance and create mechanical weakness.

Why visual inspection alone is insufficient

A crimp may appear acceptable externally while having an internal defect.

For critical applications, manufacturers may use:

  • Crimp force monitoring
  • Crimp height measurement
  • Pull-force testing
  • Cross-section analysis
  • Electrical resistance testing

These controls help verify both mechanical and electrical integrity.


4.Connector Overheating

Connector overheating is often a secondary effect rather than the original failure.

A typical chain can be:

High Resistance → Heat Generation → Material Degradation → Higher Resistance → Thermal Failure

Potential causes include:

  • Excessive current
  • Undersized contacts
  • Insufficient contact force
  • Poor crimping
  • Contamination
  • Inadequate thermal management
  • Incorrect wire size
  • Loose or partially engaged terminals

How to prevent overheating

Connector selection should consider:

  • Rated current
  • Contact resistance
  • Wire gauge
  • Ambient temperature
  • Temperature rise
  • Duty cycle
  • Number of energized contacts
  • Housing material
  • Heat dissipation

The actual application conditions are particularly important because connector current ratings can depend on temperature and the number of simultaneously loaded circuits.


5.Terminal Back-Out and Poor Retention

A terminal may gradually move backward inside the connector housing if the retention mechanism is inadequate or the terminal is not fully inserted.

This can result in:

  • Reduced contact engagement
  • Intermittent connection
  • Increased resistance
  • Complete circuit interruption

Common causes

  • Incomplete terminal insertion
  • Damaged locking lance
  • Incorrect terminal dimensions
  • Excessive cable pulling force
  • Improper assembly
  • Housing deformation

Prevention

A robust connector system should incorporate reliable primary and secondary terminal locking where appropriate.

Manufacturing processes should also verify terminal insertion and retention rather than relying entirely on operator judgment.


6.Connector Mating and Misalignment Problems

Incorrect mating can cause mechanical and electrical damage.

Typical issues include:

  • Excessive insertion force
  • Cross-mating
  • Misalignment
  • Incomplete engagement
  • Damaged contacts
  • Housing deformation
  • Locking mechanism damage

A connector may appear connected while the terminals are not fully engaged.

Engineering solutions

Good connector design should provide clear mating guidance and positive locking feedback.

Depending on the application, features such as:

  • Polarization
  • Keying
  • Mechanical coding
  • CPA/secondary locks
  • Visual confirmation
  • Audible locking feedback

can reduce assembly errors.


7.Moisture, Dust, and Contamination

Environmental contamination is another major cause of connector degradation.

Moisture can promote corrosion, while dust, oil, chemicals, and other contaminants can affect contact interfaces and sealing performance.

This is particularly important for connectors used in:

  • Industrial automation
  • Outdoor equipment
  • Robotics
  • Automotive systems
  • Energy storage equipment
  • Medical equipment
  • Heavy machinery

Common symptoms

  • Corrosion
  • Leakage current
  • Increased contact resistance
  • Intermittent signals
  • Insulation degradation
  • Seal deterioration

Solutions

The connector’s environmental protection should match the actual application.

Depending on the system, engineers may need to evaluate:

  • IP protection
  • Seal material
  • Cable jacket compatibility
  • Connector material
  • Plating
  • Drainage
  • Chemical exposure
  • Temperature cycling

Waterproof performance should be validated under realistic environmental conditions rather than assumed from the connector specification alone.


8.Contact Plating Failure

Contact plating plays a critical role in long-term connector performance.

The plating system influences:

  • Corrosion resistance
  • Wear resistance
  • Contact stability
  • Mating durability
  • Environmental performance

A plating system that works well in a clean indoor application may not provide the same performance in a high-humidity, high-vibration, or corrosive environment.

Failure mechanisms may include:

  • Plating wear
  • Porosity
  • Oxidation
  • Corrosion
  • Base-metal exposure
  • Excessive mating wear

Therefore, plating selection should be based on the electrical requirements, mating cycles, environment, current level, and expected service life.


9.Mechanical Damage and Cable Strain

Connector failures do not always originate inside the connector.

Cable routing and mechanical loading can transfer excessive stress to the connector interface.

Typical causes include:

  • Excessive cable bending
  • Sharp routing angles
  • Insufficient strain relief
  • Pulling forces
  • Twisting
  • Repeated flexing
  • Incorrect mounting

Over time, these forces can damage terminals, seals, housings, or solder/crimp connections.

Prevention

A reliable connector assembly should consider the complete mechanical load path:

Cable → Strain Relief → Connector Housing → Terminal → Mating Interface

Proper strain relief and cable routing are therefore essential parts of connector reliability.


10.Thermal Cycling and Material Mismatch

Connectors used in industrial and automotive environments may experience repeated temperature changes.

Different materials expand and contract at different rates.

Repeated thermal cycling can influence:

  • Contact force
  • Terminal position
  • Housing dimensions
  • Seal compression
  • Crimp interfaces
  • Plating durability

A connector that performs well at room temperature may therefore experience degradation after repeated thermal cycles.

Recommended validation

Depending on the application, engineers may combine:

  • Thermal cycling
  • Temperature rise testing
  • Contact resistance measurement
  • Insulation resistance testing
  • Mechanical inspection

This helps determine whether electrical performance remains stable throughout the expected temperature range.


11.Vibration and Mechanical Shock

For industrial and automotive connectors, vibration can be a major reliability factor.

Repeated mechanical movement can affect:

  • Contact interfaces
  • Terminal retention
  • Housing locks
  • Cable terminations
  • Shielding connections

The key issue is that mechanical stress can eventually create an electrical failure.

Better validation strategy

Instead of performing vibration testing alone, combine mechanical vibration with continuous electrical monitoring.

For example:

Vibration → Electrical Monitoring → Contact Resistance Analysis → Physical Inspection

This approach can reveal intermittent failures that a simple post-test continuity check may miss.


12.A Structured Connector Failure Analysis Process

When a connector fails in the field or during testing, replacing the connector immediately can remove important evidence.

A structured investigation is more effective.

Step 1: Record the Failure Condition

Document:

  • Operating current
  • Voltage
  • Temperature
  • Environmental conditions
  • Mating cycles
  • Vibration exposure
  • Installation condition
  • Failure time
  • Electrical symptoms

Step 2: Perform Visual Inspection

Check for:

  • Discoloration
  • Melting
  • Corrosion
  • Cracks
  • Terminal displacement
  • Seal damage
  • Housing deformation

Step 3: Perform Electrical Testing

Depending on the failure mode:

  • Contact resistance
  • Continuity
  • Insulation resistance
  • HiPot
  • Voltage drop
  • Temperature rise

Step 4: Inspect the Terminal and Crimp

Evaluate:

  • Crimp geometry
  • Conductor placement
  • Pull strength
  • Terminal deformation
  • Contact surface condition

Cross-section analysis can be particularly useful for identifying internal crimp defects.

Step 5: Analyze the Environment

Determine whether the connector experienced:

  • Moisture
  • Dust
  • Chemicals
  • Salt exposure
  • Vibration
  • Thermal cycling
  • Mechanical stress

Step 6: Identify the Root Cause

Separate the failure symptom from the root cause.

For example:

  • Symptom: Connector terminal overheated
  • Immediate cause: Increased contact resistance
  • Root cause: Insufficient terminal contact force

This distinction is essential when developing corrective actions.


13.Connector Failure Analysis: Symptom vs Root Cause

Failure SymptomPossible Root CausesRecommended Investigation
High contact resistanceWear, corrosion, low contact forceContact resistance + terminal inspection
Connector overheatingExcess current, poor contact, bad crimpTemperature rise + resistance test
Intermittent signalFretting, vibration, terminal movementVibration test + electrical monitoring
Terminal back-outPoor retention, incomplete insertionRetention and insertion inspection
CorrosionMoisture, chemicals, poor sealingEnvironmental and seal inspection
Broken housingMechanical stress, impact, material issueMechanical inspection
Crimp failureIncorrect tooling or wire positioningCrimp cross-section + pull test
Insulation failureDamage, contamination, thermal agingIR + HiPot + visual inspection

14.Preventing Connector Failures During Product Development

Failure analysis should not only be performed after a product fails.

The most effective approach is to integrate reliability thinking into the design stage.

Design Review

Evaluate:

  • Current and voltage requirements
  • Contact system
  • Plating
  • Housing material
  • Environmental protection
  • Locking system
  • Strain relief
  • Mating cycles
  • Vibration
  • Temperature range

DFM and Assembly Review

Check:

  • Terminal insertion
  • Crimp process
  • Assembly sequence
  • Error-proofing
  • Inspection points
  • Test coverage

Reliability Validation

Depending on the application, validation may include:

  • Contact resistance testing
  • Temperature rise testing
  • Mating cycle testing
  • Vibration
  • Mechanical shock
  • Thermal cycling
  • Humidity
  • Salt spray
  • Waterproof testing
  • Insulation resistance
  • HiPot testing

The exact test plan should be based on the connector’s application and applicable customer or industry requirements.


15.Manufacturing Quality Control Is Part of Connector Reliability

Many connector failures originate from process variation rather than fundamental product design.

Important production controls include:

  • Terminal dimensional inspection
  • Plating inspection
  • Crimp height monitoring
  • Crimp force monitoring
  • Pull-force testing
  • Terminal retention testing
  • Housing dimensional control
  • Automated electrical testing
  • Visual inspection
  • Traceability

For high-reliability applications, process capability and traceability are particularly important because they help manufacturers identify whether a failure is an isolated defect or part of a larger production trend.


How FPIC Supports Connector Reliability

FPIC supports customized connector solutions for demanding industrial and automotive applications.

Our engineering approach considers connector performance across the complete product lifecycle—from component selection and structural design to manufacturing, inspection, electrical testing, and reliability validation.

Depending on project requirements, connector development can include evaluation of:

  • Terminal and contact design
  • Contact plating
  • Housing materials
  • Sealing systems
  • Locking mechanisms
  • Crimp quality
  • Shield termination
  • Environmental protection
  • Electrical performance
  • Mechanical reliability

For automotive connector applications, FPIC also applies controlled manufacturing and quality processes designed for demanding production requirements.

This engineering-focused approach helps customers identify potential failure mechanisms earlier and develop connector solutions with more stable long-term performance.


Final Thoughts

Connector failure is rarely caused by a single factor.

Electrical loading, contact force, plating, crimp quality, vibration, temperature, contamination, sealing, and mechanical stress can interact throughout the connector’s service life.

A professional connector failure analysis process therefore needs to move beyond identifying the visible symptom. Engineers should determine the failure mechanism, trace it back to the root cause, and then verify that the corrective action actually eliminates the problem.

For critical applications, the best strategy is to combine design review, manufacturing process control, electrical testing, environmental validation, and failure analysis from the beginning of the product development cycle.


FAQ

What are the most common causes of connector failure?

Common causes include increased contact resistance, fretting corrosion, poor crimping, overheating, terminal back-out, contamination, vibration, thermal cycling, and mechanical stress.

How can connector overheating be prevented?

Select an appropriate connector and terminal system for the actual current, temperature, duty cycle, and environmental conditions. Contact resistance and temperature rise should also be validated.

Why do connectors develop intermittent failures?

Intermittent failures are often related to vibration, fretting corrosion, insufficient contact force, terminal movement, poor retention, or mechanical stress.

How can a bad connector crimp be identified?

Crimp height, crimp force, pull strength, electrical resistance, and cross-section analysis can be used to evaluate crimp quality.

Is visual inspection enough for connector quality control?

No. Visual inspection is useful but cannot detect every internal or electrical defect. Depending on the application, electrical testing, dimensional inspection, crimp analysis, and reliability testing may also be required.


Need a Reliable Custom Connector Solution?

Looking for a connector supplier that can support custom design, terminal development, connector assembly, electrical testing, and reliability validation?

FPIC can help evaluate your application requirements and develop connector solutions for industrial automation, automotive, robotics, energy systems, and other demanding applications.

Contact FPIC to discuss your connector project and reliability requirements.


Resources

  1. USCAR-2 – Performance Specification for Automotive Electrical Connector Systems
    A widely referenced specification for evaluating automotive connector performance and durability.
    USCAR-2 Information
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    Provides industry requirements and acceptance criteria for cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  3. TE Connectivity – Connector Solutions
    Technical information covering connector systems, terminals, contact technologies, and application requirements.
    TE Connectivity Connector Solutions
  4. Molex – Connector Solutions
    Technical resources covering connector design, electrical performance, reliability, and application engineering.
    Molex Connector Solutions
  5. IEC – International Electrotechnical Commission
    International standards and technical resources relevant to electrical and electronic component reliability and testing.
    IEC Standards
Connector Shielding Design for EMI Protection

As industrial equipment becomes faster, more compact, and more electronically integrated, electromagnetic interference (EMI) is becoming a more important design challenge. High-speed communication, servo drives, switching power supplies, motors, inverters, sensors, and control systems may all operate within the same equipment.

A connector is often treated as a simple interface between a cable and a device. However, in an EMC-sensitive system, the connector is also part of the shielding path.

A cable may have an effective shield, but if that shield is poorly terminated at the connector, EMI can still enter or leave the system through the connection point. This is why connector shielding should be considered as part of the complete cable and enclosure design rather than as an isolated connector feature.

This article explains the key principles of connector shielding design, including shield termination, 360° shielding, grounding, backshell selection, mechanical integration, and validation.

Connector Shielding Design for EMI Protection


Why Connector Shielding Matters for EMI Protection

EMI can affect electronic systems through conducted coupling, capacitive or inductive coupling, and radiated electromagnetic fields. Shielded cables are commonly used to reduce the exposure of signal conductors to external interference and to limit unwanted radiation from the cable.

However, the cable shield is only one part of the overall protection system.

A typical shielded connection may include:

  • Shielded cable
  • Connector shell
  • Shield termination
  • Backshell
  • Equipment enclosure
  • Ground or chassis connection

If one section has significantly higher impedance or poor mechanical contact, the effectiveness of the entire shielding system can be reduced.

TE Connectivity notes that shield termination at the backshell can provide a grounding path and that the complete circumference of a cable shield can be connected to the backshell to create a more continuous shielding structure.

This leads to an important design principle:

EMI protection depends on the continuity of the entire shielding path, not simply on whether a cable is labeled “shielded.”


Connector Shielding Starts With the Complete EMC Architecture

Connector selection should not happen independently from the cable, PCB, enclosure, and grounding strategy.

Before selecting a shielded connector, engineers should understand:

  • operating frequency range
  • signal type and data rate
  • cable construction
  • shielding method
  • enclosure material
  • grounding architecture
  • environmental conditions
  • vibration and mechanical requirements

A connector that performs well in one application may not provide the same EMC performance in another system.

For example, a high-speed industrial Ethernet application may have very different shielding requirements from a low-frequency sensor cable or a motor power connection.

Therefore, connector shielding should be designed as a complete signal path.


360° Shield Termination vs Partial Shield Termination

One of the most important considerations in connector shielding is how the cable shield is terminated.

A partial shield connection may create gaps or discontinuities around the connector interface. At higher frequencies, these discontinuities can become increasingly important because the shielding system must control electromagnetic fields rather than simply provide a low-frequency electrical connection.

A 360° termination connects the cable shield around its circumference to the connector shell or backshell.

This approach can provide a more continuous shielding path between the cable and connector.

TE Connectivity provides several connector and backshell solutions using 360° screen termination for EMI/RFI applications.

Why 360° Termination Is Important

A properly designed 360° termination can help:

  • reduce shielding discontinuities
  • maintain shield continuity through the connector
  • reduce unwanted radiation
  • improve immunity against external interference
  • support more consistent EMC performance

The exact termination method still needs to be selected according to cable construction, frequency range, environmental requirements, and mechanical constraints.

360° termination should therefore be considered a design strategy rather than a universal solution for every application.


The Connector Shell Is Part of the Shielding Path

For a shielded connector system, the metallic shell should not be treated simply as a mechanical housing.

It can form part of the electromagnetic shielding path between:

Cable Shield → Connector Shell → Equipment Interface → Chassis / Enclosure

Any discontinuity within this path can reduce the effectiveness of the overall shielding structure.

Important design considerations include:

  • conductive shell material
  • shell-to-shell contact
  • plating compatibility
  • contact pressure
  • surface contamination
  • connector mating stability
  • connection to the equipment chassis

For industrial applications exposed to vibration, the shielding interface must also remain electrically stable over the intended service life.

A connector may initially show good electrical continuity but lose performance if mechanical movement causes the shielding contact to degrade.


Backshell Design Has Multiple Functions

The backshell is another important component in connector shielding design.

Depending on the application, a backshell may provide:

  • EMI/RFI shield termination
  • cable strain relief
  • mechanical cable support
  • environmental sealing
  • cable routing control
  • connection between cable shield and connector shell

TE Connectivity describes backshells as components that can combine strain relief, EMI shielding, and environmental protection.

This makes backshell selection especially important for industrial equipment, robotics, servo systems, and other applications where cables experience vibration or repeated movement.

Select the Backshell Based on the Cable

A common design mistake is selecting a connector first and treating the backshell as an accessory afterward.

The backshell should be evaluated together with:

  • cable diameter
  • braid construction
  • foil or braid shield
  • number of shield layers
  • bend radius
  • required strain relief
  • sealing requirements
  • installation process

For example, a braided cable may require a different shield termination mechanism from a foil-shielded cable.


Shield Termination Must Balance EMI and Mechanical Reliability

A shielding connection is not useful if it cannot survive the mechanical environment.

Industrial harnesses may experience:

  • continuous vibration
  • repeated bending
  • torsion
  • temperature cycling
  • connector mating and unmating
  • cable pulling forces

The shield termination must therefore maintain electrical continuity while also providing sufficient mechanical retention.

A good design should prevent the cable shield from carrying mechanical loads that should instead be handled by the strain-relief system.

This distinction is important:

Shield termination provides electrical continuity; strain relief manages mechanical forces.

Combining these functions without proper design can create long-term reliability problems.


Grounding Strategy Is Critical

A shielded connector cannot provide effective EMI protection without a suitable grounding or chassis strategy.

The design team should determine where the shield should connect and how the shielding structure interacts with the system enclosure.

Possible considerations include:

  • chassis grounding
  • equipment enclosure bonding
  • connector shell grounding
  • cable shield termination
  • PCB ground connection
  • single-point or multi-point grounding strategy depending on frequency and system architecture

There is no universal grounding configuration for every application. The correct approach depends on the system topology, operating frequency, EMC requirements, and intended current paths.

For high-frequency systems, maintaining a low-impedance shielding path is often more important than simply achieving a low DC resistance measurement.


Avoid Pigtail Shield Termination When High-Frequency Performance Matters

A pigtail termination connects the cable shield to the connector or ground using a short wire.

Although simple and easy to manufacture, a long pigtail can introduce additional inductance into the shielding path. As frequency increases, that inductive impedance can become more significant.

This is why applications with demanding EMC or high-speed signal requirements often use shorter, wider, or circumferential shield termination methods instead of long pigtails.

The design decision should consider the actual frequency range and system requirements rather than applying one termination method universally.


Connector Shielding for High-Speed Industrial Communication

High-speed communication systems are particularly sensitive to shielding discontinuities.

Applications such as:

  • Industrial Ethernet
  • machine vision
  • industrial cameras
  • robotics
  • servo drives
  • motion control
  • high-speed sensors

can require carefully controlled shielding and grounding.

For example, TE Connectivity’s M12 X-Code connector solutions use a full metal shell and 360° cable shield termination to support high-speed data transmission and EMI protection.

This illustrates an important point: shielding design must support the complete transmission channel rather than focusing only on the connector contact itself.


Mechanical Design and EMC Performance Must Work Together

Connector shielding cannot be separated from mechanical design.

An industrial connector may need to withstand:

  • vibration
  • shock
  • repeated mating cycles
  • cable movement
  • temperature changes
  • moisture and dust

At the same time, it must maintain a stable shielding connection.

A loose shell, insufficient cable retention, or poorly controlled backshell assembly can gradually affect the shielding path.

For this reason, connector design should evaluate electrical and mechanical performance together.


Environmental Protection Can Affect Shielding Performance

Industrial connectors may operate in environments containing:

  • moisture
  • dust
  • oil
  • chemicals
  • condensation
  • salt contamination

These factors can affect conductive surfaces and mechanical interfaces.

Environmental sealing is therefore not completely separate from EMC design. A connector may require both:

EMI shielding + mechanical protection + environmental sealing

For example, a backshell may combine shield termination with a heat-shrink boot or other sealing structure. TE Connectivity’s backshell solutions demonstrate how shielding, strain relief, and environmental protection can be integrated into a single termination system.


How to Validate Connector Shielding Performance

Connector shielding should be validated as part of the complete cable assembly rather than only at component level.

Depending on the application, validation may include:

  • shield continuity testing
  • low-resistance measurement
  • EMC testing
  • radiated emission testing
  • conducted emission testing
  • immunity testing
  • vibration testing
  • temperature cycling
  • environmental exposure
  • connector mating-cycle testing

The validation method should reflect the actual application frequency range and operating environment.

A connector that passes a simple continuity test does not automatically provide adequate high-frequency EMI performance.


Common Connector Shielding Design Mistakes

Several common mistakes can reduce the effectiveness of an otherwise well-designed shielded cable assembly.

Using a shielded cable with an unshielded connector

The cable may have excellent shielding performance, but the connector interface creates an exposed section.

Terminating only part of the shield

Partial termination can create discontinuities that reduce overall shielding effectiveness.

Using excessive pigtail length

A long pigtail can add inductive impedance, particularly at higher frequencies.

Ignoring connector-to-chassis bonding

The connector shell needs an appropriate electrical relationship with the equipment enclosure.

Treating the backshell as only mechanical protection

A backshell may be a critical part of the EMI shielding and strain-relief system.

Ignoring manufacturing variation

A shielding concept that works in a prototype may perform differently if shield preparation, termination length, crimp force, or assembly position varies during mass production.


How FPIC Supports Shielded Connector and Cable Assembly Projects

For custom connector and cable assembly projects, shielding performance depends on the interaction between the connector, cable, shield termination, backshell, and assembly process.

FPIC supports custom connector and cable assembly development for industrial and other demanding applications, where connector selection, cable construction, shielding, sealing, and manufacturing consistency need to be considered together.

For applications such as industrial automation, robotics, industrial cameras, and control systems, early review of the complete cable-to-connector interface can help reduce EMC and reliability risks before mass production.

The objective is not simply to select a “shielded connector,” but to develop a complete interconnect system with a controlled electrical and mechanical shielding path.


Final Thoughts

Effective connector shielding design is about maintaining a continuous and controlled electromagnetic barrier from the cable through the connector and into the equipment enclosure.

The most important design considerations include:

  • appropriate connector shell construction
  • reliable shield termination
  • 360° shielding where required
  • suitable backshell design
  • controlled grounding and bonding
  • mechanical strain relief
  • environmental protection
  • validation under realistic operating conditions

For high-speed industrial equipment and EMC-sensitive systems, the connector should be treated as an active part of the shielding architecture.

A well-designed connector interface can help protect signal integrity, reduce EMI-related failures, and improve the long-term reliability of the complete cable assembly.


FAQ

What is connector shielding?

Connector shielding is the use of conductive connector shells, backshells, shield termination methods, and grounding structures to reduce electromagnetic interference entering or leaving an electrical connection.

Why is 360° shield termination important?

A 360° termination provides a continuous circumferential connection between the cable shield and connector shielding structure. It can help reduce shielding discontinuities and support more consistent EMI performance, particularly in demanding applications.

Is a metal connector enough for EMI protection?

No. A metal connector shell alone does not guarantee effective EMI protection. Cable shield termination, shell bonding, backshell design, grounding, cable construction, and assembly quality all influence the final shielding performance.

What is the difference between shield termination and strain relief?

Shield termination establishes electrical continuity between the cable shield and connector shielding structure. Strain relief manages mechanical forces on the cable. These functions should work together but should not be treated as the same function.

Are shielded connectors necessary for industrial Ethernet?

They may be necessary depending on the system architecture, data rate, EMC environment, cable construction, and applicable requirements. High-speed industrial communication systems often require carefully controlled shielding and grounding to maintain signal integrity.

How can connector shielding performance be tested?

Depending on the application, validation can include shield continuity, low-resistance measurement, EMC testing, radiated and conducted emissions, immunity testing, vibration, thermal cycling, and environmental testing.


Need a Custom Shielded Connector or Cable Assembly?

If your application requires reliable EMI protection for industrial automation, robotics, industrial cameras, motion control, or other demanding systems, connector and cable shielding should be considered together from the beginning.

FPIC supports custom connector and cable assembly projects with engineering review, connector integration, cable assembly, and production support.

Contact FPIC to discuss your connector shielding requirements.


Resources

  1. TE Connectivity – INTERCONTEC Connectors: provides examples of industrial connectors using 360° EMC shield termination for motor and industrial applications.
  2. TE Connectivity – Tinel-Lock Backshells for Military Applications: explains shield termination, backshell design, electrical continuity, strain relief, and 360° braid termination for demanding environments.
  3. TE Connectivity – M12 X-Code Connector Series: provides an industrial M12 example using a full metal shell and 360° cable shield termination for high-speed data applications.
  4. TE Connectivity – Space-Grade Backshells for Micro-D and D-Sub Connectors: discusses the relationship between EMI shielding, grounding, backshells, strain relief, and environmental protection.
  5. TE Connectivity – Screened Backshells and Adapters: provides examples of braided, banded, and 360° shield termination solutions for screened cable assemblies.
How Connector Plating Affects Performance and Lifetime

Connector contacts may look like simple metal components, but their surface finish plays a critical role in long-term electrical and mechanical performance.

A connector can have the correct housing design, terminal geometry and contact force, yet still experience reliability problems if the plating system is not appropriate for its application.

Connector plating influences:

  • Contact resistance
  • Corrosion resistance
  • Wear resistance
  • Mating performance
  • Electrical stability
  • Environmental durability
  • Contact lifetime

For automotive electronics, industrial automation, robotics, energy storage and other demanding applications, plating should therefore be treated as part of the overall connector reliability strategy.


1.Why Connector Plating Matters

The base metal of a contact provides the mechanical and electrical foundation, but its exposed surface interacts directly with the surrounding environment.

During service, a connector may encounter:

  • Humidity
  • Oxygen
  • Salt contamination
  • Dust
  • Chemicals
  • Temperature cycling
  • Mechanical vibration
  • Repeated mating and unmating
  • Electrical current

Without an appropriate surface finish, the contact interface can gradually deteriorate.

Typical consequences include:

Surface oxidation → higher contact resistance → localized heating → unstable electrical performance

In signal applications, surface deterioration can also contribute to intermittent electrical behavior.

This is why connector plating is not simply a cosmetic treatment. It is an engineered interface between the terminal and its operating environment.

How Connector Plating Affects Performance and Lifetime


2.What Is Connector Contact Plating?

Connector contact plating is a metallic coating applied to the surface of a conductive contact.

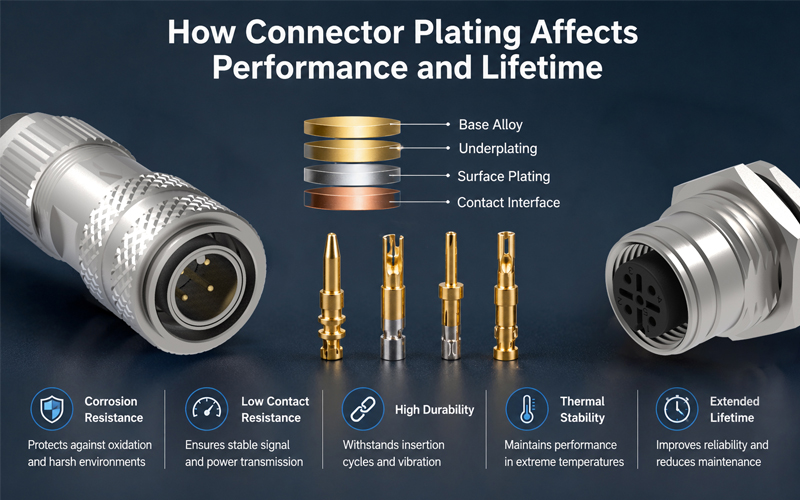
A typical contact system may contain several layers:

Base Contact Alloy

↓

Underplating

↓

Surface Plating

The base alloy provides the structural and electrical properties of the terminal.

The underplating can provide a barrier between the base material and surface plating while supporting adhesion and durability.

The surface plating is the layer that directly interacts with the mating interface and environment.

The performance of the complete system depends on how these layers work together.


3.Common Connector Plating Materials

Three commonly used plating materials are:

PlatingTypical CharacteristicsCommon Considerations
TinCost-effective, good conductivity, widely usedOxidation and wear must be considered
GoldExcellent corrosion resistance and stable contact interfaceHigher material cost
SilverHigh electrical conductivityEnvironmental and application conditions must be evaluated

The correct choice depends on the electrical, mechanical and environmental requirements rather than simply choosing the highest-value material.


4.Tin Plating

Tin is widely used for connector terminals because it provides a practical balance between performance and cost.

It is commonly considered for applications where:

  • Cost efficiency is important
  • Current levels are moderate to high
  • The connector operates in controlled environments
  • Mating frequency is limited or appropriately managed

Tin-plated contacts are often used in automotive and industrial electrical systems.

However, engineers should consider surface condition, contact force, oxidation behavior and mechanical wear.

For applications involving frequent mating or demanding environmental exposure, the complete plating design should be evaluated rather than looking only at the presence of tin plating.


5.Gold Plating

Gold is widely recognized for its excellent resistance to corrosion and stable surface characteristics.

It is particularly valuable where reliable low-level electrical contact is important.

Typical applications may include:

  • Signal connectors
  • Control electronics
  • Communication equipment
  • Industrial sensors
  • Medical electronics
  • High-reliability electronic systems

Gold plating can help maintain a stable contact interface under challenging environmental conditions.

However, gold plating is not automatically the best choice for every connector.

Engineers should also consider:

  • Plating thickness
  • Underplating
  • Contact force
  • Mating cycles
  • Base material
  • Operating environment
  • Cost target

A thin gold layer and a properly engineered gold-plating system are not necessarily equivalent.


6.Silver Plating

Silver has very high electrical conductivity and can be considered for applications where electrical performance and current handling are important.

However, silver surfaces can be affected by environmental exposure and surface contamination.

Therefore, silver plating should be evaluated according to:

  • Operating temperature
  • Current level
  • Environmental conditions
  • Contact geometry
  • Exposure to contaminants
  • Required service life

The key engineering principle is the same:

Select the plating system according to the actual operating environment.


7.How Plating Affects Contact Resistance

Contact resistance is one of the most important electrical characteristics of a connector.

Even when the bulk resistance of the terminal is low, the actual mating interface can introduce additional resistance.

A reliable plating system helps maintain a stable contact interface.

If the surface deteriorates through oxidation, corrosion or wear, contact resistance can increase.

Higher contact resistance can contribute to:

Electrical loss → Heat generation → Further degradation

This becomes especially important in higher-current applications.

For this reason, engineers should evaluate plating together with:

  • Contact force
  • Contact geometry
  • Current level
  • Terminal material
  • Surface condition
  • Temperature

Plating cannot compensate for an incorrectly designed contact system.


8.Why Plating Thickness Matters

One of the most common mistakes is evaluating plating only by material type.

For example:

Gold plated

does not fully describe the performance of a gold-plated contact.

Engineers should also consider the plating thickness and overall plating structure.

Plating thickness can influence:

  • Corrosion protection
  • Wear resistance
  • Surface durability
  • Mating lifetime
  • Barrier performance
  • Long-term contact stability

However, thicker plating is not automatically better.

Increasing plating thickness may increase cost without providing meaningful additional performance for a specific application.

The correct approach is to establish the required performance first and then define an appropriate plating system.


9.Gold Plating Thickness and Mating Cycles

For connectors with frequent mating and unmating, mechanical wear becomes a major consideration.

Every mating cycle can generate mechanical interaction between the contact surfaces.

Over time, repeated movement can gradually wear the plating.

Therefore, engineers should evaluate:

Plating Thickness + Contact Geometry + Contact Force + Mating Cycles

rather than considering plating thickness independently.

For example, a connector designed for frequent maintenance may require a different surface treatment strategy from a connector that is assembled once and expected to remain connected throughout its service life.


10.The Role of Underplating

Underplating is often overlooked because it is not visible from the finished connector surface.

However, it can play an important role in the plating system.

A properly selected underlayer can help:

  • Improve the barrier between base metal and surface plating
  • Support plating adhesion
  • Reduce migration between material layers
  • Improve long-term plating stability

The exact layer structure depends on the contact material, plating technology and application requirements.

Therefore, plating should be evaluated as a layered system, not as a single metallic coating.


11.Connector Plating and Corrosion Resistance

Corrosion is one of the major causes of connector degradation.

Environmental factors can include:

  • Moisture
  • Salt
  • Humidity
  • Industrial chemicals
  • Pollutants
  • Condensation

Corrosion at the contact interface can change the surface condition and increase electrical resistance.

For connectors used in harsh environments, engineers should consider the combined effect of:

Plating + Sealing + Housing + Environmental Protection

This is particularly important for automotive and industrial connectors installed outside protected electronic enclosures.


12.Connector Plating and Wear

Corrosion is not the only threat to plating.

Mechanical wear can also remove or damage the surface layer.

Common sources include:

  • Repeated mating
  • Vibration
  • Sliding contact movement
  • Cable movement
  • Terminal deformation
  • Assembly processes

A connector designed for high mating-cycle performance needs a plating system that can withstand the expected mechanical interaction.

This means plating selection should be connected to the connector’s mechanical design.


13.Connector Plating for High-Current Applications

High-current connectors introduce additional considerations.

As current increases, even a small increase in contact resistance can become more significant because electrical power dissipation at the contact interface increases with resistance.

Therefore, high-current connector design should consider:

  • Contact material
  • Contact cross-section
  • Contact force
  • Contact area
  • Plating
  • Thermal management
  • Terminal connection quality

For energy storage, power distribution and industrial equipment, plating should be evaluated together with the complete current-carrying system.

Plating alone does not determine current capacity.


14.Connector Plating for Signal Applications

Signal connectors have a different set of priorities.

Very low-level electrical signals can be sensitive to surface contamination and contact instability.

For these applications, engineers may prioritize:

  • Stable contact resistance
  • Corrosion resistance
  • Surface cleanliness
  • Low-level signal reliability
  • Mating-cycle performance

Gold plating is often considered in applications where maintaining a stable contact interface is particularly important.

However, the final selection still depends on connector design and operating conditions.


15.Automotive Connector Plating

Automotive connectors can experience challenging conditions, including:

  • Vibration
  • Temperature cycling
  • Humidity
  • Contamination
  • Repeated electrical loading
  • Long service periods

Therefore, plating selection must be integrated into the overall connector design.

Engineers should evaluate:

  • Terminal Material
  • Plating System
  • Contact Force
  • Sealing
  • Mechanical Retention
  • Environmental Requirements

For automotive connector production, consistent plating quality is also important because variations in surface condition can affect electrical and mechanical performance.


16.Industrial Connector Plating

Industrial connectors may be exposed to:

  • Dust
  • Oil
  • Chemicals
  • Humidity
  • Vibration
  • Frequent maintenance

Applications such as automation equipment, robotics, sensors and control cabinets may also require repeated connector service.

Therefore, plating selection should consider both environmental resistance and mechanical wear.

A connector that performs well in a clean indoor environment may require a different plating strategy when used in a factory environment with vibration, contamination or frequent maintenance.


17.Connector Plating Selection Matrix

Application RequirementKey Plating Consideration
Low-cost electrical connectionCost-effective plating system
High corrosion resistanceStable corrosion-resistant surface
Frequent matingWear resistance + plating thickness
Low-level signalsStable contact interface
High currentContact resistance + thermal performance
High humidityCorrosion resistance + sealing
Industrial environmentChemical and contamination resistance
Automotive applicationEnvironmental + mechanical durability
Long service lifeComplete plating system validation

The table should be used as an engineering starting point rather than a universal material-selection rule.


18.Common Connector Plating Selection Mistakes

Mistake 1: Choosing plating only by material

Selecting “gold” or “tin” without considering thickness, base material and application requirements can lead to an incomplete specification.

Mistake 2: Assuming thicker is always better

More plating may increase cost without providing proportional performance benefits.

Mistake 3: Ignoring mating cycles

A plating system suitable for one-time assembly may not be suitable for repeated maintenance.

Mistake 4: Ignoring the environment

Humidity, salt, chemicals and contamination can significantly influence surface durability.

Mistake 5: Evaluating plating separately from contact design

Contact force, geometry and plating work together to determine interface performance.

Mistake 6: Focusing only on initial electrical performance

A connector may pass initial electrical testing but still experience degradation during long-term environmental or mechanical exposure.


19.How to Define a Connector Plating Specification

A practical engineering specification should include more than the plating material.

Consider defining:

1.Base Contact Material

Examples include brass, phosphor bronze and other copper alloys.

2.Underplating

Define the required layer structure according to the manufacturing process and application.

3.Surface Plating

Specify tin, gold, silver or another suitable finish.

4.Plating Thickness

Define the required thickness according to performance requirements.

5.Mating Requirements

Specify expected mating and unmating cycles.

6.Environmental Requirements

Consider temperature, humidity, corrosion, chemicals and contamination.

7.Electrical Requirements

Evaluate current, voltage, contact resistance and signal characteristics.

8.Validation Requirements

Define the appropriate electrical, mechanical and environmental tests.

This creates a much stronger specification than simply stating:

“Gold plated connector.”


20.Connector Plating Quality Control

For mass production, plating quality needs to be controlled consistently.

Depending on the product and specification, manufacturers may monitor:

  • Plating thickness
  • Surface appearance
  • Adhesion
  • Contact resistance
  • Corrosion performance
  • Mechanical wear
  • Terminal dimensions
  • Base material consistency

Process control is particularly important because plating variation can affect the finished contact interface.

A robust quality system should connect:

Incoming Material → Stamping → Plating → Terminal Processing → Assembly → Electrical Testing → Final Inspection

This helps identify potential variation before products reach the customer.


21.How FPIC Supports Connector Plating and Reliability

For custom connector projects, plating should be considered during the engineering and DFM stages rather than added as a final specification.

FPIC can support connector development by evaluating the relationship between:

  • Contact material
  • Plating system
  • Terminal geometry
  • Contact force
  • Connector structure
  • Application environment
  • Manufacturing requirements
  • Electrical performance

For automotive connector applications, FPIC operates an IATF 16949 quality management system and applies controlled manufacturing and inspection processes to support consistent connector production.

The objective is not simply to provide a specific plating material, but to develop a plating and contact system that matches the customer’s actual operating requirements.


22.A Practical Connector Plating Selection Workflow

A useful engineering workflow is:

Step 1 — Define the Application

Automotive, industrial, robotics, energy storage, medical or electronics.

↓

Step 2 — Define the Environment

Temperature, humidity, corrosion, chemicals and contamination.

↓

Step 3 — Define Electrical Requirements

Current, voltage, contact resistance and signal requirements.

↓

Step 4 — Define Mechanical Requirements

Mating cycles, vibration, insertion force and contact movement.

↓

Step 5 — Select the Contact Material

Choose an appropriate conductive alloy based on mechanical and electrical requirements.

↓

Step 6 — Select the Plating System

Evaluate surface plating, underplating and thickness.

↓

Step 7 — Validate

Conduct appropriate electrical, mechanical and environmental testing.

This approach reduces the risk of selecting plating based solely on material name or initial cost.


23.Final Thoughts

Connector plating is a small physical layer with a major impact on long-term connector performance.

The right plating system can help maintain:

  • Stable contact resistance
  • Corrosion resistance
  • Mechanical durability
  • Mating performance
  • Electrical reliability
  • Long service life

But plating should never be evaluated independently.

The final performance depends on the complete system:

Contact Material + Plating + Thickness + Contact Force + Geometry + Sealing + Environment

For engineers designing reliable connectors, the key question is not:

“Which plating is best?”

It is:

“Which plating system provides the required performance for this application throughout the expected service life?”


FAQ

What is connector plating?

Connector plating is a metallic surface coating applied to electrical contacts to improve properties such as corrosion resistance, contact stability and wear performance.

Is gold plating better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact characteristics, while tin can offer a practical balance between performance and cost. The correct choice depends on the application.

Why does connector plating thickness matter?

Plating thickness can affect corrosion protection, wear resistance and service life. However, thicker plating is not automatically better because cost and application requirements must also be considered.

Does plating affect connector contact resistance?

Yes. Surface condition and plating can influence the stability of the contact interface and therefore affect contact resistance over the connector’s service life.

What plating is suitable for high-current connectors?

There is no single plating material that is universally best for high-current connectors. Engineers should evaluate plating together with contact material, geometry, contact force, resistance and thermal requirements.

How does plating affect mating cycles?

Repeated mating creates mechanical wear at the contact interface. The plating material, thickness, contact geometry and force all influence how well the surface withstands repeated cycles.

Should connector plating be specified during DFM?

Yes. Plating should be considered during connector design and DFM because it affects material selection, manufacturing processes, cost and long-term reliability.


Need Help Selecting the Right Connector Plating?

Choosing the right plating system requires more than selecting gold, tin or silver.

FPIC can help evaluate contact material, plating, terminal design, environmental requirements and manufacturing considerations for custom connector applications.

Talk to our engineering team about your connector requirements.


Resources

  • IPC/WHMA-A-620 — Requirements and Acceptance for Cable and Wire Harness Assemblies
  • SAE — Automotive engineering standards and specifications
  • IEC — International electrotechnical standards
  • IATF 16949 — Automotive quality management system requirements
Connector Material Selection Guide for Engineers

A connector may look simple from the outside, but its reliability depends heavily on the materials used throughout the assembly.

A typical connector includes several material systems:

Housing + Contacts + Plating + Seals + Locks + Secondary Components

Each material has a different function.

The housing must provide insulation and mechanical protection. The contact system must maintain stable electrical performance. Plating must protect the contact interface from corrosion and wear. Seals must maintain environmental protection without compromising assembly performance.

Selecting materials based only on cost or a single specification can create reliability problems later in the product lifecycle.

For demanding applications such as automotive electronics, industrial automation, robotics, medical equipment, and energy systems, material selection should therefore be treated as a system-level engineering decision.

The objective is to balance:

Electrical Performance + Mechanical Strength + Thermal Stability + Environmental Resistance + Manufacturability + Cost

Connector Material Selection Guide for Engineers


Why Connector Material Selection Matters

Connector materials directly influence how a connector performs throughout its service life.

Poor material selection can contribute to:

  • Contact resistance increase
  • Corrosion
  • Terminal deformation
  • Housing cracking
  • Seal degradation
  • Insulation failure
  • Poor mating performance
  • Reduced vibration resistance
  • Premature connector failure

For example, a housing material may meet the required temperature rating but lack sufficient mechanical strength.

Likewise, a contact alloy may provide excellent conductivity but require a different plating system to achieve the required corrosion and wear resistance.

This is why engineers should evaluate the complete material combination, rather than selecting each material independently.


1.Connector Housing Material Selection

The connector housing provides:

  • Electrical insulation
  • Mechanical support
  • Terminal positioning
  • Mating alignment
  • Environmental protection
  • Structural protection

The housing material therefore needs to withstand the expected electrical, thermal, mechanical, and environmental conditions.

Common connector housing materials include:

  • PA / Nylon
  • PBT
  • PPS
  • LCP
  • PEEK
  • PC and other engineering polymers

The best material depends on the application rather than simply its nominal strength.


2.PA / Nylon

Polyamide materials are widely used in connector housings because they can provide a useful combination of:

  • Mechanical strength
  • Impact resistance
  • Processability
  • Cost efficiency

However, different grades can behave differently in terms of:

  • Water absorption
  • Dimensional stability
  • Temperature resistance
  • Chemical resistance

For applications involving humidity or significant temperature variation, engineers should evaluate the specific PA grade rather than treating all nylon materials as equivalent.


3.PBT

Polybutylene terephthalate, or PBT, is commonly used for electrical and automotive connector housings.

Potential advantages include:

  • Good dimensional stability
  • Electrical insulation
  • Chemical resistance
  • Suitable molding characteristics
  • Good temperature performance for many applications

PBT can be attractive where dimensional precision and electrical insulation are important.


4.PPS for Higher-Temperature Applications

Polyphenylene sulfide (PPS) is an engineering polymer commonly considered for demanding thermal and chemical environments.

Potential characteristics include:

  • High temperature resistance
  • Low moisture absorption
  • Good dimensional stability
  • Chemical resistance
  • Electrical insulation

PPS can be useful when the connector must maintain dimensional stability under elevated temperatures.

However, material selection should always consider the actual temperature profile, not simply the maximum advertised material temperature.


5.LCP for Fine-Pitch Connectors

Liquid crystal polymer (LCP) is often considered for compact and fine-pitch connector designs.

Its characteristics can support applications requiring:

  • Thin-wall molding
  • Dimensional precision
  • Fine-pitch structures
  • Good thermal performance
  • Low moisture absorption

As connector dimensions decrease, housing dimensional stability becomes increasingly important.

A material suitable for a large connector may not necessarily be the best choice for a miniature high-density connector.


6.PEEK for Highly Demanding Applications

PEEK is a high-performance engineering polymer used in applications requiring demanding combinations of:

  • Temperature resistance
  • Chemical resistance
  • Mechanical strength
  • Dimensional stability

Its higher material cost means it is generally considered when standard engineering plastics cannot adequately meet the application requirements.

Material selection should therefore consider total system requirements, rather than simply selecting the highest-performance material available.


7.Flame Retardancy

For many electronic and industrial applications, connector housing materials may need to meet specific flammability requirements.

Engineers should consider:

  • Applicable safety requirements
  • Electrical application
  • Equipment enclosure
  • Operating voltage
  • Installation environment

A flame-retardant grade can affect other material characteristics such as:

  • Mechanical strength
  • Flow behavior
  • Moldability
  • Cost

Therefore, flame retardancy should be evaluated together with the overall material specification.


8.Connector Contact Material Selection

The contact system is responsible for maintaining the electrical interface.

Common contact alloys include:

  • Copper
  • Brass
  • Phosphor bronze
  • Copper alloys
  • Beryllium copper for specialized applications

The selected material affects:

  • Electrical conductivity
  • Spring properties
  • Contact force
  • Fatigue resistance
  • Thermal behavior
  • Corrosion resistance
  • Manufacturability

A connector contact must provide both electrical performance and mechanical reliability.


9.Brass Contacts

Brass is widely used for connector terminals because it provides a practical balance of:

  • Conductivity
  • Strength
  • Formability
  • Cost

It can be suitable for many general-purpose connector applications.

However, for high-flex or high-contact-force applications, another copper alloy may provide more suitable mechanical properties.


10.Phosphor Bronze Contacts

Phosphor bronze can provide good spring characteristics and fatigue resistance.

It is often considered when the contact must maintain stable mechanical behavior during repeated mating or long-term operation.

Potential applications include:

  • Signal connectors
  • Control connectors
  • Industrial equipment
  • Repeated mating interfaces

The final choice depends on the required contact force, conductivity, mating cycles, and environmental conditions.


11.Beryllium Copper

Beryllium copper can provide excellent spring properties and good electrical conductivity.

It may be considered for applications requiring:

  • High contact force
  • Miniaturized contacts
  • Repeated mating
  • Strong elastic recovery

Because material cost and processing considerations can be higher, engineers should use it when its performance advantages justify the additional complexity.


12.Contact Plating Selection

Contact plating forms the actual surface interface between mating contacts.

Common plating materials include:

Tin

Tin is widely used for cost-sensitive applications and can provide practical performance for many power connections.

Gold

Gold plating provides excellent corrosion resistance and stable contact behavior.

It is particularly useful where:

  • Low-level signals are involved
  • Long-term contact stability is important
  • Corrosive environments are present
  • High mating-cycle performance is required

Silver

Silver has excellent electrical conductivity and can be considered for certain power and high-current applications.

However, its behavior under specific environmental conditions must be carefully evaluated.


13.Gold Plating Thickness Matters

Simply specifying “gold plated” is not enough.

Engineers should also consider:

  • Gold thickness
  • Plating area
  • Underplating
  • Contact force
  • Mating cycles
  • Operating environment

A thin decorative gold layer and an engineered contact plating system do not necessarily provide the same long-term performance.

For demanding applications, plating specifications should be clearly defined in the connector drawing or technical specification.


14.Underplating Matters Too

The plating system can include multiple layers.

For example:

Base Contact Alloy → Underplating → Gold Surface

The underplating can help provide:

  • Corrosion protection
  • Diffusion resistance
  • Better plating stability

The complete plating structure should therefore be evaluated rather than looking only at the visible surface material.


15.Connector Seal Material Selection

Seals become critical when connectors must resist:

  • Water
  • Dust
  • Oil
  • Chemicals
  • Temperature cycling

Common sealing materials include:

  • Silicone rubber
  • EPDM
  • Fluoroelastomer materials
  • Other application-specific elastomers

The correct seal depends heavily on the environment.


16.Silicone Seals

Silicone can provide good flexibility across a broad temperature range.

It is commonly considered where connectors must tolerate:

  • Temperature variation
  • Repeated assembly
  • Flexible sealing interfaces

However, chemical compatibility must still be evaluated for the actual application.


17.EPDM Seals

EPDM can provide good resistance to:

  • Water
  • Weathering
  • Ozone
  • Certain environmental conditions

It may be suitable for outdoor or automotive environments depending on the specific fluid and temperature exposure.


18.Chemical Compatibility Is Critical

A connector material may perform well in a laboratory but degrade when exposed to the actual application environment.

Potential contaminants include:

  • Automotive fluids
  • Lubricants
  • Cleaning agents
  • Coolants
  • Hydraulic fluids
  • Industrial chemicals

Material compatibility should therefore be validated against the actual chemicals and concentrations expected during the connector’s service life.


19.Temperature Selection Should Consider the Complete System

Connector temperature performance is not determined by housing material alone.

The complete system includes:

Current → Contact Resistance → Heat Generation → Housing → Surrounding Environment

Higher current can increase temperature at the contact interface.

This means the connector must be evaluated under realistic electrical loading.

Engineers should consider:

  • Ambient temperature
  • Current load
  • Number of loaded circuits
  • Contact resistance
  • Heat dissipation
  • Housing material
  • Installation conditions

20.Material Selection for High-Current Connectors

High-current connectors place greater demands on the contact system.

Important factors include:

  • Contact resistance
  • Conductivity
  • Contact force
  • Terminal cross-section
  • Plating
  • Temperature rise
  • Thermal dissipation

Simply choosing a highly conductive alloy does not automatically create a reliable high-current connector.

The complete contact geometry and mechanical interface also matter.


21.Material Selection for Fine-Pitch Connectors

Miniaturized connectors create different material challenges.

As pitch decreases:

  • Housing walls become thinner
  • Terminal spacing decreases
  • Dimensional tolerances become tighter
  • Mating alignment becomes more sensitive

Materials with good dimensional stability and molding precision may therefore become increasingly important.

This is one reason material selection should be performed together with connector geometry and manufacturing process development.


22.Material Selection for Automotive Connectors

Automotive connectors may encounter:

  • Temperature cycling
  • Vibration
  • Humidity
  • Dust
  • Oil
  • Chemical exposure
  • Long service life requirements

Material selection should therefore consider the complete automotive environment.

For automotive connector products, FPIC applies IATF 16949 quality management requirements and supports production processes designed for demanding automotive applications.


23.Material Selection for Industrial Connectors

Industrial connectors may be exposed to:

  • Continuous vibration
  • Machinery movement
  • Oil
  • Dust
  • Chemicals
  • Outdoor environments

Industrial connector material selection should consider not only IP protection but also mechanical durability and chemical compatibility.

For example, an industrial connector used near motors may require different mechanical characteristics from one installed inside a protected control cabinet.


24.Material Selection for Medical Connectors

Medical applications may place additional requirements on:

  • Biocompatibility
  • Cleaning resistance
  • Chemical exposure
  • Sterilization
  • Reliability
  • Traceability

The material selection process should therefore begin with the applicable medical device requirements and cleaning or sterilization process.


25.Manufacturing Must Be Considered

A material with excellent laboratory performance may still be difficult to manufacture.

Engineers should evaluate:

  • Injection molding behavior
  • Shrinkage
  • Warpage
  • Flow characteristics
  • Terminal stamping
  • Plating process
  • Crimp compatibility
  • Assembly tolerances

Material selection should support not only prototype performance but also stable mass production.


Connector Material Selection Matrix

ComponentCommon MaterialsMain Selection Factors
HousingPA, PBT, PPS, LCP, PEEKTemperature, insulation, strength, chemicals
ContactBrass, phosphor bronze, copper alloysConductivity, spring force, fatigue
PlatingTin, gold, silverCorrosion, current, mating cycles
SealSilicone, EPDM, fluoroelastomerTemperature, water, chemicals
Locking PartsEngineering plastics / metalsRetention, vibration, durability
ShieldingCopper alloys / metal shellsEMC, grounding, mechanical strength

Common Connector Material Selection Mistakes

MistakePotential Consequence
Selecting housing only by temperature ratingMechanical or dimensional problems
Treating all nylon grades as identicalUnexpected moisture or thermal behavior
Selecting contact material only by conductivityInsufficient spring performance
Specifying gold plating without thicknessUnclear contact durability
Ignoring underplatingCorrosion or diffusion concerns
Selecting seals without chemical testingSwelling or degradation
Ignoring current-related heat generationExcessive temperature rise
Choosing materials without DFM reviewMolding or assembly problems
Selecting the highest-performance material automaticallyUnnecessary cost
Evaluating materials independentlySystem-level compatibility problems

A Practical Connector Material Selection Workflow

Step 1: Define the Environment

Identify:

  • Temperature
  • Humidity
  • Water
  • Dust
  • Chemicals
  • Vibration
  • UV exposure

Step 2: Define Electrical Requirements

Identify:

  • Current
  • Voltage
  • Signal type
  • Contact resistance
  • Mating cycles

Step 3: Define Mechanical Requirements

Consider:

  • Contact force
  • Mating force
  • Retention
  • Shock
  • Vibration
  • Connector size

Step 4: Select Housing Material

Match:

Temperature + Insulation + Mechanical + Environmental Requirements

Step 5: Select Contact Alloy

Match:

Conductivity + Spring Properties + Fatigue + Formability

Step 6: Select Plating

Match:

Corrosion + Wear + Current + Signal + Mating Cycles

Step 7: Select Seal Material

Match:

Temperature + Fluids + Water + Chemical Exposure

Step 8: Validate the Complete Connector

Evaluate:

  • Electrical performance
  • Mechanical performance
  • Temperature rise
  • Environmental resistance
  • Mating cycles
  • Dimensional stability
  • Production consistency

Material Selection Should Follow Application Requirements

A common mistake is starting with a preferred material and trying to make it fit the application.

A better approach is:

Application → Requirements → Material Properties → Component Design → Validation

For example, if a connector operates in a high-temperature environment, engineers should not simply select the highest-temperature housing material.

They should first ask:

  • What is the actual temperature profile?
  • How much current flows through the contacts?
  • How long is the exposure?
  • Is vibration present?
  • Are chemicals present?
  • How many mating cycles are required?

The answers determine the appropriate material combination.


Why Material Compatibility Matters

A connector is a multi-material system.

Consider:

Housing + Contact Alloy + Plating + Seal + Cable + Mating Connector

Changing one material can influence another.

For example:

  • Housing shrinkage can affect terminal position.
  • Contact force can affect plating wear.
  • Seal hardness can affect mating force.
  • Temperature can affect housing dimensions.
  • Chemical exposure can affect both housing and seals.

This is why reliable connector development requires cross-functional material engineering.


How FPIC Supports Connector Material Selection

FPIC provides customized connector development and manufacturing solutions covering:

  • Connector housing materials
  • Contact materials
  • Contact plating
  • Sealing systems
  • Terminal stamping
  • Connector assembly
  • Electrical testing
  • Dimensional inspection
  • Reliability validation

FPIC’s automotive connector products are manufactured under IATF 16949 quality management requirements.

For automotive connector production, FPIC also supports mass-production cleanliness requirements aligned with VDA 19.1 / ISO 16232 practices.

Material and component selection can be evaluated together with connector geometry, tooling, assembly, and testing requirements.

This system-level approach helps OEM customers develop connectors that balance performance, reliability, manufacturability, and cost.


Final Thoughts

Connector material selection is not simply a question of choosing the strongest plastic, most conductive metal, or thickest plating.

The correct material combination depends on the complete application.

Engineers should evaluate:

Housing + Contact + Plating + Seal + Environment + Electrical Load + Mechanical Requirements

The best connector material is the one that provides the required performance throughout the expected service life while remaining manufacturable and commercially practical.

A structured selection process can help reduce:

  • Corrosion risk
  • Thermal problems
  • Mechanical failure
  • Seal degradation
  • Manufacturing variation
  • Lifecycle cost

Ultimately, successful connector design begins with understanding the application and selecting materials that work together as a complete system.


FAQ

What is the most important factor in connector material selection?

There is no single factor. Temperature, current, environment, mechanical loading, mating cycles, dimensional requirements, and manufacturing conditions should all be considered together.

Which material is commonly used for connector housings?

PA and PBT are widely used for many connector applications, while PPS, LCP, PEEK, and other engineering polymers may be considered for more demanding thermal, dimensional, or chemical requirements.

What materials are commonly used for connector contacts?

Brass, phosphor bronze, and other copper alloys are commonly used. The selection depends on conductivity, spring properties, contact force, fatigue resistance, and application requirements.

Is gold plating always better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact performance, but it can increase cost. Tin may be suitable for many power applications. The correct plating depends on current, signal type, environment, and mating requirements.

How should connector seal material be selected?

Seal material should be evaluated against the actual temperature range, water exposure, chemicals, oils, cleaning agents, and expected service life.

Does connector housing material affect electrical reliability?

Yes. Housing material affects insulation, terminal positioning, dimensional stability, heat resistance, and mechanical protection, all of which can influence connector reliability.

Why should material selection consider manufacturing?

A material may perform well technically but create molding, stamping, plating, assembly, or cost problems at production volume. DFM should therefore be included early in the material selection process.


Need Help Selecting Materials for Your Connector?

FPIC supports OEM and engineering teams with connector design and manufacturing from material selection and tooling through assembly, testing, and mass production.

Whether you need a compact fine-pitch connector, high-current connector, automotive connector, industrial connector, or customized interconnection solution, our engineering team can evaluate the complete material and application requirements.

Contact FPIC to discuss your connector development project.


Resources

  1. IEC
    https://www.iec.ch/
    International standards and technical resources covering electrical and electronic technologies.
  2. SAE International
    https://www.sae.org/
    Automotive engineering standards and technical resources.
  3. IPC
    https://www.ipc.org/
    Industry standards and resources for electronic interconnection and manufacturing.
  4. IATF Global Oversight
    https://www.iatfglobaloversight.org/
    Resources related to IATF 16949 automotive quality management requirements.
Connector Miniaturizationfor Modern Electronics

Modern electronic systems are becoming smaller, lighter, and more integrated.

Devices that once had plenty of internal space now need to accommodate more functions within increasingly compact packages.

This trend has created strong demand for smaller and higher-density connectors.

However, making a connector smaller is not simply a matter of reducing the housing dimensions.

As connector size decreases, the available space for contacts, insulation, mechanical structures, sealing, and assembly also becomes smaller.

At the same time, electrical and mechanical requirements often remain the same—or become more demanding.

Connector miniaturization therefore requires a careful balance between:

Size + Electrical Performance + Mechanical Reliability + Manufacturability

For applications such as automotive electronics, industrial automation, medical equipment, consumer electronics, robotics, and compact control systems, successful miniaturization requires engineering optimization at every stage.

Connector Miniaturizationfor Modern Electronics


What Is Connector Miniaturization?

Connector miniaturization refers to reducing the physical size, pitch, height, or overall footprint of a connector while maintaining its required functional performance.

Miniaturization may involve:

  • Smaller housing dimensions
  • Reduced contact pitch
  • Smaller terminals
  • Lower connector height
  • Higher contact density
  • Reduced mounting footprint

The goal is usually to achieve:

More electrical functionality in less physical space.

However, reducing dimensions can create new engineering constraints.


Why Are Connectors Becoming Smaller?

Several market trends are driving connector miniaturization.

Smaller Electronic Devices

Electronic products increasingly require:

  • Compact control units
  • Smaller sensors
  • Reduced PCB size
  • Higher functional density

Connectors must fit within these increasingly constrained spaces.


Higher Functional Integration

A single electronic module may now integrate:

  • Power
  • Data
  • Sensors
  • Control signals
  • Communication interfaces

This increases the number of electrical connections required within the same physical space.


Weight Reduction

In automotive and portable equipment, reducing component size can also contribute to overall weight reduction.

Smaller connectors can help optimize:

  • Wiring space
  • Module dimensions
  • Packaging
  • System weight

1.Contact Pitch Becomes More Challenging

One of the biggest challenges in connector miniaturization is reducing contact pitch.

As the distance between contacts decreases, engineers must maintain sufficient:

  • Electrical isolation
  • Mechanical strength
  • Positioning accuracy
  • Insulation performance

A smaller pitch leaves less room for dimensional variation.

This makes:

Terminal Position + Housing Accuracy + Manufacturing Tolerance

increasingly important.


2.Electrical Clearance Becomes More Limited

When contacts are positioned closer together, the available electrical spacing decreases.

Engineers need to evaluate:

  • Clearance
  • Creepage
  • Insulation thickness
  • Working voltage
  • Pollution environment

For higher-voltage applications, simply reducing contact spacing may not be possible without changing the connector architecture.

This creates a fundamental design challenge:

How can the connector become smaller without compromising electrical safety?


3.Current Density Can Increase

Miniaturization can also increase current density.

If the same current must pass through a smaller terminal, the available conductive cross-section may decrease.

This can increase:

  • Current density
  • Joule heating
  • Contact temperature
  • Thermal stress

The design must therefore balance:

Contact Size + Material Conductivity + Contact Resistance + Current Rating

A smaller connector is not automatically suitable for the same current level as a larger connector.


4.Thermal Management Becomes More Difficult

Heat generated at a connector contact must be transferred away from the contact interface.

When connector dimensions decrease:

  • Thermal paths may become smaller
  • Contact spacing may decrease
  • Heat concentration can increase
  • Cooling space may be reduced

This can become particularly important in:

  • High-current applications
  • Compact automotive modules
  • Industrial control systems
  • Power electronics

Thermal design should therefore be considered alongside electrical design.


5.Contact Spring Design Becomes More Sensitive

Smaller terminals have less physical space for spring structures.

However, the contact still needs sufficient force to maintain reliable electrical connection.

The challenge becomes:

Small Contact + Controlled Spring Force + Long-Term Reliability

If spring force is too low:

  • Contact resistance may increase
  • Vibration resistance may decrease
  • Intermittent connections may occur

If spring force is too high:

  • Mating force increases
  • Contact wear may accelerate
  • Mating cycle life may decrease

Miniaturization therefore requires highly controlled contact geometry.


6.Mechanical Strength Can Be Reduced

Reducing terminal and housing dimensions can reduce structural strength.

Miniature connectors may be more sensitive to:

  • Insertion force
  • Extraction force
  • Cable pulling
  • Side loading
  • Vibration
  • Shock

The housing must therefore maintain sufficient:

  • Retention strength
  • Locking performance
  • Terminal support
  • Mechanical stability

Miniaturization should never compromise the mechanical integrity of the connector.


7.Manufacturing Tolerances Become More Critical

As components become smaller, the same absolute dimensional variation represents a larger percentage of the total geometry.

For example, a small terminal-position variation may have little effect in a large connector but become significant in a fine-pitch connector.

Critical areas include:

  • Terminal pitch
  • Terminal position
  • Housing cavities
  • Locking features
  • Contact geometry
  • Seal interfaces

This makes precision manufacturing and tolerance control increasingly important.


8.Assembly Becomes More Difficult

Smaller connector components can be more challenging to assemble.

Potential problems include:

  • Terminal misalignment
  • Incomplete terminal insertion
  • Seal damage
  • Housing deformation
  • Locking errors

Manual assembly becomes more difficult as component size decreases.

For high-volume production, manufacturers may need:

  • Precision assembly fixtures
  • Automated insertion
  • Vision inspection
  • Automated electrical testing

9.Inspection Becomes More Challenging

Miniaturized features may be difficult to inspect using conventional measurement methods.

Traditional tools may not provide sufficient resolution or repeatability.

Manufacturers may therefore use:

  • Optical inspection
  • CCD systems
  • Microscopic inspection
  • Coordinate measurement
  • Automated dimensional analysis

Inspection strategies must be designed around the actual critical features of the connector.


10.Miniaturization Can Affect Mating Reliability

Smaller connectors may have less mechanical tolerance for misalignment.

During mating, even a small angular or positional deviation can influence:

  • Insertion force
  • Terminal engagement
  • Contact wipe
  • Housing alignment

Good guiding features become increasingly important.

Common design solutions include:

  • Polarization keys
  • Guide posts
  • Chamfered mating surfaces
  • Self-alignment structures

These features help reduce the risk of incorrect or incomplete mating.


11.Sealing Becomes More Difficult

For miniature waterproof connectors, the available space for seals is limited.

Yet the connector may still need to achieve:

  • IP67
  • IP68
  • Other application-specific sealing requirements

Engineers must optimize:

  • Seal geometry
  • Compression
  • Housing interfaces
  • Cable diameter
  • Material selection

Reducing the connector size without compromising sealing performance can be challenging.


12.Miniaturization and Mating Cycles

A smaller connector does not necessarily have a shorter mating life, but reducing contact dimensions can make wear management more difficult.

Each mating cycle may affect:

  • Contact plating
  • Spring structure
  • Contact surface
  • Housing alignment

For applications requiring frequent connection and disconnection, engineers should validate:

  • Insertion force
  • Extraction force
  • Contact resistance
  • Wear
  • Mating cycle performance

13.Material Selection Becomes More Important

Material selection can become more critical as connector dimensions decrease.

The housing material must provide appropriate:

  • Mechanical strength
  • Dimensional stability
  • Temperature resistance
  • Electrical insulation

Contact materials must provide:

  • Conductivity
  • Elasticity
  • Fatigue resistance
  • Corrosion resistance

For miniature connectors, small changes in material performance can have a noticeable impact on the overall system.


14.Miniaturization Requires Better Thermal and Electrical Simulation

For advanced connector designs, simulation can help evaluate potential problems before tooling.

Depending on the application, engineers may evaluate:

Electrical

  • Current density
  • Voltage distribution
  • Contact resistance

Thermal

  • Temperature rise
  • Heat concentration
  • Thermal paths

Mechanical

  • Contact deformation
  • Stress distribution
  • Mating force

Simulation does not replace physical testing, but it can help identify design risks earlier.


Miniaturization Trade-Offs

Connector miniaturization is fundamentally an optimization problem.

Design GoalPotential Challenge
Smaller housingLess internal space
Higher contact densityReduced spacing
Higher currentGreater heat generation
Lower mating forcePotentially lower contact force
Smaller terminalsReduced mechanical strength
Smaller sealsMore difficult sealing
Tight tolerancesHigher manufacturing cost
More featuresMore complex assembly

The objective is not simply:

Make It Smaller.

The objective is:

Make It Smaller Without Losing Performance.


Application Considerations

Different applications have different miniaturization priorities.

ApplicationKey Miniaturization Challenge
Automotive ElectronicsSpace, vibration, temperature
Medical EquipmentCompactness, reliability, cleanliness
Industrial AutomationDensity, mechanical durability
RoboticsSize, movement, mating cycles
Consumer ElectronicsSpace and high-density interconnection
SensorsCompact size and environmental protection
Control ModulesDensity, thermal management, assembly

How to Approach Miniature Connector Design

A successful miniature connector development process should include:

Step 1: Define the Application

Identify:

  • Voltage
  • Current
  • Signal type
  • Temperature
  • Vibration
  • Mating cycles
  • Environmental exposure

Step 2: Establish the Size Target

Define:

  • Maximum housing dimensions
  • Contact pitch
  • Mounting footprint
  • Connector height

Step 3: Design the Contact System

Optimize:

  • Contact geometry
  • Spring force
  • Contact material
  • Plating
  • Current capacity

Step 4: Analyze Thermal and Electrical Performance

Evaluate:

  • Contact resistance
  • Temperature rise
  • Current density
  • Clearance
  • Creepage

Step 5: Perform Tolerance Analysis

Review:

  • Terminal position
  • Housing dimensions
  • Mating alignment
  • Locking features
  • Seal interfaces

Step 6: Validate Through Testing

Typical validation can include:

  • Contact resistance
  • Temperature rise
  • Insertion/extraction force
  • Mating cycles
  • Vibration
  • Thermal cycling
  • Environmental testing

Common Connector Miniaturization Mistakes

MistakePotential Result
Reducing size without thermal analysisExcessive temperature rise
Reducing contact pitch excessivelyElectrical clearance problems
Undersized terminalHigher current density
Insufficient spring forceUnstable contact
Excessive spring forceHigh mating force
Ignoring tolerance stack-upMating problems
Weak housing structureMechanical failure
Poor seal designWater or dust ingress
Insufficient inspectionManufacturing variation

How FPIC Supports Connector Miniaturization

FPIC supports customized connector development with engineering capabilities covering:

✔ Contact system design

✔ Housing design

✔ Terminal stamping

✔ Precision injection molding

✔ Tolerance control

✔ Electrical testing

✔ Mechanical reliability testing

✔ CCD/visual inspection

✔ Automated assembly and packaging

For demanding automotive applications, FPIC’s connector manufacturing capabilities are supported by IATF 16949 quality management requirements.

Connector production can also incorporate controlled cleanliness practices aligned with VDA 19.1 / ISO 16232 requirements where applicable.

The engineering objective is to optimize connector size without sacrificing:

  • Electrical performance
  • Mechanical reliability
  • Manufacturing consistency
  • Service life

Final Thoughts

Connector miniaturization is one of the most important trends in modern electronics.

But reducing connector dimensions creates a chain of engineering challenges.

Smaller connectors require careful control of:

Contact Density + Electrical Clearance + Thermal Performance + Spring Force + Mechanical Strength + Manufacturing Tolerance

The best miniature connector is not simply the smallest possible connector.

It is the smallest connector that can reliably meet its electrical, mechanical, environmental, manufacturing, and lifecycle requirements.

Successful miniaturization therefore requires a system-level approach:

Define → Design → Simulate → Manufacture → Test → Validate

When size reduction is combined with disciplined engineering and manufacturing control, miniature connectors can deliver high-density performance without compromising reliability.


FAQ

What is connector miniaturization?

Connector miniaturization is the process of reducing connector size, contact pitch, height, or mounting footprint while maintaining required electrical and mechanical performance.

What is the biggest challenge in miniature connector design?

There is no single challenge. Contact density, electrical clearance, thermal management, mechanical strength, manufacturing tolerance, and assembly precision often become more difficult simultaneously.

Does a smaller connector support less current?

Not necessarily, but reducing terminal size and conductive area can increase current density and heat generation. Current capability must be evaluated based on the complete contact design and application conditions.

Why are manufacturing tolerances important for miniature connectors?

As connector features become smaller, the same dimensional variation can have a greater functional impact, especially on terminal alignment, mating, and contact performance.

How can miniature connectors maintain reliability?

Reliable miniature connectors require optimized contact geometry, suitable materials and plating, controlled tolerances, appropriate thermal design, precise manufacturing, and application-specific validation.


Need a Compact Connector for a Space-Constrained Application?

FPIC supports custom connector development from contact design and tooling through precision manufacturing, testing, and mass production.

Whether you need compact signal connectors, circular connectors, automotive connectors, or customized high-density solutions, our engineering team can help balance size, performance, reliability, and manufacturability.

Contact FPIC to discuss your miniature connector requirements.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    International testing framework for electrical and mechanical performance of connectors.
  2. USCAR Standards
    https://www.uscar.org/
    Automotive connector performance and validation resources.
  3. IPC Standards
    https://www.ipc.org/
    Industry standards and technical resources for electronic interconnection and manufacturing.
  4. IATF 16949
    https://www.iatfglobaloversight.org/
    Automotive quality management requirements for organizations in the automotive supply chain.
Connector Tolerance Control in Mass Production

A connector can meet its nominal drawing dimensions and still create problems during mass production if dimensional tolerances are not properly controlled.

Connector performance depends on multiple components working together:

  • Housing
  • Terminals
  • Seals
  • Locks
  • Contact interfaces
  • Mating features

Each component has its own dimensional variation.

When these variations accumulate, the final assembly can behave differently from the nominal design.

This is why tolerance control is not simply a drawing requirement.

It is a critical part of connector manufacturing quality.

Poor tolerance control can result in:

  • Difficult mating
  • Excessive insertion force
  • Loose connections
  • Contact instability
  • Seal leakage
  • Assembly interference
  • Poor interchangeability
  • Increased production scrap

For automotive, industrial, medical, energy storage, and other demanding applications, controlling dimensional variation from design through mass production is essential for consistent field performance.

Connector Tolerance Control in Mass Production


What Is Connector Tolerance Control?

Tolerance control defines the acceptable dimensional variation of connector components and ensures that manufacturing processes remain within those limits.

Typical controlled dimensions include:

  • Terminal position
  • Contact pitch
  • Housing dimensions
  • Locking features
  • Connector alignment
  • Seal compression
  • Mounting dimensions
  • Mating interfaces

For example, a connector may have a nominal terminal position specified on the drawing.

During manufacturing, the actual position will naturally vary within a defined tolerance.

The engineering challenge is ensuring that this variation does not negatively affect:

Mating + Electrical Contact + Mechanical Retention + Sealing


Why Nominal Dimensions Are Not Enough

One common mistake is designing around nominal dimensions without considering actual manufacturing variation.

Suppose two mating connector components each have dimensional tolerances.

Even if both are individually within specification, their combined variation may produce:

  • Excessive interference
  • Excessive clearance
  • Misalignment
  • Increased insertion force

This is known as tolerance stack-up.

Mass production makes this issue especially important because thousands or millions of parts may be produced.

A small dimensional issue that occurs only occasionally can become a significant quality problem at production scale.


1.Tolerance Stack-Up Can Affect Mating Performance

Connector mating requires several features to align correctly.

For example:

Housing → Guide Feature → Terminal → Contact Interface

Each feature contributes to the final position.

If multiple tolerances shift in the same direction, the accumulated variation can become significant.

Potential consequences include:

  • Difficult mating
  • Excessive insertion force
  • Connector misalignment
  • Terminal deformation
  • Housing interference

Engineers should therefore evaluate tolerance stack-up during the design phase.


2.Terminal Position Tolerance Is Critical

Terminal position directly affects electrical and mechanical performance.

If terminals are not positioned consistently:

  • Contact alignment may change
  • Mating force may vary
  • Contact wipe may become inconsistent
  • Adjacent terminals may have reduced clearance

This becomes particularly important for:

  • High-density connectors
  • Fine-pitch connectors
  • Multi-pin automotive connectors
  • Signal connectors

Precise terminal positioning helps maintain consistent contact behavior across production lots.


3.Housing Tolerance Affects Alignment

The connector housing provides the mechanical framework for the terminal system.

Important dimensions can include:

  • Terminal cavities
  • Guide rails
  • Keying features
  • Locking structures
  • Mating interfaces
  • Mounting holes

If housing dimensions vary excessively, the terminal system may not remain in the intended position.

This can affect:

  • Mating accuracy
  • Contact alignment
  • Connector retention
  • Assembly consistency

4.Contact Tolerance Affects Electrical Reliability

Electrical performance depends on stable contact geometry.

Small dimensional changes can influence:

  • Contact force
  • Contact area
  • Contact wipe
  • Contact resistance

For example, if a terminal beam is slightly outside its intended geometry, the resulting spring force may differ from the design target.

This can create variation in electrical performance between individual connectors.

Therefore:

Dimensional Control → Contact Geometry → Contact Force → Electrical Reliability


5.Seal Tolerance Affects Waterproofing

For sealed connectors, dimensional tolerance becomes even more important.

Sealing performance depends on controlled compression between:

  • Seal
  • Housing
  • Cable
  • Mating connector

Insufficient compression may cause leakage.

Excessive compression may cause:

  • High insertion force
  • Seal deformation
  • Assembly difficulty
  • Premature seal wear

Proper tolerance analysis helps ensure that the sealing system remains within its intended operating range.

This is especially important for:

  • Automotive connectors
  • Outdoor equipment
  • Industrial machinery
  • Agricultural equipment
  • IP67/IP68 applications

6.Locking Features Require Consistent Tolerances

Connector locks need to provide reliable retention while remaining practical for assembly and service.

If the locking geometry is inconsistent:

Too Tight

The operator may experience:

  • Difficult locking
  • High assembly force
  • Component deformation

Too Loose

Potential problems include:

  • Insufficient retention
  • Connector separation
  • Poor vibration resistance

Tolerance control helps maintain the intended balance between retention force and usability.


7.Tolerance Control Improves Assembly Consistency

Mass production requires thousands of assemblies to behave similarly.

If connector dimensions vary too much, operators may encounter:

  • Different insertion forces
  • Different locking forces
  • Different terminal positions
  • Different connector fit

This can increase:

  • Assembly time
  • Rework
  • Scrap
  • Production complaints

Consistent dimensional control improves manufacturing repeatability.


8.Tolerance Control Supports Interchangeability

OEM customers often expect components manufactured at different times to remain interchangeable.

For example:

  • Connector A from Lot 1
  • Connector B from Lot 2

should still mate correctly when both comply with the approved design.

This requires consistent control of critical dimensions.

Interchangeability is particularly important for:

  • Service replacement
  • Global manufacturing
  • Multiple production lines
  • Multiple suppliers

9.Critical-to-Function Dimensions Need More Attention

Not every connector dimension has the same impact on performance.

A practical approach is to identify:

Critical Dimensions

Dimensions directly affecting:

  • Contact performance
  • Mating
  • Sealing
  • Retention
  • Safety

Important Dimensions

Dimensions affecting:

  • Assembly
  • Positioning
  • Manufacturing consistency

General Dimensions

Dimensions with relatively low functional impact.

This allows engineering and quality teams to focus measurement resources where they create the greatest value.


10.Statistical Process Control Helps Maintain Tolerance

Mass production requires more than checking finished parts.

Manufacturing processes should be monitored continuously.

Common methods include:

  • SPC
  • Process capability analysis
  • Control charts
  • Sampling inspection
  • Automated dimensional inspection

Two commonly discussed capability indicators are:

Cp

and

Cpk

These help evaluate whether a manufacturing process can consistently produce parts within specification.

The specific acceptance criteria should be defined according to the product, drawing requirements, customer standards, and quality plan.


11.Measurement Equipment Matters

Tolerance control is only meaningful when measurement systems are appropriate.

Depending on the feature, manufacturers may use:

  • Calipers
  • Micrometers
  • Height gauges
  • Coordinate measuring machines
  • Optical measurement systems
  • Vision inspection
  • Go/No-Go gauges

For high-volume connector production, automated optical inspection can help monitor dimensional features efficiently.

Measurement systems should also be properly calibrated and maintained.


12.Mold and Stamping Processes Affect Connector Tolerances

Connector mass production often involves multiple manufacturing processes.

Injection Molding

Housing dimensions can be affected by:

  • Material shrinkage
  • Mold condition
  • Processing temperature
  • Injection parameters
  • Cooling conditions

Terminal Stamping

Terminal geometry can be influenced by:

  • Tool wear
  • Material thickness
  • Stamping accuracy
  • Progressive die condition

Assembly

Final connector dimensions can also be affected by:

  • Terminal insertion
  • Seal installation
  • Locking components
  • Assembly fixtures

Tolerance control therefore requires coordination across the entire manufacturing process.


13.Design for Manufacturability Starts With Tolerance Analysis

Tolerance control should begin before mass production.

During DFM review, engineers should ask:

  • Which dimensions are function-critical?
  • Which tolerances are realistically manufacturable?
  • Where can tolerance stack-up occur?
  • Which dimensions require automated inspection?
  • Can the process maintain the required capability?
  • Are overly tight tolerances adding unnecessary cost?

An unnecessarily tight tolerance can increase:

  • Tooling cost
  • Inspection requirements
  • Production cycle time
  • Scrap rate

The goal is not to make every dimension extremely precise.

The goal is to apply the right tolerance to the right feature.


14.Tolerance Control and Cost

Tolerance and cost are closely related.

In general, tighter tolerances may require:

  • More precise tooling
  • More process control
  • More inspection
  • Higher manufacturing cost

However, loose tolerances can create:

  • Higher defect rates
  • Assembly problems
  • Field failures
  • Customer complaints

Therefore, effective tolerance design balances:

Performance + Manufacturability + Cost

This is one of the most important principles of connector DFM.


Connector Tolerance Control Example

Consider a multi-pin connector with:

  • Housing
  • Terminals
  • Seals
  • Locking mechanism

The final mating condition depends on multiple dimensions.

A simplified tolerance chain might be:

Housing Position

↓

Terminal Position

↓

Contact Alignment

↓

Contact Force

↓

Electrical Reliability

If any critical dimension is poorly controlled, the final performance can shift.

This illustrates why connector tolerance control must be treated as a system-level engineering issue.


Common Connector Tolerance Control Mistakes

MistakePotential Result
Designing only around nominal dimensionsUnexpected production variation
Ignoring tolerance stack-upMating problems
Overly tight tolerancesHigher cost and scrap
Loose terminal positioningContact instability
Poor seal tolerance controlLeakage
Insufficient process monitoringLot-to-lot variation
Inadequate measurement systemsUndetected dimensional problems
Ignoring tooling wearGradual dimensional drift

Connector Tolerance Control Checklist

Before releasing a connector for mass production, engineering and quality teams should review:

Design

✔ Are critical dimensions identified?

✔ Has tolerance stack-up been analyzed?

✔ Are tolerances function-based?

Tooling

✔ Can the mold maintain the required dimensions?

✔ Is stamping-tool wear monitored?

Manufacturing

✔ Are critical dimensions measured?

✔ Are process parameters controlled?

✔ Is SPC applied where appropriate?

Assembly

✔ Are terminal positions consistent?

✔ Are seals correctly installed?

✔ Are locking features functioning consistently?

Validation

✔ Is mating force within the intended range?

✔ Is contact resistance stable?

✔ Is sealing performance validated?

✔ Is interchangeability verified?


How FPIC Controls Connector Quality in Mass Production

FPIC applies engineering and manufacturing controls throughout connector production.

Quality management can include:

✔ Dimensional inspection

✔ Terminal position control

✔ Injection molding process control

✔ Stamping process monitoring

✔ Assembly verification

✔ Electrical testing

✔ Visual inspection

✔ Reliability validation

For automotive connector production, FPIC operates under IATF 16949 quality requirements and applies controlled manufacturing processes to support consistent product performance.

For customers requiring demanding cleanliness requirements, mass production can also be managed in accordance with VDA 19.1 / ISO 16232 practices where applicable.

The objective is not simply to produce connectors within drawing dimensions.

It is to maintain consistent performance across production batches.


Final Thoughts

Connector tolerance control is one of the foundations of reliable mass production.

A connector is a system of interacting components, and small dimensional variations can influence:

  • Mating
  • Contact force
  • Contact resistance
  • Sealing
  • Retention
  • Assembly consistency
  • Interchangeability

Effective tolerance engineering does not mean making every dimension as tight as possible.

It means identifying the dimensions that matter most and controlling them with the right manufacturing and inspection methods.

The best connector designs balance:

Function + Tolerance + Process Capability + Cost

When these elements are aligned from the beginning, manufacturers can achieve more consistent production and OEM customers can gain greater confidence in connector performance.


FAQ

Why is tolerance control important in connector manufacturing?

Tolerance control ensures that connector components consistently fit, mate, seal, and maintain electrical performance throughout mass production.

What is connector tolerance stack-up?

Tolerance stack-up is the cumulative effect of dimensional variations from multiple components or features that contribute to a final functional dimension.

Does tighter tolerance always mean better connector quality?

No. Excessively tight tolerances can increase manufacturing cost and scrap without providing additional functional benefits. Tolerances should be based on actual performance requirements.

Which connector dimensions are most critical?

Terminal position, contact geometry, mating features, locking structures, sealing interfaces, and other dimensions directly affecting electrical, mechanical, or sealing performance are typically critical.

How is connector dimensional tolerance controlled during mass production?

Manufacturers can use calibrated measurement equipment, automated inspection, SPC, process capability analysis, tooling control, and defined quality control plans.


Looking for Consistent Connector Quality in Mass Production?

FPIC supports OEM customers with connector design, tooling, precision manufacturing, assembly, testing, and quality control.

From DFM and tolerance analysis to mass production and inspection, our engineering team focuses on consistent connector performance and manufacturing reliability.

Contact FPIC to discuss your custom connector project.


Resources

  1. IATF 16949 – Automotive Quality Management Systems
    https://www.iatfglobaloversight.org/
    Quality management framework widely used across the automotive supply chain.
  2. ISO 9001 – Quality Management Systems
    https://www.iso.org/iso-9001-quality-management.html
    International framework for quality management and process control.
  3. ISO 16232 / VDA 19.1 – Technical Cleanliness
    https://www.iso.org/
    Standards and practices for technical cleanliness in automotive components.
  4. AIAG Core Tools
    https://www.aiag.org/
    Industry resources covering APQP, PPAP, FMEA, MSA, SPC, and related quality methodologies.
Connector Spring Force Design Overview

Inside every reliable connector is a carefully engineered contact system.

While connector housings provide mechanical protection, the spring force generated by the contact structure determines whether electrical connections remain stable during operation.

The correct spring force helps maintain:

  • Stable electrical contact
  • Low contact resistance
  • Resistance against vibration
  • Long mating cycle life

However, designing connector spring force is a balance.

Too little force may cause intermittent connections, while excessive force can increase insertion force and accelerate contact wear.

For automotive electronics, industrial automation, robotics, energy storage systems, and other demanding applications, spring force design is a key factor in connector reliability.

A reliable connector does not simply make contact.

It maintains consistent contact pressure throughout its service life.

Connector Spring Force Design Overview


What Is Spring Force in Connector Contacts?

Spring force refers to the mechanical force generated by the elastic deformation of a connector contact element after mating.

When two contacts are connected:

1.The male and female contacts engage.

2.The contact element deforms elastically.

3.The spring force pushes the surfaces together.

4.Stable electrical contact is maintained.

This force creates the necessary contact pressure for reliable current transmission.

Common spring structures include:

  • Cantilever beams
  • Dual-beam contacts
  • Leaf springs
  • Cage-style contacts
  • Elastic socket structures

Each design provides different performance characteristics.


Why Spring Force Matters in Connector Reliability

The contact interface is constantly exposed to mechanical and environmental stress.

A properly designed spring force helps maintain performance under:

  • Vibration
  • Shock
  • Thermal expansion
  • Repeated mating cycles
  • Mechanical movement

Without sufficient spring force, connectors may experience:

  • Increased contact resistance
  • Signal interruption
  • Electrical arcing
  • Local heating
  • Premature failure

1.Spring Force Maintains Stable Electrical Contact

Electrical current flows through the actual contact points between mating surfaces.

The spring force determines how tightly these surfaces remain connected.

Proper contact pressure helps:

✔ Increase effective contact area

✔ Reduce resistance variation

✔ Improve current stability

✔ Prevent micro-movement


Low Spring Force Problems

Insufficient spring force can cause:

Contact Interruption

Small movements caused by vibration may temporarily break the electrical connection.

Increased Resistance

Poor contact pressure creates unstable electrical pathways.

Fretting Corrosion

Micro-motion between metal surfaces may generate wear particles and oxidation.


Excessive Spring Force Problems

Too much force can create:

High Insertion Force

Users may experience difficulty during mating.

Faster Contact Wear

Higher mechanical stress accelerates surface damage.

Reduced Mating Life

Repeated cycles may permanently deform the contact structure.


2.Spring Force and Contact Resistance Relationship

Contact resistance is directly affected by contact pressure.

Higher contact pressure generally improves electrical performance by creating more stable metal-to-metal contact.

However, the relationship is not unlimited.

After reaching an optimal range, increasing force provides fewer benefits while increasing mechanical stress.

Connector engineers must optimize:

Contact Force + Material Elasticity + Surface Condition

to achieve long-term reliability.


3.Contact Spring Design Affects Connector Durability

Different contact structures generate spring force in different ways.


Cantilever Beam Contacts

A cantilever beam uses a flexible metal arm to create contact pressure.

Advantages:

✔ Simple structure

✔ Cost-effective manufacturing

✔ Good electrical performance

Common applications:

  • PCB connectors
  • Automotive connectors
  • General electronic connectors

Dual Beam Contacts

Dual beam designs use two independent contact points.

Advantages:

✔ Improved redundancy

✔ Better vibration resistance

✔ More stable connection

If one contact point experiences contamination or wear, the second contact can help maintain electrical continuity.


Leaf Spring Contacts

Leaf spring structures provide controlled elastic force.

Advantages:

✔ Stable pressure distribution

✔ Good mechanical durability

✔ Suitable for high-cycle applications


4.Spring Force Helps Improve Vibration Resistance

Many connectors operate in environments with continuous vibration.

Examples:

  • Vehicles
  • Robots
  • Industrial machinery
  • Outdoor equipment

Vibration can cause:

  • Contact separation
  • Fretting wear
  • Signal interruption

Proper spring force helps maintain contact pressure during mechanical movement.

This is especially important for:

  • Automotive connectors
  • Circular connectors
  • Industrial Ethernet connectors

5.Spring Force Influences Mating Cycle Life

Every connector mating cycle creates mechanical stress.

During repeated mating:

  • Contact surfaces slide
  • Spring elements deform
  • Plating layers experience wear

A well-designed spring system maintains:

✔ Stable force over time

✔ Controlled contact wear

✔ Reliable electrical performance

For connectors requiring thousands of mating cycles, spring force consistency is critical.


6.Material Selection Determines Spring Performance

Spring force depends heavily on contact material properties.

Important factors include:

  • Elastic strength
  • Fatigue resistance
  • Conductivity
  • Corrosion resistance

Common contact materials include:

Copper Alloys

Advantages:

✔ Good conductivity

✔ Balanced mechanical performance


Phosphor Bronze

Advantages:

✔ Excellent spring properties

✔ Good fatigue resistance

Commonly used for:

  • High-cycle connectors
  • Signal connectors

Beryllium Copper

Advantages:

✔ High elasticity

✔ Excellent mechanical durability

Used in applications requiring:

  • High reliability
  • Long service life

7.Spring Force Must Be Combined with Contact Plating

Spring force alone cannot guarantee reliability.

The contact surface also requires proper plating.


Gold Plating

Benefits:

✔ Low contact resistance

✔ Excellent corrosion resistance

✔ Long mating life

Suitable for:

  • Signal connectors
  • Precision applications

Tin Plating

Benefits:

✔ Cost-effective

✔ Suitable for many power applications

Suitable for:

  • General electrical connectors

8.Testing Spring Force and Contact Reliability

Connector manufacturers validate spring performance through testing.

Common tests include:


Insertion and Extraction Force Testing

Measures:

  • Required mating force
  • User operation performance
  • Mechanical consistency

Contact Resistance Testing

Evaluates:

  • Electrical stability
  • Contact performance

Mating Cycle Testing

Verifies:

  • Contact durability
  • Spring performance after repeated use

Vibration Testing

Evaluates:

  • Contact stability under mechanical stress

9.Spring Force Design Requirements by Application

Different industries require different spring force characteristics.

ApplicationSpring Force Requirements
Automotive ConnectorVibration resistance, stable contact pressure
Robotics ConnectorHigh cycle durability, mechanical stability
Industrial ConnectorReliable performance in harsh environments
Energy Storage ConnectorHigh current stability, thermal reliability
Medical ConnectorStable connection and low failure risk

Common Spring Force Design Mistakes

Design IssuePotential Failure
Insufficient spring forceIntermittent connection
Excessive spring forceHigh insertion force
Poor material selectionLoss of elasticity
Uneven pressure distributionContact instability
Incorrect plating combinationIncreased resistance

How FPIC Optimizes Connector Contact Reliability

FPIC focuses on connector reliability through:

✔ Precision contact structure design

✔ Optimized spring force control

✔ Material and plating selection

✔ Contact resistance testing

✔ Mechanical reliability validation

Connector designs are evaluated to ensure:

  • Stable electrical performance
  • Reliable mating cycles
  • Consistent production quality

Through engineering optimization and manufacturing control, FPIC supports customers with reliable connector solutions for industrial and automotive applications.


Final Thoughts

Spring force is one of the most important elements in connector contact reliability.

A successful connector design requires the right balance between:

  • Contact pressure
  • Electrical performance
  • Mechanical durability
  • User operation

Too little force creates unstable connections.

Too much force reduces usability and service life.

The best connector designs achieve controlled spring force that maintains reliable performance throughout thousands of operating cycles.

A connector is not reliable because the contacts touch.

It is reliable because the contacts remain stable.


FAQ

What is spring force in a connector?

Spring force is the mechanical force generated by the elastic deformation of connector contacts after mating.

Why is spring force important for connector reliability?

It maintains contact pressure, reduces resistance variation, and improves resistance to vibration and mechanical stress.

Can higher spring force improve connector performance?

Not always. Excessive force can increase wear and reduce mating cycle life.

How is connector spring force tested?

Manufacturers evaluate spring performance through insertion force, extraction force, contact resistance, mating cycle, and vibration tests.

What materials are commonly used for connector spring contacts?

Copper alloys, phosphor bronze, and beryllium copper are commonly used due to their electrical and elastic properties.


Need Reliable Connector Contact Design?

FPIC provides custom connector solutions with expertise in contact structure design, spring force optimization, material selection, and reliability testing.

From prototype development to mass production, FPIC helps OEM customers create connectors designed for long-term performance.

Contact FPIC today to discuss your connector project.


Resources

1.IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
https://www.iec.ch/

Connector testing methods covering mechanical and electrical performance evaluation.

2.EIA-364 Connector Test Standards
https://www.eia-global.org/

Industry standards for connector reliability and performance testing.

3.USCAR Connector Performance Standards
https://www.uscar.org/

Automotive connector performance requirements and validation guidelines.

Connector Reliability Overview

A connector is only as reliable as its contact system.

Although the external housing provides protection and mechanical support, the actual electrical connection happens at the contact interface.

The design of this small area determines whether a connector can maintain stable performance under:

  • High current loads
  • Vibration
  • Temperature changes
  • Repeated mating cycles
  • Harsh operating environments

For applications such as automotive electronics, industrial automation, robotics, energy storage systems, and medical equipment, contact geometry plays a critical role in connector reliability.

A well-designed connector does not simply make contact.

It maintains consistent electrical and mechanical performance throughout its service life.

Connector Reliability Overview


What Is Connector Contact Geometry?

Contact geometry refers to the physical design of the connector contact interface.

It includes:

  • Contact shape
  • Contact beam structure
  • Contact area
  • Contact engagement position
  • Contact pressure distribution
  • Wiping action during mating

The goal of contact geometry design is to achieve the right balance between:

  • Electrical conductivity
  • Mechanical strength
  • Contact stability
  • Mating durability

Different applications require different contact structures.

A high-current power connector and a high-speed signal connector may use completely different contact geometries because their performance requirements are different.


Why Contact Geometry Is Critical for Connector Reliability

When two connector contacts mate, several physical factors determine connection quality.

A reliable contact interface must provide:

Stable Electrical Path

Ensuring current can flow efficiently with minimal resistance.

Proper Contact Force

Maintaining connection stability without excessive mechanical stress.

Controlled Wear

Allowing repeated mating without rapid degradation.

Resistance to Environmental Stress

Maintaining performance against:

  • Vibration
  • Shock
  • Temperature variation
  • Corrosion

Poor contact geometry can result in:

  • Increased contact resistance
  • Intermittent electrical connection
  • Signal interruption
  • Excessive heat generation
  • Premature connector failure

1.Contact Shape Determines Connection Performance

The shape of the contact element directly affects current transmission and mechanical stability.

Common contact structures include:


Pin and Socket Contacts

Pin and socket designs are widely used in circular connectors and industrial connectors.

Advantages:

✔ Reliable alignment

✔ Stable contact interface

✔ Good environmental adaptability

The socket contact usually uses spring structures to maintain contact pressure around the pin.

This design helps compensate for:

  • Manufacturing tolerance
  • Vibration
  • Mechanical movement

Blade Contacts

Blade contacts provide a larger conductive path.

Advantages:

✔ High current capability

✔ Simple structure

✔ Good mechanical strength

They are commonly used in:

  • Power connectors
  • Automotive applications
  • Industrial equipment

Spring Contacts

Spring-based contacts use elastic deformation to maintain continuous pressure.

Advantages:

✔ Improved vibration resistance

✔ Stable contact force

✔ Longer service life

They are suitable for applications requiring frequent mating cycles.


2.Contact Force Affects Reliability and Mating Performance

Contact force is one of the most important design parameters.

The correct contact force ensures:

  • Stable electrical connection
  • Low contact resistance
  • Resistance to vibration

However, both insufficient and excessive force can create problems.


Too Low Contact Force

Potential issues:

  • Increased electrical resistance
  • Intermittent connection
  • Signal instability

Low contact force may allow micro-movement between contacts, causing electrical degradation over time.


Too High Contact Force

Potential issues:

  • Higher insertion force
  • Increased contact wear
  • Reduced mating cycles

A good connector design balances:

Contact Reliability + User Operation + Service Life


3.Contact Area Influences Current Flow and Heat Generation

The contact interface determines how efficiently electrical current transfers between mating components.

A well-designed contact area helps:

  • Reduce current concentration
  • Lower resistance
  • Minimize heat generation

However, contact area alone does not determine performance.

Engineers must also consider:

  • Contact pressure
  • Surface condition
  • Material properties
  • Contact alignment

A larger contact surface without proper pressure control may not provide better reliability.


4.Wiping Action Helps Maintain Clean Contact Surfaces

Many connector designs include wiping action during mating.

During insertion, the contact surfaces slide against each other.

This movement helps remove:

  • Dust particles
  • Surface oxidation
  • Minor contamination

Benefits include:

✔ Improved electrical stability

✔ Reduced contact resistance variation

✔ Better long-term reliability

Wiping action is especially important for:

  • Outdoor equipment
  • Industrial automation
  • High-cycle connectors

5.Contact Geometry Determines Mating Cycle Life

Every mating cycle creates mechanical stress on contacts.

Repeated connection and disconnection can cause:

  • Surface wear
  • Loss of contact force
  • Material deformation

A reliable contact design considers:

Contact Elasticity

Maintains pressure after repeated use.

Wear Resistance

Reduces surface damage.

Mechanical Stability

Prevents deformation during operation.

For connectors requiring thousands of mating cycles, optimized contact geometry is essential.


6.Alignment Design Prevents Contact Damage

Even a well-designed contact can fail if alignment is poor.

Incorrect alignment may cause:

  • Bent pins
  • Uneven contact pressure
  • Partial engagement
  • Contact damage

Reliable connector systems often include:

  • Polarization features
  • Guide structures
  • Mechanical keys
  • Alignment sleeves

These features ensure correct mating and protect the contact system.


7.Contact Geometry Influences Thermal Reliability

Electrical resistance generates heat.

When contact geometry is poor, current may concentrate in small areas, creating:

  • Hot spots
  • Temperature rise
  • Contact degradation

A properly designed contact structure improves:

  • Current distribution
  • Heat dissipation
  • Long-term stability

This is especially important for:

  • High-current connectors
  • Battery systems
  • Industrial power equipment

8.Contact Geometry Must Match Application Requirements

Different industries require different contact solutions.

ApplicationContact Design Priorities
AutomotiveVibration resistance, durability, stable contact force
RoboticsHigh mating cycles, mechanical stability
Industrial AutomationEnvironmental protection, reliability
Energy StorageHigh current capability, thermal control
Medical EquipmentStable signal transmission, safety

Connector design should always begin with understanding the actual application environment.


9.Contact Material and Plating Work Together with Geometry

Contact geometry is only one part of connector reliability.

Material selection and surface treatment are equally important.


Contact Material

Common materials include:

  • Copper alloys
  • Brass
  • Phosphor bronze

Important characteristics:

  • Electrical conductivity
  • Spring performance
  • Mechanical strength

Contact Plating

Gold Plating

Advantages:

✔ Excellent corrosion resistance

✔ Low contact resistance

✔ Long mating life

Suitable for:

  • Signal connectors
  • Precision applications

Tin Plating

Advantages:

✔ Cost-effective

✔ Suitable for many power applications

Suitable for:

  • General electrical connections

10.How FPIC Optimizes Connector Contact Design

FPIC focuses on connector reliability through:

Precision Contact Engineering

Including:

  • Contact structure optimization
  • Contact force control
  • Mechanical tolerance management

Material and Plating Selection

Considering:

  • Current requirements
  • Environment
  • Mating cycles

Reliability Testing

Including:

  • Contact resistance testing
  • Insertion and extraction force testing
  • Mating cycle evaluation
  • Environmental testing

Through engineering optimization and manufacturing control, FPIC helps customers develop reliable connector solutions for demanding applications.


Common Contact Geometry Design Mistakes

Design MistakePotential Result
Incorrect contact forceIntermittent connection
Poor alignment designContact damage
Insufficient contact areaHeat generation
Weak wiping actionIncreased resistance
Improper material selectionReduced service life

Contact Geometry Design Checklist

Before finalizing a connector design, engineers should evaluate:

✔ Is the contact force within the correct range?

✔ Can the contact maintain stability after repeated mating?

✔ Is current distribution optimized?

✔ Does the geometry support the application environment?

✔ Are material and plating choices appropriate?

✔ Has the design been validated through testing?


Final Thoughts

Contact geometry is one of the most important factors influencing connector reliability.

A reliable connector requires careful optimization of:

  • Contact shape
  • Contact force
  • Contact area
  • Alignment
  • Material selection
  • Surface treatment

The contact interface may be small, but it determines the overall performance of the connector system.

A connector is not reliable because it connects once.

It is reliable because it maintains a stable connection thousands of times under real-world conditions.


FAQ

What is contact geometry in connectors?

Contact geometry refers to the physical structure and design of the electrical contact interface, including shape, contact area, and pressure distribution.

How does contact geometry affect connector reliability?

It affects electrical resistance, current flow, mating durability, vibration resistance, and long-term performance.

Why is contact force important in connector design?

Proper contact force ensures stable electrical connection while balancing insertion force and wear.

Can contact geometry affect connector temperature?

Yes. Poor contact geometry can increase resistance and create localized heat generation.

How do engineers improve connector contact reliability?

Engineers optimize contact structure, materials, plating, alignment, and validate performance through reliability testing.


Need a Reliable Custom Connector Solution?

FPIC provides custom connector design and manufacturing services with expertise in contact engineering, material selection, reliability testing, and mass production.

From concept development to final production, FPIC helps OEM customers build connectors designed for long-term performance.

Contact FPIC today to discuss your connector requirements.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Connector testing methods covering electrical and mechanical performance evaluation.
  2. EIA-364 Connector Test Standards
    https://www.eia-global.org/
    Industry test standards for connector reliability and performance validation.
  3. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry acceptance criteria for cable and wire harness assemblies.
Connector Material Selection Overview

Selecting the right connector is not only about choosing the correct pin count, current rating, or mating interface.

The materials used inside a connector directly influence its reliability, durability, and performance throughout the product lifecycle.

A connector operating in a factory automation system, outdoor equipment, medical device, or energy storage application may face completely different challenges, including:

  • High temperature
  • Vibration
  • Moisture exposure
  • Chemical contamination
  • Mechanical stress
  • Frequent mating cycles

To achieve stable performance, engineers must carefully evaluate three major material categories:

  • Housing resin
  • Seal materials
  • Contact alloys and plating

Each material plays a different role in protecting electrical performance and mechanical reliability.

Connector Material Selection Overview


Why Connector Material Selection Matters

A connector is a combination of mechanical, electrical, and environmental protection components.

Poor material selection can lead to:

  • Cracked connector housings
  • Seal degradation
  • Increased contact resistance
  • Corrosion
  • Signal instability
  • Reduced mating life

For high-reliability applications, connector materials must match the actual operating environment rather than only meeting basic specifications.

A connector designed for indoor electronics may not perform reliably in outdoor or industrial conditions.


1.Connector Housing Resin Selection

The connector housing provides mechanical support and protects internal contacts.

Important properties include:

  • Mechanical strength
  • Temperature resistance
  • Chemical resistance
  • Dimensional stability
  • Flame retardancy
  • Insulation performance

Common housing materials include:


PA (Polyamide / Nylon)

PA is widely used for industrial and automotive connectors.

Advantages:

✔ Good mechanical strength

✔ Good wear resistance

✔ Cost-effective

✔ Suitable for many general applications

Limitations:

  • Absorbs moisture
  • Dimensional changes may occur in humid environments

Typical applications:

  • Automotive connectors
  • Industrial equipment
  • Wire harness systems

PBT (Polybutylene Terephthalate)

PBT is commonly used where dimensional stability and electrical insulation are important.

Advantages:

✔ Low moisture absorption

✔ Good chemical resistance

✔ Stable dimensions

✔ Good electrical performance

Typical applications:

  • Automotive electronics
  • Industrial connectors
  • Control systems

PPS (Polyphenylene Sulfide)

PPS is selected for demanding environments.

Advantages:

✔ Excellent temperature resistance

✔ High dimensional stability

✔ Strong chemical resistance

✔ Low moisture absorption

Typical applications:

  • High-temperature equipment
  • Industrial machinery
  • Automotive engine environments

PC (Polycarbonate)

PC provides high impact resistance.

Advantages:

✔ Excellent toughness

✔ Transparent options available

✔ Good impact strength

Typical applications:

  • Protective housings
  • Specialized electronic connectors

2.Connector Seal Material Selection

For outdoor and harsh environments, sealing materials are critical.

Seals protect connectors from:

  • Water
  • Dust
  • Oil
  • Chemicals
  • Humidity

Common sealing materials include:


Silicone Rubber

Advantages:

✔ Wide temperature range

✔ Excellent flexibility

✔ Long-term elasticity

✔ Good weather resistance

Applications:

  • Outdoor connectors
  • Medical equipment
  • High-temperature environments

EPDM Rubber

Advantages:

✔ Excellent water resistance

✔ Good ozone resistance

✔ Good weather durability

Applications:

  • Automotive
  • Outdoor industrial equipment

Fluorosilicone

Advantages:

✔ Chemical resistance

✔ Fuel and oil resistance

✔ Wide temperature capability

Applications:

  • Aerospace
  • Automotive
  • Harsh chemical environments

3.Contact Alloy Selection

The contact system determines electrical performance.

A contact must provide:

  • Stable conductivity
  • Low contact resistance
  • Mechanical durability
  • Corrosion resistance

Common contact materials include:


Copper Alloys

Copper alloys are widely used because they provide:

✔ Good electrical conductivity

✔ Good mechanical strength

✔ Reliable spring characteristics

Common materials:

  • Brass
  • Phosphor bronze
  • Copper alloy

Phosphor Bronze

Advantages:

✔ Excellent spring performance

✔ Good fatigue resistance

✔ Stable contact force

Applications:

  • High mating cycle connectors
  • Industrial connectors

Beryllium Copper

Beryllium copper is used for high-performance contact systems.

Advantages:

✔ Excellent elasticity

✔ High contact force retention

✔ Excellent fatigue resistance

Applications:

  • Precision connectors
  • High-cycle applications

4.Contact Plating Selection

The base alloy is only part of the contact performance.

Surface plating affects:

  • Contact resistance
  • Corrosion resistance
  • Mating cycle life

Common plating options:


Gold Plating

Advantages:

✔ Excellent corrosion resistance

✔ Stable electrical performance

✔ Suitable for high mating cycles

Applications:

  • Medical equipment
  • Communication systems
  • Precision electronics

Tin Plating

Advantages:

✔ Cost-effective

✔ Good solderability

✔ Suitable for many power applications

Limitations:

  • Lower corrosion resistance compared with gold

Applications:

  • General industrial connections
  • Power terminals

5.Matching Materials to Application Environments

Different applications require different material combinations.

Different applications require different material combinations.

ApplicationHousingSealContact
Industrial AutomationPA/PBTSilicone/EPDMCopper Alloy + Plating
Outdoor EquipmentPBT/PPSEPDM/SiliconeCorrosion-resistant contacts
Medical EquipmentEngineering PlasticSiliconeGold-plated contacts
RoboticsPBT/PAFlexible SealsHigh-cycle contact alloys
Energy StorageHigh-strength ResinHigh-temperature SealHigh-current Copper Alloy

Material selection should always consider:

  • Temperature range
  • Current load
  • Mechanical movement
  • Environmental exposure
  • Required service life

6.Material Selection and Connector Reliability Testing

Material selection should be supported by validation testing.

Common tests include:

Environmental Testing

  • Temperature cycling
  • Humidity testing
  • Salt spray testing

Mechanical Testing

  • Insertion and extraction force
  • Mating cycle testing
  • Vibration testing

Electrical Testing

  • Contact resistance testing
  • Insulation resistance
  • High-voltage testing

Testing confirms that the selected materials can perform reliably under real operating conditions.


How FPIC Approaches Connector Material Selection

FPIC develops and manufactures connector solutions for industrial automation, energy storage, automotive, robotics, and other demanding applications.

Our connector designs consider:

  • Housing material performance
  • Contact reliability
  • Environmental requirements
  • Mechanical durability
  • Application-specific testing

By combining material selection with engineering validation, FPIC helps customers achieve reliable connector performance from prototype development through mass production.


Final Thoughts

Connector reliability begins with material selection.

The housing resin protects the structure, sealing materials prevent environmental damage, and contact alloys ensure stable electrical performance.

Choosing the right combination requires understanding the application’s:

  • Temperature
  • Environment
  • Electrical requirements
  • Mechanical stress
  • Service life expectations

For engineers and OEM buyers, evaluating connector materials early in the design process can significantly reduce field failures and improve long-term system reliability.

The best connector is not only designed correctly—it is built with the right materials.


FAQ

What is the most important material in a connector?

There is no single most important material. Housing resin, seals, and contact materials work together to determine connector performance.

Why does connector housing material matter?

The housing provides mechanical protection, insulation, and environmental resistance for internal contacts.

What is the difference between gold and tin contacts?

Gold provides better corrosion resistance and longer mating life, while tin is more cost-effective for many general applications.

Which seal material is best for outdoor connectors?

Silicone and EPDM are commonly used because of their weather resistance and durability.

How do engineers select connector materials?

Engineers evaluate temperature, environment, electrical load, mating cycles, mechanical stress, and reliability requirements.


Need a Connector Designed for Your Application?

FPIC provides customized connector solutions for industrial automation, robotics, energy storage, automotive, and other demanding applications.

From material selection and connector design to testing and mass production, FPIC helps customers build reliable interconnection systems.

Contact FPIC today to discuss your connector requirements.


Resources

  1. IEC 60529 – Degrees of Protection Provided by Enclosures (IP Code)
    https://www.iec.ch/
    International standard defining protection levels against dust and water ingress.
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry standard covering cable assembly workmanship and acceptance criteria.
  3. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Provides test methods for connector electrical and mechanical performance.
  4. UL Solutions – Connector and Electrical Component Safety
    https://www.ul.com/
    Technical resources related to electrical component safety and reliability.
  5. ISO 16750 – Road Vehicles Environmental Conditions and Testing
    https://www.iso.org/
    Environmental testing guidance for automotive electrical and electronic components.