Tag Archive for: circular connector

Connector Shielding Design for EMI Protection

As industrial equipment becomes faster, more compact, and more electronically integrated, electromagnetic interference (EMI) is becoming a more important design challenge. High-speed communication, servo drives, switching power supplies, motors, inverters, sensors, and control systems may all operate within the same equipment.

A connector is often treated as a simple interface between a cable and a device. However, in an EMC-sensitive system, the connector is also part of the shielding path.

A cable may have an effective shield, but if that shield is poorly terminated at the connector, EMI can still enter or leave the system through the connection point. This is why connector shielding should be considered as part of the complete cable and enclosure design rather than as an isolated connector feature.

This article explains the key principles of connector shielding design, including shield termination, 360° shielding, grounding, backshell selection, mechanical integration, and validation.

Connector Shielding Design for EMI Protection


Why Connector Shielding Matters for EMI Protection

EMI can affect electronic systems through conducted coupling, capacitive or inductive coupling, and radiated electromagnetic fields. Shielded cables are commonly used to reduce the exposure of signal conductors to external interference and to limit unwanted radiation from the cable.

However, the cable shield is only one part of the overall protection system.

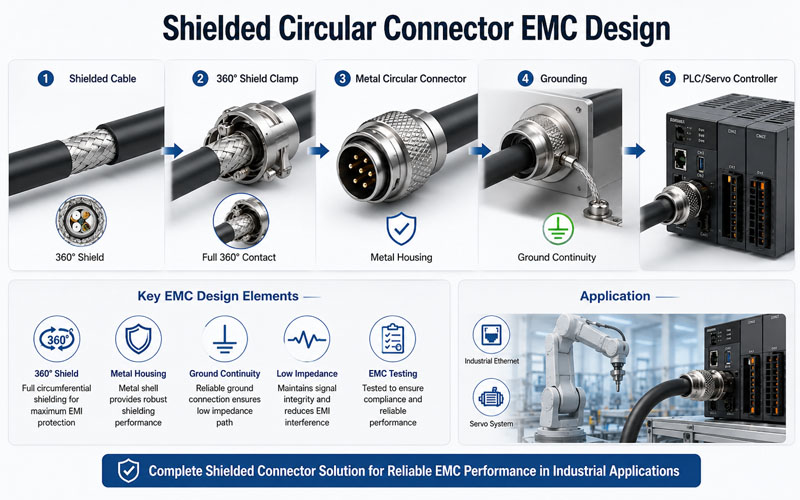
A typical shielded connection may include:

  • Shielded cable
  • Connector shell
  • Shield termination
  • Backshell
  • Equipment enclosure
  • Ground or chassis connection

If one section has significantly higher impedance or poor mechanical contact, the effectiveness of the entire shielding system can be reduced.

TE Connectivity notes that shield termination at the backshell can provide a grounding path and that the complete circumference of a cable shield can be connected to the backshell to create a more continuous shielding structure.

This leads to an important design principle:

EMI protection depends on the continuity of the entire shielding path, not simply on whether a cable is labeled “shielded.”


Connector Shielding Starts With the Complete EMC Architecture

Connector selection should not happen independently from the cable, PCB, enclosure, and grounding strategy.

Before selecting a shielded connector, engineers should understand:

  • operating frequency range
  • signal type and data rate
  • cable construction
  • shielding method
  • enclosure material
  • grounding architecture
  • environmental conditions
  • vibration and mechanical requirements

A connector that performs well in one application may not provide the same EMC performance in another system.

For example, a high-speed industrial Ethernet application may have very different shielding requirements from a low-frequency sensor cable or a motor power connection.

Therefore, connector shielding should be designed as a complete signal path.


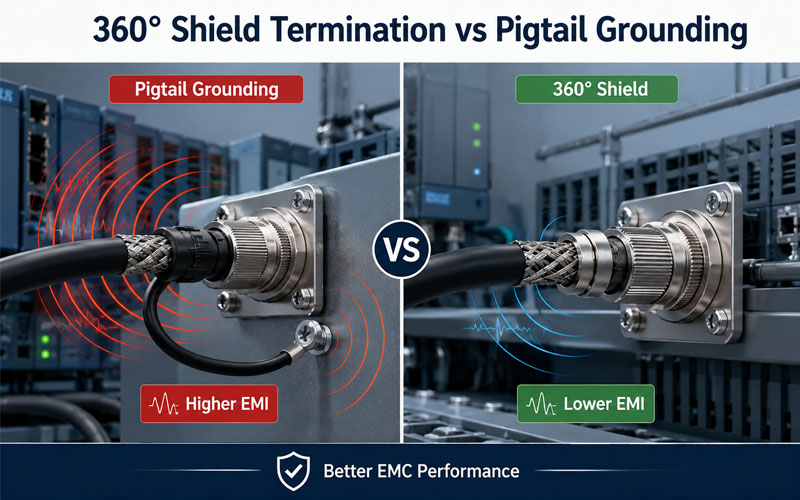
360° Shield Termination vs Partial Shield Termination

One of the most important considerations in connector shielding is how the cable shield is terminated.

A partial shield connection may create gaps or discontinuities around the connector interface. At higher frequencies, these discontinuities can become increasingly important because the shielding system must control electromagnetic fields rather than simply provide a low-frequency electrical connection.

A 360° termination connects the cable shield around its circumference to the connector shell or backshell.

This approach can provide a more continuous shielding path between the cable and connector.

TE Connectivity provides several connector and backshell solutions using 360° screen termination for EMI/RFI applications.

Why 360° Termination Is Important

A properly designed 360° termination can help:

  • reduce shielding discontinuities
  • maintain shield continuity through the connector
  • reduce unwanted radiation
  • improve immunity against external interference
  • support more consistent EMC performance

The exact termination method still needs to be selected according to cable construction, frequency range, environmental requirements, and mechanical constraints.

360° termination should therefore be considered a design strategy rather than a universal solution for every application.


The Connector Shell Is Part of the Shielding Path

For a shielded connector system, the metallic shell should not be treated simply as a mechanical housing.

It can form part of the electromagnetic shielding path between:

Cable Shield → Connector Shell → Equipment Interface → Chassis / Enclosure

Any discontinuity within this path can reduce the effectiveness of the overall shielding structure.

Important design considerations include:

  • conductive shell material
  • shell-to-shell contact
  • plating compatibility
  • contact pressure
  • surface contamination
  • connector mating stability
  • connection to the equipment chassis

For industrial applications exposed to vibration, the shielding interface must also remain electrically stable over the intended service life.

A connector may initially show good electrical continuity but lose performance if mechanical movement causes the shielding contact to degrade.


Backshell Design Has Multiple Functions

The backshell is another important component in connector shielding design.

Depending on the application, a backshell may provide:

  • EMI/RFI shield termination
  • cable strain relief
  • mechanical cable support
  • environmental sealing
  • cable routing control
  • connection between cable shield and connector shell

TE Connectivity describes backshells as components that can combine strain relief, EMI shielding, and environmental protection.

This makes backshell selection especially important for industrial equipment, robotics, servo systems, and other applications where cables experience vibration or repeated movement.

Select the Backshell Based on the Cable

A common design mistake is selecting a connector first and treating the backshell as an accessory afterward.

The backshell should be evaluated together with:

  • cable diameter
  • braid construction
  • foil or braid shield
  • number of shield layers
  • bend radius
  • required strain relief
  • sealing requirements
  • installation process

For example, a braided cable may require a different shield termination mechanism from a foil-shielded cable.


Shield Termination Must Balance EMI and Mechanical Reliability

A shielding connection is not useful if it cannot survive the mechanical environment.

Industrial harnesses may experience:

  • continuous vibration
  • repeated bending
  • torsion
  • temperature cycling
  • connector mating and unmating
  • cable pulling forces

The shield termination must therefore maintain electrical continuity while also providing sufficient mechanical retention.

A good design should prevent the cable shield from carrying mechanical loads that should instead be handled by the strain-relief system.

This distinction is important:

Shield termination provides electrical continuity; strain relief manages mechanical forces.

Combining these functions without proper design can create long-term reliability problems.


Grounding Strategy Is Critical

A shielded connector cannot provide effective EMI protection without a suitable grounding or chassis strategy.

The design team should determine where the shield should connect and how the shielding structure interacts with the system enclosure.

Possible considerations include:

  • chassis grounding
  • equipment enclosure bonding
  • connector shell grounding
  • cable shield termination
  • PCB ground connection
  • single-point or multi-point grounding strategy depending on frequency and system architecture

There is no universal grounding configuration for every application. The correct approach depends on the system topology, operating frequency, EMC requirements, and intended current paths.

For high-frequency systems, maintaining a low-impedance shielding path is often more important than simply achieving a low DC resistance measurement.


Avoid Pigtail Shield Termination When High-Frequency Performance Matters

A pigtail termination connects the cable shield to the connector or ground using a short wire.

Although simple and easy to manufacture, a long pigtail can introduce additional inductance into the shielding path. As frequency increases, that inductive impedance can become more significant.

This is why applications with demanding EMC or high-speed signal requirements often use shorter, wider, or circumferential shield termination methods instead of long pigtails.

The design decision should consider the actual frequency range and system requirements rather than applying one termination method universally.


Connector Shielding for High-Speed Industrial Communication

High-speed communication systems are particularly sensitive to shielding discontinuities.

Applications such as:

  • Industrial Ethernet
  • machine vision
  • industrial cameras
  • robotics
  • servo drives
  • motion control
  • high-speed sensors

can require carefully controlled shielding and grounding.

For example, TE Connectivity’s M12 X-Code connector solutions use a full metal shell and 360° cable shield termination to support high-speed data transmission and EMI protection.

This illustrates an important point: shielding design must support the complete transmission channel rather than focusing only on the connector contact itself.


Mechanical Design and EMC Performance Must Work Together

Connector shielding cannot be separated from mechanical design.

An industrial connector may need to withstand:

  • vibration
  • shock
  • repeated mating cycles
  • cable movement
  • temperature changes
  • moisture and dust

At the same time, it must maintain a stable shielding connection.

A loose shell, insufficient cable retention, or poorly controlled backshell assembly can gradually affect the shielding path.

For this reason, connector design should evaluate electrical and mechanical performance together.


Environmental Protection Can Affect Shielding Performance

Industrial connectors may operate in environments containing:

  • moisture
  • dust
  • oil
  • chemicals
  • condensation
  • salt contamination

These factors can affect conductive surfaces and mechanical interfaces.

Environmental sealing is therefore not completely separate from EMC design. A connector may require both:

EMI shielding + mechanical protection + environmental sealing

For example, a backshell may combine shield termination with a heat-shrink boot or other sealing structure. TE Connectivity’s backshell solutions demonstrate how shielding, strain relief, and environmental protection can be integrated into a single termination system.


How to Validate Connector Shielding Performance

Connector shielding should be validated as part of the complete cable assembly rather than only at component level.

Depending on the application, validation may include:

  • shield continuity testing
  • low-resistance measurement
  • EMC testing
  • radiated emission testing
  • conducted emission testing
  • immunity testing
  • vibration testing
  • temperature cycling
  • environmental exposure
  • connector mating-cycle testing

The validation method should reflect the actual application frequency range and operating environment.

A connector that passes a simple continuity test does not automatically provide adequate high-frequency EMI performance.


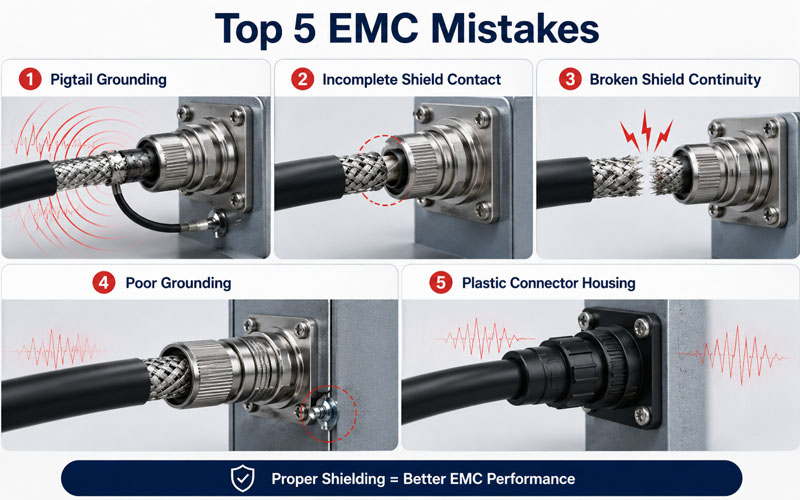
Common Connector Shielding Design Mistakes

Several common mistakes can reduce the effectiveness of an otherwise well-designed shielded cable assembly.

Using a shielded cable with an unshielded connector

The cable may have excellent shielding performance, but the connector interface creates an exposed section.

Terminating only part of the shield

Partial termination can create discontinuities that reduce overall shielding effectiveness.

Using excessive pigtail length

A long pigtail can add inductive impedance, particularly at higher frequencies.

Ignoring connector-to-chassis bonding

The connector shell needs an appropriate electrical relationship with the equipment enclosure.

Treating the backshell as only mechanical protection

A backshell may be a critical part of the EMI shielding and strain-relief system.

Ignoring manufacturing variation

A shielding concept that works in a prototype may perform differently if shield preparation, termination length, crimp force, or assembly position varies during mass production.


How FPIC Supports Shielded Connector and Cable Assembly Projects

For custom connector and cable assembly projects, shielding performance depends on the interaction between the connector, cable, shield termination, backshell, and assembly process.

FPIC supports custom connector and cable assembly development for industrial and other demanding applications, where connector selection, cable construction, shielding, sealing, and manufacturing consistency need to be considered together.

For applications such as industrial automation, robotics, industrial cameras, and control systems, early review of the complete cable-to-connector interface can help reduce EMC and reliability risks before mass production.

The objective is not simply to select a “shielded connector,” but to develop a complete interconnect system with a controlled electrical and mechanical shielding path.


Final Thoughts

Effective connector shielding design is about maintaining a continuous and controlled electromagnetic barrier from the cable through the connector and into the equipment enclosure.

The most important design considerations include:

  • appropriate connector shell construction
  • reliable shield termination
  • 360° shielding where required
  • suitable backshell design
  • controlled grounding and bonding
  • mechanical strain relief
  • environmental protection
  • validation under realistic operating conditions

For high-speed industrial equipment and EMC-sensitive systems, the connector should be treated as an active part of the shielding architecture.

A well-designed connector interface can help protect signal integrity, reduce EMI-related failures, and improve the long-term reliability of the complete cable assembly.


FAQ

What is connector shielding?

Connector shielding is the use of conductive connector shells, backshells, shield termination methods, and grounding structures to reduce electromagnetic interference entering or leaving an electrical connection.

Why is 360° shield termination important?

A 360° termination provides a continuous circumferential connection between the cable shield and connector shielding structure. It can help reduce shielding discontinuities and support more consistent EMI performance, particularly in demanding applications.

Is a metal connector enough for EMI protection?

No. A metal connector shell alone does not guarantee effective EMI protection. Cable shield termination, shell bonding, backshell design, grounding, cable construction, and assembly quality all influence the final shielding performance.

What is the difference between shield termination and strain relief?

Shield termination establishes electrical continuity between the cable shield and connector shielding structure. Strain relief manages mechanical forces on the cable. These functions should work together but should not be treated as the same function.

Are shielded connectors necessary for industrial Ethernet?

They may be necessary depending on the system architecture, data rate, EMC environment, cable construction, and applicable requirements. High-speed industrial communication systems often require carefully controlled shielding and grounding to maintain signal integrity.

How can connector shielding performance be tested?

Depending on the application, validation can include shield continuity, low-resistance measurement, EMC testing, radiated and conducted emissions, immunity testing, vibration, thermal cycling, and environmental testing.


Need a Custom Shielded Connector or Cable Assembly?

If your application requires reliable EMI protection for industrial automation, robotics, industrial cameras, motion control, or other demanding systems, connector and cable shielding should be considered together from the beginning.

FPIC supports custom connector and cable assembly projects with engineering review, connector integration, cable assembly, and production support.
Contact FPIC to discuss your connector shielding requirements.


Resources

  1. TE Connectivity – INTERCONTEC Connectors: provides examples of industrial connectors using 360° EMC shield termination for motor and industrial applications.
  2. TE Connectivity – Tinel-Lock Backshells for Military Applications: explains shield termination, backshell design, electrical continuity, strain relief, and 360° braid termination for demanding environments.
  3. TE Connectivity – M12 X-Code Connector Series: provides an industrial M12 example using a full metal shell and 360° cable shield termination for high-speed data applications.
  4. TE Connectivity – Space-Grade Backshells for Micro-D and D-Sub Connectors: discusses the relationship between EMI shielding, grounding, backshells, strain relief, and environmental protection.
  5. TE Connectivity – Screened Backshells and Adapters: provides examples of braided, banded, and 360° shield termination solutions for screened cable assemblies.
Connector Material Selection Guide for Engineers

A connector may look simple from the outside, but its reliability depends heavily on the materials used throughout the assembly.

A typical connector includes several material systems:

Housing + Contacts + Plating + Seals + Locks + Secondary Components

Each material has a different function.

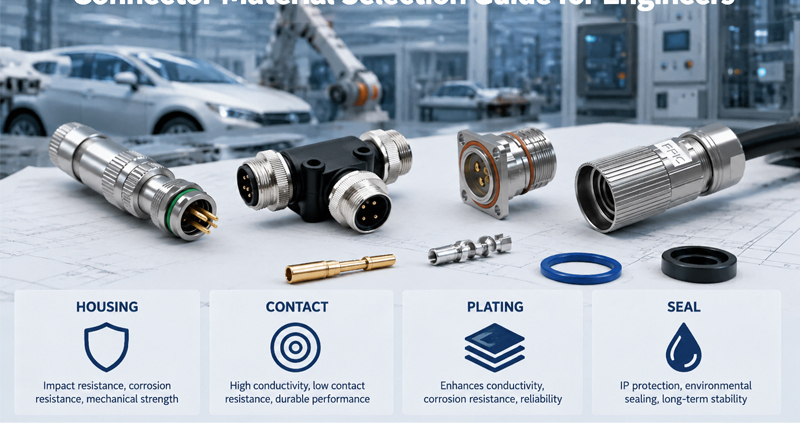
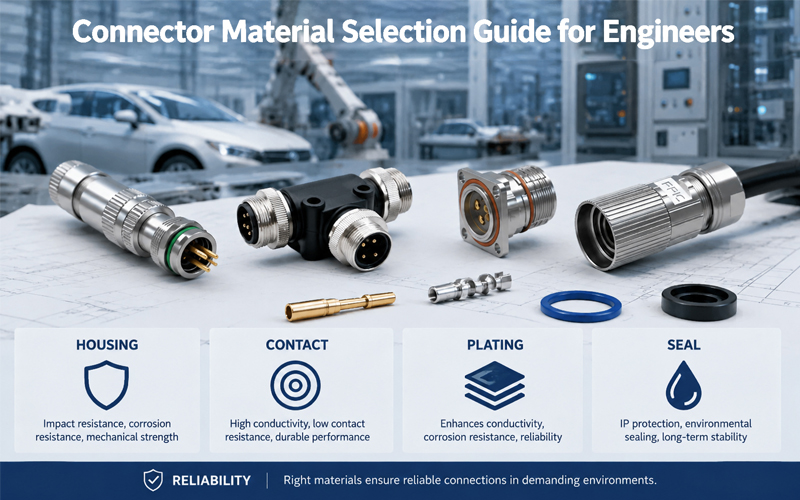
The housing must provide insulation and mechanical protection. The contact system must maintain stable electrical performance. Plating must protect the contact interface from corrosion and wear. Seals must maintain environmental protection without compromising assembly performance.

Selecting materials based only on cost or a single specification can create reliability problems later in the product lifecycle.

For demanding applications such as automotive electronics, industrial automation, robotics, medical equipment, and energy systems, material selection should therefore be treated as a system-level engineering decision.

The objective is to balance:

Electrical Performance + Mechanical Strength + Thermal Stability + Environmental Resistance + Manufacturability + Cost

Connector Material Selection Guide for Engineers


Why Connector Material Selection Matters

Connector materials directly influence how a connector performs throughout its service life.

Poor material selection can contribute to:

  • Contact resistance increase
  • Corrosion
  • Terminal deformation
  • Housing cracking
  • Seal degradation
  • Insulation failure
  • Poor mating performance
  • Reduced vibration resistance
  • Premature connector failure

For example, a housing material may meet the required temperature rating but lack sufficient mechanical strength.

Likewise, a contact alloy may provide excellent conductivity but require a different plating system to achieve the required corrosion and wear resistance.

This is why engineers should evaluate the complete material combination, rather than selecting each material independently.


1.Connector Housing Material Selection

The connector housing provides:

  • Electrical insulation
  • Mechanical support
  • Terminal positioning
  • Mating alignment
  • Environmental protection
  • Structural protection

The housing material therefore needs to withstand the expected electrical, thermal, mechanical, and environmental conditions.

Common connector housing materials include:

  • PA / Nylon
  • PBT
  • PPS
  • LCP
  • PEEK
  • PC and other engineering polymers

The best material depends on the application rather than simply its nominal strength.


2.PA / Nylon

Polyamide materials are widely used in connector housings because they can provide a useful combination of:

  • Mechanical strength
  • Impact resistance
  • Processability
  • Cost efficiency

However, different grades can behave differently in terms of:

  • Water absorption
  • Dimensional stability
  • Temperature resistance
  • Chemical resistance

For applications involving humidity or significant temperature variation, engineers should evaluate the specific PA grade rather than treating all nylon materials as equivalent.


3.PBT

Polybutylene terephthalate, or PBT, is commonly used for electrical and automotive connector housings.

Potential advantages include:

  • Good dimensional stability
  • Electrical insulation
  • Chemical resistance
  • Suitable molding characteristics
  • Good temperature performance for many applications

PBT can be attractive where dimensional precision and electrical insulation are important.


4.PPS for Higher-Temperature Applications

Polyphenylene sulfide (PPS) is an engineering polymer commonly considered for demanding thermal and chemical environments.

Potential characteristics include:

  • High temperature resistance
  • Low moisture absorption
  • Good dimensional stability
  • Chemical resistance
  • Electrical insulation

PPS can be useful when the connector must maintain dimensional stability under elevated temperatures.

However, material selection should always consider the actual temperature profile, not simply the maximum advertised material temperature.


5.LCP for Fine-Pitch Connectors

Liquid crystal polymer (LCP) is often considered for compact and fine-pitch connector designs.

Its characteristics can support applications requiring:

  • Thin-wall molding
  • Dimensional precision
  • Fine-pitch structures
  • Good thermal performance
  • Low moisture absorption

As connector dimensions decrease, housing dimensional stability becomes increasingly important.

A material suitable for a large connector may not necessarily be the best choice for a miniature high-density connector.


6.PEEK for Highly Demanding Applications

PEEK is a high-performance engineering polymer used in applications requiring demanding combinations of:

  • Temperature resistance
  • Chemical resistance
  • Mechanical strength
  • Dimensional stability

Its higher material cost means it is generally considered when standard engineering plastics cannot adequately meet the application requirements.

Material selection should therefore consider total system requirements, rather than simply selecting the highest-performance material available.


7.Flame Retardancy

For many electronic and industrial applications, connector housing materials may need to meet specific flammability requirements.

Engineers should consider:

  • Applicable safety requirements
  • Electrical application
  • Equipment enclosure
  • Operating voltage
  • Installation environment

A flame-retardant grade can affect other material characteristics such as:

  • Mechanical strength
  • Flow behavior
  • Moldability
  • Cost

Therefore, flame retardancy should be evaluated together with the overall material specification.


8.Connector Contact Material Selection

The contact system is responsible for maintaining the electrical interface.

Common contact alloys include:

  • Copper
  • Brass
  • Phosphor bronze
  • Copper alloys
  • Beryllium copper for specialized applications

The selected material affects:

  • Electrical conductivity
  • Spring properties
  • Contact force
  • Fatigue resistance
  • Thermal behavior
  • Corrosion resistance
  • Manufacturability

A connector contact must provide both electrical performance and mechanical reliability.


9.Brass Contacts

Brass is widely used for connector terminals because it provides a practical balance of:

  • Conductivity
  • Strength
  • Formability
  • Cost

It can be suitable for many general-purpose connector applications.

However, for high-flex or high-contact-force applications, another copper alloy may provide more suitable mechanical properties.


10.Phosphor Bronze Contacts

Phosphor bronze can provide good spring characteristics and fatigue resistance.

It is often considered when the contact must maintain stable mechanical behavior during repeated mating or long-term operation.

Potential applications include:

  • Signal connectors
  • Control connectors
  • Industrial equipment
  • Repeated mating interfaces

The final choice depends on the required contact force, conductivity, mating cycles, and environmental conditions.


11.Beryllium Copper

Beryllium copper can provide excellent spring properties and good electrical conductivity.

It may be considered for applications requiring:

  • High contact force
  • Miniaturized contacts
  • Repeated mating
  • Strong elastic recovery

Because material cost and processing considerations can be higher, engineers should use it when its performance advantages justify the additional complexity.


12.Contact Plating Selection

Contact plating forms the actual surface interface between mating contacts.

Common plating materials include:

Tin

Tin is widely used for cost-sensitive applications and can provide practical performance for many power connections.

Gold

Gold plating provides excellent corrosion resistance and stable contact behavior.

It is particularly useful where:

  • Low-level signals are involved
  • Long-term contact stability is important
  • Corrosive environments are present
  • High mating-cycle performance is required

Silver

Silver has excellent electrical conductivity and can be considered for certain power and high-current applications.

However, its behavior under specific environmental conditions must be carefully evaluated.


13.Gold Plating Thickness Matters

Simply specifying “gold plated” is not enough.

Engineers should also consider:

  • Gold thickness
  • Plating area
  • Underplating
  • Contact force
  • Mating cycles
  • Operating environment

A thin decorative gold layer and an engineered contact plating system do not necessarily provide the same long-term performance.

For demanding applications, plating specifications should be clearly defined in the connector drawing or technical specification.


14.Underplating Matters Too

The plating system can include multiple layers.

For example:

Base Contact Alloy → Underplating → Gold Surface

The underplating can help provide:

  • Corrosion protection
  • Diffusion resistance
  • Better plating stability

The complete plating structure should therefore be evaluated rather than looking only at the visible surface material.


15.Connector Seal Material Selection

Seals become critical when connectors must resist:

  • Water
  • Dust
  • Oil
  • Chemicals
  • Temperature cycling

Common sealing materials include:

  • Silicone rubber
  • EPDM
  • Fluoroelastomer materials
  • Other application-specific elastomers

The correct seal depends heavily on the environment.


16.Silicone Seals

Silicone can provide good flexibility across a broad temperature range.

It is commonly considered where connectors must tolerate:

  • Temperature variation
  • Repeated assembly
  • Flexible sealing interfaces

However, chemical compatibility must still be evaluated for the actual application.


17.EPDM Seals

EPDM can provide good resistance to:

  • Water
  • Weathering
  • Ozone
  • Certain environmental conditions

It may be suitable for outdoor or automotive environments depending on the specific fluid and temperature exposure.


18.Chemical Compatibility Is Critical

A connector material may perform well in a laboratory but degrade when exposed to the actual application environment.

Potential contaminants include:

  • Automotive fluids
  • Lubricants
  • Cleaning agents
  • Coolants
  • Hydraulic fluids
  • Industrial chemicals

Material compatibility should therefore be validated against the actual chemicals and concentrations expected during the connector’s service life.


19.Temperature Selection Should Consider the Complete System

Connector temperature performance is not determined by housing material alone.

The complete system includes:

Current → Contact Resistance → Heat Generation → Housing → Surrounding Environment

Higher current can increase temperature at the contact interface.

This means the connector must be evaluated under realistic electrical loading.

Engineers should consider:

  • Ambient temperature
  • Current load
  • Number of loaded circuits
  • Contact resistance
  • Heat dissipation
  • Housing material
  • Installation conditions

20.Material Selection for High-Current Connectors

High-current connectors place greater demands on the contact system.

Important factors include:

  • Contact resistance
  • Conductivity
  • Contact force
  • Terminal cross-section
  • Plating
  • Temperature rise
  • Thermal dissipation

Simply choosing a highly conductive alloy does not automatically create a reliable high-current connector.

The complete contact geometry and mechanical interface also matter.


21.Material Selection for Fine-Pitch Connectors

Miniaturized connectors create different material challenges.

As pitch decreases:

  • Housing walls become thinner
  • Terminal spacing decreases
  • Dimensional tolerances become tighter
  • Mating alignment becomes more sensitive

Materials with good dimensional stability and molding precision may therefore become increasingly important.

This is one reason material selection should be performed together with connector geometry and manufacturing process development.


22.Material Selection for Automotive Connectors

Automotive connectors may encounter:

  • Temperature cycling
  • Vibration
  • Humidity
  • Dust
  • Oil
  • Chemical exposure
  • Long service life requirements

Material selection should therefore consider the complete automotive environment.

For automotive connector products, FPIC applies IATF 16949 quality management requirements and supports production processes designed for demanding automotive applications.


23.Material Selection for Industrial Connectors

Industrial connectors may be exposed to:

  • Continuous vibration
  • Machinery movement
  • Oil
  • Dust
  • Chemicals
  • Outdoor environments

Industrial connector material selection should consider not only IP protection but also mechanical durability and chemical compatibility.

For example, an industrial connector used near motors may require different mechanical characteristics from one installed inside a protected control cabinet.


24.Material Selection for Medical Connectors

Medical applications may place additional requirements on:

  • Biocompatibility
  • Cleaning resistance
  • Chemical exposure
  • Sterilization
  • Reliability
  • Traceability

The material selection process should therefore begin with the applicable medical device requirements and cleaning or sterilization process.


25.Manufacturing Must Be Considered

A material with excellent laboratory performance may still be difficult to manufacture.

Engineers should evaluate:

  • Injection molding behavior
  • Shrinkage
  • Warpage
  • Flow characteristics
  • Terminal stamping
  • Plating process
  • Crimp compatibility
  • Assembly tolerances

Material selection should support not only prototype performance but also stable mass production.


Connector Material Selection Matrix

ComponentCommon MaterialsMain Selection Factors
HousingPA, PBT, PPS, LCP, PEEKTemperature, insulation, strength, chemicals
ContactBrass, phosphor bronze, copper alloysConductivity, spring force, fatigue
PlatingTin, gold, silverCorrosion, current, mating cycles
SealSilicone, EPDM, fluoroelastomerTemperature, water, chemicals
Locking PartsEngineering plastics / metalsRetention, vibration, durability
ShieldingCopper alloys / metal shellsEMC, grounding, mechanical strength

Common Connector Material Selection Mistakes

MistakePotential Consequence
Selecting housing only by temperature ratingMechanical or dimensional problems
Treating all nylon grades as identicalUnexpected moisture or thermal behavior
Selecting contact material only by conductivityInsufficient spring performance
Specifying gold plating without thicknessUnclear contact durability
Ignoring underplatingCorrosion or diffusion concerns
Selecting seals without chemical testingSwelling or degradation
Ignoring current-related heat generationExcessive temperature rise
Choosing materials without DFM reviewMolding or assembly problems
Selecting the highest-performance material automaticallyUnnecessary cost
Evaluating materials independentlySystem-level compatibility problems

A Practical Connector Material Selection Workflow

Step 1: Define the Environment

Identify:

  • Temperature
  • Humidity
  • Water
  • Dust
  • Chemicals
  • Vibration
  • UV exposure

Step 2: Define Electrical Requirements

Identify:

  • Current
  • Voltage
  • Signal type
  • Contact resistance
  • Mating cycles

Step 3: Define Mechanical Requirements

Consider:

  • Contact force
  • Mating force
  • Retention
  • Shock
  • Vibration
  • Connector size

Step 4: Select Housing Material

Match:

Temperature + Insulation + Mechanical + Environmental Requirements

Step 5: Select Contact Alloy

Match:

Conductivity + Spring Properties + Fatigue + Formability

Step 6: Select Plating

Match:

Corrosion + Wear + Current + Signal + Mating Cycles

Step 7: Select Seal Material

Match:

Temperature + Fluids + Water + Chemical Exposure

Step 8: Validate the Complete Connector

Evaluate:

  • Electrical performance
  • Mechanical performance
  • Temperature rise
  • Environmental resistance
  • Mating cycles
  • Dimensional stability
  • Production consistency

Material Selection Should Follow Application Requirements

A common mistake is starting with a preferred material and trying to make it fit the application.

A better approach is:

Application → Requirements → Material Properties → Component Design → Validation

For example, if a connector operates in a high-temperature environment, engineers should not simply select the highest-temperature housing material.

They should first ask:

  • What is the actual temperature profile?
  • How much current flows through the contacts?
  • How long is the exposure?
  • Is vibration present?
  • Are chemicals present?
  • How many mating cycles are required?

The answers determine the appropriate material combination.


Why Material Compatibility Matters

A connector is a multi-material system.

Consider:

Housing + Contact Alloy + Plating + Seal + Cable + Mating Connector

Changing one material can influence another.

For example:

  • Housing shrinkage can affect terminal position.
  • Contact force can affect plating wear.
  • Seal hardness can affect mating force.
  • Temperature can affect housing dimensions.
  • Chemical exposure can affect both housing and seals.

This is why reliable connector development requires cross-functional material engineering.


How FPIC Supports Connector Material Selection

FPIC provides customized connector development and manufacturing solutions covering:

  • Connector housing materials
  • Contact materials
  • Contact plating
  • Sealing systems
  • Terminal stamping
  • Connector assembly
  • Electrical testing
  • Dimensional inspection
  • Reliability validation

FPIC’s automotive connector products are manufactured under IATF 16949 quality management requirements.

For automotive connector production, FPIC also supports mass-production cleanliness requirements aligned with VDA 19.1 / ISO 16232 practices.

Material and component selection can be evaluated together with connector geometry, tooling, assembly, and testing requirements.

This system-level approach helps OEM customers develop connectors that balance performance, reliability, manufacturability, and cost.


Final Thoughts

Connector material selection is not simply a question of choosing the strongest plastic, most conductive metal, or thickest plating.

The correct material combination depends on the complete application.

Engineers should evaluate:

Housing + Contact + Plating + Seal + Environment + Electrical Load + Mechanical Requirements

The best connector material is the one that provides the required performance throughout the expected service life while remaining manufacturable and commercially practical.

A structured selection process can help reduce:

  • Corrosion risk
  • Thermal problems
  • Mechanical failure
  • Seal degradation
  • Manufacturing variation
  • Lifecycle cost

Ultimately, successful connector design begins with understanding the application and selecting materials that work together as a complete system.


FAQ

What is the most important factor in connector material selection?

There is no single factor. Temperature, current, environment, mechanical loading, mating cycles, dimensional requirements, and manufacturing conditions should all be considered together.

Which material is commonly used for connector housings?

PA and PBT are widely used for many connector applications, while PPS, LCP, PEEK, and other engineering polymers may be considered for more demanding thermal, dimensional, or chemical requirements.

What materials are commonly used for connector contacts?

Brass, phosphor bronze, and other copper alloys are commonly used. The selection depends on conductivity, spring properties, contact force, fatigue resistance, and application requirements.

Is gold plating always better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact performance, but it can increase cost. Tin may be suitable for many power applications. The correct plating depends on current, signal type, environment, and mating requirements.

How should connector seal material be selected?

Seal material should be evaluated against the actual temperature range, water exposure, chemicals, oils, cleaning agents, and expected service life.

Does connector housing material affect electrical reliability?

Yes. Housing material affects insulation, terminal positioning, dimensional stability, heat resistance, and mechanical protection, all of which can influence connector reliability.

Why should material selection consider manufacturing?

A material may perform well technically but create molding, stamping, plating, assembly, or cost problems at production volume. DFM should therefore be included early in the material selection process.


Need Help Selecting Materials for Your Connector?

FPIC supports OEM and engineering teams with connector design and manufacturing from material selection and tooling through assembly, testing, and mass production.

Whether you need a compact fine-pitch connector, high-current connector, automotive connector, industrial connector, or customized interconnection solution, our engineering team can evaluate the complete material and application requirements.

Contact FPIC to discuss your connector development project.


Resources

  1. IEC
    https://www.iec.ch/
    International standards and technical resources covering electrical and electronic technologies.
  2. SAE International
    https://www.sae.org/
    Automotive engineering standards and technical resources.
  3. IPC
    https://www.ipc.org/
    Industry standards and resources for electronic interconnection and manufacturing.
  4. IATF Global Oversight
    https://www.iatfglobaloversight.org/
    Resources related to IATF 16949 automotive quality management requirements.
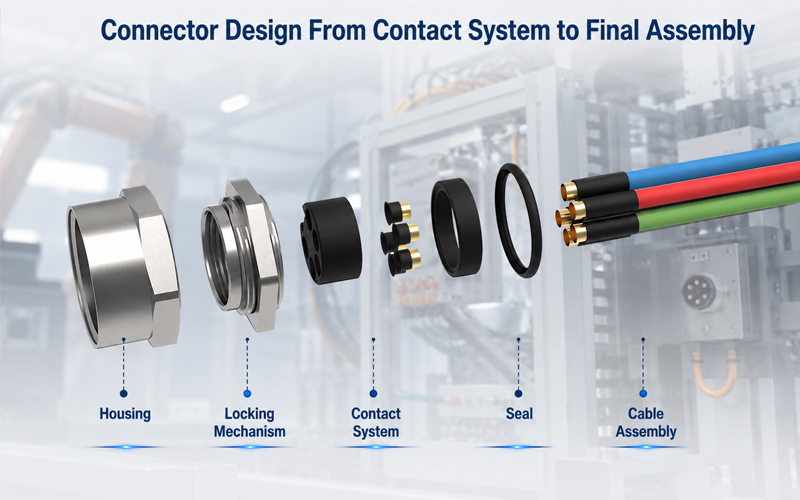
Connector Design From Contact System to Final Assembly

A connector may look like a simple component, but its performance depends on the interaction of multiple engineering elements.

A reliable connector requires careful design of:

  • Contact system
  • Housing structure
  • Locking mechanism
  • Sealing system
  • Material selection
  • Manufacturing process
  • Final assembly and testing

A mistake in any stage can affect:

  • Electrical performance
  • Mechanical reliability
  • Environmental protection
  • Service life

For engineers developing industrial, automotive, robotics, energy storage, and automation systems, connector design should be considered as a complete engineering process—not just a component selection task.

This guide explains the key stages of connector design, from the internal contact system to final production validation.

Connector Design From Contact System to Final Assembly


Why Connector Design Requires System-Level Thinking

A connector performs three primary functions:

Electrical Connection

Providing stable current or signal transmission.

Important factors:

Contact resistance

Current capacity

Signal integrity

Plating performance

Mechanical Connection

Maintaining a secure connection under real-world conditions.

Important factors:

Mating force

Locking structure

Vibration resistance

Mating cycles

Environmental Protection

Protecting internal components from harsh environments.

Important factors:

Waterproof sealing

Dust protection

Temperature resistance

Chemical exposure

A successful connector design balances all three requirements.


1.Contact System Design: The Core of Connector Performance

The contact system is the electrical heart of a connector.

Its design directly affects:

  • Conductivity
  • Heat generation
  • Reliability
  • Service life

Contact Geometry Design

Contact geometry determines how terminals connect and maintain contact force.

Key considerations include:

✔ Contact area

✔ Spring structure

✔ Contact pressure

✔ Current path design

A properly designed contact system provides:

Stable electrical connection

Low resistance

Long-term performance


Contact Material Selection

Common contact materials include:

Copper Alloys

Advantages:

✔ Good conductivity

✔ Balanced strength

✔ Cost efficiency

Phosphor Bronze

Advantages:

✔ Good spring performance

✔ Excellent fatigue resistance

Beryllium Copper

Advantages:

✔ High elasticity

✔ Excellent contact force retention

Used for:

  • High-cycle connectors
  • Precision applications

Contact Plating Selection

Surface plating affects:

  • Corrosion resistance
  • Contact stability
  • Mating life

Common options include:

Gold Plating

Advantages:

✔ Excellent corrosion resistance

✔ Reliable low contact resistance

Suitable for:

  • Signal connectors
  • Medical equipment
  • High-cycle applications

Tin Plating

Advantages:

✔ Cost-effective

✔ Suitable for many power applications

The correct plating depends on:

  • Current level
  • Environment
  • Required mating cycles

2.Housing Design: Mechanical Protection and Alignment

The connector housing protects internal contacts and ensures proper mating.

A good housing design must provide:

✔ Mechanical strength

✔ Accurate terminal positioning

✔ Electrical insulation

✔ Assembly efficiency


Housing Material Selection

Common materials include:

PA (Polyamide)

Used for:

  • Industrial connectors
  • General applications

Benefits:

  • Good strength
  • Cost efficiency

PBT

Benefits:

  • Dimensional stability
  • Low moisture absorption

PPS

Benefits:

  • High temperature resistance
  • Chemical resistance

Material selection depends on:

  • Operating temperature
  • Mechanical requirements
  • Environmental conditions

Terminal Positioning and Polarization

Connector housings should prevent incorrect assembly.

Important design features:

  • Keying structures
  • Polarization features
  • Secondary locks

These features help prevent:

❌ Wrong mating

❌ Terminal back-out

❌ Assembly mistakes


3.Locking Mechanism Design

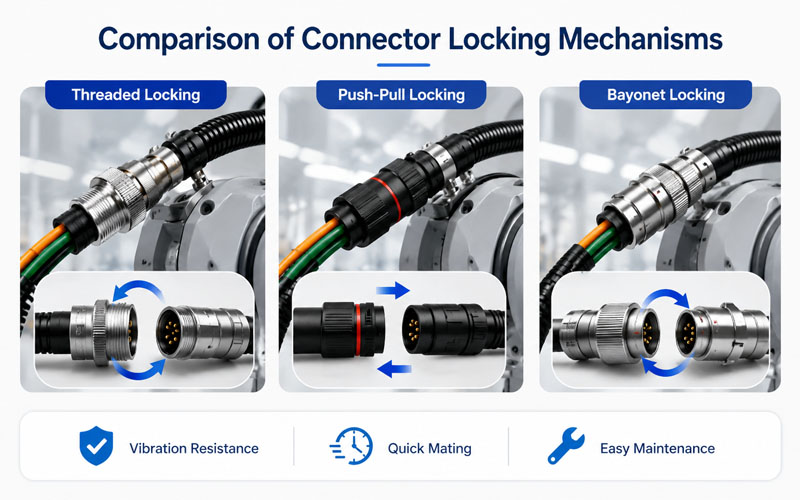
A reliable locking system prevents accidental disconnection.

Common locking methods include:


Threaded Locking

Advantages:

✔ High vibration resistance

✔ Strong mechanical retention

Applications:

  • Industrial equipment
  • Outdoor systems

Push-Pull Locking

Advantages:

✔ Fast connection

✔ Easy operation

✔ High mating efficiency

Applications:

  • Medical
  • Automation
  • Test equipment

Snap Locking

Advantages:

✔ Simple operation

✔ Cost-effective

Applications:

  • General electronic applications

4.Sealing and Environmental Protection

For harsh environments, sealing design is critical.

Connector sealing protects against:

  • Water
  • Dust
  • Oil
  • Humidity

Common sealing components include:

  • O-rings
  • Gaskets
  • Rubber seals

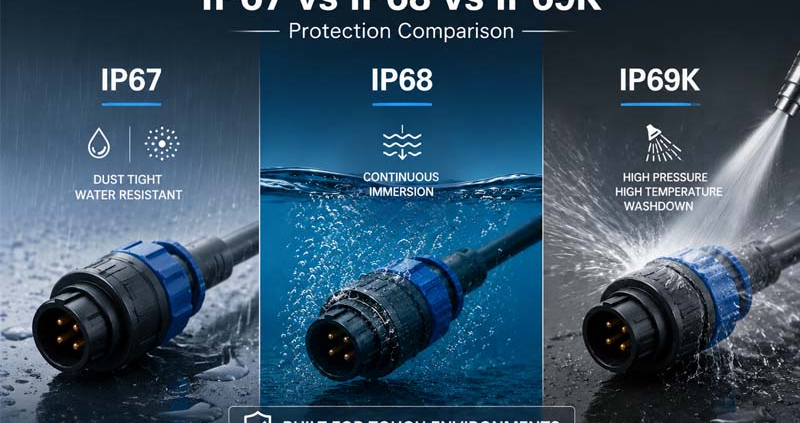
IP Protection Considerations

Depending on the application, connectors may require:

  • IP67
  • IP68
  • IP69K

Higher protection levels require careful control of:

  • Seal compression
  • Housing interface
  • Material compatibility

5.Connector Assembly Design

Connector assembly affects both quality and manufacturing efficiency.

A production-ready design should consider:


Terminal Insertion

Important factors:

✔ Insertion force

✔ Terminal retention

✔ Position accuracy


Secondary Locking System

Secondary locks improve:

  • Terminal retention
  • Assembly reliability
  • Safety

Assembly Error Prevention

Good designs include:

  • Visual identification
  • Mechanical keying
  • Assembly guidance

These features improve production consistency.


6.Connector Validation and Testing

Before mass production, connectors require validation.

Common tests include:


Electrical Testing

Including:

  • Contact resistance
  • Insulation resistance
  • Hi-Pot testing

Mechanical Testing

Including:

  • Insertion force
  • Extraction force
  • Mating cycles
  • Vibration testing

Environmental Testing

Including:

  • Temperature cycling
  • Humidity testing
  • Salt spray testing
  • Water ingress testing

Testing ensures the connector performs under real application conditions.


7.Connector Design for Mass Production

A successful connector design must also consider manufacturing.

Key DFM considerations include:

Injection Molding

Evaluate:

  • Wall thickness
  • Draft angle
  • Mold complexity

Terminal Stamping

Evaluate:

  • Material utilization
  • Contact geometry
  • Production consistency

Assembly Automation

Evaluate:

  • Assembly direction
  • Process repeatability
  • Inspection requirements

Good connector design reduces production risks.


How FPIC Approaches Connector Design

FPIC provides customized connector solutions from engineering design through mass production.

Our connector development process considers:

  • Contact system design
  • Housing structure
  • Material selection
  • Manufacturing feasibility
  • Assembly optimization
  • Reliability testing

By combining engineering experience with manufacturing capability, FPIC helps customers develop connectors that meet demanding industrial requirements.


Final Thoughts

Connector design is a system engineering process.

A reliable connector requires the right balance between:

  • Contact performance
  • Mechanical structure
  • Environmental protection
  • Manufacturing efficiency

From the first contact design to final assembly validation, every detail influences long-term reliability.

For OEM engineers, selecting the right connector partner means choosing a team that understands both product performance and manufacturing reality.

A high-quality connector is not simply assembled—it is engineered.


FAQ

What are the main parts of a connector?

The main parts include contacts, housing, locking mechanism, sealing components, and assembly features.

Why is contact design important in connectors?

The contact system determines electrical performance, contact resistance, current capability, and mating reliability.

What factors affect connector lifetime?

Key factors include materials, contact force, mating cycles, environment, vibration, and manufacturing quality.

What tests are required for connector validation?

Common tests include electrical testing, mechanical testing, environmental testing, and durability testing.

Why should connector design consider manufacturing early?

Early manufacturing consideration improves production efficiency, reduces defects, and controls cost.


Need a Custom Connector Solution?

FPIC develops customized connector solutions for industrial automation, robotics, energy storage, automotive, and other demanding applications.

From contact design and material selection to tooling, assembly, and testing, FPIC supports customers from concept development to mass production.

Contact FPIC today to discuss your connector project.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Connector testing methods covering electrical, mechanical, and environmental performance.
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry requirements for cable assembly quality and workmanship.
  3. ISO 16750 – Road Vehicles Environmental Conditions and Testing
    https://www.iso.org/
    Environmental testing guidance for automotive electrical components.
  4. IATF 16949 Automotive Quality Management System
    https://www.iatfglobaloversight.org/
    Automotive quality management requirements for production consistency.
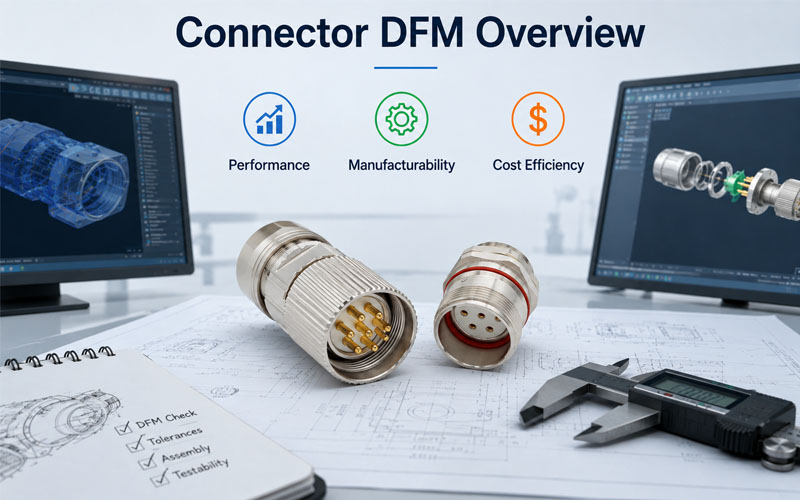
Connector DFM Design Optimization Overview

Designing a connector is not only about achieving the highest electrical performance.

A connector must also be:

  • Easy to manufacture
  • Consistent in mass production
  • Cost-effective
  • Reliable throughout its service life

Many connector designs fail to consider manufacturing requirements early enough.

The result can include:

  • Complex assembly processes
  • Higher tooling costs
  • Production delays
  • Difficult quality control
  • Increased unit cost

This is why Design for Manufacturing (DFM) plays an important role in connector development.

A successful connector design balances three key factors:

Performance + Manufacturability + Cost

Connector DFM Design Optimization Overview


What Is Connector DFM?

Connector DFM (Design for Manufacturing) is an engineering approach that considers production requirements during the design stage.

Instead of designing a connector first and solving manufacturing problems later, DFM integrates:

  • Material selection
  • Tooling requirements
  • Assembly processes
  • Testing methods
  • Production scalability

from the beginning.

The goal is to create a connector that performs well while remaining practical for high-volume manufacturing.


Why DFM Matters in Connector Development

A connector may perform well in a laboratory environment but face challenges during mass production.

Common issues caused by poor DFM include:

❌ Difficult assembly

❌ Tight manufacturing tolerances

❌ High tooling complexity

❌ Low production yield

❌ Increased inspection requirements

❌ Higher manufacturing cost

A DFM-focused design reduces these risks by considering the entire product lifecycle.


1.Design for Electrical Performance

The first priority of any connector is reliable electrical performance.

DFM does not mean reducing performance.

Instead, it means achieving required performance with an optimized design.

Key electrical considerations include:


Contact System Design

The contact structure affects:

  • Current capacity
  • Contact resistance
  • Mating cycles
  • Signal integrity

Engineers should evaluate:

✔ Contact geometry

✔ Contact force

✔ Material selection

✔ Plating thickness

✔ Current path design

A well-designed contact system improves reliability while avoiding unnecessary material costs.


Creepage and Clearance Design

For higher voltage applications, spacing requirements are critical.

Proper DFM considers:

  • Insulation distance
  • Housing structure
  • Manufacturing capability

Over-designing spacing may increase connector size and cost.

Under-designing may create safety risks.

The goal is the correct balance.


2.Design for Manufacturability

A connector designed for manufacturing should support stable and efficient production.

Important factors include:

Simplify Connector Structure

Complex structures increase:

  • Mold difficulty
  • Assembly steps
  • Failure risks

Good DFM practices include:

✔ Reducing unnecessary components

✔ Simplifying assembly direction

✔ Minimizing manual operations

✔ Improving part consistency


Optimize Housing Design

The connector housing must consider injection molding requirements.

Important factors:

  • Wall thickness
  • Draft angles
  • Rib design
  • Shrinkage control
  • Mold release

Poor housing design can lead to:

  • Warpage
  • Cracks
  • Dimensional variation

Improve Assembly Efficiency

Mass production requires repeatable assembly.

Design considerations:

✔ Easy terminal insertion

✔ Clear orientation features

✔ Locking mechanism feedback

✔ Error-proof assembly

These features reduce production errors and improve efficiency.


3.Material Selection for DFM

Material selection affects both performance and manufacturing cost.

Important factors include:

  • Temperature resistance
  • Mechanical strength
  • Chemical resistance
  • Processing requirements

Common connector materials:


Housing Materials

PA (Polyamide)

Advantages:

✔ Good mechanical strength

✔ Cost-effective

✔ Widely available

PBT

Advantages:

✔ Dimensional stability

✔ Good electrical insulation

PPS

Advantages:

✔ High temperature performance

✔ Excellent chemical resistance

The right material depends on the application requirements.


Contact Materials

Common choices:

  • Copper alloys
  • Phosphor bronze
  • Beryllium copper

Selection depends on:

  • Conductivity
  • Spring performance
  • Mating cycles
  • Cost targets

4.Design for Tooling Efficiency

Connector tooling can represent a significant development investment.

DFM helps reduce tooling complexity.

Key considerations:

Mold Design

Good connector designs consider:

✔ Fewer sliders

✔ Simple parting lines

✔ Stable cavity design

✔ Easy maintenance


Terminal Stamping Design

Terminal design affects:

  • Material usage
  • Stamping speed
  • Production consistency

Optimized terminal geometry can reduce:

  • Material waste
  • Processing cost
  • Defect rates

5.Balancing Performance and Cost

The lowest-cost connector is not always the most economical solution.

A cheaper connector may create:

  • Higher failure risk
  • More maintenance
  • Increased warranty costs

Effective cost optimization focuses on:

Right Specification

Avoid unnecessary features.

Example:

Not every application requires:

  • Premium plating
  • Extreme temperature materials
  • Maximum mating cycles

Production Efficiency

Reduce cost through:

✔ Better tooling design

✔ Automated assembly

✔ Higher yield

✔ Reduced inspection time


Lifecycle Cost

A reliable connector can reduce:

  • Downtime
  • Replacement costs
  • Field failures

The best design optimizes total value, not only unit price.


6.DFM Review Process for Connector Development

A typical connector DFM review includes:

Step 1: Requirement Analysis

Evaluate:

  • Electrical requirements
  • Mechanical conditions
  • Environmental exposure
  • Cost targets

Step 2: Design Review

Check:

  • Structure
  • Materials
  • Tolerances
  • Assembly method

Step 3: Manufacturing Evaluation

Review:

  • Mold feasibility
  • Stamping process
  • Automation possibility
  • Testing requirements

Step 4: Prototype Validation

Perform:

  • Dimensional inspection
  • Electrical testing
  • Mechanical testing
  • Environmental testing

Step 5: Mass Production Optimization

Monitor:

  • Yield
  • Process stability
  • Quality data
  • Cost performance

How FPIC Applies DFM Principles to Connector Development

FPIC supports customers from connector concept development to mass production.

Our engineering approach considers:

  • Application requirements
  • Connector structure
  • Material selection
  • Tooling feasibility
  • Assembly efficiency
  • Quality validation

Through DFM-driven development, FPIC helps customers achieve connectors that are:

✔ Reliable

✔ Manufacturable

✔ Cost-efficient

✔ Ready for mass production


Final Thoughts

A successful connector design requires more than excellent technical specifications.

The best connector balances:

  • Electrical performance
  • Mechanical reliability
  • Manufacturing efficiency
  • Cost control

By applying DFM principles early, engineers can reduce development risks, improve production consistency, and create products that perform reliably in real-world applications.

Good connector design begins before production starts.


FAQ

What does DFM mean in connector design?

DFM means Design for Manufacturing, an approach that optimizes connector design for efficient and reliable production.

Why is DFM important for connectors?

DFM reduces manufacturing problems, improves production yield, lowers cost, and helps ensure consistent quality.

Does DFM reduce connector performance?

No. Proper DFM achieves the required performance while improving manufacturability and cost efficiency.

What factors should be considered during connector DFM?

Engineers should consider materials, tooling, assembly process, tolerances, testing, and production requirements.

When should DFM review happen?

DFM should begin during the early connector design stage before tooling and mass production.


Need a Connector Designed for Mass Production?

FPIC provides customized connector solutions with engineering support from design optimization to volume manufacturing.

With experience in connector development, tooling coordination, assembly, and testing, FPIC helps OEM customers create reliable and production-ready connector solutions.

Contact FPIC today to discuss your connector development project.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Connector testing methods for electrical and mechanical performance evaluation.
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry requirements for cable and harness manufacturing quality.
  3. ISO 9001 Quality Management Systems
    https://www.iso.org/iso-9001-quality-management.html
    Quality management principles supporting consistent manufacturing processes.
  4. IATF 16949 Automotive Quality Management System
    https://www.iatfglobaloversight.org/
    Automotive quality requirements focused on process control and defect prevention.
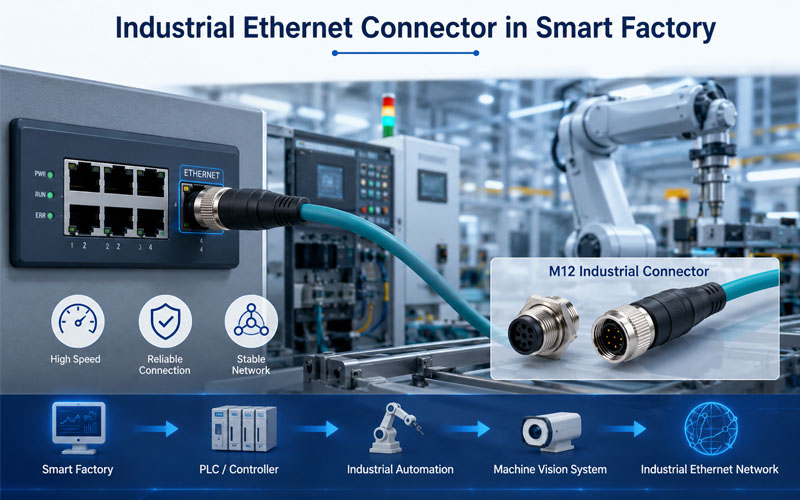
Industrial Ethernet Connector in Smart Factory

Industrial Ethernet has become the communication backbone of modern automation systems. Protocols such as EtherCAT, PROFINET, EtherNet/IP, and Modbus TCP connect PLCs, servo drives, robots, machine vision systems, and distributed I/O with high-speed, real-time data exchange.

As communication speeds continue to increase, engineers often focus on bandwidth, cable category, and protocol compatibility. However, one equally important factor is frequently overlooked—mechanical stability.

Even a connector capable of supporting Gigabit Ethernet can experience intermittent communication if vibration, repeated movement, or unstable contact compromises the physical connection.

This article explores why connector mechanical design is just as important as transmission speed for reliable Industrial Ethernet performance.

Industrial Ethernet Connector in Smart Factory


High-Speed Communication Depends on Stable Physical Connections

Industrial Ethernet transmits high-frequency differential signals that are far more sensitive than conventional power circuits.

Any variation in contact pressure or electrical continuity can negatively affect communication quality.

Poor mechanical stability may result in:

  • Packet loss
  • Increased bit error rate
  • Network reconnection
  • Communication interruptions
  • Unexpected production downtime

For high-speed industrial networks, electrical performance begins with a mechanically reliable connection.


Industrial Environments Are Constantly Moving

Unlike office networks, industrial Ethernet connectors operate under continuous mechanical stress.

Typical sources include:

  • Robot arm acceleration
  • Servo motor vibration
  • Conveyor movement
  • Machine tool impacts
  • AGV and AMR motion
  • Continuous drag chain movement

These conditions can gradually loosen poorly designed connectors or reduce contact stability over time.

Connector reliability must therefore be evaluated under real operating conditions rather than laboratory environments.


Locking Mechanisms Improve Network Reliability

One of the primary functions of an Industrial Ethernet connector is preventing accidental disconnection.

Common locking mechanisms include:

Threaded Locking

Advantages:

  • Excellent vibration resistance
  • High mechanical retention
  • Suitable for permanent installations

Typical applications:

  • Servo systems
  • CNC machines
  • Heavy industrial equipment

Push-Pull Locking

Advantages:

  • Fast installation
  • One-handed operation
  • Secure self-locking
  • Reduced maintenance time

Typical applications:

  • Robotics
  • Medical equipment
  • Automated production lines

Bayonet Locking

Advantages:

  • Quick quarter-turn connection
  • Reliable positioning
  • Good mechanical security

Typical applications:

  • Mobile machinery
  • Outdoor automation
  • Portable industrial equipment

Selecting the correct locking mechanism helps maintain stable Ethernet communication while simplifying maintenance.


Contact Stability Directly Affects Signal Integrity

Industrial Ethernet connectors must maintain consistent electrical contact despite vibration and repeated movement.

Important design factors include:

  • Contact spring design
  • Contact force
  • Gold-plated contacts
  • Precision machining
  • Stable insertion force

High-quality contacts minimize fluctuations in resistance and help preserve signal integrity over long operating periods.


Shielding Is More Than EMI Protection

Industrial environments contain numerous sources of electromagnetic interference, including:

  • Variable frequency drives
  • Servo amplifiers
  • Switching power supplies
  • High-current power cables

Shielded connectors provide:

  • Reduced electromagnetic interference
  • Better signal integrity
  • Stable high-speed communication
  • Lower communication error rates

For maximum EMC performance, connector shielding should include continuous 360° shield termination between the cable braid and the connector housing.


Environmental Protection Supports Long-Term Reliability

Industrial Ethernet connectors are often exposed to:

  • Dust
  • Oil
  • Coolant
  • Moisture
  • Metal particles
  • Cleaning chemicals

Appropriate IP ratings help maintain connector performance in harsh environments.

Typical protection levels include:

IP RatingTypical Application
IP67Industrial automation and robotics
IP68Outdoor automation and renewable energy
IP69KFood processing and washdown equipment

Environmental sealing protects both electrical contacts and communication reliability.


Validation Beyond Data Speed

A connector should never be selected based solely on its data rate specification.

Comprehensive validation should include:

  • Vibration testing
  • Mechanical shock testing
  • Mating cycle testing
  • Contact resistance measurement
  • EMC testing
  • Cable flex testing
  • Environmental sealing verification

Testing complete cable assemblies under real operating conditions provides the most reliable performance assessment.


How FPIC Supports Industrial Ethernet Connectivity

FPIC develops high-performance circular connectors, push-pull self-locking connectors, waterproof connectors, and customized connector assemblies for Industrial Ethernet applications.

Our solutions are engineered to provide reliable locking, stable electrical contacts, effective EMC shielding, and long-term durability for robotics, factory automation, machine vision, servo systems, and intelligent manufacturing equipment. With over 23 years of manufacturing experience, FPIC supports customers from design optimization to mass production.


Final Thoughts

Industrial Ethernet performance depends on far more than bandwidth specifications.

Mechanical stability, secure locking, contact reliability, shielding, and environmental protection all contribute to long-term communication performance.

As factories become increasingly connected and automated, connector design plays a vital role in reducing downtime, maintaining stable network communication, and ensuring reliable operation throughout the equipment lifecycle.


FAQ

Why is mechanical stability important for Industrial Ethernet connectors?

Mechanical stability ensures consistent electrical contact under vibration, motion, and shock, reducing communication interruptions and network failures.

Which locking mechanism is best for Industrial Ethernet?

The best locking mechanism depends on the application. Threaded connectors provide excellent vibration resistance, while push-pull connectors offer faster maintenance and secure self-locking.

Do Industrial Ethernet connectors require shielding?

Yes. Shielded connectors help reduce electromagnetic interference (EMI), improve signal integrity, and support reliable high-speed communication.

What IP rating is recommended for Industrial Ethernet connectors?

IP67 is suitable for many factory automation applications, while IP68 or IP69K may be required for outdoor or washdown environments.

How should Industrial Ethernet connectors be tested?

Recommended tests include vibration, EMC, contact resistance, mating cycles, cable flex, mechanical shock, and environmental sealing.


Looking for Reliable Industrial Ethernet Connector Solutions?

FPIC provides high-performance circular connectors, push-pull self-locking connectors, and customized Industrial Ethernet connectivity solutions for robotics, factory automation, machine vision, and intelligent manufacturing. Our engineering team helps customers achieve reliable communication through robust mechanical design, effective shielding, and application-specific connector solutions.

Contact FPIC today to discuss your Industrial Ethernet connector requirements.


Resources

  1. IEC 61076 – Connectors for Electrical and Electronic Equipment
    https://webstore.iec.ch/
    International standards covering the design, testing, and performance of industrial and circular connectors.
  2. IEC 61158 – Industrial Communication Networks (Fieldbus Specifications)
    https://webstore.iec.ch/
    Defines communication standards widely used in industrial Ethernet and automation networks.
  3. ODVA – EtherNet/IP Technology Overview
    https://www.odva.org/
    Provides technical guidance on EtherNet/IP architecture, industrial networking, and physical connectivity.
  4. PROFIBUS & PROFINET International (PI)
    https://www.profibus.com/
    Offers technical resources for PROFINET communication, connector requirements, and industrial networking best practices.
  5. Phoenix Contact – Industrial Ethernet Connectivity Solutions
    https://www.phoenixcontact.com/
    Provides engineering resources on Industrial Ethernet connectors, shielding, and reliable network infrastructure.
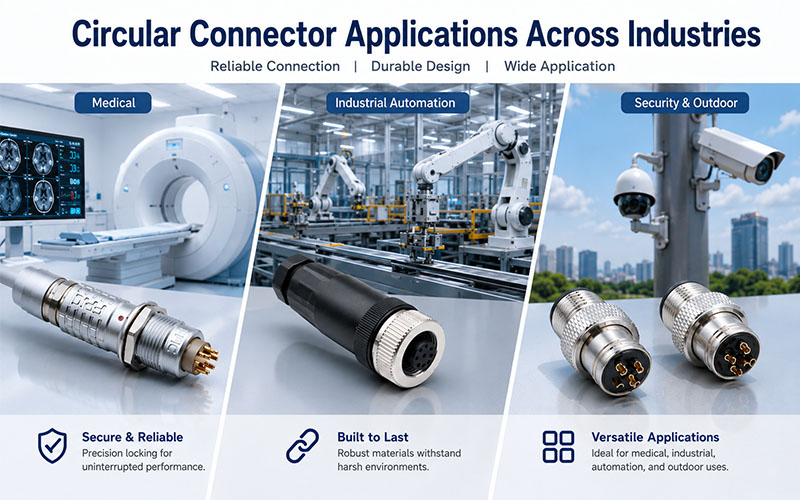
Circular Connector Applications Across Industries

Circular connectors are widely used because they combine compact size, reliable electrical performance, and excellent environmental protection. From medical imaging systems and industrial robots to outdoor automation and renewable energy equipment, they provide dependable connections for power, signal, and data transmission.

However, there is no universal circular connector suitable for every application. A connector designed for a surgical device may not survive on construction machinery, while an outdoor waterproof connector may be unnecessarily large for laboratory equipment.

Selecting the right connector requires balancing electrical performance, environmental protection, mechanical reliability, and maintenance requirements.

This guide explains the most important factors engineers should consider when choosing circular connectors for different industries.

Circular Connector Applications Across Industries


Start with the Application Environment

Before comparing connector specifications, first understand where the connector will operate.

Typical environments include:

Medical Equipment

  • Diagnostic systems
  • Patient monitoring devices
  • Surgical equipment
  • Laboratory instruments

Design priorities:

  • Compact size
  • Frequent cleaning
  • High mating reliability
  • Excellent signal integrity

Industrial Automation

Typical applications include:

  • Industrial robots
  • Servo motors
  • PLC control systems
  • Machine tools
  • Factory automation

Design priorities:

  • Vibration resistance
  • EMC performance
  • High mating durability
  • Reliable locking

Outdoor Equipment

Typical applications include:

  • Renewable energy systems
  • Agricultural machinery
  • Construction equipment
  • Rail transportation
  • EV charging infrastructure

Design priorities:

  • Waterproof sealing
  • UV resistance
  • Corrosion resistance
  • Wide operating temperature

Different environments require different connector designs.


Choose the Appropriate Locking Mechanism

Connector locking directly affects operational reliability.

Common options include:

Push-Pull Locking

Advantages:

  • Fast connection
  • One-hand operation
  • Easy maintenance
  • Secure automatic locking

Ideal for:

  • Medical equipment
  • Laboratory systems
  • Collaborative robots

Threaded Locking

Advantages:

  • Excellent vibration resistance
  • Strong mechanical retention
  • Long-term stability

Ideal for:

  • Industrial automation
  • Servo systems
  • Heavy equipment

Bayonet Locking

Advantages:

  • Quick quarter-turn locking
  • Reliable positioning
  • Outdoor suitability

Ideal for:

  • Portable equipment
  • Field instruments
  • Mobile machinery

Consider Environmental Protection

Environmental sealing is critical when connectors are exposed to dust, water, oil, or cleaning chemicals.

Common protection levels include:

IP Rating                Typical Applications

IP67                         Industrial automation, robotics

IP68                        Outdoor automation, renewable energy

IP69K                      Food processing, washdown equipment, heavy-duty vehicles

The required protection level should match the actual operating conditions rather than simply selecting the highest rating available.


Evaluate EMC Requirements

Modern equipment often combines:

  • Power transmission
  • Industrial Ethernet
  • CAN Bus
  • High-speed data
  • Precision sensors

Shielded circular connectors help:

  • Reduce EMI
  • Improve signal integrity
  • Maintain communication stability
  • Support reliable automation

For high-speed communication, connector shielding should include proper 360° shield termination.


Select the Right Contact Configuration

Connector selection also depends on:

  • Number of contacts
  • Signal type
  • Power rating
  • Mixed power and signal transmission

Many applications combine:

  • Power contacts
  • Signal contacts
  • Data contacts
  • Ground contacts

Hybrid connectors simplify installation while reducing cable complexity.


Consider Mating Cycle Requirements

Some connectors remain installed for years.

Others are connected and disconnected daily.

Typical examples include:

Low Mating Frequency

  • Wind turbines
  • Energy storage systems
  • Control cabinets

High Mating Frequency

  • Medical devices
  • Test equipment
  • Portable instruments

Applications with frequent reconnection should prioritize connectors designed for thousands of mating cycles.


Material Selection Matters

Connector housing materials influence durability and EMC performance.

Common choices include:

Metal Housing

Advantages:

  • Better shielding
  • Higher mechanical strength
  • Improved heat dissipation

Engineering Plastic Housing

Advantages:

  • Lightweight
  • Corrosion resistant
  • Cost-effective

Material selection should reflect the environmental and mechanical demands of the application.


Validate Before Production

Connector selection should always be verified through testing.

Recommended evaluations include:

  • Mating cycle testing
  • Vibration testing
  • Salt spray testing
  • IP protection testing
  • Contact resistance testing
  • EMC verification
  • Temperature cycling

Testing complete connector assemblies under actual operating conditions provides the highest confidence in long-term performance.


How FPIC Supports Circular Connector Applications

FPIC develops circular connectors, push-pull self-locking connectors, waterproof connectors, and customized connectivity solutions for medical equipment, industrial automation, robotics, renewable energy, and outdoor applications.

With more than 23 years of manufacturing experience, our engineering team helps customers select the right connector based on electrical performance, environmental requirements, mechanical reliability, and application-specific standards. From prototype development to mass production, FPIC provides dependable connector solutions designed for long-term performance.


Final Thoughts

Choosing the right circular connector involves much more than selecting the correct number of contacts.

Engineers must consider the operating environment, locking mechanism, environmental sealing, EMC performance, durability, and maintenance requirements together

Whether designing a medical device, an industrial robot, or an outdoor energy system, selecting the appropriate connector improves equipment reliability, simplifies maintenance, and reduces lifecycle costs.


FAQ

What factors should be considered when choosing a circular connector?

Key factors include application environment, IP protection, locking mechanism, shielding, contact configuration, mating cycles, and environmental durability.

Which locking mechanism is best for medical equipment?

Push-pull connectors are widely used in medical equipment because they provide fast, secure, one-handed operation and support frequent mating cycles.

Is IP69K always better than IP67?

Not necessarily. The appropriate IP rating should match the operating environment. Higher protection levels may increase size and cost without adding practical benefits.

When are shielded circular connectors required?

Shielded connectors are recommended for applications involving Industrial Ethernet, CAN Bus, servo systems, or environments with significant electromagnetic interference.

Why is mating cycle life important?

Applications requiring frequent connection and disconnection need connectors with high mating durability to maintain reliable electrical performance over time.


Looking for the Right Circular Connector for Your Application?

Whether you’re designing medical equipment, industrial automation systems, or outdoor electrical installations, FPIC provides high-quality circular connectors, push-pull self-locking connectors, and waterproof connectivity solutions tailored to your application. Our engineering team can help you select the ideal connector for reliable performance in demanding environments.

Contact FPIC today to discuss your circular connector requirements.


Resources

  1. IEC 61076 – Connectors for Electrical and Electronic Equipment
    https://webstore.iec.ch/
    Provides international standards for the design, performance, and testing of circular and industrial connectors.
  2. IEC 60529 – Degrees of Protection Provided by Enclosures (IP Code)
    https://webstore.iec.ch/
    Defines IP67, IP68, and IP69K protection ratings for connectors used in industrial and outdoor environments.
  3. IEC 60601-1 – Medical Electrical Equipment
    https://webstore.iec.ch/
    Specifies general safety and essential performance requirements for medical electrical equipment, including connector-related considerations.
  4. Phoenix Contact – Circular Connectors for Industrial Applications
    https://www.phoenixcontact.com/
    Provides technical information on circular connector selection, industrial connectivity, and environmental protection.
  5. TE Connectivity – Circular Connector Solutions
    https://www.te.com/
    Offers engineering resources on circular connectors for medical devices, industrial automation, transportation, and energy applications.
Common Shield Termination Mistakes

As industrial automation systems continue to adopt high-speed communication protocols such as Industrial Ethernet, EtherCAT, PROFINET, and CAN Bus, electromagnetic compatibility (EMC) has become an essential part of circular connector design.

While engineers often focus on cable shielding, one critical detail is frequently overlooked—the shield termination inside the connector.

A high-quality shielded cable can still perform poorly if the shield is improperly terminated. In many EMC failures, the connector itself is not the problem; rather, it is the way the shield is connected.

This article explains the most common shield termination mistakes found in circular connectors and provides practical recommendations for improving EMC performance.

360° Shield Termination vs Pigtail Grounding


What Is Shield Termination?

Shield termination refers to the method used to electrically connect the cable shield to the connector housing or grounding system.

Its purpose is to:

  • Maintain shield continuity
  • Minimize electromagnetic emissions
  • Improve immunity against external interference
  • Provide a low-impedance path for high-frequency noise

A properly terminated shield allows electromagnetic energy to flow safely to ground instead of coupling into nearby signal conductors.


Why Shield Termination Matters

Modern industrial equipment contains numerous EMI sources, including:

  • Servo drives
  • Frequency inverters
  • Switching power supplies
  • Industrial Ethernet
  • High-speed digital communication
  • High-current power cables

Without effective shield termination, these noise sources may result in:

  • Communication failures
  • Packet loss
  • Encoder errors
  • Sensor instability
  • Unexpected equipment shutdown

Proper shield termination is often the difference between passing and failing EMC testing.


Common Mistake #1: Pigtail Grounding

One of the most common installation mistakes is connecting the shield through a long drain wire or “pigtail.”

Although convenient, this creates additional inductance that significantly reduces shielding effectiveness at high frequencies.

Recommended practice:

  • Avoid long pigtails.
  • Use direct 360° shield termination whenever possible.

Common Mistake #2: Incomplete 360° Shield Contact

Some connectors only contact a small portion of the cable braid.

This creates gaps in the shielding path and allows electromagnetic energy to leak.

Good shield termination should provide:

  • Full circumferential contact
  • Uniform pressure
  • Continuous metal-to-metal connection

Complete 360° termination offers substantially better EMC performance.

Common Shield Termination Mistakes


Common Mistake #3: Poor Shield Continuity

The shield should remain electrically continuous from one connector to the other.

Common problems include:

  • Broken braid
  • Damaged foil
  • Poor crimping
  • Loose shield clamps
  • Oxidized metal surfaces

Even small discontinuities may reduce shielding effectiveness.


Common Mistake #4: Incorrect Grounding Strategy

Shield grounding depends on system architecture.

Single-end grounding may reduce low-frequency ground loops.

Dual-end grounding generally provides better high-frequency EMC performance.

The appropriate strategy should be selected according to:

  • Operating frequency
  • Equipment layout
  • Grounding system
  • EMC requirements

There is no universal solution for every application.


Common Mistake #5: Ignoring Connector Housing Material

Plastic connector shells provide little shielding capability.

For demanding industrial environments, engineers often prefer:

  • Metal circular connectors
  • Conductive connector shells
  • Nickel-plated housings
  • Aluminum alloy housings

Metal housings improve overall shielding continuity and EMC performance.


Selecting Connectors for High EMC Applications

When selecting circular connectors for robotics, industrial automation, or energy storage systems, engineers should evaluate:

  • 360° shield termination
  • Metal housing
  • Shield continuity
  • Contact resistance
  • IP protection level
  • Vibration resistance
  • Mating cycle durability

Connector performance should be evaluated as part of the complete cable assembly rather than as an individual component.


Verifying Shield Performance

Proper shield termination should be validated through testing.

Typical evaluations include:

  • Shield continuity measurement
  • Contact resistance testing
  • Radiated emission testing
  • Conducted emission testing
  • EMC immunity testing
  • High-frequency impedance measurement
  • Cable flex testing

Laboratory verification ensures consistent EMC performance before production.

Shielded Circular Connector EMC Design


Industry Standards

Shielded circular connectors commonly reference:

  • IEC 61000 Series — Electromagnetic Compatibility (EMC)
  • IEC 61076 Series — Connectors for Electronic Equipment
  • CISPR 11 — Industrial Equipment Emissions
  • CISPR 32 — Multimedia Equipment EMC Requirements
  • IEC 60512 — Connector Mechanical and Electrical Tests

Compliance with these standards helps ensure reliable operation in industrial environments.


How FPIC Supports EMC Connector Solutions

FPIC develops circular connectors, push-pull self-locking connectors, and customized connector assemblies for industrial automation, robotics, medical devices, and energy storage applications.

Our engineering team focuses on optimized shield termination, reliable connector grounding, and robust mechanical design to help customers achieve stable signal transmission and improved EMC performance in demanding environments.


Final Thoughts

Shield termination is one of the most important—but often overlooked—factors affecting connector EMC performance.

Even the highest-quality shielded cable cannot compensate for poor connector termination.

By using proper 360° shield termination, maintaining continuous shielding, selecting appropriate connector materials, and validating EMC performance, engineers can significantly improve communication reliability and reduce electromagnetic interference.

As industrial communication speeds continue to increase, connector shield termination will play an even greater role in system performance.


FAQ

What is shield termination in a circular connector?

Shield termination is the electrical connection between the cable shield and the connector housing or grounding system, providing a controlled path for electromagnetic noise.

Why is a 360° shield termination better than a pigtail?

A 360° termination minimizes high-frequency impedance and provides continuous shielding around the cable, while pigtails introduce inductance that reduces EMC performance.

Do metal connector housings improve EMC?

Yes. Metal housings help maintain shield continuity and provide better electromagnetic shielding than plastic housings.

Should cable shields be grounded at one end or both ends?

The best grounding method depends on operating frequency, grounding architecture, and EMC requirements. High-frequency applications often benefit from dual-end grounding.

How is shield termination verified?

Common tests include shield continuity, contact resistance, EMC emissions, immunity testing, and high-frequency performance evaluation.


Looking for High-Performance Shielded Circular Connectors?

Reliable EMC performance begins with proper connector design. FPIC provides shielded circular connectors, push-pull self-locking connectors, and custom connector solutions engineered for industrial automation, robotics, medical equipment, and energy storage systems. Our engineering team supports customers with optimized shielding, connector integration, and reliable manufacturing for demanding applications.

Contact FPIC today to discuss your EMC connector requirements.


Resources

  1. IEC 61000 Series – Electromagnetic Compatibility (EMC)
    https://webstore.iec.ch/
    International EMC standards covering electromagnetic emissions, immunity, and grounding practices.
  2. IEC 61076 Series – Connectors for Electrical and Electronic Equipment
    https://webstore.iec.ch/
    Provides international standards for the design, testing, and performance of circular and industrial connectors.
  3. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://webstore.iec.ch/
    Specifies mechanical, electrical, and environmental test methods for connector assemblies.
  4. Phoenix Contact – EMC Connection Technology
    https://www.phoenixcontact.com/
    Explains shield termination, grounding concepts, and EMC best practices for industrial connectors.
  5. TE Connectivity – EMC Shielding Solutions for Industrial Connectivity
    https://www.te.com/
    Provides technical guidance on connector shielding, 360° shield termination, and high-speed industrial communication.
Robotics Connector Selection Guide

Industrial robots operate in demanding environments where connectors are exposed to constant motion, vibration, electromagnetic interference (EMI), and frequent maintenance. While much attention is often given to servo motors and robot controllers, connector selection is equally important for ensuring reliable power delivery and stable signal transmission.

A poorly selected connector can loosen under vibration, introduce communication errors, restrict cable movement, or shorten cable life. Choosing the right connector requires more than matching the voltage and current ratings—it involves evaluating the complete operating environment.

This article explains the key considerations when selecting connectors for robotic systems, focusing on locking mechanisms, EMC shielding, cable exit orientation, and long-term durability.

Robotics Connector Selection Guide


Why Connector Selection Matters in Robotics

Unlike stationary industrial equipment, robotic systems perform continuous multi-axis movements that repeatedly bend, twist, and accelerate cables.

Connectors must therefore withstand:

  • Continuous vibration
  • Frequent movement
  • Mechanical shock
  • Electromagnetic interference
  • Repeated mating cycles
  • Limited installation space

Connector reliability directly influences machine uptime and maintenance costs.


Choosing the Right Locking Mechanism

One of the most critical connector features is the locking system.

A connector that loosens during robot operation can interrupt power or communication, causing unexpected machine stops.

Common locking mechanisms include:

Threaded Locking

Advantages:

  • Excellent vibration resistance
  • High mechanical strength
  • Suitable for industrial automation

Applications:

  • Servo motors
  • Industrial robots
  • Machine tools

Push-Pull Locking

Advantages:

  • Quick connection and disconnection
  • Secure automatic locking
  • Compact design
  • Fast maintenance

Applications:

  • Collaborative robots (Cobots)
  • Medical robots
  • Inspection equipment
  • Automated production lines

Bayonet Locking

Advantages:

  • Fast quarter-turn locking
  • Good vibration performance
  • Reliable positioning

Applications:

  • Mobile robots
  • Outdoor equipment
  • Industrial machinery

Selecting the locking method should balance installation efficiency with vibration resistance.

Comparison of Connector Locking Mechanisms


Why Shielding Is Essential

Modern robots contain numerous high-speed electrical devices, including:

  • Servo drives
  • Frequency converters
  • Industrial Ethernet
  • Encoders
  • Vision systems

These devices generate electromagnetic interference that may affect communication signals.

Shielded connectors help:

  • Reduce EMI
  • Improve signal integrity
  • Lower communication errors
  • Support high-speed data transmission

Proper shield continuity between cable and connector is essential for achieving effective EMC performance.


Selecting the Best Cable Exit Direction

Cable exit orientation is often overlooked during connector selection.

However, it directly affects cable stress and available installation space.

Typical exit options include:

Straight Exit

Best for:

  • Open installation space
  • Linear cable routing
  • Easy assembly

Right-Angle Exit

Best for:

  • Compact robot joints
  • Tight cabinet layouts
  • Reduced bending stress
  • Improved cable management

Proper cable exit selection helps extend cable flex life and minimizes mechanical strain near the connector.


Environmental Protection Requirements

Robots frequently operate in challenging environments.

Connector selection should consider:

  • Dust
  • Water spray
  • Oil
  • Coolant
  • Metal particles
  • Cleaning chemicals

Depending on the application, connectors may require:

  • IP67 protection
  • IP68 protection
  • IP69K protection

Environmental sealing improves long-term reliability and reduces maintenance frequency.


Connector Durability and Mating Cycles

Industrial robots often require periodic replacement of end effectors or tooling.

Frequent connection and disconnection demand connectors with long mating life.

Typical industrial requirements include:

  • More than 500 insertion cycles
  • 2,000–5,000 cycles for automation equipment
  • Higher durability for collaborative robots and testing equipment

Gold-plated contacts further improve contact stability and corrosion resistance.


Size and Weight Considerations

As robots become smaller and faster, connector size becomes increasingly important.

Compact connectors provide:

  • Lower moving mass
  • Improved joint flexibility
  • Easier cable routing
  • Better space utilization

Miniaturization is especially important in collaborative robots and precision automation equipment.


Validation Before Deployment

Connectors should be validated under realistic operating conditions.

Recommended tests include:

  • Vibration testing
  • Mechanical shock testing
  • Cable flex testing
  • Salt spray testing
  • Contact resistance measurement
  • Insertion and extraction force testing
  • EMC verification
  • Environmental sealing tests

System-level validation provides the highest confidence in connector performance.


How FPIC Supports Robotics Connector Solutions

FPIC develops high-performance connector solutions for industrial automation, robotics, and intelligent manufacturing.

Our product portfolio includes push-pull self-locking connectors, circular connectors, waterproof connectors, and customized connector assemblies designed for demanding robotic applications. With over 23 years of manufacturing experience, FPIC supports customers from rapid prototyping through mass production, providing reliable connectivity solutions that improve equipment uptime and long-term performance.


Final Thoughts

Selecting the right connector for robotic applications involves much more than matching electrical specifications.

Locking mechanisms, shielding performance, cable exit orientation, environmental protection, and durability all influence system reliability.

As robotic systems continue to become faster, smarter, and more compact, connector design plays an increasingly important role in maintaining stable operation and reducing maintenance costs.


FAQ

Why are locking connectors important in robotics?

Locking mechanisms prevent accidental disconnection caused by vibration, motion, or mechanical shock, improving system reliability.

When should shielded connectors be used?

Shielded connectors are recommended whenever high-speed communication or servo systems operate in environments with significant electromagnetic interference.

Which cable exit is better, straight or right-angle?

It depends on available space and cable routing. Right-angle exits are often preferred in compact robot joints to reduce bending stress.

What IP rating is recommended for industrial robots?

Many industrial robots require IP67 protection, while washdown or outdoor applications may require IP68 or IP69K connectors.

How are robotics connectors validated?

Typical validation includes vibration, cable flex, EMC, sealing, mating cycle, and contact resistance testing.


Looking for Reliable Connectors for Robotics and Industrial Automation?

FPIC provides high-performance connector solutions for industrial robots, collaborative robots, servo systems, and automated equipment. From push-pull self-locking connectors to waterproof circular connectors, our engineering team helps customers select the right connectivity solution for demanding motion applications.

Contact FPIC today to discuss your robotics connector requirements.


Resources

  1. IEC 60529 – Degrees of Protection Provided by Enclosures (IP Code)
    https://webstore.iec.ch/
    Defines IP ratings such as IP67, IP68, and IP69K for connector protection against dust and water ingress.
  2. IEC 61076 – Connectors for Electrical and Electronic Equipment
    https://webstore.iec.ch/
    International standards covering the design, performance, and testing of industrial connectors.
  3. ODVA – EtherNet/IP Physical Layer and Industrial Connectivity
    https://www.odva.org/
    Provides technical guidance on industrial Ethernet connectivity and connector performance in automation systems.
  4. TE Connectivity – Industrial Robotics Connectivity Solutions
    https://www.te.com/
    Explains connector technologies, shielding solutions, and rugged interconnect systems for robotics and automation.
  5. Phoenix Contact – Connectors for Industrial Automation
    https://www.phoenixcontact.com/
    Offers technical resources on circular connectors, EMC protection, and reliable industrial connectivity.
IP67 vs IP68 vs IP69K Connectors Protection Comparison

When selecting industrial connectors, one of the first specifications engineers notice is the IP rating. Products are commonly advertised as IP67, IP68, or IP69K, often implying that a higher number automatically means better protection.

However, this assumption is not always correct.

Each protection level is designed for different environmental conditions, and choosing the wrong rating can either reduce equipment reliability or unnecessarily increase product cost.

This article explains what IP67, IP68, and IP69K ratings actually mean, how they are tested, and how engineers should interpret these ratings in real-world applications.

IP67 vs IP68 vs IP69K Connectors Protection Comparison


Understanding the IP Rating System

The Ingress Protection (IP) rating is defined by IEC 60529, an international standard used to classify the degree of protection provided by electrical enclosures against solid particles and liquids.

An IP rating consists of two digits.

  • The first digit indicates protection against solid objects and dust.
  • The second digit indicates protection against water.

For industrial connectors, the first digit is commonly 6, representing complete protection against dust ingress.

The primary difference between IP67, IP68, and IP69K lies in their resistance to water under different conditions.


What Does IP67 Mean?

IP67 is one of the most common protection ratings used in industrial automation.

A connector meeting IP67 requirements must:

  • Be completely dust-tight (IP6X)
  • Withstand temporary immersion in water up to 1 meter for 30 minutes

Typical Applications

IP67 connectors are commonly used in:

  • Industrial automation equipment
  • Sensors
  • Factory machinery
  • AGVs
  • Warehouse automation
  • Outdoor lighting

What IP67 Does Not Mean

One common misconception is that IP67 connectors are suitable for continuous underwater operation.

In reality, IP67 is designed for temporary immersion only. Continuous submersion may eventually compromise the sealing system unless the connector is specifically designed for that environment.


What Does IP68 Mean?

IP68 provides protection against continuous immersion.

Unlike IP67, IEC 60529 does not specify a fixed immersion depth or duration.

Instead, the manufacturer defines the test conditions.

Typical examples include:

  • 2 meters for 24 hours
  • 5 meters for 48 hours
  • Other application-specific requirements

Because of this flexibility, two IP68 connectors may have significantly different underwater performance.

Typical Applications

IP68 connectors are often selected for:

  • Marine equipment
  • Underground monitoring systems
  • Water treatment facilities
  • Outdoor telecommunications
  • Renewable energy systems

When comparing IP68 products, engineers should always verify the manufacturer’s immersion specifications rather than relying solely on the IP rating.


What Does IP69K Mean?

IP69K addresses a completely different challenge.

Instead of prolonged immersion, IP69K evaluates resistance to high-pressure, high-temperature water jets.

During testing, connectors are exposed to:

  • Water temperatures up to 80°C
  • Pressures around 80–100 bar
  • Spray angles of 0°, 30°, 60°, and 90°
  • Rotating spray conditions

The objective is to verify sealing performance during aggressive cleaning processes.

Typical Applications

IP69K connectors are widely used in:

  • Food processing equipment
  • Beverage production
  • Pharmaceutical manufacturing
  • Agricultural machinery
  • Construction equipment
  • Commercial vehicles

Frequent washdown environments often require IP69K rather than IP68.

IP67 vs IP68 vs IP69K Connectors Application


IP67 vs IP68 vs IP69K: A Practical Comparison

FeatureIP67IP68IP69K
Dust ProtectionYesYesYes
Temporary Water ImmersionNot primary purpose
Continuous SubmersionLimitedNot designed for this
High-Pressure WashdownLimited
High-Temperature Cleaning

The table shows that none of these ratings is universally “better.” Each addresses a different environmental challenge.


Common Misconceptions About IP Ratings

Higher IP Ratings Are Not Always Better

Selecting IP69K for a machine that only requires occasional rain exposure may increase cost without providing additional practical benefits.

Conversely, using IP67 in a high-pressure washdown environment may result in premature seal failure.

IP68 Is Not a Universal Underwater Rating

Because manufacturers define immersion conditions, engineers should always request the specific IP68 test parameters.

Connector Design Matters

Even when connectors share the same IP rating, long-term field performance depends on factors such as:

  • sealing materials
  • connector locking mechanism
  • cable gland quality
  • installation practices
  • maintenance procedures

Proper installation is just as important as connector selection.


Additional Factors Beyond the IP Rating

An IP rating only evaluates protection against dust and water.

Industrial connector selection should also consider:

  • vibration resistance
  • operating temperature
  • UV resistance
  • chemical compatibility
  • mating cycle life
  • corrosion resistance
  • EMC shielding

In harsh environments, these characteristics often determine connector reliability more than the IP rating itself.


Validation in Real Applications

Field validation should include tests that reflect actual operating conditions.

Typical validation activities include:

  • water immersion testing
  • pressure wash testing
  • thermal cycling
  • vibration testing
  • salt spray testing
  • connector durability testing
  • sealing inspection after repeated mating cycles

Laboratory certification alone does not guarantee long-term field reliability.


How FPIC Supports Sealed Connector Development

Selecting the correct protection level requires understanding the actual operating environment rather than simply choosing the highest IP rating.

FPIC develops custom connector and cable assembly solutions for industrial automation, robotics, energy storage, transportation, medical equipment, and harsh-environment applications. Our engineering team supports customers in selecting sealing structures, connector configurations, and validation methods that match real operating conditions while balancing performance, durability, and cost.


Final Thoughts

IP67, IP68, and IP69K are often misunderstood as progressive levels of waterproof performance.

In reality, each rating addresses different environmental conditions.

Understanding the testing methods behind these ratings allows engineers to make better connector selections, improve equipment reliability, and avoid unnecessary costs.

Rather than asking which rating is higher, the more important question is:

Which rating best matches the actual application?


FAQ

Is IP69K better than IP68?

Not necessarily. IP69K is designed for high-pressure, high-temperature washdown, while IP68 is intended for continuous water immersion.

Can an IP67 connector be used underwater?

Only for temporary immersion. Continuous underwater applications generally require a connector specifically qualified for IP68 conditions.

Does IP68 always mean the same immersion depth?

No. The immersion depth and duration are defined by the manufacturer and should always be verified.

Are IP69K connectors also dustproof?

Yes. Like IP67 and IP68, IP69K connectors provide complete protection against dust ingress.

What other factors should be considered besides IP ratings?

Engineers should also evaluate vibration resistance, temperature range, UV resistance, chemical compatibility, mating cycle life, and corrosion resistance.


Looking for Reliable Sealed Connector Solutions?

Choosing the right IP rating is only one part of connector selection. FPIC provides custom sealed connectors and cable assemblies engineered for demanding industrial environments, helping customers improve equipment reliability while avoiding unnecessary design costs.

Contact FPIC today to discuss your application requirements.


Resources

  1. IEC 60529 – Degrees of Protection Provided by Enclosures (IP Code): Defines the international IP rating system, including IP67 and IP68 test requirements.
  2. ISO 20653 – Road Vehicles – Degrees of Protection (IP Code): Specifies IP69K testing methods for high-pressure, high-temperature water jet protection used in automotive and industrial applications.
  3. Phoenix Contact – IP Protection Classes Explained: Explains how IP ratings apply to industrial connectors and highlights practical selection considerations.
  4. TE Connectivity – Sealed Connector Solutions: Discusses sealing technologies, environmental performance, and connector selection for harsh environments.
  5. UL Solutions – Environmental Testing Services: Provides an overview of environmental validation methods, including water ingress, thermal cycling, and durability testing.
Single Pair Ethernet Connectors Overview

Industrial automation networks are entering a new phase of connectivity.

For decades, factory communication systems have relied on:

  • Fieldbus networks
  • Industrial Ethernet
  • M8 and M12 connectors
  • RJ45 interfaces
  • Multi-pair communication cables

Today, Single Pair Ethernet (SPE) is emerging as one of the most important technologies supporting Industry 4.0, IIoT, and smart manufacturing initiatives.

While SPE has been discussed for several years, 2026 is expected to be a significant milestone as more industrial equipment manufacturers move from pilot projects to commercial deployment.

For engineers, OEM buyers, and system integrators, understanding upcoming SPE connector trends can help guide future product and infrastructure decisions.

Single Pair Ethernet Connectors Overview


Why SPE Is Gaining Momentum

Industrial networks continue to evolve toward greater connectivity.

Factories now require:

  • more sensors
  • more data collection
  • more edge devices
  • more intelligent actuators

Traditional Ethernet remains effective, but many field-level devices do not require the size and complexity of four-pair Ethernet infrastructure.

Single Pair Ethernet offers:

  • reduced cable size
  • lighter harnesses
  • simplified installation
  • Ethernet-based communication down to the sensor level

This makes SPE highly attractive for next-generation automation architectures.


Trend #1: Increasing Adoption of IEC 63171 Connector Standards

One of the biggest developments to watch in 2026 is the growing acceptance of IEC 63171 connector standards.

These standards define connector interfaces for SPE applications.

Common variants include:

  • IEC 63171-2
  • IEC 63171-5
  • IEC 63171-6

As more automation suppliers adopt standardized interfaces, interoperability across equipment platforms is expected to improve.

For buyers, connector standard compatibility will become an increasingly important procurement criterion.


Trend #2: Expansion of SPE in Smart Sensors and Actuators

Many industrial sensors currently use:

  • discrete I/O
  • fieldbus interfaces
  • proprietary communication methods

SPE enables direct Ethernet connectivity to field devices.

Benefits include:

  • simplified architectures
  • real-time diagnostics
  • easier device integration
  • reduced gateway requirements

By 2026, more sensor and actuator manufacturers are expected to release SPE-enabled products.


Trend #3: Growth of Power over Data Line (PoDL)

Power over Data Line (PoDL) remains one of the most compelling SPE features.

PoDL allows:

  • data transmission
  • device power

through the same twisted pair.

Potential advantages include:

  • fewer cables
  • reduced installation costs
  • smaller harnesses
  • simplified device deployment

As SPE ecosystems mature, PoDL adoption is expected to accelerate across industrial automation markets.


Trend #4: Smaller and More Compact Industrial Devices

Machine builders continue to pursue:

  • smaller equipment footprints
  • higher device density
  • reduced cabinet space

SPE connectors support these goals through:

  • compact connector designs
  • reduced cable diameter
  • lighter cable assemblies

This trend is particularly important in:

  • robotics
  • machine vision
  • semiconductor equipment
  • compact automation cells

Connector miniaturization will remain a major development focus in 2026.


Trend #5: Stronger Focus on EMC Performance

As industrial networks become more data-driven, communication reliability becomes increasingly critical.

Industrial environments contain significant sources of electromagnetic interference:

  • servo drives
  • VFDs
  • motors
  • switching power supplies

Although SPE cables are smaller, EMC challenges remain.

Future SPE connector development will likely emphasize:

  • improved shielding
  • lower transfer impedance
  • optimized grounding
  • enhanced connector shielding continuity

EMC performance will continue to be a key differentiator among suppliers.


Trend #6: More SPE Solutions for Robotics

Robotic systems require communication solutions that can withstand:

  • continuous flexing
  • torsion
  • vibration

As robots become more connected, SPE presents an opportunity to simplify communication architectures.

However, robotic SPE cable assemblies must still address:

  • dynamic motion
  • shielding durability
  • flex life requirements

2026 may see a broader range of SPE products specifically designed for robotic applications.


Trend #7: Integration with Industry 4.0 Architectures

Industry 4.0 initiatives emphasize:

  • unified communication
  • real-time data access
  • device interoperability

SPE aligns closely with these goals.

Benefits include:

  • end-to-end Ethernet connectivity
  • simplified networking
  • easier data collection
  • scalable architectures

Many manufacturers view SPE as a foundational technology for future smart factories.


Trend #8: Growing Demand for Hybrid Connectivity Solutions

The transition to SPE will not happen overnight.

Many facilities will operate mixed environments including:

  • traditional Ethernet
  • fieldbus networks
  • SPE networks

As a result, demand is growing for:

  • SPE-to-Ethernet adapters
  • hybrid cable assemblies
  • migration-friendly connectivity solutions

Suppliers that support both legacy and emerging standards may have a competitive advantage.


Trend #9: Higher Expectations for IP Protection

Industrial users continue to demand robust environmental protection.

Common requirements include:

IP67

Factory automation equipment.

IP68

Harsh industrial environments.

IP69K

Washdown applications.

Future SPE connectors will need to maintain industrial-grade sealing despite smaller form factors.


Trend #10: Supplier Qualification Will Become More Important

As SPE adoption grows, buyers will increasingly evaluate suppliers based on:

  • connector standard compliance
  • EMC performance
  • environmental testing
  • manufacturing quality
  • application engineering support

Selecting the right connectivity partner may become as important as selecting the connector itself.


Challenges That Still Need Attention

Although SPE offers significant advantages, several challenges remain.

Standard Fragmentation

Multiple connector standards continue to coexist.

Ecosystem Maturity

Some industrial markets are still in the early adoption phase.

Infrastructure Transition

Existing Ethernet systems remain deeply established.

Education and Training

Many engineers are still learning SPE design principles.

These factors will influence adoption rates over the coming years.


Questions Buyers Should Ask in 2026

Before selecting SPE connector solutions, buyers should ask:

  • Which IEC 63171 standard is supported?
  • Is PoDL available?
  • What EMC testing has been completed?
  • What IP protection level is achieved?
  • Is the connector suitable for robotics or drag-chain applications?
  • What interoperability testing has been performed?
  • How does the supplier support future scalability?

Typical Applications Expected to Grow

SPE connectors are expected to expand across:

  • Smart sensors
  • Intelligent actuators
  • Industrial IoT devices
  • Edge computing equipment
  • Robotics
  • Machine vision systems
  • Process automation
  • Smart manufacturing platforms

How FPIC Supports Emerging SPE Connectivity Needs

FPIC develops advanced industrial connectivity solutions including:

  • SPE cable assemblies
  • Industrial Ethernet harnesses
  • M8 and M12 communication cables
  • Shielded data cable assemblies
  • Robotic communication harnesses
  • Custom overmolded connector solutions

Our engineering team helps customers evaluate emerging connectivity technologies while maintaining compatibility with current industrial infrastructure.


Final Thoughts

Single Pair Ethernet connectors are moving from concept to practical deployment.

In 2026, key developments are expected around:

  • IEC 63171 standard adoption
  • PoDL expansion
  • connector miniaturization
  • robotics integration
  • Industry 4.0 implementation
  • EMC optimization

For OEMs and industrial buyers, now is the time to understand SPE technologies and prepare for the next generation of industrial networking.

Organizations that evaluate SPE early may gain advantages in system simplification, scalability, and future connectivity readiness.


FAQ

What is a Single Pair Ethernet connector?

An SPE connector is a connector designed to transmit Ethernet communication through a single twisted pair of conductors.

What is PoDL?

Power over Data Line (PoDL) enables both power and data transmission over the same SPE cable.

Will SPE replace Industrial Ethernet?

Not immediately. SPE is expected to complement existing Ethernet infrastructure, particularly at the device level.

Which SPE connector standards are most important?

IEC 63171-2, IEC 63171-5, and IEC 63171-6 are among the most widely discussed industrial SPE connector standards.

Why is SPE important for Industry 4.0?

SPE enables direct Ethernet connectivity to sensors and actuators, supporting unified and scalable industrial communication architectures.


Planning for Next-Generation Industrial Connectivity?

FPIC provides custom SPE cable assemblies, Industrial Ethernet harnesses, M8/M12 connectivity solutions, and engineering support for automation, robotics, and Industrial IoT applications.

Contact us to discuss your future Single Pair Ethernet connectivity requirements.


Resources

  1. IEC 63171 Series – Single Pair Ethernet Connector Standards
  2. IEEE 802.3cg – 10BASE-T1L and 10BASE-T1S Standards
  3. PROFIBUS & PROFINET International (PI) SPE Resources
  4. ODVA Single Pair Ethernet Guidance
  5. Phoenix Contact and HARTING SPE Technology Documentation

Source References: IEC 63171, IEEE 802.3cg, PI, ODVA, Phoenix Contact, HARTING SPE technical resources.