Tag Archive for: connector reliability

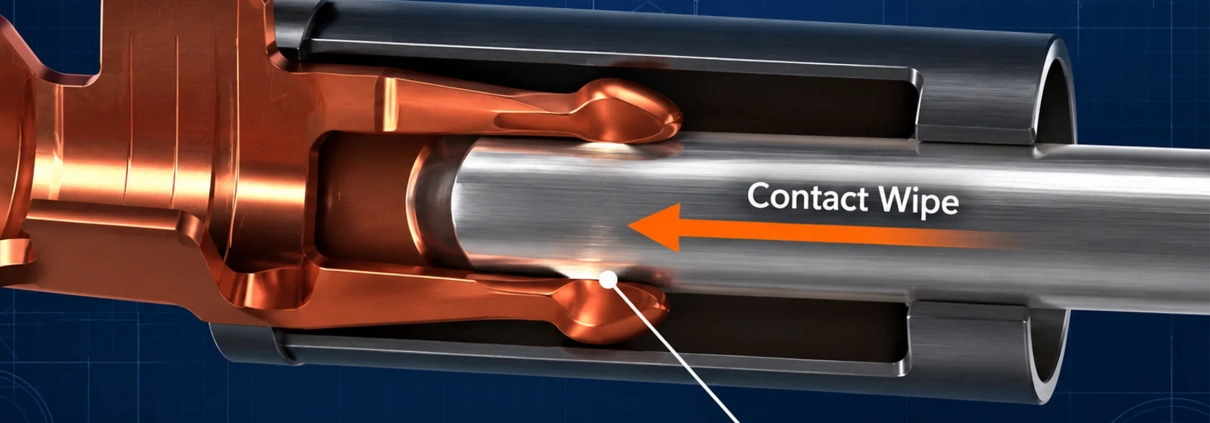
Connector contact wipe along a mating terminal surface

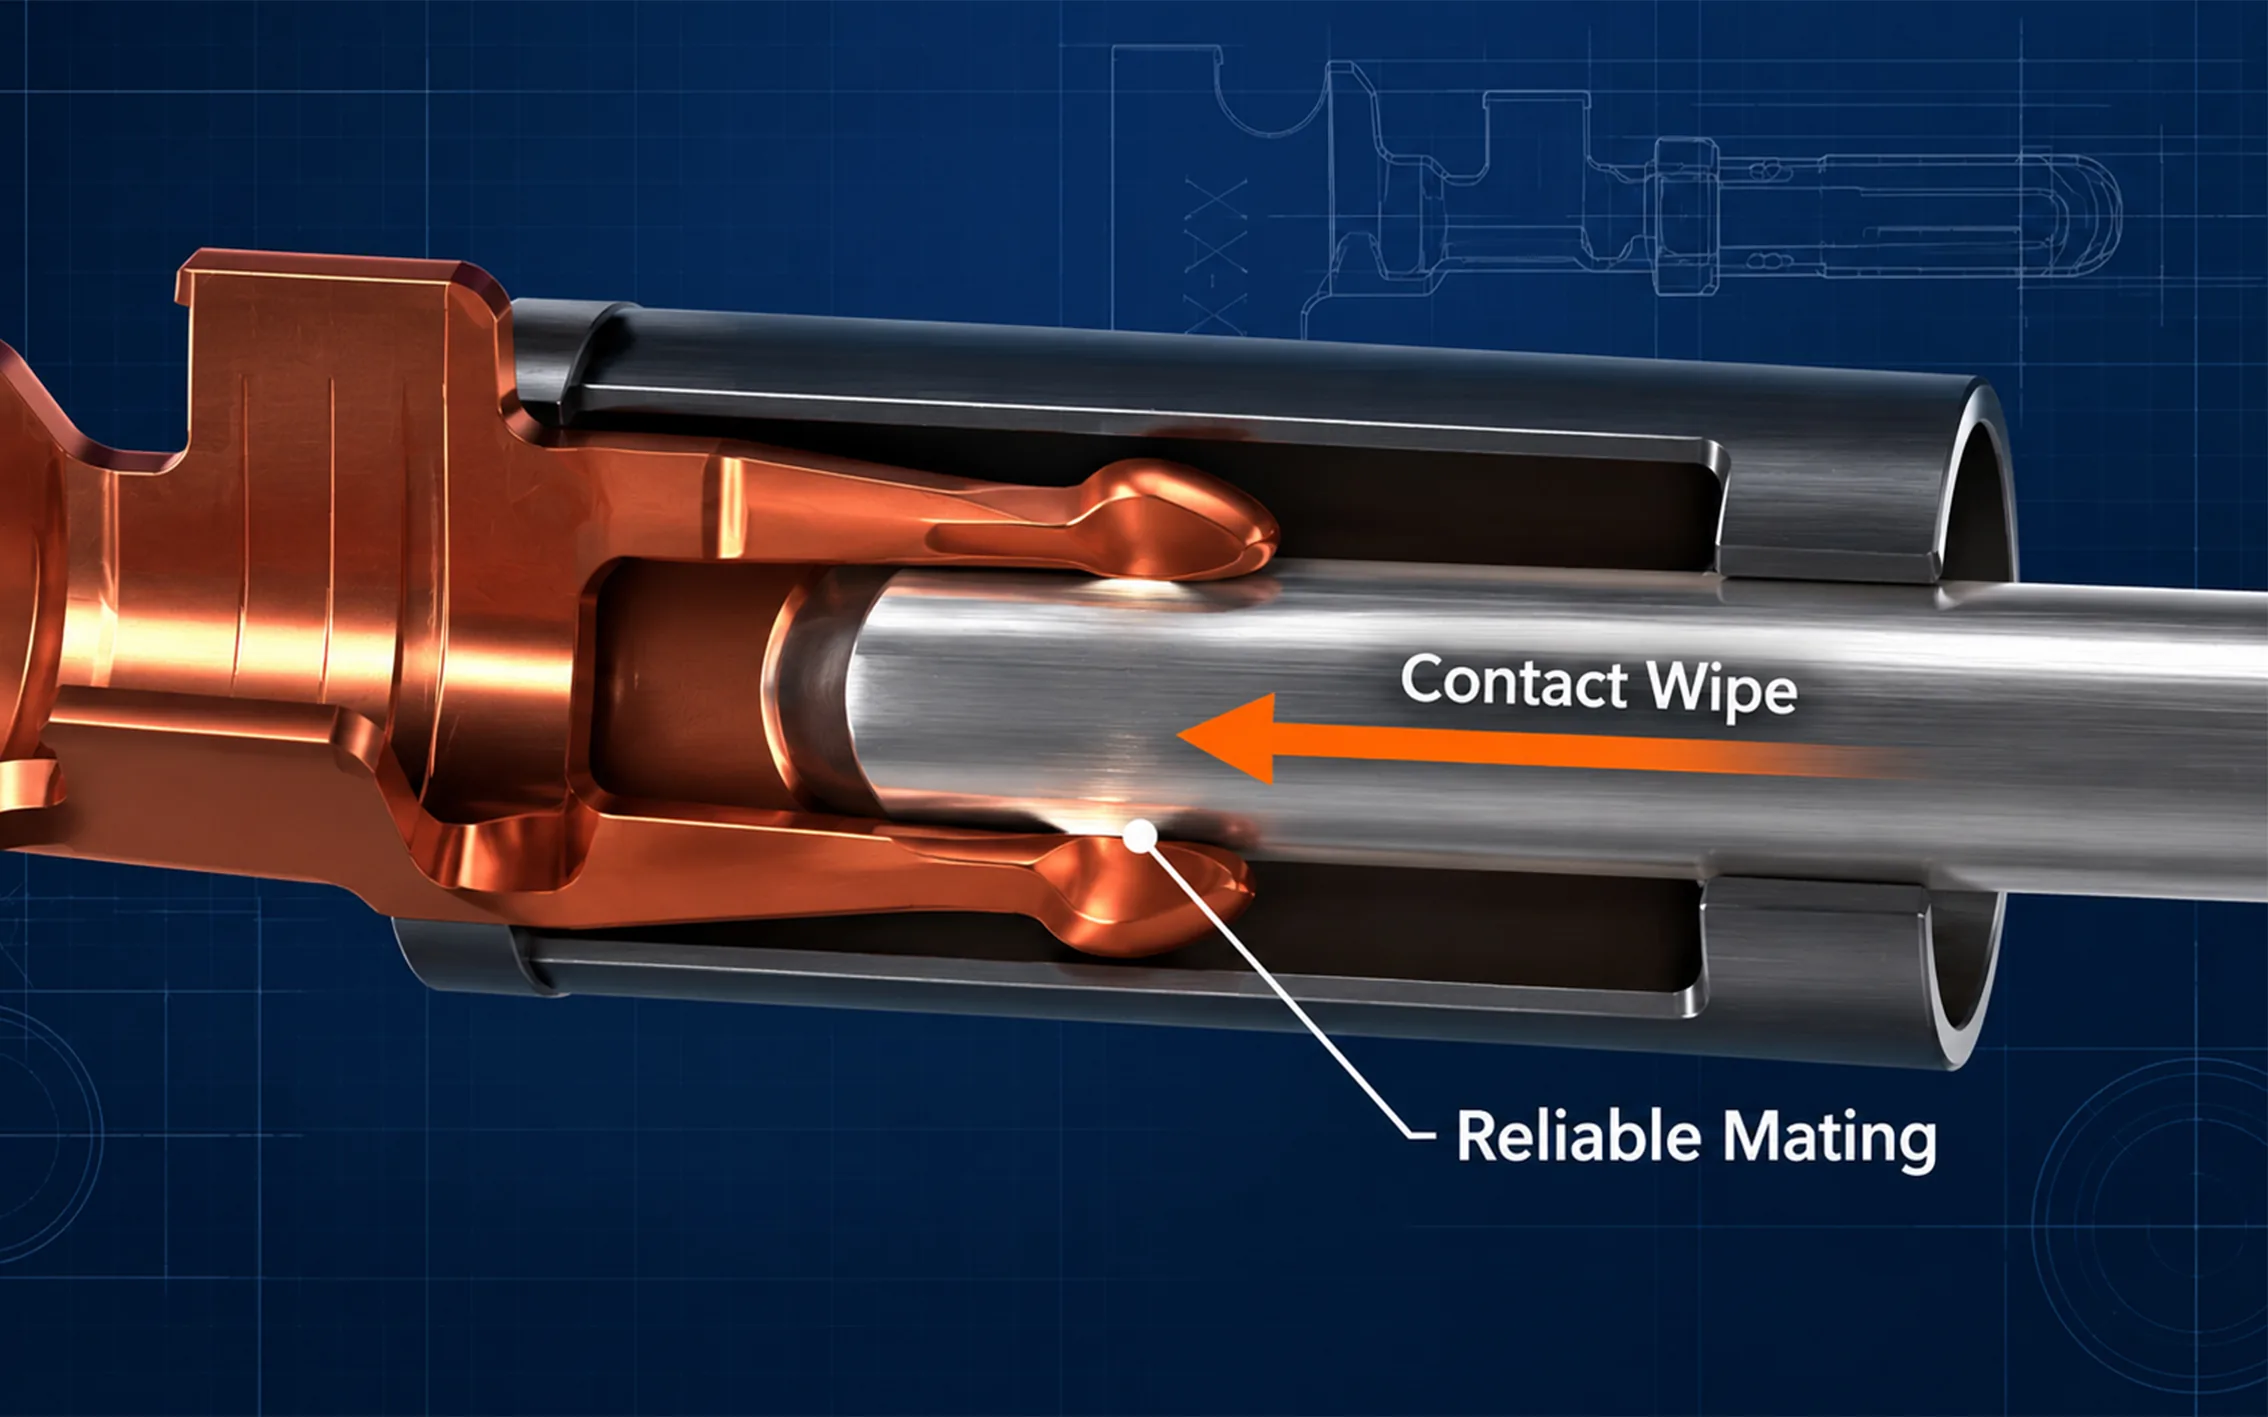
Connector contact wipe is the relative sliding of mating surfaces while they are pressed together during engagement. This motion can disrupt surface films and help establish conductive contact spots. Its effectiveness depends on the finish, contact geometry, and applied load—not distance alone.

For an engineer reviewing a terminal drawing, the useful questions are practical: Where do the surfaces first touch? How far do they slide under load? Where does the contact finally rest? And will that sequence still work at the limits of the assembly tolerances?

What Is Contact Wipe?

In a typical pin-and-socket interface, the pin begins to touch a spring contact before the connector reaches its final mated position. Continued insertion creates sliding between the contacting surfaces. That sliding is the wiping action.

The relevant distance is the travel at the contact interface. It is not automatically the entire housing insertion stroke. A connector may move some distance before its conductive surfaces touch.

Samtec’s technical explanation of contact wipe connects this action with surface-film disruption and highlights the importance of insertion depth, board spacing, and assembly tolerances.

TermWhat It DescribesDesign Question
Wipe distanceRelative sliding travel at the loaded contact interfaceIs the intended contact track traversed?
Normal forceLoad perpendicular to the local mating surfaceIs adequate load maintained during engagement and service?
Mating strokeMovement of the connector halves during assemblyWhen does electrical contact begin within that movement?
Mated overlapEngagement remaining at the final positionDoes the interface remain properly engaged across the allowed assembly range?

These dimensions and forces are related, but a drawing should define them separately. A supplier’s definition of insertion depth or engagement length should also be checked before it is used as a wipe specification.
Connector contact wipe along a mating terminal surface


How Sliding Helps Disrupt Surface Films

An electrical contact operates through microscopic conducting regions. Oxide and contamination films can obstruct those regions even when two metal parts appear to be touching. Contact-mechanics research explains how surface roughness and films influence resistance at the interface. Persson, 2022

During engagement, local pressure and sliding can work together to fracture or displace films. The outcome depends on what covers the surface and on the contact system itself. Wiping should therefore be understood as a designed interface action, not a guarantee that a connector cleans away every contaminant.

Tin and gold illustrate why the surface finish matters. Tin forms an oxide film in air; properly designed tin interfaces use contact load and sliding to establish electrical contact through that film. Gold is resistant to oxidation and generally supports different force and travel requirements. Samtec discusses these distinctions in its plating selection guidance.

For a custom project, define the expected surface condition before selecting the travel. Storage, handling, assembly residues, and service exposure should be part of that discussion. Heavy contamination or damaged plating calls for investigation rather than repeated mating as a production remedy.

Contact Wipe and Contact Resistance

A useful wiping action can help establish a lower-resistance interface when films are obstructing conduction. However, there is no universal equation that converts a particular travel distance into a guaranteed resistance value.

The measured result also depends on contact load, surface condition, material, and the arrangement of the conducting spots. Moreover, a measurement taken across a connector assembly may include conductor and termination resistance in addition to the separable interface. Wiping does not correct a defective crimp or solder joint.

For design comparison, specify consistent measurement locations and sample preparation. Otherwise, differences attributed to the contact track may actually come from the fixture or another part of the current path.

IEC 60512-2-1 provides a millivolt-level contact-resistance measurement method. The product specification must still define the applicable limits and conditioning. A basic continuity result answers whether a path exists; it does not establish the resistance margin or predict durability.


How Terminal Geometry Determines the Sliding Path

Review the interface in successive positions, rather than only as a fully mated CAD section. The lead-in, spring profile, mating-pin dimensions, and final stop determine how engagement develops. Materion’s insertion-force analysis shows why contact location, angle, and load change as a pin enters a spring contact.

For a new terminal design, the following review sequence helps turn the concept into drawing requirements:

  1. Identify first touch. Locate the initial contact point for the specified mating counterpart.
  2. Follow the loaded path. Check how the contact point and spring deflection change during insertion.
  3. Locate final seating. Confirm where the interface rests when the assembly reaches its approved mated position.
  4. Compare the path with the finish specification. Check the specified contact zone and transitions between finishes.
  5. Repeat at dimensional limits. Review the allowed variation in both connector halves and their mounting arrangement.

For automotive connector systems, include terminal seating and housing engagement in this review. For board-to-board connectors, use the installed board arrangement, including the permitted board spacing and alignment.

A Practical Tolerance Example

Consider a hypothetical pair of PCB connectors. The nominal CAD assembly shows a contact track with comfortable engagement. In the installed product, the board spacing reaches its upper permitted limit while a mating terminal reaches the short end of its tolerance. The contact may engage later than it does in the nominal model.

The design-review question is whether sufficient loaded travel and final engagement remain in that combination. At the opposite dimensional extreme, check spring deflection and mechanical clearance as well.

This is an illustrative review scenario, not FPIC test data. It shows why a nominal travel dimension alone cannot establish the suitability of a finished assembly.


Plating Wear and Excessive Wipe

The same sliding that helps condition an interface also exposes the finish to friction and wear. Extending the track should therefore be evaluated against the required number of mating operations and the condition of the contact surfaces afterward.

A useful specification identifies the mating finish, underplate, thickness requirements, and designated contact area. “Gold plated” or “tin plated” alone leaves too much undefined for a durability comparison. Samtec’s plating guidance treats finish selection as a balance among electrical behavior, operating life, and application requirements.

For a development review, ask:

  • Does the mating pair use the approved finish combination?
  • Is the final contact position within the specified contact zone at every allowed assembly condition?
  • Does the durability test represent production finishes and any specified lubricant?
  • Are wear tracks, resistance changes, and mating force assessed together?
  • If the travel is increased, what evidence shows the revised interface still meets its life requirement?

A visible track is evidence of sliding, not automatically evidence of failure. It also does not prove acceptable remaining plating. Interpret the track against the drawing, inspection criteria, and electrical results.

Vibration and Micro-Movement Are a Different Problem

The intended sliding during assembly and repeated movement during service require separate consideration. Small oscillatory motion at a loaded interface can produce fretting damage; oxidation of susceptible surfaces and wear debris can contribute to deteriorating electrical contact.

The engineering literature identifies contact load, motion, temperature, and interface design as relevant variables. Braunovic’s review of fretting in electrical connections also discusses the value of connection design and lubrication in reducing its effects.

A connector that establishes a satisfactory interface during insertion must still preserve it in service. For design review, consider housing support, board mounting, terminal restraint, and cable loading alongside the contact system. If lubrication is proposed, qualify it for the actual materials and environment.

Do not treat additional insertion travel as evidence that vibration testing is unnecessary. The two address different stages of the connector’s life.


Why Wipe and Normal Force Must Be Designed Together

Travel describes the movement; normal force describes the perpendicular load during that movement. Effective engagement requires a suitable combination of both, with the surface finish included in the decision.

As Materion explains, contact angle and force can vary during insertion. The final seated load therefore does not describe every point along the path. Spring material must also retain suitable force through the required operating life. Materion technical analysis

Review the pair as a system:

Design Condition to InvestigateQuestion for Validation
Travel available, but low load along part of the pathDoes the interface establish acceptable resistance under the specified surface condition?
Adequate seated load, but limited sliding before seatingDoes the design still meet its initial and conditioned electrical requirements?
High load combined with substantial slidingAre mating effort and surface wear acceptable over the required cycles?
Acceptable nominal geometry, but reduced engagement at tolerance limitsDoes the installed assembly retain the required performance margin?

The companion topic, contact normal force, examines spring loading and retained force. This article adds the path taken to reach the final electrical contact position. Both belong in the same interface review.

How to Validate the Design

Use the applicable product and customer specifications to establish the test sequence. The following is a planning framework, not a universal qualification procedure.

Review or TestEvidence to CollectQuestion It Helps Answer
Mated geometry and tolerance reviewFirst-touch position, loaded travel, seated position, assembly limitsDoes the intended path exist in the actual assembly?
Material and finish verificationApproved alloy, finish system, thickness and contact-zone recordsDo samples represent the proposed production design?
Baseline electrical measurementResistance measured at defined pointsIs initial electrical performance within specification?
Mechanical operationSpecified mating cycles, force observations, post-cycle inspectionHow does repeated engagement affect the interface?
Environmental conditioningExposure and measurements specified for the applicationDoes performance remain acceptable after the relevant aging conditions?
Dynamic testingApplicable vibration or shock conditions and electrical monitoringDoes the mated assembly remain stable during movement?
Final examinationElectrical results, wear observations, dimensional or mechanical findingsWhich mechanism explains any change?

IEC 60512-9-1 addresses mechanical operation. IEC 60512-6-4 addresses sinusoidal vibration. These method references do not establish one minimum wipe distance or one acceptance limit for all connectors.

Record whether samples were unmated before a post-test measurement. Another mating operation changes the surface history and can complicate interpretation of the conditioned interface. Follow the specified sequence and keep sample handling traceable.

For procurement, request the approved mating drawing and qualification scope together with the electrical specification. A resistance value without the associated counterpart, assembly condition, and conditioning history provides limited evidence for a new application.

From Terminal Design to Production Control

For custom automotive and PCB projects, FPIC’s R&D capabilities connect terminal structure and material review with tooling, prototype validation, and project-specific testing. Relevant manufacturing work includes precision stamping, molding, and assembly, with dimensional and finish verification supporting the approved design.

The practical starting point is a mating-pair drawing, the installed assembly limits, finish requirements, operating environment, and expected mating cycles. These inputs help define what needs to be reviewed and demonstrated before production approval.


Conclusion

Reliable mating depends on a controlled contact path, a suitable finish, and sufficient load throughout engagement and service. Specify the sliding action as part of the complete interface, then validate its electrical and mechanical behavior across tolerances and the required life.

For a custom terminal or connector design review, send the mating drawings and application requirements to info@fpiconn.com.


Frequently Asked Questions

Is wipe distance the same as connector insertion depth?

Not necessarily. The housings can travel before the conductive surfaces first touch. Use the product drawing’s defined reference points to distinguish insertion depth, loaded sliding travel, and final overlap.

Is a longer wiping path always better?

No. Evaluate the travel together with load, finish, assembly tolerances, and required mating life. A change should be supported by electrical and durability results rather than length alone.

Do gold-plated contacts still need a defined mating path?

Yes. Gold’s resistance to oxidation does not remove the need to control engagement, surface condition, and wear. The required movement is specific to the contact design.

What is the minimum acceptable distance?

There is no single value applicable to every connector. Use the mating-pair specification and validation results for the particular geometry, finish, loading, and application.

Does wiping during insertion prevent fretting in service?

It does not establish fretting immunity. Initial engagement and repeated micro-movement in service are different conditions and should be evaluated separately.

What should an OEM provide for a custom terminal review?

Provide both mating-part drawings, mounting and engagement limits, material and finish specifications, current and temperature requirements, environmental exposure, expected mating cycles, and the applicable qualification requirements.


Resources

  1. Samtec, Is Contact Wipe Important?, published July 23, 2025; page also displays June 4, 2026.
  2. B. N. J. Persson, On the Electric Contact Resistance, Tribology Letters, July 20, 2022.
  3. Samtec, What Plating Option Is Best For My Connector?, published October 19, 2017; page also displays January 17, 2025.
  4. Materion, How Can Connector Insertion Force Be Reduced?, January 1, 2024.
  5. Milenko Braunovic, Fretting in Electrical/Electronic Connections: A Review, IEICE Transactions on Electronics, August 1, 2009. Public abstract and bibliographic record.
  6. IEC, IEC 60512-2-1:2002 — Contact Resistance, Millivolt Level Method.
  7. IEC, IEC 60512-9-1:2010 — Mechanical Operation.
  8. IEC, IEC 60512-6-4:2002 — Vibration, Sinusoidal.
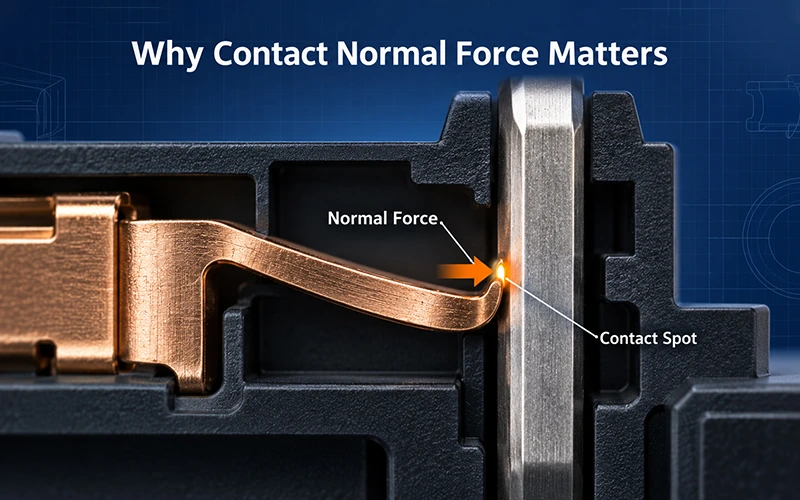
Spring contact applying normal force to a mating connector terminal

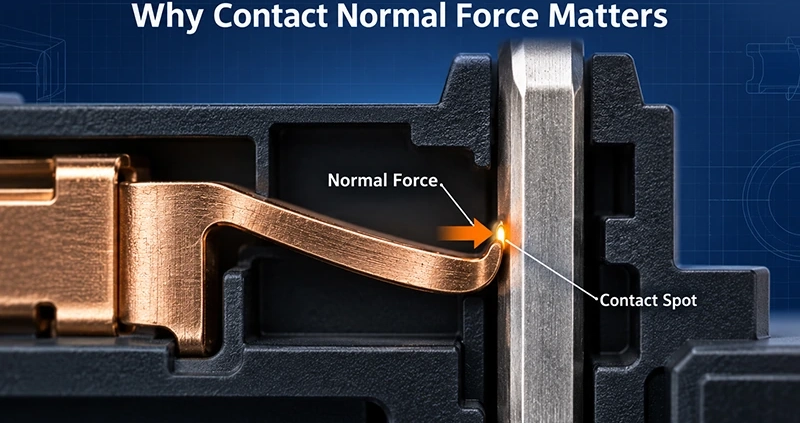
Contact normal force is the perpendicular load a spring contact applies to its mating surface. If that force is too low – or falls after heat, wear, or vibration – a connector can pass an initial continuity test yet develop unstable resistance later.

Short answer: A reliable separable contact needs enough normal force to create and preserve microscopic conductive contact spots. Too little force makes the interface more sensitive to surface films and movement. Excessive force increases mating effort, plating wear, and the risk of permanent deformation. The correct target is a controlled force window over the connector’s intended life.

That is why normal force should be treated as a lifetime design parameter, not just a value checked on a new sample.


What Is Contact Normal Force?

When a pin or blade enters a receptacle, the receptacle’s spring feature deflects. The elastic reaction presses the two conductive surfaces together. The component of that load acting perpendicular to the mating surface is the contact normal force.

The term is often confused with three other connector measurements:

MeasurementWhat It DescribesWhy It Matters
Contact normal forcePerpendicular load applied by the spring contact to the mating surfaceControls the stability of the separable electrical interface
Mating and unmating forceAxial force required to engage or separate the connector halvesAffects assembly, serviceability, ergonomics, and wear
Terminal retention forceForce required to pull a terminal from its housing cavityVerifies the terminal lock, lance, or secondary retention system
Crimp pull-out forceMechanical strength of the wire-to-terminal crimpVerifies the permanent termination, not the mating interface

A connector can meet terminal-retention and crimp requirements while still having inadequate spring force at the electrical contact point. It can also have acceptable normal force but excessive total mating force because seals, locks, alignment, friction, and multiple circuits add resistance during engagement.

Spring contact applying normal force to a mating connector terminal

How Contact Force Affects Contact Resistance

Metal surfaces may look smooth, but at microscopic scale they touch at small high points called asperities. Current therefore crosses the interface through a limited number of real contact spots rather than the full visible area.

Applying normal load deforms some asperities, increases effective contact area, and can help penetrate or displace oxide and contamination films. This reduces the constriction and film-related components of interface resistance. Research on electrical contact mechanics links constriction resistance to the mechanical stiffness and load of the interface, while also showing that surface films can strongly change the result.

It helps to separate three parts of a connector’s conductive path:

  1. Bulk resistance through the metal contact.
  2. Termination resistance at the crimp, solder joint, or press-fit section.
  3. Interface resistance where the separable contacts meet.

Normal force mainly influences the third part. Changing spring pressure does not repair a poor crimp, undersized conductor, damaged solder joint, or unsuitable base material.

More Force Is Not Always Better

At the low end, insufficient pressure can produce fewer stable contact spots and greater sensitivity to films, contamination, vibration, and tolerance variation. Raising the load generally reduces and stabilizes interface resistance, but the benefit does not continue without limit.

Excessive force can create other problems:

  • High insertion and withdrawal loads, especially in multi-position connectors
  • Faster wear of tin, gold, or other contact finishes
  • Damage to the mating surface during repeated operation
  • Permanent set if the spring exceeds its elastic design range
  • Housing distortion, difficult assembly, or incomplete mating

The engineering objective is therefore not maximum force. It is sufficient retained force with acceptable mating effort, wear, temperature rise, and dimensional margin. The target must be defined for the specific contact geometry, material, plating system, mating counterpart, environment, and required service life.

Spring Geometry and Material Set the Force Window

Within its elastic range, a contact spring behaves approximately as force equals stiffness multiplied by deflection. That simple relationship explains why the male contact, female spring, housing, and manufacturing tolerances must be designed as one system.

Spring stiffness and working stress are influenced by:

  • Beam length, width, thickness, and formed geometry
  • Contact angle and the location of the contact point
  • Bend radii and transitions that concentrate or distribute stress
  • Deflection created by the minimum and maximum mating-contact dimensions
  • Elastic modulus, yield strength, fatigue performance, and material temper
  • Residual stress introduced during stamping and forming

Thickness is especially sensitive in many spring designs because a small dimensional change can cause a much larger change in stiffness. The exact relationship depends on the contact form, so designers should use calculation or simulation together with physical force-displacement measurements.

Material Selection Is a Trade-Off

Brass, phosphor bronze, and higher-performance copper alloys can all be appropriate contact materials in the right design. Selection should consider conductivity, yield strength, formability, fatigue resistance, corrosion behavior, cost, and stress-relaxation performance at the expected temperature.

A highly conductive alloy may help control bulk heating but may not retain spring stress as well as another alloy. A stronger material may allow useful deflection in a compact geometry, but strength alone does not prove long-term force retention. Material temper, grain direction, forming history, and operating temperature also matter.

Production Variation Changes Real Contact Force

The CAD model represents a nominal condition. Production parts contain normal variation from strip thickness, stamping dimensions, forming angles, tool wear, material properties, plating thickness, housing dimensions, and mating-pin size.

These variations form a tolerance stack. At one extreme, the contact may be too loose. At the other, it may be overstressed or difficult to mate. Critical spring dimensions therefore require production controls linked to the force and electrical requirements they influence.

Plating and lubrication also affect friction. They can change total mating force even when spring pressure stays similar, which is another reason not to infer normal force from connector insertion force alone.

Stress Relaxation at High Temperature

Stress relaxation is the gradual loss of stress in a spring held at a substantially constant deflection. In a connector, the contact may remain mated while its spring load slowly decreases. Higher temperature generally accelerates this process, and different copper alloys can retain force at very different rates.

The contact experiences both ambient heat and self-heating. For a current-carrying interface, local power dissipation follows:

P = I²R

If interface resistance rises, local heating can rise. Higher temperature can then accelerate force loss, oxidation, or other degradation mechanisms. This does not mean every connector enters thermal runaway, but it shows why electrical, thermal, and mechanical design cannot be separated.

Designers often allow for expected force loss by starting above the minimum end-of-life requirement. However, simply increasing initial force can raise mating effort and plating wear. A better approach balances spring geometry, alloy, temperature exposure, finish, and required life so that sufficient force remains after aging without creating excessive force when new.

Repeated Mating Changes the Interface

Mating creates a wiping action between the contact surfaces. Controlled wiping can help disrupt surface films and establish a conductive contact region. The same sliding action also creates friction and gradually wears the finish.

Normal force affects both effects. Too little pressure may not create a stable interface. Too much pressure can increase friction and remove plating faster. Once the finish is locally worn through, exposed underplate or base metal may behave differently in humidity, pollutants, or corrosive environments.

Cycle count alone is therefore incomplete. A durability plan should define the mating counterpart, engagement speed, alignment, lubrication condition, environmental exposure, and measurements taken before and after cycling. Contact resistance and force after the required number of operations are more informative than a visual statement that the connector still mates.

Vibration and Micro-Movement

A connector lock prevents the housings from separating, but it does not automatically stop microscopic motion at the contact spot. Vehicle vibration, equipment movement, cable loading, and differential thermal expansion can produce small relative displacements inside a fully mated connector.

This movement can damage surface films and generate wear debris. With susceptible finishes and environments, the debris can oxidize and increase resistance – a process commonly associated with fretting corrosion. The result may be a gradual resistance increase or intermittent discontinuity that does not appear during a static bench check.

Retained normal force and suitable spring stiffness help stabilize the interface, but they are only part of the solution. Contact geometry, finish, lubrication where permitted, housing support, locking, cable strain relief, and vibration spectrum must be considered together.

Why Initial Continuity Does Not Prove Long-Term Reliability

A continuity check confirms that an electrical path exists at the moment of measurement. New, clean contacts can pass even when the design has limited margin against force loss or environmental aging.

An initial test does not by itself reveal:

  • How much normal force remains at the lowest material and dimensional condition
  • Whether high-temperature exposure will relax the spring
  • Whether the finish will survive the specified mating cycles
  • Whether vibration will cause micro-motion or intermittent events
  • Whether corrosion products will increase resistance
  • Whether current-induced heating will remain acceptable

Low-level contact resistance testing provides a more sensitive view of the mated interface than a basic continuity check. It should still be combined with mechanical and environmental conditioning. IEC 60512-2-1 defines a millivolt-level method for measuring resistance across mated contacts, while other parts of the IEC 60512 series address temperature rise, vibration, mechanical operation, and corrosion exposure.

The applicable customer specification may instead reference USCAR, LV214, EIA-364, or another sector-specific standard. The correct sequence, severity, sample preparation, monitoring method, and acceptance limits must come from the product’s detail specification and application requirements.

A Practical Contact Validation Plan

Long-term performance is best evaluated as a sequence rather than a group of unrelated pass/fail checks.

Validation StageWhat to Control or MeasureEngineering Question
Design inputCurrent, temperature, vibration, mating cycles, environment, mating counterpartWhat conditions must the interface survive?
Material and dimensionsAlloy, temper, strip thickness, spring geometry, plating, housing and mating-contact tolerancesDoes the full tolerance stack stay within the intended force window?
Baseline mechanicsForce-displacement behavior, mating/unmating force, gauge retention where applicableIs the new contact mechanically correct without overstress?
Baseline electricalLow-level contact resistance, voltage drop, temperature rise or current derating as requiredDoes the interface perform before conditioning?
DurabilitySpecified mating cycles followed by force, resistance, and surface reviewDoes wiping or wear change performance?
Thermal and climatic agingHigh-temperature exposure, thermal cycling, humidity, or corrosive atmosphere as applicableDoes the spring retain force and does the finish protect the interface?
Dynamic testingVibration and shock, with discontinuity monitoring when requiredDoes the mated system remain stable under movement?
Final assessmentRepeat mechanical and electrical measurements; inspect contact surfacesIs the design still within its acceptance limits after the full sequence?

IEC 60512-9-1 addresses mechanical operational endurance, IEC 60512-6-4 covers sinusoidal vibration, and IEC 60512-11-7 provides a flowing mixed-gas method for evaluating low-concentration pollutant effects on contacts. These standards define test methods, not universal acceptance values for every connector.

Questions to Resolve During Design Review

Before approving a contact system, engineering and procurement teams should ask:

  • What is the minimum required force after thermal aging and durability testing?
  • What force occurs at the maximum mating-contact dimension?
  • Could any tolerance condition exceed the material’s elastic limit?
  • What ambient temperature, current, and local temperature rise are expected?
  • Which plating system and thickness are specified at the contact zone?
  • How many mating operations must the interface withstand?
  • What vibration, shock, humidity, pollutant, or corrosive exposure applies?
  • How will force and resistance be measured before and after conditioning?
  • Which dimensions and material properties require production monitoring?

These questions turn a vague request for a “reliable terminal” into measurable design and validation requirements.

How FPIC Supports Contact-System Development

For applicable automotive, PCB, wire-to-board, and precision-terminal projects, FPIC can coordinate terminal design review, tooling, stamping, molding, assembly, and project-specific verification. Available laboratory support includes contact-resistance, insertion-and-withdrawal-force, temperature-rise, vibration, and coating-thickness checks according to the agreed validation plan.

The acceptance criteria remain product- and application-specific. Customers should provide the terminal and housing drawings, mating-contact dimensions, material and plating requirements, current, temperature range, mating cycles, environmental conditions, target volume, and applicable standards for technical evaluation.

Conclusion

A contact system needs normal force to remain inside the required window after tolerances, heat, mating wear, and vibration have done their work. Initial continuity is a starting measurement; long-term confidence comes from coordinated spring design, materials, manufacturing control, and sequence-based validation.

To discuss a custom connector, terminal, or PCB interconnect project, contact FPIC at info@fpiconn.com.


Frequently Asked Questions

What is contact normal force in a connector?

Contact normal force is the perpendicular load that a spring contact applies to its mating pin, blade, or pad. It helps establish and maintain the microscopic conductive spots at the separable interface.

Does higher contact force always reduce resistance?

No. Increasing a low force can improve interface stability, but excessive force can raise mating effort, wear the plating, distort the housing, or permanently deform the spring. Designers need a validated operating window rather than the highest possible value.

Is contact normal force the same as insertion force?

No. Normal force acts at the contact surface, while insertion force is measured in the mating direction and also includes friction, contact angle, seals, alignment, locks, and the combined effect of multiple circuits.

How does high temperature affect terminal spring force?

High temperature can accelerate stress relaxation, causing a deflected spring contact to lose load over time. The rate depends on alloy, temper, geometry, stress level, temperature, and exposure duration.

Can a connector pass continuity testing and still fail later?

Yes. A clean new interface may pass continuity even if it has limited margin against thermal relaxation, plating wear, fretting, corrosion, or dimensional variation. Mechanical and environmental conditioning followed by resistance measurement provides stronger evidence.

Which tests help evaluate long-term contact reliability?

The validation plan may include force-displacement measurement, low-level contact resistance, temperature rise or derating, mating durability, thermal aging, temperature cycling, humidity or corrosion exposure, vibration, shock, and post-test surface inspection. The applicable standard and limits depend on the product and application.


Resources

  1. B. N. J. Persson, “On the Electric Contact Resistance,” Tribology Letters, 2022.
  2. Materion, “What Is Stress Relaxation of Materials?” 2024.
  3. Materion, “How Can Connector Insertion Force Be Reduced?” 2024.
  4. Materion, “What Makes a Good Spring Material?” 2024.
  5. IEC 60512-2-1:2002, Contact Resistance – Millivolt Level Method.
  6. IEC 60512-5-1:2002, Temperature Rise.
  7. IEC 60512-6-4:2002, Vibration (Sinusoidal).
  8. IEC 60512-9-1:2010, Mechanical Operation.
  9. IEC 60512-11-7:2003, Flowing Mixed Gas Corrosion Test.
  10. SAE International, USCAR2-9, Performance Specification for Automotive Electrical Connector Systems, 2024.
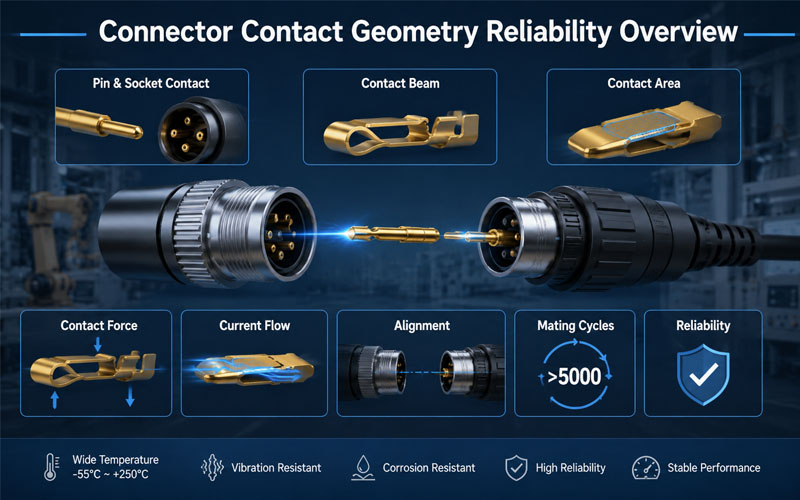
Connector Reliability Overview

A connector is only as reliable as its contact system.

Although the external housing provides protection and mechanical support, the actual electrical connection happens at the contact interface.

The design of this small area determines whether a connector can maintain stable performance under:

  • High current loads
  • Vibration
  • Temperature changes
  • Repeated mating cycles
  • Harsh operating environments

For applications such as automotive electronics, industrial automation, robotics, energy storage systems, and medical equipment, contact geometry plays a critical role in connector reliability.

A well-designed connector does not simply make contact.

It maintains consistent electrical and mechanical performance throughout its service life.

Connector Reliability Overview


What Is Connector Contact Geometry?

Contact geometry refers to the physical design of the connector contact interface.

It includes:

  • Contact shape
  • Contact beam structure
  • Contact area
  • Contact engagement position
  • Contact pressure distribution
  • Wiping action during mating

The goal of contact geometry design is to achieve the right balance between:

  • Electrical conductivity
  • Mechanical strength
  • Contact stability
  • Mating durability

Different applications require different contact structures.

A high-current power connector and a high-speed signal connector may use completely different contact geometries because their performance requirements are different.


Why Contact Geometry Is Critical for Connector Reliability

When two connector contacts mate, several physical factors determine connection quality.

A reliable contact interface must provide:

Stable Electrical Path

Ensuring current can flow efficiently with minimal resistance.

Proper Contact Force

Maintaining connection stability without excessive mechanical stress.

Controlled Wear

Allowing repeated mating without rapid degradation.

Resistance to Environmental Stress

Maintaining performance against:

  • Vibration
  • Shock
  • Temperature variation
  • Corrosion

Poor contact geometry can result in:

  • Increased contact resistance
  • Intermittent electrical connection
  • Signal interruption
  • Excessive heat generation
  • Premature connector failure

1.Contact Shape Determines Connection Performance

The shape of the contact element directly affects current transmission and mechanical stability.

Common contact structures include:


Pin and Socket Contacts

Pin and socket designs are widely used in circular connectors and industrial connectors.

Advantages:

✔ Reliable alignment

✔ Stable contact interface

✔ Good environmental adaptability

The socket contact usually uses spring structures to maintain contact pressure around the pin.

This design helps compensate for:

  • Manufacturing tolerance
  • Vibration
  • Mechanical movement

Blade Contacts

Blade contacts provide a larger conductive path.

Advantages:

✔ High current capability

✔ Simple structure

✔ Good mechanical strength

They are commonly used in:

  • Power connectors
  • Automotive applications
  • Industrial equipment

Spring Contacts

Spring-based contacts use elastic deformation to maintain continuous pressure.

Advantages:

✔ Improved vibration resistance

✔ Stable contact force

✔ Longer service life

They are suitable for applications requiring frequent mating cycles.


2.Contact Force Affects Reliability and Mating Performance

Contact force is one of the most important design parameters.

The correct contact force ensures:

  • Stable electrical connection
  • Low contact resistance
  • Resistance to vibration

However, both insufficient and excessive force can create problems.


Too Low Contact Force

Potential issues:

  • Increased electrical resistance
  • Intermittent connection
  • Signal instability

Low contact force may allow micro-movement between contacts, causing electrical degradation over time.


Too High Contact Force

Potential issues:

  • Higher insertion force
  • Increased contact wear
  • Reduced mating cycles

A good connector design balances:

Contact Reliability + User Operation + Service Life


3.Contact Area Influences Current Flow and Heat Generation

The contact interface determines how efficiently electrical current transfers between mating components.

A well-designed contact area helps:

  • Reduce current concentration
  • Lower resistance
  • Minimize heat generation

However, contact area alone does not determine performance.

Engineers must also consider:

  • Contact pressure
  • Surface condition
  • Material properties
  • Contact alignment

A larger contact surface without proper pressure control may not provide better reliability.


4.Wiping Action Helps Maintain Clean Contact Surfaces

Many connector designs include wiping action during mating.

During insertion, the contact surfaces slide against each other.

This movement helps remove:

  • Dust particles
  • Surface oxidation
  • Minor contamination

Benefits include:

✔ Improved electrical stability

✔ Reduced contact resistance variation

✔ Better long-term reliability

Wiping action is especially important for:

  • Outdoor equipment
  • Industrial automation
  • High-cycle connectors

5.Contact Geometry Determines Mating Cycle Life

Every mating cycle creates mechanical stress on contacts.

Repeated connection and disconnection can cause:

  • Surface wear
  • Loss of contact force
  • Material deformation

A reliable contact design considers:

Contact Elasticity

Maintains pressure after repeated use.

Wear Resistance

Reduces surface damage.

Mechanical Stability

Prevents deformation during operation.

For connectors requiring thousands of mating cycles, optimized contact geometry is essential.


6.Alignment Design Prevents Contact Damage

Even a well-designed contact can fail if alignment is poor.

Incorrect alignment may cause:

  • Bent pins
  • Uneven contact pressure
  • Partial engagement
  • Contact damage

Reliable connector systems often include:

  • Polarization features
  • Guide structures
  • Mechanical keys
  • Alignment sleeves

These features ensure correct mating and protect the contact system.


7.Contact Geometry Influences Thermal Reliability

Electrical resistance generates heat.

When contact geometry is poor, current may concentrate in small areas, creating:

  • Hot spots
  • Temperature rise
  • Contact degradation

A properly designed contact structure improves:

  • Current distribution
  • Heat dissipation
  • Long-term stability

This is especially important for:

  • High-current connectors
  • Battery systems
  • Industrial power equipment

8.Contact Geometry Must Match Application Requirements

Different industries require different contact solutions.

ApplicationContact Design Priorities
AutomotiveVibration resistance, durability, stable contact force
RoboticsHigh mating cycles, mechanical stability
Industrial AutomationEnvironmental protection, reliability
Energy StorageHigh current capability, thermal control
Medical EquipmentStable signal transmission, safety

Connector design should always begin with understanding the actual application environment.


9.Contact Material and Plating Work Together with Geometry

Contact geometry is only one part of connector reliability.

Material selection and surface treatment are equally important.


Contact Material

Common materials include:

  • Copper alloys
  • Brass
  • Phosphor bronze

Important characteristics:

  • Electrical conductivity
  • Spring performance
  • Mechanical strength

Contact Plating

Gold Plating

Advantages:

✔ Excellent corrosion resistance

✔ Low contact resistance

✔ Long mating life

Suitable for:

  • Signal connectors
  • Precision applications

Tin Plating

Advantages:

✔ Cost-effective

✔ Suitable for many power applications

Suitable for:

  • General electrical connections

10.How FPIC Optimizes Connector Contact Design

FPIC focuses on connector reliability through:

Precision Contact Engineering

Including:

  • Contact structure optimization
  • Contact force control
  • Mechanical tolerance management

Material and Plating Selection

Considering:

  • Current requirements
  • Environment
  • Mating cycles

Reliability Testing

Including:

  • Contact resistance testing
  • Insertion and extraction force testing
  • Mating cycle evaluation
  • Environmental testing

Through engineering optimization and manufacturing control, FPIC helps customers develop reliable connector solutions for demanding applications.


Common Contact Geometry Design Mistakes

Design MistakePotential Result
Incorrect contact forceIntermittent connection
Poor alignment designContact damage
Insufficient contact areaHeat generation
Weak wiping actionIncreased resistance
Improper material selectionReduced service life

Contact Geometry Design Checklist

Before finalizing a connector design, engineers should evaluate:

✔ Is the contact force within the correct range?

✔ Can the contact maintain stability after repeated mating?

✔ Is current distribution optimized?

✔ Does the geometry support the application environment?

✔ Are material and plating choices appropriate?

✔ Has the design been validated through testing?


Final Thoughts

Contact geometry is one of the most important factors influencing connector reliability.

A reliable connector requires careful optimization of:

  • Contact shape
  • Contact force
  • Contact area
  • Alignment
  • Material selection
  • Surface treatment

The contact interface may be small, but it determines the overall performance of the connector system.

A connector is not reliable because it connects once.

It is reliable because it maintains a stable connection thousands of times under real-world conditions.


FAQ

What is contact geometry in connectors?

Contact geometry refers to the physical structure and design of the electrical contact interface, including shape, contact area, and pressure distribution.

How does contact geometry affect connector reliability?

It affects electrical resistance, current flow, mating durability, vibration resistance, and long-term performance.

Why is contact force important in connector design?

Proper contact force ensures stable electrical connection while balancing insertion force and wear.

Can contact geometry affect connector temperature?

Yes. Poor contact geometry can increase resistance and create localized heat generation.

How do engineers improve connector contact reliability?

Engineers optimize contact structure, materials, plating, alignment, and validate performance through reliability testing.


Need a Reliable Custom Connector Solution?

FPIC provides custom connector design and manufacturing services with expertise in contact engineering, material selection, reliability testing, and mass production.

From concept development to final production, FPIC helps OEM customers build connectors designed for long-term performance.

Contact FPIC today to discuss your connector requirements.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Connector testing methods covering electrical and mechanical performance evaluation.
  2. EIA-364 Connector Test Standards
    https://www.eia-global.org/
    Industry test standards for connector reliability and performance validation.
  3. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry acceptance criteria for cable and wire harness assemblies.