Tag Archive for: Connector Design

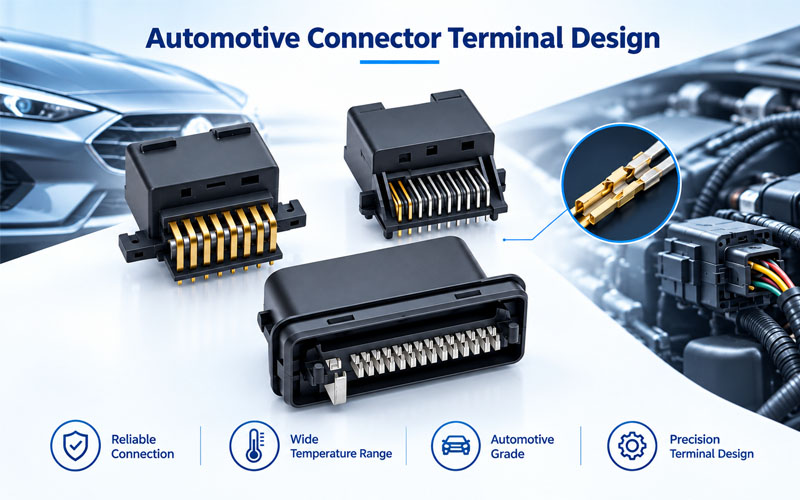
Automotive Connector Terminal Design for Electrical Reliability

In an automotive connector system, the plastic housing provides structure and protection, but the terminal creates the electrical connection.

This makes the terminal one of the most important components for electrical reliability.

A connector may have a robust housing, reliable locking mechanism, and effective sealing system, but poor terminal design can still result in:

  • High contact resistance
  • Localized heating
  • Intermittent electrical signals
  • Voltage drop
  • Fretting corrosion
  • Terminal deformation
  • Electrical discontinuity
  • Premature connector failure

The challenge becomes even greater in modern vehicles, where electrical systems must operate under higher current loads, tighter packaging constraints, vibration, temperature variation, and increasingly demanding reliability requirements.

For this reason, automotive terminal design should not be treated simply as a metal component selection problem.

It is a system involving:

Terminal Geometry + Contact Force + Material + Plating + Crimping + Retention + Thermal Behavior + Manufacturing Control
Automotive Connector Terminal Design for Electrical Reliability


1.Why Automotive Connector Terminals Matter

The terminal is the conductive path between the wire and the mating connector.

A simplified current path is:

Wire → Crimp Area → Terminal Body → Contact Interface → Mating Terminal → Electrical Circuit

Every interface in this path contributes to overall electrical performance.

A weak point anywhere in the current path can increase resistance or create instability.

For example:

  • Poor crimping can increase wire-to-terminal resistance.
  • Insufficient contact force can increase contact resistance.
  • Damaged plating can expose the base material.
  • Terminal deformation can reduce contact area.
  • Poor retention can cause terminal movement.
  • Excessive current can increase terminal temperature.

Therefore, automotive electrical reliability begins with controlling the complete terminal system.


2.Contact Force Is Fundamental to Electrical Reliability

When two metal contacts mate, the surfaces are not perfectly flat at the microscopic level.

Actual electrical conduction occurs through localized contact points.

Contact force helps maintain stable physical contact between the mating surfaces.

If contact force is too low, the terminal may become more sensitive to:

  • Vibration
  • Thermal expansion
  • Fretting
  • Surface contamination
  • Oxidation
  • Mechanical movement

As the contact interface becomes less stable, electrical resistance can increase.

But higher force is not always better

Excessive contact force can create other problems:

  • Higher mating force
  • Difficult assembly
  • Increased terminal wear
  • Deformation
  • Reduced serviceability

The design objective is therefore controlled and stable contact force, not simply maximum contact force.


3.Terminal Geometry Controls the Contact Interface

Terminal geometry directly influences how the mating contacts interact.

Depending on the terminal system, engineers may optimize:

  • Contact beam geometry
  • Contact point location
  • Contact length
  • Beam thickness
  • Spring characteristics
  • Contact angle
  • Terminal stiffness
  • Contact normal force
  • Mating alignment

A well-designed contact system should maintain sufficient contact force while accommodating manufacturing tolerances and service conditions.

Multi-point contact

Some terminal architectures use multiple contact points to improve electrical redundancy.

If one microscopic contact area experiences contamination or surface degradation, other contact areas can help maintain the electrical path.

This can be particularly useful in applications exposed to vibration or environmental stress.


4.Terminal Material Affects Current Carrying and Reliability

Terminal materials must provide an appropriate combination of:

  • Electrical conductivity
  • Mechanical strength
  • Spring properties
  • Formability
  • Corrosion resistance
  • Thermal stability
  • Manufacturing compatibility

Copper-based alloys are widely used in electrical terminals because they provide a useful balance between conductivity and mechanical properties.

However, the specific alloy should be selected according to the terminal design and application requirements.

A terminal carrying substantial current must also manage heat generation.

The relationship between electrical power and resistance is:

P = I²R

As current increases, even a relatively small resistance can generate significant heat.

This makes material selection particularly important for higher-current automotive applications.


5.Plating Protects the Contact Interface

Terminal plating is used to improve the stability and durability of the contact surface.

Common plating systems may include:

  • Tin
  • Nickel
  • Gold
  • Silver

The appropriate plating depends on the electrical, mechanical, environmental, and cost requirements of the application.

Tin plating

Tin is widely used for automotive terminals because of its practical balance of cost, conductivity, solderability, and corrosion protection.

However, tin contact systems require appropriate contact design because surface films can influence electrical performance.

Gold plating

Gold provides excellent corrosion resistance and stable electrical contact characteristics.

It may be selected for applications requiring high reliability or specific environmental performance, although cost and application requirements must be considered.

Silver plating

Silver offers excellent electrical conductivity and can be useful in certain higher-current applications, subject to the environmental and design requirements.

The important point is that plating should be designed together with the contact system, rather than selected independently.


6.Contact Resistance Depends on the Entire Terminal System

Automotive connector contact resistance is influenced by multiple factors.

These include:

  • Contact force
  • Contact geometry
  • Contact area
  • Surface condition
  • Plating
  • Crimp quality
  • Temperature
  • Vibration
  • Contamination
  • Corrosion
  • Mating cycles

This means that a terminal cannot be considered reliable simply because its initial resistance is low.

A stronger design objective is:

Maintain stable contact resistance throughout the expected service life.

This is particularly important when connectors are exposed to vibration, thermal cycling, moisture, or high current.


7.Crimp Quality Directly Affects Electrical Performance

The mating interface is only one part of the electrical path.

The connection between the wire and terminal is equally important.

A properly designed crimp creates a mechanically stable and electrically conductive connection between the conductor and terminal.

Poor crimping can cause:

  • Increased electrical resistance
  • Localized heating
  • Wire pull-out
  • Intermittent electrical connection
  • Conductor damage
  • Long-term fatigue

Important crimp characteristics can include:

  • Crimp height
  • Crimp width
  • Conductor insertion
  • Terminal position
  • Pull-out force
  • Crimp geometry
  • Cross-section condition

For automotive production, crimp quality should be controlled as a manufacturing process rather than inspected only at the end.


8.Terminal Retention Prevents Electrical Instability

The terminal must remain correctly positioned inside the connector housing.

A terminal that moves backward during mating or vehicle operation can reduce the effective contact interface.

This can cause:

  • Incomplete mating
  • Reduced contact force
  • Intermittent signals
  • Increased contact resistance
  • Circuit interruption

Terminal retention features therefore contribute indirectly but significantly to electrical reliability.

Common retention concepts include:

  • Primary terminal locks
  • Secondary terminal locks
  • TPA systems
  • Housing retention features

The terminal and housing must be designed as a complete system.


9.TPA and CPA Support Reliable Terminal Positioning

Two commonly used automotive connector features are TPA and CPA.

TPA — Terminal Position Assurance

TPA helps confirm that terminals are correctly seated and helps prevent terminal movement.

It can provide a secondary level of terminal retention after insertion.

CPA — Connector Position Assurance

CPA helps verify that the connector is fully mated and locked.

It can reduce the risk of incomplete mating caused by:

  • Partial insertion
  • Misalignment
  • Assembly error
  • Vibration-related disengagement

These features are particularly valuable in automotive manufacturing, where assembly accuracy and field reliability are closely connected.


10.Fretting and Vibration Can Degrade Terminal Performance

Automotive connectors can experience continuous vibration.

Small relative movements at the contact interface can produce fretting.

Over time, fretting can contribute to:

  • Surface wear
  • Oxide formation
  • Plating damage
  • Increased contact resistance
  • Intermittent electrical behavior

Terminal design can help reduce these risks through:

  • Stable contact force
  • Appropriate contact geometry
  • Suitable plating
  • Controlled mechanical movement
  • Robust connector retention
  • Proper cable strain relief

Vibration validation should therefore evaluate both mechanical integrity and electrical stability.


11.Thermal Performance Matters for High-Current Terminals

Higher current creates greater thermal challenges.

Using:

P = I²R

doubling current results in four times the resistive power at the same resistance.

For example, if a terminal interface has:

  • 1 mΩ resistance at 50 A → 2.5 W
  • 1 mΩ resistance at 100 A → 10 W
  • 2 mΩ resistance at 100 A → 20 W

This illustrates why resistance control becomes increasingly important as current increases.

Excessive temperature can accelerate:

  • Material degradation
  • Contact force loss
  • Oxidation
  • Plating deterioration
  • Housing deformation

Therefore, high-current terminal design requires consideration of both electrical and thermal performance.


12.Terminal Geometry Must Consider Current Distribution

Current does not always distribute uniformly across a terminal.

Localized current concentration can increase temperature in specific regions.

Engineers may need to evaluate:

  • Conductor cross-section
  • Terminal thickness
  • Contact geometry
  • Current path length
  • Contact area
  • Crimp transition
  • Thermal dissipation
  • Housing constraints

For high-current applications, the terminal should be evaluated as part of the complete electrical and thermal system.

Simply increasing terminal size is not always the optimal solution.


13.Terminal Tolerances Affect Electrical Reliability

Automotive terminals are manufactured at high volumes, which means dimensional variation must be controlled.

Critical dimensions can include:

  • Contact beam geometry
  • Terminal width
  • Terminal thickness
  • Crimp dimensions
  • Locking features
  • Mating interface
  • Position within the housing

Excessive dimensional variation can affect:

  • Contact force
  • Mating force
  • Terminal retention
  • Electrical resistance
  • Connector assembly

This is why tooling capability and process control are essential for stable terminal performance.


14.Terminal Manufacturing Quality Is as Important as Design

A good terminal design can still fail if manufacturing variation is not controlled.

Automotive terminal production may involve:

Stamping → Forming → Plating → Inspection → Crimping → Assembly → Electrical Testing

Each stage can affect final performance.

Stamping and forming

Poor forming can change the contact geometry or spring characteristics.

Plating

Plating thickness, coverage, adhesion, and surface condition can influence contact durability.

Crimping

Incorrect crimp dimensions can increase electrical resistance or reduce mechanical strength.

Assembly

Incorrect terminal insertion or incomplete locking can result in terminal back-out.

Therefore, terminal reliability depends on both engineering design and process capability.


15.How Automotive Connector Terminals Are Validated

Terminal validation should cover both initial performance and performance after stress exposure.

Typical evaluation areas include:

Electrical

  • Contact resistance
  • Voltage drop
  • Insulation resistance where applicable
  • Current carrying capability
  • Electrical continuity

Mechanical

  • Terminal retention
  • Mating and unmating force
  • Crimp pull force
  • Terminal insertion force
  • Mating-cycle durability

Environmental

  • Temperature cycling
  • High-temperature exposure
  • Humidity
  • Corrosion
  • Chemical exposure
  • Water or sealing-related testing where applicable

Dynamic reliability

  • Vibration
  • Mechanical shock
  • Intermittent electrical monitoring

The exact test program should be based on the applicable automotive standard, customer specification, connector architecture, and vehicle installation environment.


16.Initial Performance Is Not Enough

One of the most important principles in automotive terminal validation is to evaluate performance retention.

A terminal may initially demonstrate:

  • Low contact resistance
  • Good retention
  • Stable mating force
  • Good plating condition

But after environmental and mechanical exposure, performance may change.

For this reason, engineers should compare:

Initial Condition → Stress Exposure → Final Condition

Key parameters may include:

  • Contact resistance
  • Contact force
  • Mating force
  • Terminal retention
  • Visual condition
  • Plating condition
  • Crimp integrity

The change between initial and final measurements can provide valuable information about degradation mechanisms.


17.Common Automotive Terminal Failure Modes

Failure ModePossible CauseElectrical Impact
High contact resistanceLow contact force / surface degradationVoltage drop and heating
Terminal back-outWeak retention / incomplete insertionIntermittent or open circuit
FrettingVibration / micro-motionResistance instability
Crimp failureIncorrect crimp geometryIncreased resistance / wire separation
Plating wearExcessive mating / poor material selectionCorrosion and resistance increase
Terminal deformationExcessive mechanical loadPoor contact engagement
CorrosionMoisture / contaminationIncreased resistance
Thermal degradationExcessive current / resistanceFurther electrical degradation
Contact fatigueRepeated mechanical stressLoss of stable electrical connection

Failure analysis should identify the underlying mechanism rather than only the visible symptom.


18.Designing Terminals for Long-Term Electrical Reliability

A reliable automotive terminal design should consider several factors simultaneously.

1.Optimize contact force

Maintain sufficient force throughout the intended service life.

2.Select the right material

Balance conductivity, strength, formability, corrosion resistance, and thermal requirements.

3.Match the plating to the application

Consider current, environment, mating cycles, and required reliability.

4.Control crimp geometry

Ensure stable electrical and mechanical connection between wire and terminal.

5.Control terminal position

Use appropriate retention and secondary locking features.

6.Manage vibration

Minimize harmful relative movement at the contact interface.

7.Evaluate thermal behavior

Consider current, resistance, heat generation, and heat dissipation.

8.Validate after environmental stress

Measure performance before and after relevant reliability tests.

This integrated approach is more effective than optimizing any single parameter independently.


19.Automotive Terminal Reliability and Global Standards

Terminal validation may need to align with standards and customer requirements such as:

  • LV214
  • USCAR-2
  • ISO 16750
  • Customer-specific OEM specifications
  • Terminal and crimp specifications

These standards should not simply be treated as interchangeable checklists.

The actual validation plan should identify:

  • Applicable standard revision
  • Connector configuration
  • Terminal type
  • Test method
  • Test severity
  • Sample quantity
  • Acceptance criteria
  • Customer-specific requirements

For example, LV214 and USCAR-2 have overlapping automotive connector reliability objectives but belong to different qualification frameworks. The applicable requirements should therefore be mapped before formal testing begins.


How FPIC Supports Automotive Connector Terminal Reliability

Automotive connector reliability depends heavily on terminal engineering and manufacturing consistency.

FPIC supports automotive connector projects with capabilities covering connector development, terminal processing, automated inspection, electrical testing, assembly, and mass production.

For automotive applications, engineering teams can evaluate terminal geometry, contact performance, crimp quality, retention, electrical characteristics, and production requirements as part of the complete connector system.

Automotive connector production can also incorporate inspection and testing processes designed to control critical characteristics from terminal manufacturing through final assembly.

The objective is to connect:

Terminal Design → Material & Plating → Crimping → Assembly → Electrical Testing → Reliability Validation → Mass Production

This helps ensure that terminal performance is not only strong during initial testing but also consistent across production.


Final Thoughts

Automotive connector terminals are at the heart of electrical reliability.

Their performance depends on far more than conductivity alone. Contact force, terminal geometry, material, plating, crimp quality, retention, vibration resistance, thermal behavior, and manufacturing control all influence the stability of the electrical connection.

A reliable terminal should maintain a stable electrical interface throughout its expected service life—not simply achieve a low initial contact resistance.

By combining robust terminal design with controlled manufacturing, electrical testing, mechanical validation, and environmental reliability testing, automotive connector manufacturers can reduce electrical failure risks and build more dependable connector systems.


FAQ

What is the most important factor in automotive connector terminal reliability?

There is no single factor. Contact force, terminal geometry, plating, material, crimp quality, retention, vibration resistance, and thermal behavior all contribute to reliability.

How does terminal contact force affect electrical performance?

Adequate contact force helps maintain stable physical contact between mating surfaces. Insufficient force can increase sensitivity to vibration, fretting, contamination, and surface degradation.

Why is terminal plating important?

Plating protects the contact interface and influences corrosion resistance, wear behavior, and electrical stability. The appropriate plating depends on the application, current, environment, mating cycles, and reliability requirements.

How does crimp quality affect connector reliability?

The crimp forms the electrical and mechanical connection between the wire and terminal. Poor crimp geometry can increase resistance, generate heat, reduce mechanical strength, and cause intermittent electrical failures.

What is the role of TPA in automotive connectors?

TPA, or Terminal Position Assurance, helps confirm that terminals are properly seated and provides additional protection against terminal movement within the connector housing.

Why is terminal retention important?

If a terminal moves backward during mating or vehicle operation, the contact interface may become unstable. This can cause increased resistance, intermittent signals, or circuit interruption.

How are automotive connector terminals validated?

Validation can include contact resistance, crimp pull force, terminal retention, mating cycles, vibration, temperature cycling, humidity, corrosion, chemical exposure, and other application-specific tests.

Are automotive terminal tests the same for every connector?

No. The test plan depends on the connector architecture, terminal type, electrical load, vehicle installation position, environmental conditions, customer requirements, and applicable standards such as LV214 or USCAR-2.


Developing a custom automotive connector or terminal?

FPIC supports automotive connector projects from terminal and connector design through prototyping, electrical testing, reliability validation, and mass production.

Contact our engineering team to discuss your terminal requirements, current rating, crimp configuration, plating, validation plan, and production needs.


Resources

  1. SAE International – USCAR2-9: Performance Specification for Automotive Electrical Connector Systems
    Official SAE specification covering performance testing requirements for automotive electrical connector systems.
    SAE USCAR2-9
  2. ISO – ISO 16750 Road Vehicles: Environmental Conditions and Testing
    International standard series covering environmental conditions and testing for electrical and electronic equipment in road vehicles.
    ISO 16750
  3. USCAR – Automotive Connector Testing Resources
    Industry resources related to automotive electrical connector performance and validation.
    USCAR
  4. TE Connectivity – Automotive Terminals and Connector Systems
    Technical and product information covering automotive terminals, connectors, contact systems, and related technologies.
    TE Connectivity Automotive Solutions
LV214 vs USCAR-2 Automotive Connector Standards

Automotive connector operate under a combination of electrical, mechanical, thermal, vibration, moisture, corrosion, and assembly stresses. A connector that performs well in a laboratory at room temperature may still experience contact degradation, terminal movement, sealing problems, or intermittent electrical failures during vehicle operation.

This is why automotive connector qualification relies on structured testing standards and customer-specific requirements.

Two frequently encountered references are LV214 and SAE/USCAR-2.

Although both are used to evaluate automotive connector reliability, they are not identical standards and should not be treated as one-for-one alternatives.

LV214 is associated with the German automotive industry and the AK testing framework for automotive connectors. USCAR-2 is maintained within the USCAR/SAE ecosystem and defines performance testing for automotive electrical connector systems.

The right validation approach depends on the customer, vehicle program, connector architecture, electrical requirements, installation environment, and applicable specification.

LV214 vs USCAR-2 Automotive Connector Standards


1.What Is LV214?

LV214 is an automotive connector test specification developed within the German automotive industry.

It is commonly referenced in European automotive connector programs and is closely associated with German OEM requirements. Testing laboratories list LV214 alongside customer-specific specifications such as VW 75174 and other German automotive requirements.

The purpose of LV214 is to evaluate the performance and reliability of automotive connectors and terminals under defined mechanical, electrical, climatic, and application-related stresses.

Depending on the applicable revision and customer requirements, the validation framework can address areas such as:

  • Dimensional conformity
  • Visual inspection
  • Terminal characteristics
  • Contact resistance
  • Mating and unmating behavior
  • Terminal retention
  • Vibration
  • Temperature exposure
  • Temperature cycling
  • Humidity
  • Corrosion
  • Mechanical durability
  • Connector locking
  • Crimp-related characteristics

LV214 is therefore more than a simple environmental test. It is part of a broader connector qualification approach.


2.What Is USCAR-2?

USCAR-2 is the Performance Specification for Automotive Electrical Connector Systems developed within the USCAR/SAE framework.

The current published revision is USCAR2-9, revised December 6, 2024. It covers performance testing of electrical terminals, connectors, and related components used in road-vehicle electrical connection systems. The current scope includes low-voltage systems from 0 to 60 VDC as well as coaxial applications, with specific exclusions defined by the specification.

USCAR-2 covers testing across different stages of the product lifecycle, including:

  • Development
  • Production
  • Field analysis

It also places responsibility on the supplier for verifying and documenting applicable test results and acceptance criteria.

This makes USCAR-2 particularly important when developing connector systems for automotive programs that specify the USCAR validation framework.


3.LV214 vs USCAR-2: The Basic Difference

The easiest way to understand the relationship is to look at their origins and intended engineering ecosystems.

ItemLV214USCAR-2
Industry backgroundGerman / European automotiveNorth American automotive
Organization / frameworkAK automotive connector testing frameworkUSCAR / SAE
Main purposeAutomotive connector and terminal qualificationAutomotive electrical connector system performance
Typical program contextEuropean / German OEM programsNorth American OEM programs
Test philosophyStructured connector qualification and reliability testingPerformance testing across development, production and field analysis
Customer-specific requirementsOften importantOften important
Interchangeable?NoNo

The key point is that LV214 and USCAR-2 overlap in many technical objectives, but their requirements, test methods, severity levels, sample plans, and acceptance criteria can differ.

A connector passing one standard should not automatically be described as compliant with the other.


4.Why Do Both Standards Exist?

Automotive connector reliability is influenced by vehicle architecture, regional engineering practices, OEM requirements, and historical validation methods.

Different automotive markets developed their own qualification frameworks.

As a result, connector manufacturers supplying global automotive customers may encounter several validation systems within the same product portfolio.

For example, a supplier may need to support:

  • LV214
  • USCAR-2
  • ISO 16750
  • Customer-specific OEM specifications
  • Terminal and crimp specifications
  • Internal engineering validation requirements

The important engineering task is therefore not to ask:

Which standard is better?

A more useful question is:

Which validation requirements apply to this specific connector, vehicle program, and installation environment?


5.How LV214 and USCAR-2 Overlap

Despite their differences, both standards address the fundamental reliability challenges of automotive connectors.

These include:

Electrical reliability

Both validation approaches consider electrical performance such as contact behavior and electrical continuity.

The objective is to ensure that the connection remains electrically stable under the specified conditions.

Mechanical reliability

Automotive connectors must withstand:

  • Vibration
  • Mechanical loads
  • Mating cycles
  • Terminal movement
  • Connector retention forces

Mechanical degradation can eventually become an electrical failure.

Environmental reliability

Automotive connectors may experience:

  • High temperature
  • Low temperature
  • Thermal cycling
  • Humidity
  • Water exposure
  • Corrosive environments
  • Automotive fluids

Both validation frameworks therefore require consideration of environmental stress.

Terminal performance

The terminal is one of the most critical elements in the connector system.

Poor terminal geometry, inadequate contact force, improper retention, or unstable crimping can produce failures even when the connector housing itself is mechanically intact.


6.LV214 vs USCAR-2: Test Philosophy

One of the most important differences is not simply which tests exist, but how the overall qualification process is structured.

LV214

LV214 is commonly used as part of European automotive connector qualification, with strong attention to connector and terminal characteristics under defined test groups and automotive environmental conditions.

Testing laboratories identify LV214 as an automotive connector test specification and list it alongside German OEM-related connector specifications.

USCAR-2

USCAR-2 takes a broader performance-specification approach covering testing through development, production, and field analysis.

The current USCAR2-9 also emphasizes documented verification of applicable requirements and acceptance criteria by the supplier.

Therefore, the validation strategy should consider not only the test list but also:

  • Sample configuration
  • Test sequence
  • Test severity
  • Acceptance criteria
  • Measurement method
  • Documentation
  • Customer requirements

7.Electrical Testing: Contact Resistance Matters

Contact resistance is one of the most important parameters in automotive connector validation.

A connector with excessive or unstable contact resistance can generate localized heating and electrical performance problems.

The basic relationship is:

P = I²R

where:

  • P = power dissipated as heat
  • I = current
  • R = resistance

For this reason, contact resistance should not be considered only as an initial value.

A robust validation strategy should examine whether contact resistance remains stable after exposure to:

  • Vibration
  • Thermal cycling
  • Humidity
  • Corrosion
  • Mating cycles
  • Mechanical stress

The important engineering question is not simply:

Is the initial resistance low?

It is:

Does the contact system maintain stable electrical performance after the expected service stresses?


8.Mechanical Validation: Vibration and Terminal Retention

Automotive connectors can experience continuous mechanical excitation throughout vehicle operation.

Vibration can produce microscopic relative movement between mating contacts, potentially contributing to fretting and contact degradation.

Terminal retention is another important area.

A terminal that moves backward inside the housing can result in:

  • Incomplete mating
  • Reduced contact engagement
  • Increased electrical resistance
  • Intermittent signal
  • Loss of circuit continuity

Therefore, connector validation should evaluate both the electrical interface and the mechanical retention system.

The exact vibration profile and mechanical requirements should always be taken from the applicable standard revision and customer specification rather than assumed from a generic test matrix.


9.Environmental Validation: Temperature and Humidity

Automotive connectors can operate across large temperature ranges.

Thermal stress affects:

  • Housing materials
  • Terminal materials
  • Contact force
  • Plating
  • Seals
  • Dimensional stability

Temperature cycling can be especially important because repeated expansion and contraction may gradually change the mechanical relationship between different materials.

Humidity and water exposure introduce another set of risks.

Moisture can contribute to:

  • Corrosion
  • Leakage current
  • Insulation degradation
  • Contact resistance increase

For sealed automotive connectors, environmental validation should therefore consider both the initial sealing capability and the ability of the sealing system to maintain performance after mechanical and thermal stresses.


10.Corrosion and Surface Protection

Terminal plating is an important part of automotive connector reliability.

A connector’s electrical performance depends on the condition of its contact interface.

Potential problems include:

  • Oxidation
  • Corrosion
  • Plating wear
  • Surface contamination
  • Fretting-related surface damage

The plating system must therefore be selected according to:

  • Base material
  • Contact force
  • Mating cycles
  • Current level
  • Environmental exposure
  • Temperature
  • Required service life

Validation should confirm that the contact interface remains within the required performance limits after applicable environmental and mechanical stresses.


11.LV214 and USCAR-2 Are Not Interchangeable

This is one of the most important points for automotive connector manufacturers.

A connector tested according to LV214 should not automatically be described as USCAR-2 compliant.

Likewise, passing USCAR-2 does not automatically establish LV214 compliance.

Why?

Because standards can differ in:

  • Test methods
  • Test sequences
  • Severity levels
  • Sample quantities
  • Acceptance criteria
  • Measurement methods
  • Environmental conditions
  • Mechanical loads
  • Customer-specific interpretations

A real connector project may require testing against one standard, the other, or a combination of applicable standards.

A manufacturer should therefore create a requirements-to-test matrix before validation begins.


12.Customer Requirements Always Come First

Industry standards provide a technical framework, but automotive programs frequently include additional customer requirements.

For example, an OEM may specify:

  • Specific vibration severity
  • Specific temperature range
  • Specific mating-cycle requirements
  • Additional water-ingress testing
  • Special chemical exposure
  • Additional terminal tests
  • Special crimp requirements
  • Additional electrical monitoring
  • Customer-specific acceptance criteria

This means that a connector cannot be validated correctly simply by saying:

“We tested it according to LV214.”

or:

“We tested it according to USCAR-2.”

The engineering team needs to identify the exact revision, applicable clauses, customer deviations, additional requirements, and connector configuration.


13.How to Choose Between LV214 and USCAR-2

The decision should start with the customer and vehicle program.

Choose LV214 when:

  • The customer specification requires LV214.
  • The program is based on a European or German automotive qualification framework.
  • The OEM drawing or validation plan references LV214.
  • The connector is being developed for a program that specifically requires LV214 testing.

Choose USCAR-2 when:

  • The customer specification requires USCAR-2.
  • The program follows the USCAR/SAE validation framework.
  • The OEM or Tier-1 customer references USCAR-2.
  • The connector is intended for an application requiring USCAR-2 performance validation.

Use both when required

Global automotive programs may require evidence against multiple standards.

In that situation, the best approach is not simply to duplicate the entire test program without analysis.

Instead, engineers should create a gap analysis:

LV214 Requirements

↓

USCAR-2 Requirements

↓

Common Tests

↓

Different Tests

↓

Different Severity / Acceptance Criteria

↓

Customer-Specific Requirements

↓

Final Validation Matrix

This can reduce unnecessary duplication while ensuring that no required test is overlooked.


14.Building a Connector Validation Matrix

A validation matrix helps engineers convert standards into an executable test plan.

A simplified structure could look like this:

Validation AreaLV214USCAR-2Project Requirement
Visual / dimensional inspectionApplicableApplicableConfirm drawing
Contact resistanceApplicableApplicableDefine limits
Insulation performanceApplicable as specifiedApplicable as specifiedCustomer requirement
Mating / mechanical behaviorApplicableApplicableDefine cycles/force
Terminal retentionApplicableApplicableConfirm terminal system
VibrationApplicableApplicableDefine severity
Temperature exposureApplicableApplicableDefine profile
Thermal cyclingApplicableApplicableDefine profile
Humidity / waterApplication-dependentApplication-dependentDefine environment
CorrosionApplication-dependentApplication-dependentDefine exposure
Additional OEM testsPossiblePossibleCustomer-specific

This table is only a planning framework.

The actual test conditions, sample quantities, acceptance criteria, and sequences must be taken from the applicable standard revision and customer documentation.


15.Why Test Sequence Matters

Testing individual characteristics separately does not always reproduce the actual degradation mechanism.

For example:

Thermal Cycling → Vibration → Electrical Measurement

can reveal a different result from testing the same parameters independently.

A connector may initially have:

  • Low contact resistance
  • Strong terminal retention
  • Good sealing

But after repeated environmental and mechanical stress, the interface may experience:

  • Contact movement
  • Seal compression changes
  • Material expansion mismatch
  • Surface wear
  • Corrosion

Therefore, validation planning should consider test sequence and accumulated exposure, not only individual test items.


16.Validation Should Connect With DFMEA

A good connector validation program should be connected to Design FMEA.

For example:

Failure ModePotential CauseValidation Focus
High contact resistanceContact wearElectrical measurement + durability
Intermittent signalVibration / frettingVibration + dynamic monitoring
Terminal back-outWeak retentionRetention testing
Water ingressSeal compression lossEnvironmental / sealing testing
Housing crackThermal or mechanical stressTemperature + mechanical validation
CorrosionMoisture / contaminationEnvironmental exposure
Lock failureInsufficient locking strengthMechanical validation

This approach ensures that testing is driven by actual engineering risk rather than simply by a checklist.


17.LV214 vs USCAR-2 for Global Automotive Connector Suppliers

For suppliers serving international automotive customers, maintaining capability for multiple validation frameworks can be valuable.

A global connector development process may need to accommodate:

  • European OEM requirements
  • North American OEM requirements
  • Customer-specific specifications
  • Regional environmental conditions
  • Different vehicle installation positions
  • Different terminal and connector architectures

The engineering challenge is therefore not simply laboratory capability.

It is the ability to translate customer requirements into:

Design Requirements → DFMEA → Test Matrix → Sample Preparation → Validation → Failure Analysis → Corrective Action → Documentation

This creates a repeatable development process across different automotive programs.


18.What Automotive Connector Manufacturers Should Verify Before Testing

Before starting formal validation, engineers should confirm:

1.Standard revision

Do not rely on an old copy or outdated test matrix.

2.Product configuration

Confirm:

  • Housing
  • Terminal
  • Seal
  • CPA/TPA
  • Plating
  • Wire size
  • Mating connector
  • Mounting configuration

3.Application environment

Identify:

  • Vehicle location
  • Temperature
  • Vibration
  • Moisture
  • Chemical exposure
  • Cable movement
  • Current load

4.Customer requirements

Check all OEM and Tier-1 requirements in addition to the base standard.

5.Acceptance criteria

Define exactly what constitutes a pass or failure.

6.Documentation

Plan the required test report, sample identification, measurement data, photographs, failure analysis, and DVP&R documentation before testing starts.

USCAR2-9 specifically requires applicable verification and documentation of results and acceptance criteria by the supplier.


How FPIC Approaches Automotive Connector Validation

Automotive connector validation should be connected to the complete product development process rather than treated as an isolated laboratory activity.

FPIC supports automotive connector projects with engineering development, prototyping, automated production, electrical testing, dimensional inspection, and mass-production quality control.

For customer-specific automotive programs, the validation strategy can be structured around the applicable requirements, including LV214, USCAR-2, customer specifications, and project-specific environmental conditions.

FPIC’s automotive connector manufacturing experience also includes production quality requirements associated with automotive applications, helping connect:

Connector Design → Prototype Verification → Reliability Validation → Process Control → Mass Production

This integrated approach can help identify potential failure risks earlier and improve consistency when a validated connector moves into production.


Final Thoughts

LV214 and USCAR-2 both play important roles in automotive connector validation, but they serve different automotive engineering ecosystems and should not be treated as interchangeable standards.

LV214 is widely associated with European and German automotive connector qualification, while USCAR-2 is an SAE/USCAR performance specification used extensively in North American automotive programs. The current USCAR2-9 revision was published in December 2024 and defines its own scope, testing requirements, verification responsibilities, and documentation expectations.

For connector manufacturers, the best approach is to start with the customer and vehicle application, identify the exact applicable standard revision, map common and unique requirements, and then build a project-specific validation matrix.

The goal is not simply to pass a standard.

The goal is to demonstrate that the connector can maintain electrical, mechanical, environmental, and manufacturing reliability throughout its intended service life.


FAQ

Is LV214 the same as USCAR-2?

No. LV214 and USCAR-2 have overlapping automotive connector reliability objectives, but they originate from different automotive qualification frameworks and can differ in test methods, severity, sample requirements, and acceptance criteria.

Which is stricter, LV214 or USCAR-2?

There is no universally correct answer. The severity depends on the specific test, revision, connector configuration, application, and customer requirement. A better approach is to compare the actual project requirements rather than labeling one standard as universally stricter.

Is LV214 mainly used for European automotive programs?

LV214 is strongly associated with German and European automotive connector qualification and is commonly encountered in European OEM programs. However, the applicable requirement must always be confirmed from the specific customer documentation.

Is USCAR-2 only for American car manufacturers?

Not necessarily. USCAR-2 is part of the SAE/USCAR ecosystem and is widely used in North American automotive programs, but suppliers in other regions may also encounter it when serving customers or programs that specify USCAR requirements.

Can a connector tested to LV214 also pass USCAR-2?

It may perform well against both, but LV214 testing alone does not automatically establish USCAR-2 compliance. The actual requirements must be compared and any additional or different tests completed.

What is the current USCAR-2 revision?

The current SAE specification is USCAR2-9, revised December 6, 2024. It covers road-vehicle electrical connection systems within its defined scope, including 0–60 VDC low-voltage applications and coaxial applications.

Should automotive connector suppliers test to both standards?

Only when required by the customer, vehicle program, or project validation plan. When both are required, a requirements gap analysis can identify common tests and additional requirements before the final validation matrix is established.


Need an automotive connector validated to LV214, USCAR-2, or customer-specific requirements?

FPIC supports automotive connector development from engineering design and prototype verification to reliability testing, production validation, and mass production. Contact our engineering team to discuss your connector configuration and validation requirements.


Resources

  1. SAE International – USCAR2-9: Performance Specification for Automotive Electrical Connector Systems
    Official SAE information for the current USCAR2-9 revision, including scope and verification requirements.
    SAE USCAR2-9 Official Specification
  2. USCAR – USCAR-2 Connector Testing
    Official USCAR resource for automotive connector testing information and related documentation.
    USCAR-2 Connector Testing
  3. IMA Dresden – LV214 Automotive Connector Testing
    Testing reference describing LV214 as an automotive connector test specification and its relationship with other European automotive requirements.
    IMA Dresden LV214 Testing Reference
  4. Molex – Product Specification Referencing LV214 and USCAR2
    Example of an automotive connector product specification referencing both LV-214 and USCAR2 as applicable standards.
    Molex Automotive Connector Specification
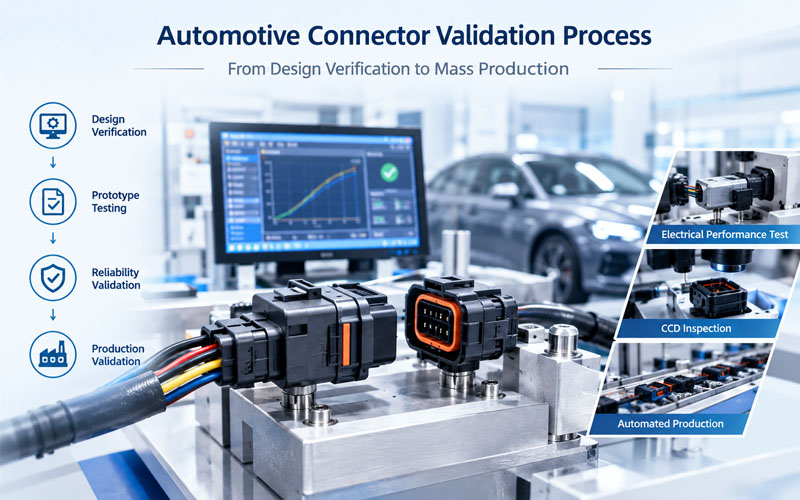
Automotive Connector Validation Process

An automotive connector must perform reliably throughout the vehicle’s service life while being exposed to vibration, temperature variation, moisture, chemicals, mating cycles, mechanical loads, and electrical stress.

For this reason, connector validation cannot be treated as a single final inspection step. It is a staged engineering process that begins with design requirements and continues through prototype verification, reliability testing, manufacturing validation, and mass-production control.

The objective is not simply to demonstrate that one connector sample works. The objective is to establish evidence that the design is suitable, the manufacturing process is capable, and the production connector will consistently meet defined requirements.

Automotive connector validation commonly involves customer-specific specifications together with applicable industry and vehicle standards. For example, ISO 16750 provides environmental testing frameworks for road-vehicle electrical and electronic components, while SAE/USCAR specifications are used for particular connector and terminal validation requirements. The exact validation matrix should always be based on the customer’s drawing, specification, application, and mounting environment.

Automotive Connector Validation Process


1.Automotive Connector Validation Starts With Design Requirements

Before testing begins, engineers need to establish exactly what the connector is expected to withstand.

Typical requirements include:

  • Rated voltage and current
  • Contact resistance
  • Insulation resistance
  • Dielectric withstand voltage
  • Number of circuits
  • Terminal size and contact system
  • Mating and unmating force
  • Terminal retention force
  • Connector locking force
  • CPA and TPA requirements
  • Sealing and IP protection requirements
  • Operating temperature range
  • Vibration and mechanical loads
  • Thermal cycling requirements
  • Humidity and water exposure
  • Chemical resistance
  • Mating-cycle requirements
  • Packaging and transportation requirements
  • Dimensional and tolerance requirements

The connector’s installation position is particularly important. A connector mounted inside a protected passenger compartment does not necessarily experience the same environmental stresses as one located in an engine compartment, underbody area, door, battery system, or other exposed location.

ISO 16750-3:2023 addresses mechanical loads, while ISO 16750-4:2023 addresses climatic loads for road-vehicle electrical and electronic equipment. These standards emphasize that environmental requirements should be related to the component’s specific vehicle mounting conditions.

Key question at this stage

The engineering team should be able to answer:

What failure modes must this connector prevent during its intended service life?

This question becomes the foundation for the validation plan.


2.Design Verification: Check the Connector Before Formal Reliability Testing

Design verification is intended to confirm that the physical connector design satisfies its engineering requirements before significant resources are invested in full validation.

Typical design verification activities include:

Dimensional verification

Critical dimensions should be measured against the released drawing.

Important characteristics may include:

  • Terminal cavity dimensions
  • Connector mating interface
  • Terminal positioning
  • CPA and TPA dimensions
  • Seal dimensions
  • Mounting features
  • Polarization features
  • Locking structures
  • Keying geometry

Dimensional variation can directly affect terminal retention, mating performance, sealing, and assembly compatibility.

Material verification

Engineers may verify:

  • Housing material
  • Terminal base material
  • Plating system
  • Seal material
  • CPA/TPA material
  • Temperature capability
  • Chemical compatibility

Material selection should be considered together with the actual application environment rather than evaluated independently.

Mechanical design verification

Mechanical checks can include:

  • Mating force
  • Unmating force
  • Terminal insertion force
  • Terminal retention
  • Connector retention
  • Lock engagement
  • CPA engagement
  • TPA engagement
  • Housing strength

These tests help identify weaknesses in the connector architecture before environmental validation begins.


3.Prototype Validation: Confirm the Design With Representative Samples

Once the design has passed initial verification, representative prototypes can be used for more comprehensive testing.

Prototype samples should reflect the intended production design as closely as possible.

This includes:

  • Final or production-intent materials
  • Production-intent terminals
  • Production-intent plating
  • Representative seals
  • Representative molding conditions
  • Correct assembly configuration

Testing an early prototype made from temporary materials may provide useful engineering information, but it should not automatically be treated as production validation evidence.

Why production-intent samples matter

Connector performance can be influenced by:

  • Resin shrinkage
  • Molding parameters
  • Terminal forming
  • Plating thickness
  • Crimp geometry
  • Seal compression
  • Assembly variation

Therefore, validation should progressively move toward samples produced using the same materials, tooling concepts, processes, and controls expected in mass production.


4.Electrical Validation

Electrical validation confirms that the connector can maintain safe and stable electrical performance.

Common electrical tests include:

Contact resistance

Low and stable contact resistance is important because resistance generates heat under current load.

The basic relationship is:

P = I²R

Even a small increase in resistance can create additional localized heating in high-current applications.

Contact resistance should therefore be evaluated both initially and after applicable environmental or mechanical stresses.

Insulation resistance

Insulation resistance testing evaluates whether adequate electrical isolation exists between conductive circuits and other specified points.

This becomes particularly important for connectors exposed to:

  • Moisture
  • Contamination
  • High temperature
  • Thermal cycling
  • Aging
  • High voltage

Dielectric withstand voltage

Dielectric withstand testing evaluates the connector’s ability to withstand a specified voltage without electrical breakdown.

The actual test voltage, duration, configuration, and acceptance criteria should be defined by the applicable customer and product specification.

Continuity and intermittent monitoring

For connectors exposed to vibration or mechanical movement, continuous electrical monitoring during mechanical testing can help identify intermittent contact events that may not be visible during a simple pre-test and post-test resistance measurement.


5.Mechanical Validation

Automotive connectors must remain mechanically stable after repeated mating and exposure to vehicle loads.

Typical mechanical validation may include:

Mating and unmating force

Excessive mating force can create assembly problems, while insufficient retention or locking force can increase the risk of incomplete engagement.

The target is a controlled interface that supports reliable assembly and serviceability.

Terminal retention

Terminal retention testing verifies that terminals remain properly positioned within the connector housing.

Terminal back-out can cause:

  • Intermittent electrical connection
  • Increased contact resistance
  • Incomplete mating
  • Circuit interruption

Connector retention

The complete connector may also need to remain securely mounted to a mating component, bracket, module, or vehicle structure.

Vibration and mechanical loads

Automotive connectors can experience continuous vibration and mechanical loads throughout vehicle operation.

ISO 16750-3:2023 specifically addresses mechanical loads for road-vehicle electrical and electronic equipment.

Validation should consider the actual mounting condition, connector orientation, cable loading, and expected vehicle environment.


6.Environmental Validation

Environmental validation is where many connector design weaknesses become visible.

Automotive connectors may encounter:

  • High and low temperatures
  • Rapid temperature changes
  • Humidity
  • Water exposure
  • Salt contamination
  • Dust
  • Automotive fluids
  • Vibration
  • Mechanical shock

ISO 16750-4:2023 addresses climatic loads for road-vehicle electrical and electronic equipment, while ISO 16750-2:2023 addresses electrical loads.

Temperature cycling

Thermal cycling can create repeated expansion and contraction of:

  • Housing materials
  • Terminals
  • Seals
  • Plated surfaces
  • Mating interfaces

Differences in material expansion can gradually affect contact force, sealing, and dimensional stability.

Humidity and water exposure

Moisture can contribute to:

  • Corrosion
  • Leakage current
  • Insulation degradation
  • Contact resistance increase

For sealed connectors, validation should consider both the sealing system and the mechanical interface.

Chemical exposure

Depending on the application, connectors may be exposed to substances such as:

  • Engine fluids
  • Cleaning agents
  • Fuel-related contaminants
  • Salt
  • Coolants
  • Oils and lubricants

The exact chemical test conditions should follow the applicable customer specification.


7.Connector Sealing and Water Ingress Validation

For sealed automotive connectors, environmental protection depends on the entire sealing architecture rather than the housing alone.

Important elements include:

  • Interface seals
  • Wire seals
  • Cable diameter compatibility
  • Seal compression
  • Housing tolerances
  • Terminal cavity geometry
  • Connector locking
  • Assembly condition

A connector may pass a basic sealing test initially but experience leakage after thermal cycling, vibration, or repeated mating.

Therefore, sealing validation should be considered as part of the complete reliability sequence.

A practical validation principle

Instead of asking only:

Does the connector pass the water-ingress test?

Engineers should also ask:

Does the connector maintain its sealing performance after the mechanical and environmental stresses expected during service?

This distinction is important for long-term reliability.


8.Validation After Environmental Stress

Post-test inspection is just as important as the environmental test itself.

After a test sequence, engineers may evaluate:

  • Contact resistance
  • Insulation resistance
  • Dielectric withstand
  • Terminal retention
  • Mating force
  • Seal condition
  • Housing deformation
  • Terminal plating
  • Corrosion
  • Cracking
  • Discoloration
  • Terminal displacement

The purpose is to identify both immediate failures and degradation trends.

For example, a connector that still functions after thermal cycling but shows a significant increase in contact resistance may require further engineering investigation.


9.Reliability Validation Should Reflect Real Failure Mechanisms

A strong validation plan is not simply a long list of tests.

Each test should have a reason.

For example:

Potential Failure ModeRelevant Validation Focus
Contact resistance increaseElectrical resistance measurement
Terminal back-outTerminal retention and mechanical testing
FrettingVibration and electrical monitoring
Housing crackingMechanical and thermal stress
Water ingressSealing and environmental testing
CorrosionHumidity, salt and chemical exposure
Lock failureMating, retention and mechanical testing
Seal degradationTemperature and environmental exposure
Insulation breakdownIR and dielectric withstand testing

This approach makes validation more efficient because the test plan is connected directly to identified risks.


10.DFMEA and Validation Should Be Connected

Design Failure Mode and Effects Analysis (DFMEA) can help engineers identify potential failure modes before testing begins.

For an automotive connector, DFMEA considerations may include:

  • Contact system
  • Terminal geometry
  • Housing structure
  • Locking mechanism
  • CPA/TPA
  • Sealing system
  • Material selection
  • Plating
  • Mounting features
  • Cable interface
  • Assembly orientation

The validation plan should then address the significant risks identified during design analysis.

This creates a closed engineering loop:

Requirement → Design → DFMEA → Validation Plan → Testing → Failure Analysis → Design Improvement → Revalidation

This process is more effective than waiting for a final validation test to reveal a design weakness.


11.From Design Validation to Manufacturing Validation

Passing design validation does not automatically mean that the connector is ready for mass production.

The manufacturing process must also be validated.

Typical manufacturing considerations include:

  • Injection molding capability
  • Terminal stamping and forming
  • Plating control
  • Crimping process
  • Terminal insertion
  • Seal installation
  • Connector assembly
  • Automated inspection
  • Electrical testing
  • Dimensional inspection
  • Traceability

The objective is to demonstrate that the production process can repeatedly manufacture connectors that meet the validated design requirements.


12.Process Validation Before Mass Production

Manufacturing validation should focus on process capability and repeatability.

Typical controls may include:

Incoming material control

Verify critical materials and components before production.

Tooling control

Injection molds and stamping tools should maintain critical dimensions throughout production.

Crimp process control

For connector assemblies involving wires and terminals, crimp quality is critical.

Possible controls include:

  • Crimp height
  • Crimp width
  • Pull force
  • Cross-section analysis
  • Terminal position
  • Conductor insertion

Automated inspection

Depending on product complexity, production may use:

  • CCD vision inspection
  • Dimensional inspection
  • Terminal position detection
  • Electrical continuity testing
  • Functional testing

Traceability

Production traceability can connect:

Raw Material → Process Lot → Tooling → Machine → Operator/Station → Inspection Data → Finished Product

This becomes especially important when supplying automotive customers.


13.Pilot Production and Production Validation

Before full-scale mass production, a pilot or production-validation run can help confirm that the manufacturing process performs under realistic production conditions.

The objective is to verify:

  • Production cycle stability
  • Assembly consistency
  • Inspection capability
  • Yield
  • Process capability
  • Packaging
  • Labeling
  • Traceability
  • Operator workflow
  • Quality control points

The samples from this stage should represent the actual production process as closely as possible.

A successful engineering prototype does not necessarily guarantee stable mass production. Production validation closes this gap.


14.PPAP and Customer Approval

For many automotive programs, production approval involves structured documentation and customer-specific requirements.

Depending on the customer and program, documentation may include:

  • Design records
  • Engineering change documentation
  • Process flow
  • PFMEA
  • Control plan
  • Measurement system analysis
  • Dimensional results
  • Material and performance results
  • Initial sample inspection
  • Process capability evidence
  • Packaging specifications
  • Sample parts
  • Customer-specific documents

PPAP requirements vary by customer and program, so the exact submission package should be aligned with the applicable customer requirements.

The key objective is to demonstrate that the supplier understands the product requirements and has established a controlled process for producing conforming parts.


15.Mass Production Control Must Continue After Validation

Validation is not the end of quality management.

Once the connector enters mass production, the manufacturer must maintain control over the characteristics that were validated.

Important production controls may include:

  • Incoming inspection
  • First-piece inspection
  • In-process inspection
  • Automated electrical testing
  • Visual inspection
  • Dimensional monitoring
  • Crimp monitoring
  • Plating control
  • Process capability monitoring
  • Lot traceability
  • Final inspection
  • Periodic reliability testing

Process changes should also be managed carefully.

Changes involving materials, tooling, terminal geometry, plating, sealing components, or manufacturing parameters may require engineering review and potentially additional validation.


16.A Practical Automotive Connector Validation Flow

A complete validation process can be structured as follows:

1.Customer Requirements

↓

2.Application and Environmental Analysis

↓

3.Connector Design

↓

4.DFMEA and Risk Analysis

↓

5.Design Verification

↓

6.Prototype Testing

↓

7.Electrical, Mechanical and Environmental Validation

↓

8.Failure Analysis and Design Improvement

↓

9.Production-Intent Samples

↓

10.Manufacturing Process Validation

↓

11.Pilot Production

↓

12.PPAP / Customer Approval

↓

13.Mass Production

↓

14.Ongoing Quality and Change Control

This structure helps connect engineering development with manufacturing readiness.


17.Common Automotive Connector Validation Mistakes

Mistake 1: Testing too late

If reliability testing begins only after the design is finalized, failures may result in expensive redesign and schedule delays.

Better approach: connect DFMEA and validation planning to the early design stage.

Mistake 2: Validating only electrical performance

A connector may pass electrical testing while still having mechanical or environmental weaknesses.

Better approach: combine electrical, mechanical, climatic, sealing, and material-related validation.

Mistake 3: Using non-representative samples

Prototype samples made with temporary materials or processes may not accurately represent production performance.

Better approach: progressively transition toward production-intent samples.

Mistake 4: Ignoring post-test measurements

A pass/fail result alone may hide degradation.

Better approach: compare key parameters before and after environmental and mechanical testing.

Mistake 5: Treating validation as the end of quality control

A validated design can still experience production variation.

Better approach: connect product validation with process validation and ongoing production controls.


18.What a Strong Validation Report Should Demonstrate

A useful automotive connector validation report should clearly connect requirements, test conditions, results, and conclusions.

A typical structure includes:

SectionPurpose
Product identificationDefines the exact connector configuration
Applicable requirementsEstablishes acceptance criteria
Sample informationIdentifies samples and production status
Test methodDefines how the test was performed
Test conditionsRecords temperature, load, duration and other parameters
Initial resultsEstablishes baseline performance
Stress exposureRecords environmental or mechanical conditions
Final resultsShows post-test performance
Visual inspectionIdentifies physical degradation
Failure analysisExplains any abnormal result
Corrective actionDocuments engineering response
Final conclusionConfirms validation status

Good documentation makes validation results traceable and easier to review during customer approval and future engineering changes.


How FPIC Supports Automotive Connector Development

For automotive connector projects, validation should be considered together with design, manufacturing, and quality control.

FPIC supports automotive connector development from prototype and engineering verification through production, with automotive manufacturing experience and quality systems designed for demanding applications.

Its automotive connector capabilities include connector development, terminal processing, automated inspection, electrical testing, and production quality control. For projects requiring customer-specific validation, the test plan can be aligned with the applicable drawings, specifications, environmental conditions, and reliability requirements.

The goal is to establish a clear engineering path from:

Customer Requirement → Connector Design → Validation → Process Verification → Mass Production

This approach helps reduce late-stage design changes and supports more consistent production performance.


Final Thoughts

Automotive connector validation is not a single laboratory test. It is a staged process that begins with requirements and design verification and continues through reliability testing, manufacturing validation, customer approval, and mass-production control.

The most effective validation strategies connect each test to a specific failure mechanism and use representative samples to verify both product performance and process capability.

By integrating DFMEA, electrical testing, mechanical validation, environmental testing, production-intent samples, process controls, and ongoing quality management, automotive connector manufacturers can build a stronger technical foundation for reliable mass production.


FAQ

What is automotive connector validation?

Automotive connector validation is the process of verifying that a connector meets defined electrical, mechanical, environmental, reliability, and manufacturing requirements before and during production release.

What tests are commonly included in automotive connector validation?

Depending on the application, testing may include contact resistance, insulation resistance, dielectric withstand, mating force, terminal retention, vibration, temperature cycling, humidity, water ingress, corrosion, chemical exposure, and mating-cycle testing.

What is the difference between design verification and validation?

Design verification checks whether the connector design meets specified engineering requirements. Validation typically provides broader evidence that the product performs as intended under representative application and environmental conditions.

Why is production-intent sampling important?

Production-intent samples better represent the materials, tooling, processes, and assembly conditions expected during mass production, making the validation results more representative.

Is ISO 16750 sufficient for automotive connector validation?

Not necessarily. ISO 16750 provides environmental and electrical/mechanical testing frameworks for road-vehicle electrical and electronic equipment, but connector validation may also require customer-specific specifications and connector or terminal standards. The applicable validation matrix should be defined for the specific product and application.

When should connector validation begin?

Validation planning should begin during the design stage. Requirements, DFMEA, failure modes, and intended vehicle environment should be considered before formal reliability testing begins.


Developing a custom automotive connector?

FPIC can support automotive connector projects from design and prototype development to testing, process verification, and mass production. Contact our engineering team to discuss connector requirements, validation plans, environmental conditions, and production needs.


Resources

  1. ISO 16750-2:2023 – Electrical Loads
    International standard covering electrical loads and related test requirements for electrical and electronic equipment in road vehicles.
    ISO 16750-2:2023
  2. ISO 16750-3:2023 – Mechanical Loads
    Provides requirements and test guidance related to mechanical loads for road-vehicle electrical and electronic equipment.
    ISO 16750-3:2023
  3. ISO 16750-4:2023 – Climatic Loads
    Covers climatic loads and related testing considerations for vehicle electrical and electronic equipment.
    ISO 16750-4:2023
  4. USCAR-2 – Performance Specification for Automotive Electrical Connector Systems
    Provides an automotive connector validation framework covering new connector designs and related validation requirements.
    USCAR-2 Connector Testing Specification
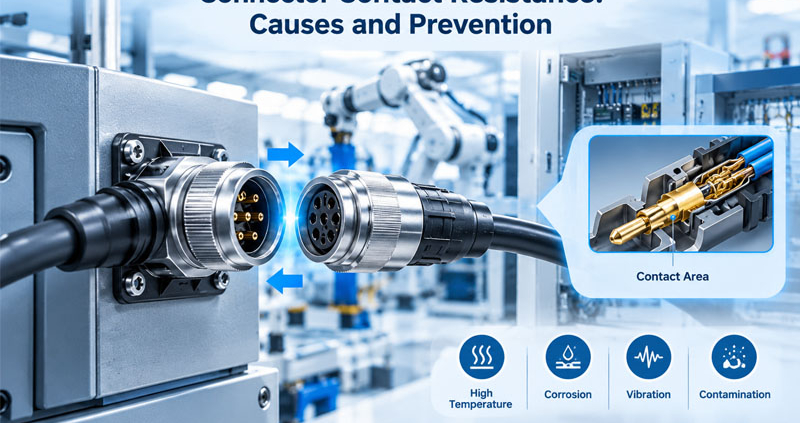
Connector Contact Resistance Causes and Prevention

Connector contact resistance is a critical electrical parameter that directly affects the reliability and efficiency of an electrical connection.

An ideal connector should provide a stable, low-resistance path between mating conductors. In real applications, however, the actual contact area is much smaller than the apparent physical contact area. Surface roughness, contact force, plating condition, contamination, vibration, temperature, and mechanical deformation can all influence the resistance of the connection.

When contact resistance increases, electrical losses and localized heating increase as well. The relationship can be expressed as:

P = I²R

where P is power loss, I is current, and R is contact resistance.

This becomes particularly important in high-current connectors, automotive systems, industrial automation equipment, energy storage systems, and other applications where connectors must operate reliably under continuous electrical and mechanical stress.

Understanding what causes contact resistance to increase—and how to prevent it—is therefore an important part of connector design and validation.

Connector Contact Resistance Causes and Prevention


1.What Is Connector Contact Resistance?

Connector contact resistance is the electrical resistance introduced at the interface between two mating conductive surfaces.

It is different from the resistance of the wire itself.

A simplified connection can be considered as:

Wire → Crimp → Terminal → Mating Contact → Terminal → Crimp → Wire

Each interface contributes to the overall electrical performance.

The mating contact is particularly important because two metal surfaces do not actually touch across their entire apparent area. Microscopic surface irregularities create localized conductive contact points known as asperities.

The effective electrical contact area is therefore much smaller than the visible mechanical contact area.

This is why contact force, surface condition, material selection, and plating have such a significant influence on connector resistance.


2.Why Low and Stable Contact Resistance Matters

Low contact resistance is important, but stable contact resistance over the connector’s service life is even more important.

A connector may initially show excellent electrical performance but experience increasing resistance after:

  • Repeated mating cycles
  • Vibration
  • Thermal cycling
  • Humidity exposure
  • Corrosion
  • High-current operation
  • Mechanical deformation
  • Surface wear

Increasing resistance can lead to several problems.

Electrical losses

Higher resistance increases voltage drop:

V = I × R

In low-voltage systems, even a small voltage drop can become significant.

Heat generation

Because:

P = I²R

heat generation increases rapidly as current rises.

For example, if current doubles, the resistive heating increases by approximately four times for the same resistance.

Accelerated degradation

Local heating can affect:

  • Contact plating
  • Terminal spring properties
  • Connector housing
  • Insulation
  • Sealing materials

This can create a feedback loop in which electrical degradation leads to additional thermal and mechanical degradation.


3.Contact Force and Contact Resistance

Contact force is one of the most important design factors affecting connector contact resistance.

When mating contacts are pressed together, sufficient force helps establish stable conductive contact points and break through surface films or contamination.

However, simply increasing contact force is not always the correct solution.

Excessive contact force can cause:

  • Higher insertion force
  • Difficult mating
  • Increased wear
  • Terminal deformation
  • Reduced connector service life

The objective is therefore to establish an appropriate contact-force window rather than maximizing force.

Important design factors include:

  • Contact geometry
  • Spring characteristics
  • Terminal material
  • Plating system
  • Contact wipe
  • Mating cycles
  • Required insertion force

A well-designed contact system should maintain adequate force throughout the expected operating life.


4.Contact Plating and Surface Condition

The contact surface plays a major role in electrical stability.

Common contact materials and plating systems are selected based on requirements such as:

  • Electrical conductivity
  • Corrosion resistance
  • Wear resistance
  • Mating frequency
  • Environmental exposure
  • Current level

Gold plating is commonly used where stable low-level electrical performance and corrosion resistance are important.

Tin plating can provide a practical solution for many applications, particularly where cost and current-carrying requirements are important.

However, plating selection should always be considered together with the contact geometry, environment, mating cycles, and application requirements.

Plating failure mechanisms

Contact resistance can increase when the surface experiences:

  • Wear-through
  • Oxidation
  • Corrosion
  • Plating porosity
  • Contamination
  • Mechanical damage

The correct plating system is therefore not simply a material-selection decision. It is part of the overall contact reliability strategy.


5.Fretting Corrosion and Vibration

Vibration can cause microscopic movement between mating contacts.

Although the movement may be too small to notice visually, repeated micro-motion can damage the contact surface.

This phenomenon is commonly associated with fretting corrosion.

A typical progression is:

Vibration → Micro-Motion → Surface Wear → Oxidation/Contamination → Increased Resistance

The problem can be especially challenging because a connector may pass a static resistance test while experiencing intermittent resistance changes during actual vibration.

Prevention strategies

Depending on the application, engineers can consider:

  • Appropriate contact force
  • Stable terminal retention
  • Suitable plating
  • Connector locking
  • Mechanical support
  • Cable strain relief
  • Vibration-resistant mounting

For vibration-sensitive systems, electrical monitoring during mechanical testing can provide more useful information than measuring resistance only before and after the test.


6.Crimp Quality Directly Affects Resistance

The contact interface is not the only resistance-sensitive area.

The wire-to-terminal crimp is another critical electrical connection.

A poor crimp can produce:

  • Higher resistance
  • Localized heating
  • Mechanical weakness
  • Intermittent electrical performance

Common causes include:

  • Incorrect crimp height
  • Wrong tooling
  • Improper conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Incorrect terminal-wire combination

How to control crimp resistance

Production quality control can include:

  • Crimp height measurement
  • Crimp force monitoring
  • Pull-force testing
  • Cross-section inspection
  • Electrical resistance testing

This is especially important for high-current and high-reliability cable assemblies.


7.Contamination and Oxidation

Even a well-designed contact system can experience resistance increases if the mating interface becomes contaminated.

Potential contaminants include:

  • Dust
  • Oil
  • Moisture
  • Chemical residues
  • Oxidation products
  • Assembly debris

Contamination can reduce the effective conductive area and interfere with stable metal-to-metal contact.

Environmental conditions therefore need to be considered during connector selection.

For outdoor or harsh industrial applications, engineers may need to evaluate:

  • Sealing
  • IP protection
  • Plating
  • Housing material
  • Environmental compatibility
  • Corrosion resistance

8.Connector Overheating and Thermal Runaway

High contact resistance is closely related to connector temperature rise.

Consider a high-current connection carrying 100 A.

If contact resistance is:

R = 1 mΩ

then:

P = 100² × 0.001 = 10 W

That means the contact interface is generating approximately 10 W of heat at that resistance.

If resistance increases to:

R = 2 mΩ

the heat generation becomes:

P = 100² × 0.002 = 20 W

The electrical loss has doubled.

This demonstrates why small changes in resistance can have a significant effect in high-current applications.

Thermal design should consider:

  • Current level
  • Number of energized contacts
  • Contact resistance
  • Ambient temperature
  • Duty cycle
  • Wire size
  • Connector housing
  • Heat dissipation
  • Installation conditions

Connector current ratings should therefore not be considered independently from the actual system conditions.


9.Mating Cycles and Contact Wear

Every mating and unmating operation can cause mechanical movement at the contact interface.

The contact surfaces may experience:

  • Sliding
  • Wiping
  • Friction
  • Plating wear
  • Spring deformation

After repeated cycles, the original surface condition may change.

For applications requiring frequent connection and disconnection, engineers should evaluate:

  • Rated mating cycles
  • Contact plating
  • Contact force
  • Wiping action
  • Wear resistance
  • Contact resistance after cycling

A connector should be validated against the actual expected service profile rather than relying solely on an initial resistance measurement.


10.Temperature Effects on Contact Resistance

Temperature can influence both electrical and mechanical properties.

As temperature changes, materials can expand and contract, affecting:

  • Contact dimensions
  • Contact force
  • Terminal alignment
  • Housing geometry
  • Plating interfaces
  • Crimp connections

High temperatures can also accelerate material aging and surface degradation.

Low temperatures may influence material flexibility and contact mechanics.

For connectors operating across wide temperature ranges, thermal cycling should therefore be included in reliability validation.


11.Connector Geometry and Current Distribution

Contact resistance is not determined by material alone.

The geometry of the contact system also matters.

Important design variables include:

  • Contact beam shape
  • Contact area
  • Contact normal force
  • Current path length
  • Terminal thickness
  • Contact alignment
  • Mating depth
  • Current distribution

For high-current applications, engineers need to consider how current flows through the complete terminal system rather than focusing only on the nominal contact area.

Poor geometry can create localized current concentration and thermal hotspots.


12.How to Measure Connector Contact Resistance

Accurate contact resistance measurement requires an appropriate test method.

For very low resistance values, ordinary two-wire measurements can be affected significantly by:

  • Test lead resistance
  • Connection resistance
  • Instrument limitations

A four-wire Kelvin measurement can provide better accuracy for low-resistance measurements because the current and voltage measurement paths are separated.

A simplified test arrangement is:

Current Source → Connector → Current Return

while separate sensing leads measure the voltage drop directly across the contact interface.

The resistance can then be calculated using:

R = V / I

Measurement consistency matters

Testing should define:

  • Test current
  • Test voltage
  • Measurement location
  • Mating condition
  • Stabilization time
  • Temperature
  • Number of samples
  • Acceptance criteria

Without consistent test conditions, resistance results may be difficult to compare.


13.Contact Resistance Testing During Reliability Validation

Initial resistance testing is only one part of connector validation.

A more useful strategy is to measure contact resistance at different stages.

For example:

Initial Measurement

↓

Mating Cycle Test

↓

Vibration Test

↓

Thermal Cycling

↓

Environmental Exposure

↓

Final Resistance Measurement

For demanding applications, electrical performance can also be monitored during mechanical or environmental testing.

This helps identify intermittent changes that may not be visible in a simple before-and-after measurement.


14.Common Connector Contact Resistance Problems

ProblemLikely CausePotential Solution
Initial resistance too highPoor contact geometryOptimize terminal design
Resistance increases after cyclingContact wearReview plating and contact force
Resistance fluctuates during vibrationFrettingImprove retention and contact stability
Resistance rises at high currentThermal stressOptimize current capacity and thermal design
High wire-to-terminal resistancePoor crimpImprove tooling and process control
Resistance increases in humid environmentsCorrosionImprove sealing and plating
Different samples show large variationProcess variationStrengthen dimensional and electrical controls
Localized terminal heatingCurrent concentrationReview contact geometry and current path

15.How to Prevent High Connector Contact Resistance

Preventing contact resistance problems requires cooperation between electrical, mechanical, material, and manufacturing design.

1.Optimize contact geometry

Design the contact system to maintain stable force and current distribution.

2.Select suitable plating

Match the plating system to electrical requirements, mating cycles, and environmental exposure.

3.Control crimp quality

Use controlled tooling, dimensional inspection, and appropriate mechanical and electrical verification.

4.Protect the contact interface

Use appropriate sealing and environmental protection for the application.

5.Control mechanical movement

Minimize vibration-induced micro-motion through proper locking, retention, mounting, and strain relief.

6.Validate under realistic conditions

Combine contact resistance testing with mating cycles, vibration, thermal cycling, and environmental exposure where applicable.

7.Monitor manufacturing variation

Stable connector performance requires stable production processes.


16.Design Considerations for High-Current Connectors

High-current applications are particularly sensitive to contact resistance.

Examples include:

  • Energy storage systems
  • Battery systems
  • Industrial power equipment
  • Power distribution
  • Automotive electrical systems
  • Inverters
  • Power conversion equipment

In these applications, engineers should evaluate the entire current path:

Cable → Crimp → Terminal → Contact Interface → Terminal → Crimp → Cable

A low-resistance contact interface cannot compensate for a poor crimp or undersized conductor.

The complete assembly therefore needs to be designed as one electrical and thermal system.


17.Manufacturing Controls for Stable Contact Resistance

For mass production, the challenge is not only achieving low resistance on one sample.

The objective is to maintain consistent performance across large production volumes.

Important controls may include:

  • Terminal dimensional inspection
  • Contact-force verification
  • Plating inspection
  • Crimp-height control
  • Crimp-force monitoring
  • Pull-force testing
  • Automated continuity testing
  • Contact resistance testing
  • Visual inspection
  • Traceability

Process data can help identify gradual changes before they become field failures.

For customized connectors and cable assemblies, early control of critical-to-quality characteristics can significantly improve production consistency.


How FPIC Supports Connector Electrical Reliability

FPIC develops customized connector and cable assembly solutions for industrial, automotive, energy, robotics, and other demanding applications.

Contact resistance can be evaluated as part of the complete electrical and mechanical design rather than treated as an isolated specification.

Depending on project requirements, engineering evaluation may cover:

  • Contact geometry
  • Terminal material
  • Plating
  • Contact force
  • Crimp design
  • Current capacity
  • Temperature rise
  • Environmental protection
  • Mating durability
  • Electrical testing
  • Reliability validation

This approach helps customers identify resistance-related risks early and develop connector systems with stable electrical performance throughout their intended service life.


Final Thoughts

Connector contact resistance is a small electrical parameter with potentially significant consequences.

When resistance increases, voltage drop and heat generation increase. In high-current systems, even a small resistance change can create substantial localized heating.

The most effective prevention strategy is therefore not simply to specify a low initial resistance.

Engineers should consider the complete system:

Contact Geometry + Contact Force + Plating + Crimp Quality + Environmental Protection + Mechanical Stability + Thermal Design + Validation

When these factors are controlled together, connector systems can maintain more stable electrical performance and reliability over their expected operating life.


FAQ

What causes connector contact resistance to increase?

Common causes include contact wear, insufficient contact force, damaged plating, fretting corrosion, contamination, oxidation, poor crimping, vibration, thermal cycling, and mechanical deformation.

Why does contact resistance cause connector overheating?

According to P = I²R, electrical power converted into heat increases with resistance and the square of current. High-current applications are therefore particularly sensitive to small resistance increases.

How is connector contact resistance measured?

Low-resistance connector contacts are commonly evaluated using controlled current and voltage measurements. Four-wire Kelvin measurement can improve measurement accuracy by reducing the influence of test lead resistance.

Does contact force affect connector resistance?

Yes. Contact force affects the stability and effective area of the conductive interface. Too little force can increase resistance, while excessive force can increase mating force and accelerate wear.

How can connector contact resistance be reduced?

Key methods include optimizing contact geometry, selecting suitable plating, controlling crimp quality, improving environmental protection, reducing vibration-induced micro-motion, and validating resistance after mechanical and environmental testing.


Need a Reliable Custom Connector Solution?

Looking for a connector solution with stable electrical performance under demanding operating conditions?

FPIC supports custom connector and cable assembly development, including contact design, terminal and plating selection, crimping, electrical testing, and reliability validation.

Contact FPIC to discuss your connector requirements and application conditions.


Resources

  1. TE Connectivity – Connector Solutions
    Technical resources covering connector systems, contacts, terminals, and electrical connection technologies.
    TE Connectivity Connector Solutions
  2. Molex – Connector Solutions
    Technical information covering connector design, contact technologies, and electrical performance considerations.
    Molex Connector Solutions
  3. IPC/WHMA-A-620 – Cable and Wire Harness Assemblies
    Industry requirements and acceptance criteria relevant to cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  4. IEC – International Electrotechnical Commission
    International standards and technical resources for electrical and electronic components and systems.
    IEC Standards
Connector Failure Analysis Common Causes and Solutions

Connectors are designed to provide a reliable electrical and mechanical interface between components, cables, and equipment. However, even a correctly specified connector can fail when electrical, mechanical, environmental, and manufacturing factors interact over time.

A connector failure may appear as a simple open circuit, intermittent signal, increased contact resistance, overheating, or mechanical disconnection. The visible symptom, however, is often not the actual root cause.

Effective connector failure analysis therefore requires more than replacing the failed component. Engineers need to determine why the connector failed, whether the failure originated in the contact system, terminal crimp, housing, sealing system, mating interface, or application environment.

This article examines the most common connector failure causes and explains practical methods for diagnosis, root-cause analysis, prevention, and validation.

Connector Failure Analysis Common Causes and Solutions


Why Connector Failure Analysis Matters

A connector is a system rather than a single component.

Its reliability depends on the interaction of:

  • Contact terminals
  • Plating and base materials
  • Connector housing
  • Crimp or termination system
  • Locking mechanism
  • Sealing components
  • Cable and strain relief
  • Mounting interface
  • Mating and unmating conditions
  • Electrical load
  • Temperature
  • Vibration and mechanical stress
  • Environmental contamination

A failure in any one of these areas can affect the complete electrical connection.

For example, an increase in contact resistance may initially appear to be a terminal problem. However, the actual cause could be insufficient contact force, fretting caused by vibration, damaged plating, terminal misalignment, or excessive thermal cycling.

This is why a structured failure analysis process is essential for demanding industrial and automotive applications.


1.Increased Contact Resistance

One of the most common connector problems is an increase in contact resistance.

When contact resistance rises, electrical losses increase according to:

P = I²R

At high current levels, even a relatively small increase in resistance can generate significant heat.

Common causes include:

  • Contact surface contamination
  • Oxidation or corrosion
  • Insufficient contact force
  • Damaged plating
  • Terminal deformation
  • Poor terminal alignment
  • Fretting corrosion
  • Excessive mating wear

Possible symptoms:

  • Localized heating
  • Voltage drop
  • Intermittent electrical performance
  • Discoloration around the terminal
  • Thermal damage to the housing

Solutions

Engineers should evaluate contact force, plating thickness, terminal geometry, mating cycles, and environmental conditions.

For high-current applications, the connector should also be evaluated under the actual operating current and temperature conditions rather than relying only on room-temperature resistance measurements.


2.Fretting Corrosion and Micro-Motion

Fretting is a particularly important failure mechanism in connectors exposed to vibration.

Small relative movements between mating contact surfaces can repeatedly disturb the contact interface. Over time, this can damage the plating and generate wear debris or oxidation products.

The result may be:

  • Increased contact resistance
  • Intermittent electrical connection
  • Signal instability
  • Progressive contact degradation

Fretting can be difficult to diagnose because the connector may initially pass a standard continuity test.

How to reduce fretting risk

Connector designs should consider:

  • Adequate contact normal force
  • Stable terminal retention
  • Appropriate plating systems
  • Mechanical locking
  • Vibration-resistant mounting
  • Proper cable strain relief

For applications involving continuous vibration, validation should include mechanical vibration testing combined with electrical monitoring.


3.Poor Crimping and Terminal Connection

A connector can contain a high-quality terminal and housing but still fail because the wire-to-terminal connection is defective.

Typical crimping problems include:

  • Insufficient crimp height
  • Excessive crimp height
  • Incorrect conductor positioning
  • Incomplete wire insertion
  • Damaged conductor strands
  • Improper tooling
  • Incorrect terminal-wire combination

A poor crimp can increase resistance and create mechanical weakness.

Why visual inspection alone is insufficient

A crimp may appear acceptable externally while having an internal defect.

For critical applications, manufacturers may use:

  • Crimp force monitoring
  • Crimp height measurement
  • Pull-force testing
  • Cross-section analysis
  • Electrical resistance testing

These controls help verify both mechanical and electrical integrity.


4.Connector Overheating

Connector overheating is often a secondary effect rather than the original failure.

A typical chain can be:

High Resistance → Heat Generation → Material Degradation → Higher Resistance → Thermal Failure

Potential causes include:

  • Excessive current
  • Undersized contacts
  • Insufficient contact force
  • Poor crimping
  • Contamination
  • Inadequate thermal management
  • Incorrect wire size
  • Loose or partially engaged terminals

How to prevent overheating

Connector selection should consider:

  • Rated current
  • Contact resistance
  • Wire gauge
  • Ambient temperature
  • Temperature rise
  • Duty cycle
  • Number of energized contacts
  • Housing material
  • Heat dissipation

The actual application conditions are particularly important because connector current ratings can depend on temperature and the number of simultaneously loaded circuits.


5.Terminal Back-Out and Poor Retention

A terminal may gradually move backward inside the connector housing if the retention mechanism is inadequate or the terminal is not fully inserted.

This can result in:

  • Reduced contact engagement
  • Intermittent connection
  • Increased resistance
  • Complete circuit interruption

Common causes

  • Incomplete terminal insertion
  • Damaged locking lance
  • Incorrect terminal dimensions
  • Excessive cable pulling force
  • Improper assembly
  • Housing deformation

Prevention

A robust connector system should incorporate reliable primary and secondary terminal locking where appropriate.

Manufacturing processes should also verify terminal insertion and retention rather than relying entirely on operator judgment.


6.Connector Mating and Misalignment Problems

Incorrect mating can cause mechanical and electrical damage.

Typical issues include:

  • Excessive insertion force
  • Cross-mating
  • Misalignment
  • Incomplete engagement
  • Damaged contacts
  • Housing deformation
  • Locking mechanism damage

A connector may appear connected while the terminals are not fully engaged.

Engineering solutions

Good connector design should provide clear mating guidance and positive locking feedback.

Depending on the application, features such as:

  • Polarization
  • Keying
  • Mechanical coding
  • CPA/secondary locks
  • Visual confirmation
  • Audible locking feedback

can reduce assembly errors.


7.Moisture, Dust, and Contamination

Environmental contamination is another major cause of connector degradation.

Moisture can promote corrosion, while dust, oil, chemicals, and other contaminants can affect contact interfaces and sealing performance.

This is particularly important for connectors used in:

  • Industrial automation
  • Outdoor equipment
  • Robotics
  • Automotive systems
  • Energy storage equipment
  • Medical equipment
  • Heavy machinery

Common symptoms

  • Corrosion
  • Leakage current
  • Increased contact resistance
  • Intermittent signals
  • Insulation degradation
  • Seal deterioration

Solutions

The connector’s environmental protection should match the actual application.

Depending on the system, engineers may need to evaluate:

  • IP protection
  • Seal material
  • Cable jacket compatibility
  • Connector material
  • Plating
  • Drainage
  • Chemical exposure
  • Temperature cycling

Waterproof performance should be validated under realistic environmental conditions rather than assumed from the connector specification alone.


8.Contact Plating Failure

Contact plating plays a critical role in long-term connector performance.

The plating system influences:

  • Corrosion resistance
  • Wear resistance
  • Contact stability
  • Mating durability
  • Environmental performance

A plating system that works well in a clean indoor application may not provide the same performance in a high-humidity, high-vibration, or corrosive environment.

Failure mechanisms may include:

  • Plating wear
  • Porosity
  • Oxidation
  • Corrosion
  • Base-metal exposure
  • Excessive mating wear

Therefore, plating selection should be based on the electrical requirements, mating cycles, environment, current level, and expected service life.


9.Mechanical Damage and Cable Strain

Connector failures do not always originate inside the connector.

Cable routing and mechanical loading can transfer excessive stress to the connector interface.

Typical causes include:

  • Excessive cable bending
  • Sharp routing angles
  • Insufficient strain relief
  • Pulling forces
  • Twisting
  • Repeated flexing
  • Incorrect mounting

Over time, these forces can damage terminals, seals, housings, or solder/crimp connections.

Prevention

A reliable connector assembly should consider the complete mechanical load path:

Cable → Strain Relief → Connector Housing → Terminal → Mating Interface

Proper strain relief and cable routing are therefore essential parts of connector reliability.


10.Thermal Cycling and Material Mismatch

Connectors used in industrial and automotive environments may experience repeated temperature changes.

Different materials expand and contract at different rates.

Repeated thermal cycling can influence:

  • Contact force
  • Terminal position
  • Housing dimensions
  • Seal compression
  • Crimp interfaces
  • Plating durability

A connector that performs well at room temperature may therefore experience degradation after repeated thermal cycles.

Recommended validation

Depending on the application, engineers may combine:

  • Thermal cycling
  • Temperature rise testing
  • Contact resistance measurement
  • Insulation resistance testing
  • Mechanical inspection

This helps determine whether electrical performance remains stable throughout the expected temperature range.


11.Vibration and Mechanical Shock

For industrial and automotive connectors, vibration can be a major reliability factor.

Repeated mechanical movement can affect:

  • Contact interfaces
  • Terminal retention
  • Housing locks
  • Cable terminations
  • Shielding connections

The key issue is that mechanical stress can eventually create an electrical failure.

Better validation strategy

Instead of performing vibration testing alone, combine mechanical vibration with continuous electrical monitoring.

For example:

Vibration → Electrical Monitoring → Contact Resistance Analysis → Physical Inspection

This approach can reveal intermittent failures that a simple post-test continuity check may miss.


12.A Structured Connector Failure Analysis Process

When a connector fails in the field or during testing, replacing the connector immediately can remove important evidence.

A structured investigation is more effective.

Step 1: Record the Failure Condition

Document:

  • Operating current
  • Voltage
  • Temperature
  • Environmental conditions
  • Mating cycles
  • Vibration exposure
  • Installation condition
  • Failure time
  • Electrical symptoms

Step 2: Perform Visual Inspection

Check for:

  • Discoloration
  • Melting
  • Corrosion
  • Cracks
  • Terminal displacement
  • Seal damage
  • Housing deformation

Step 3: Perform Electrical Testing

Depending on the failure mode:

  • Contact resistance
  • Continuity
  • Insulation resistance
  • HiPot
  • Voltage drop
  • Temperature rise

Step 4: Inspect the Terminal and Crimp

Evaluate:

  • Crimp geometry
  • Conductor placement
  • Pull strength
  • Terminal deformation
  • Contact surface condition

Cross-section analysis can be particularly useful for identifying internal crimp defects.

Step 5: Analyze the Environment

Determine whether the connector experienced:

  • Moisture
  • Dust
  • Chemicals
  • Salt exposure
  • Vibration
  • Thermal cycling
  • Mechanical stress

Step 6: Identify the Root Cause

Separate the failure symptom from the root cause.

For example:

  • Symptom: Connector terminal overheated
  • Immediate cause: Increased contact resistance
  • Root cause: Insufficient terminal contact force

This distinction is essential when developing corrective actions.


13.Connector Failure Analysis: Symptom vs Root Cause

Failure SymptomPossible Root CausesRecommended Investigation
High contact resistanceWear, corrosion, low contact forceContact resistance + terminal inspection
Connector overheatingExcess current, poor contact, bad crimpTemperature rise + resistance test
Intermittent signalFretting, vibration, terminal movementVibration test + electrical monitoring
Terminal back-outPoor retention, incomplete insertionRetention and insertion inspection
CorrosionMoisture, chemicals, poor sealingEnvironmental and seal inspection
Broken housingMechanical stress, impact, material issueMechanical inspection
Crimp failureIncorrect tooling or wire positioningCrimp cross-section + pull test
Insulation failureDamage, contamination, thermal agingIR + HiPot + visual inspection

14.Preventing Connector Failures During Product Development

Failure analysis should not only be performed after a product fails.

The most effective approach is to integrate reliability thinking into the design stage.

Design Review

Evaluate:

  • Current and voltage requirements
  • Contact system
  • Plating
  • Housing material
  • Environmental protection
  • Locking system
  • Strain relief
  • Mating cycles
  • Vibration
  • Temperature range

DFM and Assembly Review

Check:

  • Terminal insertion
  • Crimp process
  • Assembly sequence
  • Error-proofing
  • Inspection points
  • Test coverage

Reliability Validation

Depending on the application, validation may include:

  • Contact resistance testing
  • Temperature rise testing
  • Mating cycle testing
  • Vibration
  • Mechanical shock
  • Thermal cycling
  • Humidity
  • Salt spray
  • Waterproof testing
  • Insulation resistance
  • HiPot testing

The exact test plan should be based on the connector’s application and applicable customer or industry requirements.


15.Manufacturing Quality Control Is Part of Connector Reliability

Many connector failures originate from process variation rather than fundamental product design.

Important production controls include:

  • Terminal dimensional inspection
  • Plating inspection
  • Crimp height monitoring
  • Crimp force monitoring
  • Pull-force testing
  • Terminal retention testing
  • Housing dimensional control
  • Automated electrical testing
  • Visual inspection
  • Traceability

For high-reliability applications, process capability and traceability are particularly important because they help manufacturers identify whether a failure is an isolated defect or part of a larger production trend.


How FPIC Supports Connector Reliability

FPIC supports customized connector solutions for demanding industrial and automotive applications.

Our engineering approach considers connector performance across the complete product lifecycle—from component selection and structural design to manufacturing, inspection, electrical testing, and reliability validation.

Depending on project requirements, connector development can include evaluation of:

  • Terminal and contact design
  • Contact plating
  • Housing materials
  • Sealing systems
  • Locking mechanisms
  • Crimp quality
  • Shield termination
  • Environmental protection
  • Electrical performance
  • Mechanical reliability

For automotive connector applications, FPIC also applies controlled manufacturing and quality processes designed for demanding production requirements.

This engineering-focused approach helps customers identify potential failure mechanisms earlier and develop connector solutions with more stable long-term performance.


Final Thoughts

Connector failure is rarely caused by a single factor.

Electrical loading, contact force, plating, crimp quality, vibration, temperature, contamination, sealing, and mechanical stress can interact throughout the connector’s service life.

A professional connector failure analysis process therefore needs to move beyond identifying the visible symptom. Engineers should determine the failure mechanism, trace it back to the root cause, and then verify that the corrective action actually eliminates the problem.

For critical applications, the best strategy is to combine design review, manufacturing process control, electrical testing, environmental validation, and failure analysis from the beginning of the product development cycle.


FAQ

What are the most common causes of connector failure?

Common causes include increased contact resistance, fretting corrosion, poor crimping, overheating, terminal back-out, contamination, vibration, thermal cycling, and mechanical stress.

How can connector overheating be prevented?

Select an appropriate connector and terminal system for the actual current, temperature, duty cycle, and environmental conditions. Contact resistance and temperature rise should also be validated.

Why do connectors develop intermittent failures?

Intermittent failures are often related to vibration, fretting corrosion, insufficient contact force, terminal movement, poor retention, or mechanical stress.

How can a bad connector crimp be identified?

Crimp height, crimp force, pull strength, electrical resistance, and cross-section analysis can be used to evaluate crimp quality.

Is visual inspection enough for connector quality control?

No. Visual inspection is useful but cannot detect every internal or electrical defect. Depending on the application, electrical testing, dimensional inspection, crimp analysis, and reliability testing may also be required.


Need a Reliable Custom Connector Solution?

Looking for a connector supplier that can support custom design, terminal development, connector assembly, electrical testing, and reliability validation?

FPIC can help evaluate your application requirements and develop connector solutions for industrial automation, automotive, robotics, energy systems, and other demanding applications.

Contact FPIC to discuss your connector project and reliability requirements.


Resources

  1. USCAR-2 – Performance Specification for Automotive Electrical Connector Systems
    A widely referenced specification for evaluating automotive connector performance and durability.
    USCAR-2 Information
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    Provides industry requirements and acceptance criteria for cable and wire harness assembly processes.
    IPC/WHMA-A-620 Standard
  3. TE Connectivity – Connector Solutions
    Technical information covering connector systems, terminals, contact technologies, and application requirements.
    TE Connectivity Connector Solutions
  4. Molex – Connector Solutions
    Technical resources covering connector design, electrical performance, reliability, and application engineering.
    Molex Connector Solutions
  5. IEC – International Electrotechnical Commission
    International standards and technical resources relevant to electrical and electronic component reliability and testing.
    IEC Standards
How Connector Plating Affects Performance and Lifetime

Connector contacts may look like simple metal components, but their surface finish plays a critical role in long-term electrical and mechanical performance.

A connector can have the correct housing design, terminal geometry and contact force, yet still experience reliability problems if the plating system is not appropriate for its application.

Connector plating influences:

  • Contact resistance
  • Corrosion resistance
  • Wear resistance
  • Mating performance
  • Electrical stability
  • Environmental durability
  • Contact lifetime

For automotive electronics, industrial automation, robotics, energy storage and other demanding applications, plating should therefore be treated as part of the overall connector reliability strategy.


1.Why Connector Plating Matters

The base metal of a contact provides the mechanical and electrical foundation, but its exposed surface interacts directly with the surrounding environment.

During service, a connector may encounter:

  • Humidity
  • Oxygen
  • Salt contamination
  • Dust
  • Chemicals
  • Temperature cycling
  • Mechanical vibration
  • Repeated mating and unmating
  • Electrical current

Without an appropriate surface finish, the contact interface can gradually deteriorate.

Typical consequences include:

Surface oxidation → higher contact resistance → localized heating → unstable electrical performance

In signal applications, surface deterioration can also contribute to intermittent electrical behavior.

This is why connector plating is not simply a cosmetic treatment. It is an engineered interface between the terminal and its operating environment.

How Connector Plating Affects Performance and Lifetime


2.What Is Connector Contact Plating?

Connector contact plating is a metallic coating applied to the surface of a conductive contact.

A typical contact system may contain several layers:

Base Contact Alloy

↓

Underplating

↓

Surface Plating

The base alloy provides the structural and electrical properties of the terminal.

The underplating can provide a barrier between the base material and surface plating while supporting adhesion and durability.

The surface plating is the layer that directly interacts with the mating interface and environment.

The performance of the complete system depends on how these layers work together.


3.Common Connector Plating Materials

Three commonly used plating materials are:

PlatingTypical CharacteristicsCommon Considerations
TinCost-effective, good conductivity, widely usedOxidation and wear must be considered
GoldExcellent corrosion resistance and stable contact interfaceHigher material cost
SilverHigh electrical conductivityEnvironmental and application conditions must be evaluated

The correct choice depends on the electrical, mechanical and environmental requirements rather than simply choosing the highest-value material.


4.Tin Plating

Tin is widely used for connector terminals because it provides a practical balance between performance and cost.

It is commonly considered for applications where:

  • Cost efficiency is important
  • Current levels are moderate to high
  • The connector operates in controlled environments
  • Mating frequency is limited or appropriately managed

Tin-plated contacts are often used in automotive and industrial electrical systems.

However, engineers should consider surface condition, contact force, oxidation behavior and mechanical wear.

For applications involving frequent mating or demanding environmental exposure, the complete plating design should be evaluated rather than looking only at the presence of tin plating.


5.Gold Plating

Gold is widely recognized for its excellent resistance to corrosion and stable surface characteristics.

It is particularly valuable where reliable low-level electrical contact is important.

Typical applications may include:

  • Signal connectors
  • Control electronics
  • Communication equipment
  • Industrial sensors
  • Medical electronics
  • High-reliability electronic systems

Gold plating can help maintain a stable contact interface under challenging environmental conditions.

However, gold plating is not automatically the best choice for every connector.

Engineers should also consider:

  • Plating thickness
  • Underplating
  • Contact force
  • Mating cycles
  • Base material
  • Operating environment
  • Cost target

A thin gold layer and a properly engineered gold-plating system are not necessarily equivalent.


6.Silver Plating

Silver has very high electrical conductivity and can be considered for applications where electrical performance and current handling are important.

However, silver surfaces can be affected by environmental exposure and surface contamination.

Therefore, silver plating should be evaluated according to:

  • Operating temperature
  • Current level
  • Environmental conditions
  • Contact geometry
  • Exposure to contaminants
  • Required service life

The key engineering principle is the same:

Select the plating system according to the actual operating environment.


7.How Plating Affects Contact Resistance

Contact resistance is one of the most important electrical characteristics of a connector.

Even when the bulk resistance of the terminal is low, the actual mating interface can introduce additional resistance.

A reliable plating system helps maintain a stable contact interface.

If the surface deteriorates through oxidation, corrosion or wear, contact resistance can increase.

Higher contact resistance can contribute to:

Electrical loss → Heat generation → Further degradation

This becomes especially important in higher-current applications.

For this reason, engineers should evaluate plating together with:

  • Contact force
  • Contact geometry
  • Current level
  • Terminal material
  • Surface condition
  • Temperature

Plating cannot compensate for an incorrectly designed contact system.


8.Why Plating Thickness Matters

One of the most common mistakes is evaluating plating only by material type.

For example:

Gold plated

does not fully describe the performance of a gold-plated contact.

Engineers should also consider the plating thickness and overall plating structure.

Plating thickness can influence:

  • Corrosion protection
  • Wear resistance
  • Surface durability
  • Mating lifetime
  • Barrier performance
  • Long-term contact stability

However, thicker plating is not automatically better.

Increasing plating thickness may increase cost without providing meaningful additional performance for a specific application.

The correct approach is to establish the required performance first and then define an appropriate plating system.


9.Gold Plating Thickness and Mating Cycles

For connectors with frequent mating and unmating, mechanical wear becomes a major consideration.

Every mating cycle can generate mechanical interaction between the contact surfaces.

Over time, repeated movement can gradually wear the plating.

Therefore, engineers should evaluate:

Plating Thickness + Contact Geometry + Contact Force + Mating Cycles

rather than considering plating thickness independently.

For example, a connector designed for frequent maintenance may require a different surface treatment strategy from a connector that is assembled once and expected to remain connected throughout its service life.


10.The Role of Underplating

Underplating is often overlooked because it is not visible from the finished connector surface.

However, it can play an important role in the plating system.

A properly selected underlayer can help:

  • Improve the barrier between base metal and surface plating
  • Support plating adhesion
  • Reduce migration between material layers
  • Improve long-term plating stability

The exact layer structure depends on the contact material, plating technology and application requirements.

Therefore, plating should be evaluated as a layered system, not as a single metallic coating.


11.Connector Plating and Corrosion Resistance

Corrosion is one of the major causes of connector degradation.

Environmental factors can include:

  • Moisture
  • Salt
  • Humidity
  • Industrial chemicals
  • Pollutants
  • Condensation

Corrosion at the contact interface can change the surface condition and increase electrical resistance.

For connectors used in harsh environments, engineers should consider the combined effect of:

Plating + Sealing + Housing + Environmental Protection

This is particularly important for automotive and industrial connectors installed outside protected electronic enclosures.


12.Connector Plating and Wear

Corrosion is not the only threat to plating.

Mechanical wear can also remove or damage the surface layer.

Common sources include:

  • Repeated mating
  • Vibration
  • Sliding contact movement
  • Cable movement
  • Terminal deformation
  • Assembly processes

A connector designed for high mating-cycle performance needs a plating system that can withstand the expected mechanical interaction.

This means plating selection should be connected to the connector’s mechanical design.


13.Connector Plating for High-Current Applications

High-current connectors introduce additional considerations.

As current increases, even a small increase in contact resistance can become more significant because electrical power dissipation at the contact interface increases with resistance.

Therefore, high-current connector design should consider:

  • Contact material
  • Contact cross-section
  • Contact force
  • Contact area
  • Plating
  • Thermal management
  • Terminal connection quality

For energy storage, power distribution and industrial equipment, plating should be evaluated together with the complete current-carrying system.

Plating alone does not determine current capacity.


14.Connector Plating for Signal Applications

Signal connectors have a different set of priorities.

Very low-level electrical signals can be sensitive to surface contamination and contact instability.

For these applications, engineers may prioritize:

  • Stable contact resistance
  • Corrosion resistance
  • Surface cleanliness
  • Low-level signal reliability
  • Mating-cycle performance

Gold plating is often considered in applications where maintaining a stable contact interface is particularly important.

However, the final selection still depends on connector design and operating conditions.


15.Automotive Connector Plating

Automotive connectors can experience challenging conditions, including:

  • Vibration
  • Temperature cycling
  • Humidity
  • Contamination
  • Repeated electrical loading
  • Long service periods

Therefore, plating selection must be integrated into the overall connector design.

Engineers should evaluate:

  • Terminal Material
  • Plating System
  • Contact Force
  • Sealing
  • Mechanical Retention
  • Environmental Requirements

For automotive connector production, consistent plating quality is also important because variations in surface condition can affect electrical and mechanical performance.


16.Industrial Connector Plating

Industrial connectors may be exposed to:

  • Dust
  • Oil
  • Chemicals
  • Humidity
  • Vibration
  • Frequent maintenance

Applications such as automation equipment, robotics, sensors and control cabinets may also require repeated connector service.

Therefore, plating selection should consider both environmental resistance and mechanical wear.

A connector that performs well in a clean indoor environment may require a different plating strategy when used in a factory environment with vibration, contamination or frequent maintenance.


17.Connector Plating Selection Matrix

Application RequirementKey Plating Consideration
Low-cost electrical connectionCost-effective plating system
High corrosion resistanceStable corrosion-resistant surface
Frequent matingWear resistance + plating thickness
Low-level signalsStable contact interface
High currentContact resistance + thermal performance
High humidityCorrosion resistance + sealing
Industrial environmentChemical and contamination resistance
Automotive applicationEnvironmental + mechanical durability
Long service lifeComplete plating system validation

The table should be used as an engineering starting point rather than a universal material-selection rule.


18.Common Connector Plating Selection Mistakes

Mistake 1: Choosing plating only by material

Selecting “gold” or “tin” without considering thickness, base material and application requirements can lead to an incomplete specification.

Mistake 2: Assuming thicker is always better

More plating may increase cost without providing proportional performance benefits.

Mistake 3: Ignoring mating cycles

A plating system suitable for one-time assembly may not be suitable for repeated maintenance.

Mistake 4: Ignoring the environment

Humidity, salt, chemicals and contamination can significantly influence surface durability.

Mistake 5: Evaluating plating separately from contact design

Contact force, geometry and plating work together to determine interface performance.

Mistake 6: Focusing only on initial electrical performance

A connector may pass initial electrical testing but still experience degradation during long-term environmental or mechanical exposure.


19.How to Define a Connector Plating Specification

A practical engineering specification should include more than the plating material.

Consider defining:

1.Base Contact Material

Examples include brass, phosphor bronze and other copper alloys.

2.Underplating

Define the required layer structure according to the manufacturing process and application.

3.Surface Plating

Specify tin, gold, silver or another suitable finish.

4.Plating Thickness

Define the required thickness according to performance requirements.

5.Mating Requirements

Specify expected mating and unmating cycles.

6.Environmental Requirements

Consider temperature, humidity, corrosion, chemicals and contamination.

7.Electrical Requirements

Evaluate current, voltage, contact resistance and signal characteristics.

8.Validation Requirements

Define the appropriate electrical, mechanical and environmental tests.

This creates a much stronger specification than simply stating:

“Gold plated connector.”


20.Connector Plating Quality Control

For mass production, plating quality needs to be controlled consistently.

Depending on the product and specification, manufacturers may monitor:

  • Plating thickness
  • Surface appearance
  • Adhesion
  • Contact resistance
  • Corrosion performance
  • Mechanical wear
  • Terminal dimensions
  • Base material consistency

Process control is particularly important because plating variation can affect the finished contact interface.

A robust quality system should connect:

Incoming Material → Stamping → Plating → Terminal Processing → Assembly → Electrical Testing → Final Inspection

This helps identify potential variation before products reach the customer.


21.How FPIC Supports Connector Plating and Reliability

For custom connector projects, plating should be considered during the engineering and DFM stages rather than added as a final specification.

FPIC can support connector development by evaluating the relationship between:

  • Contact material
  • Plating system
  • Terminal geometry
  • Contact force
  • Connector structure
  • Application environment
  • Manufacturing requirements
  • Electrical performance

For automotive connector applications, FPIC operates an IATF 16949 quality management system and applies controlled manufacturing and inspection processes to support consistent connector production.

The objective is not simply to provide a specific plating material, but to develop a plating and contact system that matches the customer’s actual operating requirements.


22.A Practical Connector Plating Selection Workflow

A useful engineering workflow is:

Step 1 — Define the Application

Automotive, industrial, robotics, energy storage, medical or electronics.

↓

Step 2 — Define the Environment

Temperature, humidity, corrosion, chemicals and contamination.

↓

Step 3 — Define Electrical Requirements

Current, voltage, contact resistance and signal requirements.

↓

Step 4 — Define Mechanical Requirements

Mating cycles, vibration, insertion force and contact movement.

↓

Step 5 — Select the Contact Material

Choose an appropriate conductive alloy based on mechanical and electrical requirements.

↓

Step 6 — Select the Plating System

Evaluate surface plating, underplating and thickness.

↓

Step 7 — Validate

Conduct appropriate electrical, mechanical and environmental testing.

This approach reduces the risk of selecting plating based solely on material name or initial cost.


23.Final Thoughts

Connector plating is a small physical layer with a major impact on long-term connector performance.

The right plating system can help maintain:

  • Stable contact resistance
  • Corrosion resistance
  • Mechanical durability
  • Mating performance
  • Electrical reliability
  • Long service life

But plating should never be evaluated independently.

The final performance depends on the complete system:

Contact Material + Plating + Thickness + Contact Force + Geometry + Sealing + Environment

For engineers designing reliable connectors, the key question is not:

“Which plating is best?”

It is:

“Which plating system provides the required performance for this application throughout the expected service life?”


FAQ

What is connector plating?

Connector plating is a metallic surface coating applied to electrical contacts to improve properties such as corrosion resistance, contact stability and wear performance.

Is gold plating better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact characteristics, while tin can offer a practical balance between performance and cost. The correct choice depends on the application.

Why does connector plating thickness matter?

Plating thickness can affect corrosion protection, wear resistance and service life. However, thicker plating is not automatically better because cost and application requirements must also be considered.

Does plating affect connector contact resistance?

Yes. Surface condition and plating can influence the stability of the contact interface and therefore affect contact resistance over the connector’s service life.

What plating is suitable for high-current connectors?

There is no single plating material that is universally best for high-current connectors. Engineers should evaluate plating together with contact material, geometry, contact force, resistance and thermal requirements.

How does plating affect mating cycles?

Repeated mating creates mechanical wear at the contact interface. The plating material, thickness, contact geometry and force all influence how well the surface withstands repeated cycles.

Should connector plating be specified during DFM?

Yes. Plating should be considered during connector design and DFM because it affects material selection, manufacturing processes, cost and long-term reliability.


Need Help Selecting the Right Connector Plating?

Choosing the right plating system requires more than selecting gold, tin or silver.

FPIC can help evaluate contact material, plating, terminal design, environmental requirements and manufacturing considerations for custom connector applications.

Talk to our engineering team about your connector requirements.


Resources

  • IPC/WHMA-A-620 — Requirements and Acceptance for Cable and Wire Harness Assemblies
  • SAE — Automotive engineering standards and specifications
  • IEC — International electrotechnical standards
  • IATF 16949 — Automotive quality management system requirements
Connector Material Selection Guide for Engineers

A connector may look simple from the outside, but its reliability depends heavily on the materials used throughout the assembly.

A typical connector includes several material systems:

Housing + Contacts + Plating + Seals + Locks + Secondary Components

Each material has a different function.

The housing must provide insulation and mechanical protection. The contact system must maintain stable electrical performance. Plating must protect the contact interface from corrosion and wear. Seals must maintain environmental protection without compromising assembly performance.

Selecting materials based only on cost or a single specification can create reliability problems later in the product lifecycle.

For demanding applications such as automotive electronics, industrial automation, robotics, medical equipment, and energy systems, material selection should therefore be treated as a system-level engineering decision.

The objective is to balance:

Electrical Performance + Mechanical Strength + Thermal Stability + Environmental Resistance + Manufacturability + Cost

Connector Material Selection Guide for Engineers


Why Connector Material Selection Matters

Connector materials directly influence how a connector performs throughout its service life.

Poor material selection can contribute to:

  • Contact resistance increase
  • Corrosion
  • Terminal deformation
  • Housing cracking
  • Seal degradation
  • Insulation failure
  • Poor mating performance
  • Reduced vibration resistance
  • Premature connector failure

For example, a housing material may meet the required temperature rating but lack sufficient mechanical strength.

Likewise, a contact alloy may provide excellent conductivity but require a different plating system to achieve the required corrosion and wear resistance.

This is why engineers should evaluate the complete material combination, rather than selecting each material independently.


1.Connector Housing Material Selection

The connector housing provides:

  • Electrical insulation
  • Mechanical support
  • Terminal positioning
  • Mating alignment
  • Environmental protection
  • Structural protection

The housing material therefore needs to withstand the expected electrical, thermal, mechanical, and environmental conditions.

Common connector housing materials include:

  • PA / Nylon
  • PBT
  • PPS
  • LCP
  • PEEK
  • PC and other engineering polymers

The best material depends on the application rather than simply its nominal strength.


2.PA / Nylon

Polyamide materials are widely used in connector housings because they can provide a useful combination of:

  • Mechanical strength
  • Impact resistance
  • Processability
  • Cost efficiency

However, different grades can behave differently in terms of:

  • Water absorption
  • Dimensional stability
  • Temperature resistance
  • Chemical resistance

For applications involving humidity or significant temperature variation, engineers should evaluate the specific PA grade rather than treating all nylon materials as equivalent.


3.PBT

Polybutylene terephthalate, or PBT, is commonly used for electrical and automotive connector housings.

Potential advantages include:

  • Good dimensional stability
  • Electrical insulation
  • Chemical resistance
  • Suitable molding characteristics
  • Good temperature performance for many applications

PBT can be attractive where dimensional precision and electrical insulation are important.


4.PPS for Higher-Temperature Applications

Polyphenylene sulfide (PPS) is an engineering polymer commonly considered for demanding thermal and chemical environments.

Potential characteristics include:

  • High temperature resistance
  • Low moisture absorption
  • Good dimensional stability
  • Chemical resistance
  • Electrical insulation

PPS can be useful when the connector must maintain dimensional stability under elevated temperatures.

However, material selection should always consider the actual temperature profile, not simply the maximum advertised material temperature.


5.LCP for Fine-Pitch Connectors

Liquid crystal polymer (LCP) is often considered for compact and fine-pitch connector designs.

Its characteristics can support applications requiring:

  • Thin-wall molding
  • Dimensional precision
  • Fine-pitch structures
  • Good thermal performance
  • Low moisture absorption

As connector dimensions decrease, housing dimensional stability becomes increasingly important.

A material suitable for a large connector may not necessarily be the best choice for a miniature high-density connector.


6.PEEK for Highly Demanding Applications

PEEK is a high-performance engineering polymer used in applications requiring demanding combinations of:

  • Temperature resistance
  • Chemical resistance
  • Mechanical strength
  • Dimensional stability

Its higher material cost means it is generally considered when standard engineering plastics cannot adequately meet the application requirements.

Material selection should therefore consider total system requirements, rather than simply selecting the highest-performance material available.


7.Flame Retardancy

For many electronic and industrial applications, connector housing materials may need to meet specific flammability requirements.

Engineers should consider:

  • Applicable safety requirements
  • Electrical application
  • Equipment enclosure
  • Operating voltage
  • Installation environment

A flame-retardant grade can affect other material characteristics such as:

  • Mechanical strength
  • Flow behavior
  • Moldability
  • Cost

Therefore, flame retardancy should be evaluated together with the overall material specification.


8.Connector Contact Material Selection

The contact system is responsible for maintaining the electrical interface.

Common contact alloys include:

  • Copper
  • Brass
  • Phosphor bronze
  • Copper alloys
  • Beryllium copper for specialized applications

The selected material affects:

  • Electrical conductivity
  • Spring properties
  • Contact force
  • Fatigue resistance
  • Thermal behavior
  • Corrosion resistance
  • Manufacturability

A connector contact must provide both electrical performance and mechanical reliability.


9.Brass Contacts

Brass is widely used for connector terminals because it provides a practical balance of:

  • Conductivity
  • Strength
  • Formability
  • Cost

It can be suitable for many general-purpose connector applications.

However, for high-flex or high-contact-force applications, another copper alloy may provide more suitable mechanical properties.


10.Phosphor Bronze Contacts

Phosphor bronze can provide good spring characteristics and fatigue resistance.

It is often considered when the contact must maintain stable mechanical behavior during repeated mating or long-term operation.

Potential applications include:

  • Signal connectors
  • Control connectors
  • Industrial equipment
  • Repeated mating interfaces

The final choice depends on the required contact force, conductivity, mating cycles, and environmental conditions.


11.Beryllium Copper

Beryllium copper can provide excellent spring properties and good electrical conductivity.

It may be considered for applications requiring:

  • High contact force
  • Miniaturized contacts
  • Repeated mating
  • Strong elastic recovery

Because material cost and processing considerations can be higher, engineers should use it when its performance advantages justify the additional complexity.


12.Contact Plating Selection

Contact plating forms the actual surface interface between mating contacts.

Common plating materials include:

Tin

Tin is widely used for cost-sensitive applications and can provide practical performance for many power connections.

Gold

Gold plating provides excellent corrosion resistance and stable contact behavior.

It is particularly useful where:

  • Low-level signals are involved
  • Long-term contact stability is important
  • Corrosive environments are present
  • High mating-cycle performance is required

Silver

Silver has excellent electrical conductivity and can be considered for certain power and high-current applications.

However, its behavior under specific environmental conditions must be carefully evaluated.


13.Gold Plating Thickness Matters

Simply specifying “gold plated” is not enough.

Engineers should also consider:

  • Gold thickness
  • Plating area
  • Underplating
  • Contact force
  • Mating cycles
  • Operating environment

A thin decorative gold layer and an engineered contact plating system do not necessarily provide the same long-term performance.

For demanding applications, plating specifications should be clearly defined in the connector drawing or technical specification.


14.Underplating Matters Too

The plating system can include multiple layers.

For example:

Base Contact Alloy → Underplating → Gold Surface

The underplating can help provide:

  • Corrosion protection
  • Diffusion resistance
  • Better plating stability

The complete plating structure should therefore be evaluated rather than looking only at the visible surface material.


15.Connector Seal Material Selection

Seals become critical when connectors must resist:

  • Water
  • Dust
  • Oil
  • Chemicals
  • Temperature cycling

Common sealing materials include:

  • Silicone rubber
  • EPDM
  • Fluoroelastomer materials
  • Other application-specific elastomers

The correct seal depends heavily on the environment.


16.Silicone Seals

Silicone can provide good flexibility across a broad temperature range.

It is commonly considered where connectors must tolerate:

  • Temperature variation
  • Repeated assembly
  • Flexible sealing interfaces

However, chemical compatibility must still be evaluated for the actual application.


17.EPDM Seals

EPDM can provide good resistance to:

  • Water
  • Weathering
  • Ozone
  • Certain environmental conditions

It may be suitable for outdoor or automotive environments depending on the specific fluid and temperature exposure.


18.Chemical Compatibility Is Critical

A connector material may perform well in a laboratory but degrade when exposed to the actual application environment.

Potential contaminants include:

  • Automotive fluids
  • Lubricants
  • Cleaning agents
  • Coolants
  • Hydraulic fluids
  • Industrial chemicals

Material compatibility should therefore be validated against the actual chemicals and concentrations expected during the connector’s service life.


19.Temperature Selection Should Consider the Complete System

Connector temperature performance is not determined by housing material alone.

The complete system includes:

Current → Contact Resistance → Heat Generation → Housing → Surrounding Environment

Higher current can increase temperature at the contact interface.

This means the connector must be evaluated under realistic electrical loading.

Engineers should consider:

  • Ambient temperature
  • Current load
  • Number of loaded circuits
  • Contact resistance
  • Heat dissipation
  • Housing material
  • Installation conditions

20.Material Selection for High-Current Connectors

High-current connectors place greater demands on the contact system.

Important factors include:

  • Contact resistance
  • Conductivity
  • Contact force
  • Terminal cross-section
  • Plating
  • Temperature rise
  • Thermal dissipation

Simply choosing a highly conductive alloy does not automatically create a reliable high-current connector.

The complete contact geometry and mechanical interface also matter.


21.Material Selection for Fine-Pitch Connectors

Miniaturized connectors create different material challenges.

As pitch decreases:

  • Housing walls become thinner
  • Terminal spacing decreases
  • Dimensional tolerances become tighter
  • Mating alignment becomes more sensitive

Materials with good dimensional stability and molding precision may therefore become increasingly important.

This is one reason material selection should be performed together with connector geometry and manufacturing process development.


22.Material Selection for Automotive Connectors

Automotive connectors may encounter:

  • Temperature cycling
  • Vibration
  • Humidity
  • Dust
  • Oil
  • Chemical exposure
  • Long service life requirements

Material selection should therefore consider the complete automotive environment.

For automotive connector products, FPIC applies IATF 16949 quality management requirements and supports production processes designed for demanding automotive applications.


23.Material Selection for Industrial Connectors

Industrial connectors may be exposed to:

  • Continuous vibration
  • Machinery movement
  • Oil
  • Dust
  • Chemicals
  • Outdoor environments

Industrial connector material selection should consider not only IP protection but also mechanical durability and chemical compatibility.

For example, an industrial connector used near motors may require different mechanical characteristics from one installed inside a protected control cabinet.


24.Material Selection for Medical Connectors

Medical applications may place additional requirements on:

  • Biocompatibility
  • Cleaning resistance
  • Chemical exposure
  • Sterilization
  • Reliability
  • Traceability

The material selection process should therefore begin with the applicable medical device requirements and cleaning or sterilization process.


25.Manufacturing Must Be Considered

A material with excellent laboratory performance may still be difficult to manufacture.

Engineers should evaluate:

  • Injection molding behavior
  • Shrinkage
  • Warpage
  • Flow characteristics
  • Terminal stamping
  • Plating process
  • Crimp compatibility
  • Assembly tolerances

Material selection should support not only prototype performance but also stable mass production.


Connector Material Selection Matrix

ComponentCommon MaterialsMain Selection Factors
HousingPA, PBT, PPS, LCP, PEEKTemperature, insulation, strength, chemicals
ContactBrass, phosphor bronze, copper alloysConductivity, spring force, fatigue
PlatingTin, gold, silverCorrosion, current, mating cycles
SealSilicone, EPDM, fluoroelastomerTemperature, water, chemicals
Locking PartsEngineering plastics / metalsRetention, vibration, durability
ShieldingCopper alloys / metal shellsEMC, grounding, mechanical strength

Common Connector Material Selection Mistakes

MistakePotential Consequence
Selecting housing only by temperature ratingMechanical or dimensional problems
Treating all nylon grades as identicalUnexpected moisture or thermal behavior
Selecting contact material only by conductivityInsufficient spring performance
Specifying gold plating without thicknessUnclear contact durability
Ignoring underplatingCorrosion or diffusion concerns
Selecting seals without chemical testingSwelling or degradation
Ignoring current-related heat generationExcessive temperature rise
Choosing materials without DFM reviewMolding or assembly problems
Selecting the highest-performance material automaticallyUnnecessary cost
Evaluating materials independentlySystem-level compatibility problems

A Practical Connector Material Selection Workflow

Step 1: Define the Environment

Identify:

  • Temperature
  • Humidity
  • Water
  • Dust
  • Chemicals
  • Vibration
  • UV exposure

Step 2: Define Electrical Requirements

Identify:

  • Current
  • Voltage
  • Signal type
  • Contact resistance
  • Mating cycles

Step 3: Define Mechanical Requirements

Consider:

  • Contact force
  • Mating force
  • Retention
  • Shock
  • Vibration
  • Connector size

Step 4: Select Housing Material

Match:

Temperature + Insulation + Mechanical + Environmental Requirements

Step 5: Select Contact Alloy

Match:

Conductivity + Spring Properties + Fatigue + Formability

Step 6: Select Plating

Match:

Corrosion + Wear + Current + Signal + Mating Cycles

Step 7: Select Seal Material

Match:

Temperature + Fluids + Water + Chemical Exposure

Step 8: Validate the Complete Connector

Evaluate:

  • Electrical performance
  • Mechanical performance
  • Temperature rise
  • Environmental resistance
  • Mating cycles
  • Dimensional stability
  • Production consistency

Material Selection Should Follow Application Requirements

A common mistake is starting with a preferred material and trying to make it fit the application.

A better approach is:

Application → Requirements → Material Properties → Component Design → Validation

For example, if a connector operates in a high-temperature environment, engineers should not simply select the highest-temperature housing material.

They should first ask:

  • What is the actual temperature profile?
  • How much current flows through the contacts?
  • How long is the exposure?
  • Is vibration present?
  • Are chemicals present?
  • How many mating cycles are required?

The answers determine the appropriate material combination.


Why Material Compatibility Matters

A connector is a multi-material system.

Consider:

Housing + Contact Alloy + Plating + Seal + Cable + Mating Connector

Changing one material can influence another.

For example:

  • Housing shrinkage can affect terminal position.
  • Contact force can affect plating wear.
  • Seal hardness can affect mating force.
  • Temperature can affect housing dimensions.
  • Chemical exposure can affect both housing and seals.

This is why reliable connector development requires cross-functional material engineering.


How FPIC Supports Connector Material Selection

FPIC provides customized connector development and manufacturing solutions covering:

  • Connector housing materials
  • Contact materials
  • Contact plating
  • Sealing systems
  • Terminal stamping
  • Connector assembly
  • Electrical testing
  • Dimensional inspection
  • Reliability validation

FPIC’s automotive connector products are manufactured under IATF 16949 quality management requirements.

For automotive connector production, FPIC also supports mass-production cleanliness requirements aligned with VDA 19.1 / ISO 16232 practices.

Material and component selection can be evaluated together with connector geometry, tooling, assembly, and testing requirements.

This system-level approach helps OEM customers develop connectors that balance performance, reliability, manufacturability, and cost.


Final Thoughts

Connector material selection is not simply a question of choosing the strongest plastic, most conductive metal, or thickest plating.

The correct material combination depends on the complete application.

Engineers should evaluate:

Housing + Contact + Plating + Seal + Environment + Electrical Load + Mechanical Requirements

The best connector material is the one that provides the required performance throughout the expected service life while remaining manufacturable and commercially practical.

A structured selection process can help reduce:

  • Corrosion risk
  • Thermal problems
  • Mechanical failure
  • Seal degradation
  • Manufacturing variation
  • Lifecycle cost

Ultimately, successful connector design begins with understanding the application and selecting materials that work together as a complete system.


FAQ

What is the most important factor in connector material selection?

There is no single factor. Temperature, current, environment, mechanical loading, mating cycles, dimensional requirements, and manufacturing conditions should all be considered together.

Which material is commonly used for connector housings?

PA and PBT are widely used for many connector applications, while PPS, LCP, PEEK, and other engineering polymers may be considered for more demanding thermal, dimensional, or chemical requirements.

What materials are commonly used for connector contacts?

Brass, phosphor bronze, and other copper alloys are commonly used. The selection depends on conductivity, spring properties, contact force, fatigue resistance, and application requirements.

Is gold plating always better than tin plating?

Not necessarily. Gold can provide excellent corrosion resistance and stable contact performance, but it can increase cost. Tin may be suitable for many power applications. The correct plating depends on current, signal type, environment, and mating requirements.

How should connector seal material be selected?

Seal material should be evaluated against the actual temperature range, water exposure, chemicals, oils, cleaning agents, and expected service life.

Does connector housing material affect electrical reliability?

Yes. Housing material affects insulation, terminal positioning, dimensional stability, heat resistance, and mechanical protection, all of which can influence connector reliability.

Why should material selection consider manufacturing?

A material may perform well technically but create molding, stamping, plating, assembly, or cost problems at production volume. DFM should therefore be included early in the material selection process.


Need Help Selecting Materials for Your Connector?

FPIC supports OEM and engineering teams with connector design and manufacturing from material selection and tooling through assembly, testing, and mass production.

Whether you need a compact fine-pitch connector, high-current connector, automotive connector, industrial connector, or customized interconnection solution, our engineering team can evaluate the complete material and application requirements.

Contact FPIC to discuss your connector development project.


Resources

  1. IEC
    https://www.iec.ch/
    International standards and technical resources covering electrical and electronic technologies.
  2. SAE International
    https://www.sae.org/
    Automotive engineering standards and technical resources.
  3. IPC
    https://www.ipc.org/
    Industry standards and resources for electronic interconnection and manufacturing.
  4. IATF Global Oversight
    https://www.iatfglobaloversight.org/
    Resources related to IATF 16949 automotive quality management requirements.
Connector Design From Contact System to Final Assembly

A connector may look like a simple component, but its performance depends on the interaction of multiple engineering elements.

A reliable connector requires careful design of:

  • Contact system
  • Housing structure
  • Locking mechanism
  • Sealing system
  • Material selection
  • Manufacturing process
  • Final assembly and testing

A mistake in any stage can affect:

  • Electrical performance
  • Mechanical reliability
  • Environmental protection
  • Service life

For engineers developing industrial, automotive, robotics, energy storage, and automation systems, connector design should be considered as a complete engineering process—not just a component selection task.

This guide explains the key stages of connector design, from the internal contact system to final production validation.

Connector Design From Contact System to Final Assembly


Why Connector Design Requires System-Level Thinking

A connector performs three primary functions:

Electrical Connection

Providing stable current or signal transmission.

Important factors:

Contact resistance

Current capacity

Signal integrity

Plating performance

Mechanical Connection

Maintaining a secure connection under real-world conditions.

Important factors:

Mating force

Locking structure

Vibration resistance

Mating cycles

Environmental Protection

Protecting internal components from harsh environments.

Important factors:

Waterproof sealing

Dust protection

Temperature resistance

Chemical exposure

A successful connector design balances all three requirements.


1.Contact System Design: The Core of Connector Performance

The contact system is the electrical heart of a connector.

Its design directly affects:

  • Conductivity
  • Heat generation
  • Reliability
  • Service life

Contact Geometry Design

Contact geometry determines how terminals connect and maintain contact force.

Key considerations include:

✔ Contact area

✔ Spring structure

✔ Contact pressure

✔ Current path design

A properly designed contact system provides:

Stable electrical connection

Low resistance

Long-term performance


Contact Material Selection

Common contact materials include:

Copper Alloys

Advantages:

✔ Good conductivity

✔ Balanced strength

✔ Cost efficiency

Phosphor Bronze

Advantages:

✔ Good spring performance

✔ Excellent fatigue resistance

Beryllium Copper

Advantages:

✔ High elasticity

✔ Excellent contact force retention

Used for:

  • High-cycle connectors
  • Precision applications

Contact Plating Selection

Surface plating affects:

  • Corrosion resistance
  • Contact stability
  • Mating life

Common options include:

Gold Plating

Advantages:

✔ Excellent corrosion resistance

✔ Reliable low contact resistance

Suitable for:

  • Signal connectors
  • Medical equipment
  • High-cycle applications

Tin Plating

Advantages:

✔ Cost-effective

✔ Suitable for many power applications

The correct plating depends on:

  • Current level
  • Environment
  • Required mating cycles

2.Housing Design: Mechanical Protection and Alignment

The connector housing protects internal contacts and ensures proper mating.

A good housing design must provide:

✔ Mechanical strength

✔ Accurate terminal positioning

✔ Electrical insulation

✔ Assembly efficiency


Housing Material Selection

Common materials include:

PA (Polyamide)

Used for:

  • Industrial connectors
  • General applications

Benefits:

  • Good strength
  • Cost efficiency

PBT

Benefits:

  • Dimensional stability
  • Low moisture absorption

PPS

Benefits:

  • High temperature resistance
  • Chemical resistance

Material selection depends on:

  • Operating temperature
  • Mechanical requirements
  • Environmental conditions

Terminal Positioning and Polarization

Connector housings should prevent incorrect assembly.

Important design features:

  • Keying structures
  • Polarization features
  • Secondary locks

These features help prevent:

❌ Wrong mating

❌ Terminal back-out

❌ Assembly mistakes


3.Locking Mechanism Design

A reliable locking system prevents accidental disconnection.

Common locking methods include:


Threaded Locking

Advantages:

✔ High vibration resistance

✔ Strong mechanical retention

Applications:

  • Industrial equipment
  • Outdoor systems

Push-Pull Locking

Advantages:

✔ Fast connection

✔ Easy operation

✔ High mating efficiency

Applications:

  • Medical
  • Automation
  • Test equipment

Snap Locking

Advantages:

✔ Simple operation

✔ Cost-effective

Applications:

  • General electronic applications

4.Sealing and Environmental Protection

For harsh environments, sealing design is critical.

Connector sealing protects against:

  • Water
  • Dust
  • Oil
  • Humidity

Common sealing components include:

  • O-rings
  • Gaskets
  • Rubber seals

IP Protection Considerations

Depending on the application, connectors may require:

  • IP67
  • IP68
  • IP69K

Higher protection levels require careful control of:

  • Seal compression
  • Housing interface
  • Material compatibility

5.Connector Assembly Design

Connector assembly affects both quality and manufacturing efficiency.

A production-ready design should consider:


Terminal Insertion

Important factors:

✔ Insertion force

✔ Terminal retention

✔ Position accuracy


Secondary Locking System

Secondary locks improve:

  • Terminal retention
  • Assembly reliability
  • Safety

Assembly Error Prevention

Good designs include:

  • Visual identification
  • Mechanical keying
  • Assembly guidance

These features improve production consistency.


6.Connector Validation and Testing

Before mass production, connectors require validation.

Common tests include:


Electrical Testing

Including:

  • Contact resistance
  • Insulation resistance
  • Hi-Pot testing

Mechanical Testing

Including:

  • Insertion force
  • Extraction force
  • Mating cycles
  • Vibration testing

Environmental Testing

Including:

  • Temperature cycling
  • Humidity testing
  • Salt spray testing
  • Water ingress testing

Testing ensures the connector performs under real application conditions.


7.Connector Design for Mass Production

A successful connector design must also consider manufacturing.

Key DFM considerations include:

Injection Molding

Evaluate:

  • Wall thickness
  • Draft angle
  • Mold complexity

Terminal Stamping

Evaluate:

  • Material utilization
  • Contact geometry
  • Production consistency

Assembly Automation

Evaluate:

  • Assembly direction
  • Process repeatability
  • Inspection requirements

Good connector design reduces production risks.


How FPIC Approaches Connector Design

FPIC provides customized connector solutions from engineering design through mass production.

Our connector development process considers:

  • Contact system design
  • Housing structure
  • Material selection
  • Manufacturing feasibility
  • Assembly optimization
  • Reliability testing

By combining engineering experience with manufacturing capability, FPIC helps customers develop connectors that meet demanding industrial requirements.


Final Thoughts

Connector design is a system engineering process.

A reliable connector requires the right balance between:

  • Contact performance
  • Mechanical structure
  • Environmental protection
  • Manufacturing efficiency

From the first contact design to final assembly validation, every detail influences long-term reliability.

For OEM engineers, selecting the right connector partner means choosing a team that understands both product performance and manufacturing reality.

A high-quality connector is not simply assembled—it is engineered.


FAQ

What are the main parts of a connector?

The main parts include contacts, housing, locking mechanism, sealing components, and assembly features.

Why is contact design important in connectors?

The contact system determines electrical performance, contact resistance, current capability, and mating reliability.

What factors affect connector lifetime?

Key factors include materials, contact force, mating cycles, environment, vibration, and manufacturing quality.

What tests are required for connector validation?

Common tests include electrical testing, mechanical testing, environmental testing, and durability testing.

Why should connector design consider manufacturing early?

Early manufacturing consideration improves production efficiency, reduces defects, and controls cost.


Need a Custom Connector Solution?

FPIC develops customized connector solutions for industrial automation, robotics, energy storage, automotive, and other demanding applications.

From contact design and material selection to tooling, assembly, and testing, FPIC supports customers from concept development to mass production.

Contact FPIC today to discuss your connector project.


Resources

  1. IEC 60512 – Connectors for Electronic Equipment – Tests and Measurements
    https://www.iec.ch/
    Connector testing methods covering electrical, mechanical, and environmental performance.
  2. IPC/WHMA-A-620 – Requirements and Acceptance for Cable and Wire Harness Assemblies
    https://www.ipc.org/
    Industry requirements for cable assembly quality and workmanship.
  3. ISO 16750 – Road Vehicles Environmental Conditions and Testing
    https://www.iso.org/
    Environmental testing guidance for automotive electrical components.
  4. IATF 16949 Automotive Quality Management System
    https://www.iatfglobaloversight.org/
    Automotive quality management requirements for production consistency.
800V EV CONNECTOR Design Trade-Off Overview

The transition from 400V to 800V vehicle architectures is reshaping the design of high-voltage connector.

Automakers are adopting 800V systems to support:

  • faster charging
  • higher power density
  • improved drivetrain efficiency
  • reduced cable weight

However, increasing system voltage creates new engineering challenges.

Connector designers must balance two competing objectives:

  • minimizing size and weight
  • maintaining adequate electrical safety margins

This trade-off affects nearly every aspect of connector development, from insulation design to thermal performance and EMC behavior.

800V EV CONNECTOR Design Trade-Off Overview


Why 800V Systems Change Connector Design

At first glance, an 800V connector may appear similar to a 400V connector.

In reality, the higher operating voltage increases the importance of:

  • insulation coordination
  • creepage distance
  • clearance distance
  • dielectric performance
  • contamination resistance
  • transient voltage withstand capability

The design window becomes significantly smaller.


The Industry Push Toward Compact Packaging

Vehicle manufacturers constantly seek:

  • lighter vehicles
  • smaller power electronics
  • tighter battery packaging
  • reduced installation space

As a result, connectors are expected to deliver:

  • higher voltage
  • higher current
  • smaller size

These requirements often conflict with each other.


The Creepage and Clearance Challenge

One of the most significant design constraints is maintaining sufficient electrical spacing.

Higher voltages generally require:

  • larger clearance distances
  • longer creepage paths
  • improved insulation structures

However, increasing spacing also increases connector size.

Designers often use:

  • insulating ribs
  • internal barriers
  • recessed terminals
  • optimized conductor geometry

to maximize electrical separation within limited packaging volume.

Compact Design vs Electrical Safety Comparison


Safety Margin vs Minimum Compliance

Meeting a standard requirement is not always enough.

A connector may technically comply with a specified spacing requirement while having limited margin for:

  • manufacturing tolerances
  • contamination
  • aging
  • vibration
  • environmental exposure

Experienced engineers typically design beyond minimum values to improve robustness.


Thermal Performance Trade-Offs

Higher voltage systems often support higher power levels.

To reduce size, designers may attempt to:

  • reduce terminal dimensions
  • decrease connector footprint
  • increase current density

These changes can increase:

  • contact temperature
  • thermal stress
  • material aging

Thermal validation becomes increasingly important in compact 800V designs.


Shielding and EMC Constraints

Modern 800V systems contain:

  • traction inverters
  • onboard chargers
  • DC/DC converters
  • high-speed communication networks

Effective shielding often requires:

  • metal shells
  • conductive backshells
  • 360° shield termination

These features consume valuable packaging space.

Reducing connector size may compromise EMC performance if shielding design is not carefully optimized.


HVIL Integration Challenges

Many 800V connectors incorporate HVIL (High Voltage Interlock Loop) functionality.

Additional HVIL contacts require:

  • dedicated space
  • mechanical protection
  • routing paths
  • insulation separation

Compact packaging increases the complexity of integrating these safety functions.


Mechanical Durability Considerations

Smaller connectors are often more sensitive to:

  • tolerance variation
  • vibration
  • mating misalignment
  • terminal movement

Maintaining long-term durability while reducing size requires careful mechanical design.


Environmental Sealing Trade-Offs

800V connectors frequently require:

  • IP67 protection
  • IP68 protection
  • chemical resistance
  • pressure resistance

Adding robust sealing features increases:

  • connector volume
  • mating force
  • manufacturing complexity

Yet inadequate sealing can significantly reduce safety margins.


Material Selection Becomes More Important

Material choice directly influences:

  • dielectric strength
  • CTI performance
  • thermal stability
  • mechanical durability

Higher-performance materials may allow more compact designs but often increase cost.


Manufacturing Tolerance Considerations

A design that appears acceptable in CAD may become risky in production.

Engineers must account for:

  • molding variation
  • terminal positioning tolerance
  • assembly variation
  • wear over product life

Reduced safety margins leave less room for manufacturing variation.


Validation Requirements for 800V Connectors

Because design margins are tighter, validation becomes more critical.

Typical tests include:

  • HiPot testing
  • insulation resistance testing
  • thermal cycling
  • vibration testing
  • humidity exposure
  • salt spray
  • EMC validation
  • HVIL functional testing

Validation should simulate real operating conditions whenever possible.


Common Design Mistakes

Optimizing Only for Size

Electrical safety margins may become insufficient.

Ignoring Long-Term Aging

Material degradation can reduce insulation performance.

Underestimating EMC Requirements

Shielding limitations often appear late in development.

Relying Solely on Standard Minimums

Minimum compliance does not guarantee robustness.

Reducing Validation Scope

Aggressive packaging requires more testing, not less.


The Best Approach: Balanced Engineering

Successful 800V connector design is not about achieving the smallest possible package.

It is about balancing:

  • electrical safety
  • thermal performance
  • EMC performance
  • manufacturability
  • reliability
  • serviceability

The most reliable connectors typically incorporate appropriate engineering margin rather than pursuing extreme miniaturization.


How FPIC Supports 800V Connector Development

FPIC develops high-voltage connectors and cable assemblies for EV, ESS, and industrial electrification applications.

Our engineering support includes:

  • 800V connector architecture review
  • creepage and clearance optimization
  • HVIL integration
  • shielding design
  • thermal validation
  • prototype development
  • production manufacturing support

We help customers balance compact packaging with long-term reliability and safety.


Final Thoughts

The move to 800V architectures creates significant opportunities for vehicle performance and charging efficiency.

However, higher voltage leaves less room for design mistakes.

Engineers must carefully balance:

  • size
  • weight
  • insulation performance
  • thermal behavior
  • EMC requirements
  • durability

In high-voltage connector design, safety margin is not wasted space—it is often the foundation of long-term reliability.


FAQ

Why are 800V connectors more challenging than 400V connectors?

Higher voltage increases insulation and safety requirements while packaging space continues to shrink.

Can connector size always be reduced?

Not without affecting safety margin, thermal performance, or EMC behavior.

Why are creepage and clearance more critical in 800V systems?

Higher voltage increases the risk of arcing and surface tracking.

Does compact packaging affect EMC?

Yes. Reduced space can limit shielding effectiveness and grounding paths.

Should engineers design beyond minimum standard requirements?

In many applications, additional safety margin improves long-term reliability.


Developing an 800V EV or ESS Platform?

FPIC provides custom high-voltage connectors and cable assemblies designed for 800V architectures, combining compact packaging, robust insulation design, and validated reliability.

Contact us to discuss your high-voltage interconnect requirements.


Resources

  1. ISO 6469 – Electrically Propelled Vehicle Safety Requirements
    Safety requirements for high-voltage EV systems.
  2. IEC 60664-1 – Insulation Coordination for Low-Voltage Systems
    Fundamental guidance on creepage and clearance.
  3. LV214 / LV215 High-Voltage Automotive Connector Standards
    Automotive connector validation and design requirements.
  4. USCAR-2 Automotive Connector Performance Specification
    Connector reliability and environmental test requirements.
  5. TE Connectivity – High Voltage EV Connectivity Solutions
    Industry guidance on EV high-voltage interconnect design.
Square Pin Terminals vs. Automotive Rounded Pin Terminals

A square pin terminal works well in standard PCB headers and low-vibration electronics. An automotive rounded pin terminal is built for stronger guidance, better vibration resistance, improved self-cleaning contact, and higher long-term reliability. If the application is automotive or high-reliability industrial equipment, the rounded automotive design is usually the better choice.

The main difference is not just the shape. Standard square pin terminals prioritize easy insertion and low cost for general electronics, while automotive rounded pin terminals are designed for vibration resistance, guided mating, stable contact, and long service life in harsher environments. Their structure, stamping process, plating method, and performance targets are all different.

If you only look at the pin tip, the difference may seem small. In real applications, though, terminal geometry affects contact stability, corrosion resistance, plating consistency, insertion feel, and even failure risk over time. This article breaks down the differences step by step so engineers, sourcing teams, and product managers can make better design decisions.

Start With the Right Terminology

Before comparing the products, it is important to use the right language.

In this article:

  • Standard square pin terminal means the square or flat-edged metal pin commonly used in PCB pin headers.
  • Automotive rounded pin terminal means the rounded or bullet-shaped male terminal used in automotive low-voltage connector systems.

This distinction matters because industry-leading suppliers do not treat pin headers and terminals as the same category. Aptiv’s public connection systems catalog lists Connectors, Terminals, Seals, and Pin Headers as separate product groups, which confirms that “pin header” and “automotive terminal” should not be used interchangeably.

Why This Comparison Matters

Automotive connectors work in a very different environment from ordinary board-level connectors.

According to VDA, electrical and electronic components in vehicles must continuously adapt to stricter requirements around safety, reliability, environmental exposure, vibration, temperature, and chemical resistance. VDA also highlights that wiring systems and connector components are part of that evolving standardization work.

That is why a terminal for a vehicle cannot be chosen the same way as a terminal for a simple PCB header. Even if both parts are conductive metal pins, the design priorities are different:

  1. Consumer electronics focus more on cost, compactness, and ease of assembly
  2. Automotive systems focus more on durability, vibration stability, and long-term consistency
  3. Harsh environments require stronger protection against debris, contact instability, plating wear, and corrosion

FPIC’s internal technical comparison document makes the same point very clearly: a standard square pin terminal is meant for lower-stress electronic connections, while the automotive rounded pin terminal is designed for high-vibration, high-reliability service conditions.

Structural Differences

Square Pin Terminals vs. Automotive Rounded Pin Terminals

Standard Square Pin Terminals

A standard square pin terminal usually has:

  • Tip: Sharp/pyramidal, small flat surface, obvious edges
  • Root: 90° dead-angle
  • Design focus: Easy insertion, low cost, for consumer electronics (low vibration, few insertions)
  • Example applications: PCB headers, low-end electronic devices, DuPont-style wiring

This kind of structure is common in:

  • Board-to-board connections
  • Standard PCB headers
  • Consumer electronics
  • Simple control boards
  • Low-vibration devices

The main benefits are easy insertion, easy manufacturing, and lower cost. But the structure also has limitations. Sharp edges and dead corners can create areas where stress concentrates, and in demanding environments they are less forgiving.

Automotive Rounded Pin Terminals

An automotive rounded pin terminal usually has:

  • Tip: Rounded bullet-head / dome-shaped
  • Root: Smooth tapered transition, no dead corner
  • Pin body: Thicker, stronger
  • Core benefits: Guided insertion, vibration resistance, self-cleaning, short-circuit protection
  • Designed for automotive harsh conditions: ECU, BCM, lighting, window, seat control modules

This design offers several practical advantages:

  • Better insertion guidance
  • Reduced scraping at the mating interface
  • More stable contact behavior
  • Better vibration resistance
  • Lower risk of debris staying in sharp dead corners
  • Improved contact reliability over long service life

Structural Comparison Table

ItemStandard Square Pin TerminalAutomotive Rounded Pin Terminal
Tip shapeSharp / pyramidal / flat-edgedRounded / bullet-shaped / dome-like
Root transition90° style transition, dead-corner tendencySmooth tapered transition
Edge conditionObvious corners and flat facesRounded surface, fewer stress points
Contact styleFlat or edge-dominantArc-guided, more stable engagement
Main design goalEasy insertion, simple structure, lower costGuidance, vibration resistance, reliability
Typical environmentGeneral electronicsAutomotive low-voltage systems
Debris toleranceLowerBetter
Reliability expectationBasicHigh

Why Rounded Geometry Helps in Automotive Use

The rounded automotive design is not just about appearance. It changes how the terminal behaves during mating and in long-term service.

1. Better Guidance

A rounded tip helps the male terminal find its way into the mating contact more smoothly. This matters when connector tolerances, insertion angle variation, or assembly speed introduce small alignment changes.

2. Better Vibration Resistance

In vehicles, connectors see repeated vibration from engine systems, road conditions, opening and closing actions, and general operating movement. A more robust and better-guided terminal geometry helps maintain a stable contact relationship.

3. Better Self-Cleaning Behavior

When two contacts mate and unmate repeatedly, a rounded guided structure can help wipe the contact area more consistently. FPIC’s internal document specifically notes this self-cleaning advantage as one reason automotive rounded terminals better resist contamination-related issues.

4. Lower Short-Circuit Risk

The internal comparison also notes that the absence of obvious dead-angle geometry helps reduce the chance of debris buildup around the terminal root, which is one of the practical design benefits of the automotive rounded form.

Industry Background and Design Thinking

FPIC’s internal document cites historical automotive field-failure discussions as a turning point in how the industry views low-voltage terminal design. The document explains that older low-voltage connector approaches using more ordinary square-pin-like forms could create higher risk when vibration, thermal cycling, and debris were involved, which pushed the market toward more robust automotive-specific terminal geometry.

Even without repeating every historical claim, the design lesson is clear:

Automotive connectors are not just “stronger consumer connectors.” They are engineered differently because the environment is different.

That view also aligns with the broader work of VDA and USCAR, where connector systems and related specifications are continuously reviewed to meet the demands of safety, durability, and vehicle operating conditions.

Manufacturing Process Differences

The structure difference is only one part of the story. The manufacturing route is also very different.

How Standard Square Pin Terminals Are Made

  • Equipment: Multi-wheel forming machines
  • Process: Wire extrusion → straightening → forming → cutting
  • Output: Loose independent pins
  • Automation: Limited
  • Use case: Standard PCB headers

How Standard Square Pin Terminals Are Made

How Standard Square Pin Terminals Are Made

How Automotive Rounded Pin Terminals Are Made

  • Equipment: High-speed precision stamping, continuous progressive dies
  • Process: Brass strip → stamping → punching → bending → forming → cutting
  • Output: Continuous strip carrier for automated assembly
  • Automation: High compatibility, precise dimensions, supports reel-to-reel plating

How Automotive Rounded Pin Terminals Are Made

Manufacturing Comparison Table

ItemStandard Square Pin TerminalAutomotive Rounded Pin Terminal
Main equipmentMulti-wheel square pin forming machineHigh-speed precision stamping press
Input materialWire stockCopper alloy strip
Core processExtrusion/forming/cuttingProgressive stamping/forming
Finished formLoose pin / independent pinContinuous carrier strip
Automation compatibilityMediumHigh
Dimensional controlBasic to mediumHigher
Mass-production suitabilityGood for standard electronicsBetter for automotive-scale process control

Plating Process Differences

The plating route is one of the biggest technical differences, and it directly affects contact quality.

Standard Square Pin Terminal Plating

  • Barrel/batch plating
  • Less uniform coating; edges and tips prone to thin plating
  • Manual sorting required for automation

Automotive Rounded Pin Terminal Plating

  • Reel-to-reel continuous precision plating
  • Uniform thickness, strong adhesion
  • Fully compatible with automated assembly, injection molding, and SMT

Plating Comparison Table

ItemStandard Square Pin TerminalAutomotive Rounded Pin Terminal
Workpiece formLoose individual pinsContinuous strip terminal
Typical plating methodBarrel / bulk platingReel-to-reel precision plating
Thickness consistencyLowerHigher
Edge coverage consistencyLess stableBetter controlled
Adhesion behaviorMore variationMore stable
Automation supportLimitedExcellent

Performance Comparison

FPIC’s internal technical comparison gives a clear picture of why automotive rounded terminals are chosen for more demanding systems.

MetricSquare PinRounded Pin
Contact resistanceHigh batch variationLow, ≤±1mΩ
Mating cycles≤500>10,000
Vibration resistanceLowHigh, car-grade
Salt spray resistancePoor>10 years in automotive environment
Current carryingLocal heatingUniform, stable temperature rise
Temperature toleranceLimited-40°C to +125°C
High-frequency signalPoorLVDS compatible, stable signal

Industry Standards & Background

  1. Early Mercedes W210/W220 ECU/BCM PCB failures due to square pins → large recalls, safety issues
  2. USCAR / VDA / QC/T standards: automotive ≥2-pin low-voltage connectors must use rounded bullet-head terminals
  3. Safety, vibration, long-term reliability, and manufacturing precision are mandatory in automotive-grade terminals

Application Comparison

Best Uses for Standard Square Pin Terminals

A standard square pin terminal is usually a good fit for:

  • PCB headers
  • Consumer electronics
  • Low-vibration control boards
  • Cost-sensitive electronics
  • Standard signal connections

Best Uses for Automotive Rounded Pin Terminals

An automotive rounded pin terminal is usually the better fit for:

  • Automotive low-voltage systems
  • Control modules
  • Lighting systems
  • Window lift systems
  • Power seat systems
  • Multimedia systems
  • Industrial equipment with demanding vibration requirements
  • Long-life signal or low-voltage power transmission

FPIC Engineering Perspective

At FPIC, terminal selection is not treated as an isolated metal-part decision. It is part of the full connector-system design process.

A good connector terminal must be evaluated together with:

  • Housing design
  • Material selection
  • Plating specification
  • Contact force
  • Current path
  • Assembly process
  • Testing method
  • End-use environment

This system-level mindset also matches FPIC’s broader manufacturing strengths. According to FPIC company materials, the company supports connector development through:

  • Product design and tooling development
  • Metal stamping
  • Plastic injection molding
  • Auto assembly with CCD
  • Quality assurance testing
  • Automotive connector manufacturing under IATF 16949-related systems and process control

That manufacturing foundation matters because a good terminal design only delivers real value when it can also be produced consistently.

What Engineers and Buyers Should Ask Before Selecting a Terminal

When reviewing a connector concept, ask these questions:

1) What is the real operating environment?

Will the connector see:

  • Road vibration?
  • Temperature cycling?
  • Moisture?
  • Corrosive conditions?
  • Repeated mating?

If yes, a general square pin may not be the right solution.

2) Is insertion feel important?

Rounded automotive terminals generally provide smoother and more forgiving insertion behavior, especially when alignment is not perfect.

3) How important is long-term consistency?

If the product must stay reliable over years, especially in automotive or industrial systems, terminal geometry and plating consistency become much more important.

4) Will the part be made at scale?

If the project needs high automation, stable dimensions, and controlled plating, strip-based automotive-style terminal production has strong advantages.

Practical Selection Guide

Application ScenarioRecommended ChoiceWhy
Standard PCB headerStandard square pin terminalCost-effective and suitable for simple board-level use
Consumer electronicsStandard square pin terminalEnough performance for lower-stress environments
Automotive low-voltage connectorAutomotive rounded pin terminalBetter vibration resistance and long-term reliability
Signal connector in harsh industrial equipmentAutomotive rounded pin terminalBetter guidance and contact stability
High-reliability long-life designAutomotive rounded pin terminalBetter process consistency and service performance

Conclusion

A standard square pin terminal and an automotive rounded pin terminal may look similar at first glance, but they are built for different jobs.

The square pin version is a practical choice for general electronics where cost and simplicity matter most. The automotive rounded version is designed for a tougher world: vibration, temperature change, longer service life, and higher reliability requirements.

So if the project is automotive, or if the application behaves more like automotive in terms of durability demands, the safer decision is usually the automotive rounded terminal.

FAQ

1. Is a pin header the same as an automotive terminal?

No. A pin header usually refers to a connector category used on PCBs, while an automotive terminal refers to a terminal system designed for vehicle-grade electrical connection. Leading supplier catalogs treat them as separate categories.

2. Why are automotive terminals often rounded?

Because the rounded shape improves insertion guidance, reduces sharp-edge stress, supports more stable mating, and performs better in vibration-heavy environments.

3. Are square pin terminals bad?

Not at all. They are a good solution for the right application. The issue is not quality, but fit. They are simply intended for less demanding operating conditions than automotive terminals.

4. Does plating really make a big difference?

Yes. Plating consistency affects contact resistance, corrosion resistance, wear behavior, and long-term performance. Reel-to-reel precision plating generally offers better consistency for automotive terminals.

5. When should I choose the automotive rounded design?

Choose it when the connector must survive vibration, repeated mating, wider temperature exposure, and longer service life requirements.

Ready to choose the right terminal for your automotive or industrial application?

Explore FPIC’s complete range of low-voltage automotive connectors and bullet-head terminals for high-reliability, vibration-resistant, and long-life performance.

View Products: https://fpiconn.com/products/

Contact Sales: info@fpiconn.com

💡 Tip: Our engineering team can help you select the right terminal and connector solution for your exact application, including rapid prototyping and mass-production guidance

Resources

  1. FPIC Internal Technical Document: “Differences Between Automotive Low-Voltage Connector Terminals and Standard Pin Header Terminals”
    This internal FPIC source provided the core technical comparison for structure, process route, plating method, performance differences, and application recommendations used in this article.
  2. Aptiv – Connection Systems Catalog
    Aptiv’s official catalog clearly separates Terminals and Pin Headers into different product categories, which supports the terminology distinction used in this article.
    Link: https://www.aptiv.com/en/solutions/connection-systems/catalog
  3. VDA – Electrical/Electronic Components and General System Requirements
    VDA explains that automotive electrical and electronic components must continuously adapt to requirements involving safety, reliability, vibration, temperature, chemicals, and other operating conditions.
    Link: https://www.vda.de/en/topics/automotive-industry/standardization-and-technical-standards/e-e-components-and-general-system-requirements
  4. USCAR – EWCAP / Connector Validation Context
    USCAR materials help show the broader North American automotive context for connector and terminal validation work.
    Link: https://uscar.org/